Connect with us

Economy & Market

The main pushback against automation is budget

Published

on

Shares

Mehul Doshi, Head of Department — Customer Support and Service, HAVER & BOECKER, shares insights on leveraging diagnostics and optimisation tools to address challenges in automation of bagging, packaging, and palletising processes.

In the fiercely competitive cement industry, optimising bagging, packaging and palletising processes is no longer a luxury but a necessity. Cutting-edge diagnostics and tailored optimisation plans are transforming how plants enhance efficiency, reduce waste, and boost safety — all while advancing sustainability goals. Through a seamless blend of digital monitoring and hands-on audits, manufacturers are now able to identify bottlenecks, minimise product loss and future-proof their operations, shares Mehul Doshi, Head of Department — Customer Support and Service, HAVER & BOECKER, in this exclusive interview.

How do QUAT2RO® and POP enhance efficiency in bagging, packaging, and palletising for the cement industry?
Comprising the diagnostics section of HAVER & BOECKER’s PROcheck lifecycle approach, QUAT2RO® and the Plant Optimisation Plan (POP) help operations increase plant performance, optimise machine conditions, set up and use resources, raise health and safety standards and improve energy efficiency.
As the digital tool of HAVER & BOECKER’s diagnostics approach, QUAT2RO® collects short-term and long-term production data on all connected machines. The data combines performance and maintenance reports into a single dashboard to make monitoring equipment settings simple. QUAT2RO® System Monitoring alerts operators to any discrepancy in the packing or palletising machines to allow faster maintenance and increase efficiency on the packing line. HAVER & BOECKER recommends installing QUAT2RO® on packing lines before engaging in a Plant Optimisation Plan (POP) to collect information on the baseline performance of the line.
POP is the human approach toward diagnostics. For the POP, HAVER & BOECKER engineers visit the customer plant to observe the operation and recommend enhancements classified by level of urgency. The full plant audit considers all areas, from product storage and handling to packing, bag transport, palletising and loading lines, as well as surrounding machines and environmental factors. The engineers send a full report tagged with green, yellow or red to highlight areas for improvement, ensuring that critical updates are prioritised.
HAVER & BOECKER’s Bag Optimisation Plan (BOP) is a very important part of the POP and allows it to go beyond the mechanical equipment and into the important role of consumables. While the goal of the POP is to find the perfect harmony between the bag, the product and the machine, the BOP focuses on all aspects of the bag and includes a bag volume test, bag valve check, visual pallet check and a bag specification check. The HAVER & BOECKER Institute tests and analyses the bag and the product to optimise all three major factors in the packing process — machine, bag and product —resulting in the highest levels of productivity and efficiency.

What common challenges in cement packing plants do your diagnostics tools address, and how are the solutions tailored?
HAVER & BOECKER diagnostics tools primarily focus on production issues, whether that’s tracking equipment efficiency through QUAT2RO® or providing recommendations for optimising existing equipment and processes. One of the biggest challenges plants face is dust escaping as bags are filled. Most packing equipment comes in a one-size-fits-all approach, meaning it’s not optimised for each individual product. If not treated properly, free-flowing powder material like cement will settle on the floor, equipment and operators instead of in the bag. HAVER & BOECKER diagnostics, specifically their POP and BOP, considers the individual properties of the cement being poured and how to direct it into the bag most effectively.
The bags used for packing cement can contribute to the amount of material lost in the packing process. Unsealed valve bags rely on the inner pressure of the bag to close, which results in the bag being only 70 per cent closed, leaving a 30 per cent opening for spillage. An improperly sealed bag results in material loss at a rapid rate while in storage and throughout transport, leading to a total product loss of up to 5 per cent. That’s why HAVER & BOECKER offers SEAL technology. Ultrasonic sealing effectively welds bags shut, resulting in the bag being 100 per cent closed. Unlike adhesive closed bags, this type of seal means bags won’t unstick over time and cause spillage if left in storage. This bag also eliminates product loss during transport.
If a facility is seeing similar product loss in their plant, HAVER & BOECKER will address the type of bag being used and recommend an upgrade to SEAL technology in their optimisation plan. They will also address any dust production issues in the full packing line to optimise production.

How does QUAT2RO® improve process efficiency, and which KPIs are critical?
QUAT2RO® detects issues before they become critical to the packing line. Operators can monitor machines’ production rates in real time to see how their equipment is performing. The results can be used to check production levels and identify solutions to productivity challenges and inefficiencies. This data can show any bottlenecks in the packing line so operators can address the issue immediately.
All data is stored in a single online portal with customisable alert systems and report templates. The portal keeps track of maintenance intervals for all assemblies and components and sends early notifications as a reminder to order wear parts. The system can also be accessed by the HAVER & BOECKER service team, providing cement plants with direct contact with our experts to address any of their concerns.

How do your solutions support sustainability goals like energy efficiency and waste reduction?
Sustainability and energy efficiency are at the heart of what we do. HAVER & BOECKER offers 10 energy saving solutions for packing lines that cover everything from optimising equipment performance to keeping equipment clean and having equipment serviced regularly. Optimising machine performance leads to energy efficiency because any material that escapes the packing process is a loss, which means the rest of the production plant needs to produce more to make up for it. Having a packing line fully optimised is one easy way to ensure energy efficiency and waste reduction.

How does the PROcheck lifecycle approach integrate with existing equipment in cement plants?
One of the many benefits of PROcheck lifestyle approach is that it can be integrated into the cement plant’s processes at any time. The first step to a full PROcheck is the Plant Optimisation Plan where an engineer comes to visit the plant and assess the technology, packing line and product being produced. No matter what technology is currently in use, our engineers provide a full report addressing any concerns and suggesting updates.

What trends in bagging, packaging, and palletising are shaping the cement industry?
Sustainability and automation are prime motivators for the cement industry right now. Whether that’s completely automating processes to increase efficiency or using electric equipment to cut down on carbon emissions, cement producers want to be able to produce better quality cement with more technologically advanced equipment.
The industry has seen a huge push toward automation in many places around the world. However, the main pushback against automation is budget. Budgetary restrictions are universal and often hold cement plants back from taking the plunge. We recognise this need and have started working with The Portland Company to provide Assemble to Order packing equipment with introductory automation that helps plants start their journey with plenty of room to expand into more customised equipment with us later. This ensures that all operations, no matter where in the world they’re located, can get an automated option suited for their unique packing line and access best-in-class service.

How does POP (and BOP) ensure optimal coordination of machines, bags, and products?
A POP includes a full plant audit that considers all areas, from product storage and handling to packing, bag transport, palletising and loading lines as well as surrounding machines and environmental factors. The goal of the report is to give plant managers a thorough, solid idea of how their plant is currently performing and where critical updates need to be made. The full POP, including the BOP, considers machines, bags and products to give an overarching recommendation on how all of them can work together for the best results.
The HAVER & BOECKER Institute completes the BOP, checking the chemical composition of the product, how the machine can aerate the product for maximum efficiency in filling and which bags provide the best protection for that specific product. The goal is to have a cohesive packing line that works together in the most efficient way possible.

What new innovations or upgrades are you introducing to improve packing plant performance?
Our newest products are meant to continually improve the packing line and provide the best support possible throughout the packing process. One major update we’ve introduced is the AMICUS Advanced Robot Family. The AMICUS DEPAL Edition depalletises bags and places them on an automatic bag applicator while the AMICUS PAL Edition palletises bags, boxes, drums and pails for transport. The AMICUS DEPAL replaces a previously manual process and increases safety, which is one of the major benefits of the system. If a facility invests in both an AMICUS PAL and DEPAL, they can create a fully automated packing line from empty to full bag.
Another optimisation HAVER & BOECKER is focused on is the unique ADAMS® Technology. ADAMS® is the system for packing cement into PE bags, offering an unlimited list of advantages. There has been rapid growth in the way ADAMS® is used, including how it has expanded into the cement sector. The FFS film bags used with the ADAMS® ROTO-PACKER protect powder cement from the elements while in transit and in storage. The waterproof, weatherproof bags offer a variety of benefits to all the industries we touch, which is an exciting expansion of our pre-existing line.

Concrete

Capacity with Conscience

Published

on

By

Shares

Ambuja Cements has locked in its next phase of growth. The Adani Group company has earmarked 14,500 crore, roughly 145 billion, for greenfield and brownfield projects that will add 30 MTPA and lift its total capacity to 155 MTPA by FY2030.
It is hardly alone. The industry added about 55 million tonnes in FY2025-26, taking installed grinding capacity to an estimated 720 to 730 MT by March 2026. UltraTech Cement, Adani Cement, Shree Cement, Dalmia Bharat and JK Cement are expected to drive another 115 to 125 MT by FY2027-28. Production itself reached close to 490 million tonnes in FY26. The appetite to build is not in doubt.
Costs are another matter. The conflict in West Asia continues to push up fuel and freight bills, and the pressure on profitability is real. More capacity arriving in a market that is absorbing higher input costs leaves little room for inefficiency.
Then there is carbon. Indian cement emits around 0.62 tonnes of CO2 per tonne of cement, and the decarbonisation roadmap points to 0.56 by 2030 and 0.51 by 2047. Output, meanwhile, is projected to climb towards 1,546 million tonnes by 2070, the year India has set for net zero. Intensity can fall steadily while total emissions still rise. That is the arithmetic the industry must solve.
So, how does the sector sustain its expansion momentum while honouring its net-zero commitments? That question anchors the discussions at the Indian Cement Review Conference & Awards and Cement Expo 2026. More than 60 industry leaders will weigh how rising demand, capacity growth and productivity gains can sit alongside decarbonisation across the value chain. They will also examine which technologies, investments and strategies will make that possible.
The Expo runs from 15 to 17 December at India Expo Mart, Greater Noida. Come and be part of the answer.

Continue Reading

Concrete

The Clean Air Equation

Published

on

By

Shares

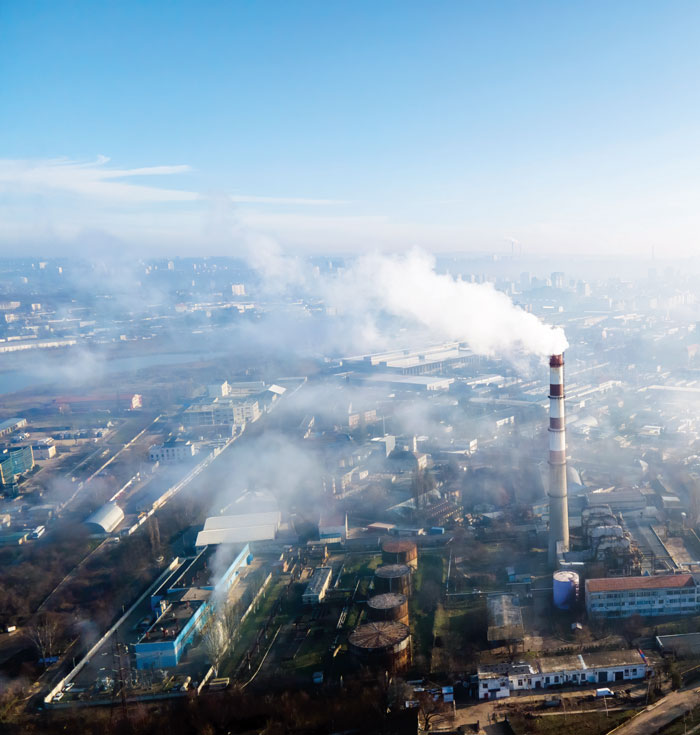
Indian Cement Review explores how cement manufacturers are combining advanced filtration, pollution-control technologies, cleaner fuels, carbon capture and digital monitoring to reduce emissions and achieve more sustainable, compliant and efficient operations.

India’s cement industry faces the dual challenge of meeting growing infrastructure demand while reducing its environmental footprint. According to the India Brand Equity Foundation (IBEF), cement production reached 491.4 million tonnes in FY2025–26, an 8.6 per cent year-on-year increase. As production expands, controlling particulate matter, nitrogen oxides (NOx), sulphur oxides (SOx) and carbon dioxide (CO2) is becoming increasingly important. The American Council for an Energy-Efficient Economy (ACEEE) estimates that cement production accounts for approximately 6 to 7 per cent of India’s greenhouse gas emissions, underlining the need for effective emissions-management strategies.
The challenge is particularly complex because cement emissions arise from both fuel combustion and the chemical conversion of limestone into clinker. According to NITI Aayog’s Roadmap for Cement Sector Decarbonisation, the sector emitted approximately 246 million tonnes of CO2-equivalent in 2023, with an emissions intensity of 0.63 tonnes of CO2-equivalent per tonne of cement. Meanwhile, the Central Pollution Control Board (CPCB) has established particulate-matter emission standards for cement plants, reinforcing the importance of effective dust collection and pollution-control systems. For manufacturers, the priority is to combine advanced filtration, cleaner fuels, process optimisation and emerging carbon-capture technologies to meet regulatory requirements while maintaining production efficiency and cost competitiveness.

Understanding emissions
Emissions from cement manufacturing originate primarily from kiln operations, fuel combustion and the chemical conversion of limestone into clinker. CO2 is released both when fossil fuels are burned to generate heat and when limestone decomposes during calcination. According to the International Energy Agency (IEA), around two-thirds of direct CO2 emissions from cement production arise from the chemical process of clinker production, with the remainder largely associated with fuel combustion. Alongside greenhouse gases, cement plants generate particulate matter (PM) during crushing, grinding, kiln operations and material handling, while nitrogen oxides (NOx) form at high combustion temperatures and sulphur oxides (SOx) can arise from sulphur present in raw materials and fuels.
Dr LP Singh, Director General, National Council for Cement and Building Materials, at the 16th Edition of the Conference on Alternative Fuel & Raw Material Usage (AFR) said, “AFR offers the Indian cement industry a significant opportunity to advance decarbonisation while addressing waste management challenges. The fly ash journey demonstrates how innovation and industry collaboration can transform waste into a valuable resource. Replicating this success with AFR will require addressing quality, technology and economic challenges through stronger collaboration among industry, researchers and policymakers to accelerate the transition to a circular economy.”
The scale of these emissions varies with raw-material composition, kiln technology, fuel mix and pollution-control equipment. A 2026 report by the American Council for an Energy-Efficient Economy (ACEEE) estimates that limestone calcination contributes approximately 56 per cent of India’s cement-sector emissions, fuel combustion 32 per cent and electricity use 12 per cent. Meanwhile, India’s Central Pollution Control Board (CPCB) identifies crushers, coal mills, raw mills, kilns, clinker coolers, cement mills and packing plants as major sources of particulate emissions. Understanding these sources is essential to selecting appropriate controls, from bag filters and electrostatic precipitators to combustion optimisation and carbon capture, while ensuring compliance with environmental standards.

Advanced air pollution control
Particulate matter is generated at several stages of cement manufacturing, including limestone crushing, raw-material grinding, kiln operations, clinker cooling, cement milling and packing. Modern air pollution control systems use electrostatic precipitators (ESPs) and bag filters to capture dust before exhaust gases are released into the atmosphere. ESPs remove particles by electrically charging them and collecting them on plates, while bag filters trap dust as gases pass through specialised filter media. Enclosed conveyors, covered storage, efficient dust extraction and automated material-handling systems further help prevent fugitive emissions across the plant.
The Central Pollution Control Board (CPCB) identifies crushers, coal mills, raw mills, kilns, clinker coolers, cement mills and packing plants as major sources of particulate emissions. Its guidance highlights the use of ESPs, baghouse filters and hybrid filtration systems to control dust at these points. The World Bank Group’s Environmental, Health, and Safety Guidelines for Cement and Lime Manufacturing also recommend enclosing material-transfer points, using water sprays and dust suppressants, and maintaining paved roads and effective housekeeping to limit fugitive dust. Combining high-efficiency filtration with preventive maintenance and improved material handling is therefore essential to reducing dust emissions and maintaining compliance with applicable standards.

Controlling NOx and Sox
NOx and SOx require targeted control strategies because they arise from different sources within cement manufacturing. NOx forms mainly during high-temperature kiln combustion, while SOx emissions depend on the sulphur content of fuels and raw materials. Low-NOx burners, staged combustion and optimised kiln operating conditions help limit NOx formation, while selective non-catalytic reduction (SNCR) and selective catalytic reduction (SCR) reduce NOx in exhaust gases through chemical reactions. For SOx, manufacturers can optimise raw-material selection and kiln conditions or deploy suitable gas-treatment systems to capture sulphur compounds before release.
The World Bank Group’s Environmental, Health, and Safety Guidelines for Cement and Lime Manufacturing (2022) provide indicative emission levels of 600 mg/Nm3 for NOx and 400 mg/Nm3 for SO2 from cement kiln stacks, subject to the guideline’s specified operating and measurement conditions. European Commission best available techniques (BAT) conclusions also identify low-NOx burners, staged combustion and SNCR as key NOx-control options, with SCR available where appropriate. For cement manufacturers, selecting the right combination depends on kiln design, fuel and raw-material chemistry, emissions targets and operating costs; continuous monitoring is essential to verify performance and maintain compliance.

Carbon capture and low-carbon cement
Decarbonising cement requires solutions that go beyond improving energy efficiency because a substantial share of emissions comes from the chemical decomposition of limestone during clinker production. Clinker substitution offers an immediate pathway to reduce this impact by incorporating supplementary cementitious materials (SCMs), such as fly ash, blast furnace slag and calcined clay, into cement formulations. Limestone calcined clay cement (LC3) and other blended cements can lower clinker content while maintaining the performance required for construction. These innovations also encourage the productive use of industrial by-products and locally available materials, helping manufacturers reduce the carbon intensity of cement.
Carbon capture, utilisation and storage (CCUS) offers another pathway for addressing residual process emissions. According to the Global Cement and Concrete Association’s Cement Industry Net Zero Progress Report 2024/25, CCUS is expected to contribute 36 per cent of the cement and concrete industry’s emissions reductions by 2050 under its net-zero roadmap. In India, the Department of Science and Technology announced five CCU testbeds for the cement sector in 2025 to demonstrate technologies that capture CO2 and convert it into value-added products, including concrete aggregates and synthetic fuels, as reported by the Press Information Bureau. Scaling these innovations will depend on technological maturity, investment, infrastructure and standards that support wider adoption of low-carbon cement.

Extending emission control beyond the plant
Emission control in cement manufacturing must extend beyond the production line to include the transportation of raw materials, fuels and finished cement. Road transport contributes to fuel consumption, greenhouse gas emissions and particulate pollution, particularly around plant gates, loading areas and distribution routes. Optimising truck movements, reducing vehicle idling and improving fleet utilisation can help minimise these impacts. Covered conveyors, enclosed loading systems and effective dust suppression at material transfer points can further reduce fugitive dust during handling and transportation.
Vinita Singhania, Chairperson and Managing Director, JK Lakshmi Cement, said, “At JK Lakshmi Cement, we are focused on integrating sustainable practices across our operations while ensuring long-term business efficiency. With a fleet of 70+ electric vehicles currently operating across our logistics network, we are making tangible progress in adopting cleaner transportation solutions. The transition to EV-based clinker dispatches on the Sirohi–Kalol route is an important milestone in this journey and reinforces our commitment to scaling sustainable logistics as part of our broader decarbonisation strategy.”
Shifting suitable freight from road to rail, improving vehicle maintenance and adopting digital logistics platforms can further support emission reduction across the cement supply chain. GPS based fleet tracking and route optimisation can reduce unnecessary travel, while bulk cement transportation can help limit packaging waste and handling related dust. Integrating these measures with plant level emissions monitoring provides a more comprehensive approach to pollution management, recognising that cleaner cement manufacturing depends not only on controlling emissions at the kiln but also on how materials and products move through the supply chain.
Anand Mimani, CEO – EV and New Energy Business, Blue Energy Motors, says “As India accelerates its transition towards a lower-carbon future, decarbonising freight transportation will be critical to achieving meaningful emissions reductions. Electric heavy-duty trucks are increasingly proving their ability to deliver the performance, reliability and economics required for commercial operations. This deployment is a strong example of how clean mobility solutions can help industries reduce transportation-related emissions while advancing their broader sustainability ambitions.”

Digital monitoring and regulatory compliance
Continuous Emissions Monitoring Systems (CEMS) are helping cement manufacturers move from periodic testing towards real-time emissions tracking. These systems measure pollutants such as particulate matter (PM), nitrogen oxides (NOx) and sulphur dioxide (SO2), transmitting data to plant operators and regulatory authorities. The Central Pollution Control Board (CPCB) identifies cement as a sector requiring online monitoring of PM, NOx and SO2, with data connected to regulatory servers. Integrating CEMS with automated process controls and analytics can help operators identify emission spikes, investigate their causes and adjust kiln combustion, fuel feed or pollution-control equipment before deviations persist.
However, monitoring is only effective when the data is reliable and acted upon. A 2024 report by the Council on Energy, Environment and Water (CEEW) highlights the need to improve the accuracy and credibility of India’s industrial emissions-monitoring data, despite the widespread adoption of CEMS. Regular calibration, equipment maintenance, data validation and cross-checking against approved reference methods are therefore essential. When combined with predictive analytics and automated alerts, reliable emissions data can strengthen regulatory reporting, support faster corrective action and help cement plants balance environmental compliance with operational efficiency.

Conclusion
Emission control in cement plants requires a comprehensive approach that combines advanced pollution-control technologies, energy efficiency and process innovation. From high-efficiency bag filters and NOx and SOx treatment systems to alternative fuels, low-carbon cement formulations and carbon capture, these solutions offer multiple pathways to reduce the industry’s environmental footprint. Digital monitoring and real-time analytics further strengthen these efforts by enabling manufacturers to identify emission spikes, optimise plant operations and improve regulatory compliance. The challenge lies in integrating these technologies effectively while maintaining production reliability and cost competitiveness.
As India’s cement demand continues to grow, the industry must move beyond compliance-driven measures towards a proactive, long-term emissions-reduction strategy. Greater investment in research and development, modern infrastructure, reliable emissions monitoring and collaboration between manufacturers, technology providers and policymakers will be essential to scaling effective solutions. Ultimately, the future of cleaner cement manufacturing will depend on translating technological advances into measurable environmental improvements, ensuring that industrial growth goes hand in hand with resource efficiency, responsible production and India’s broader decarbonisation ambitions.


  • Kanika Mathur

Continue Reading

Concrete

Decarbonisation in the Indian Cement Industry

Published

on

By

Shares

Authored by Jordana Georgin, Dison S. P. Franco, Claudete Gindri Ramos and Noureddine El Messaoudi, this review, published in Sustainability (Vol. 18, 2026, Article 7383), examines cement industry impacts on air, water, soil and noise, and assesses technologies to mitigate pollution and ecological risks.

The report identifies cement manufacturing as a significant contributor to India’s greenhouse gas emissions, accounting for approximately 6 per cent to 7 per cent of the country’s total emissions. It identifies three principal sources: limestone calcination, responsible for 56 per cent of sector emissions; fuel combustion, contributing 32 per cent; and electricity consumption, accounting for the remaining 12 per cent. Despite significant improvements in energy efficiency over the past decade, the report notes that further reductions will require structural changes in production processes, material utilisation and energy sourcing.
India’s cement industry already operates among the world’s most energy-efficient sectors, with average thermal energy consumption of approximately 731 kcal/kg of clinker and electrical energy consumption of 73 kWh/tonne of cement, compared with global averages of 838 kcal/kg and 104 kWh/tonne, respectively. The report emphasises that future decarbonisation must therefore go beyond incremental efficiency improvements and focus on alternative fuels, clinker substitution, renewable electricity and carbon capture.

Strategic levers for reducing emissions
The report identifies five strategic levers for decarbonisation. Increasing the use of alternative fuels such as biomass and refuse-derived fuel (RDF) could reduce dependence on conventional fossil fuels; however, these fuels currently account for only 6 per cent of the energy used to heat cement kilns in India. The report recommends increasing the thermal substitution rate to 20 per cent by 2030, supported by reliable fuel supplies and streamlined transportation and approval systems.
Clinker substitution through supplementary cementitious materials (SCMs), including fly ash, slag and limestone calcined clay cement (LC3), offers another significant opportunity, with the potential to address 7 to 15 per cent of cement-sector emissions. The report also identifies electricity decarbonisation through renewable power, waste heat recovery and efficient grinding systems as important interventions. India’s installed waste heat recovery capacity stands at 538 MW, with potential to reach approximately 1,100 MW.

Emerging technologies and low-carbon cement
The report highlights LC3, composite cement and geopolymer cement as promising alternatives to conventional Portland cement. LC3 combines clinker, calcined clay, limestone and gypsum, with the potential to reduce CO2 emissions by up to 40 per cent compared with traditional Portland cement. Pilot projects and early commercial trials in India have demonstrated clinker reductions of 30 per cent to 40 per cent while maintaining comparable performance to ordinary Portland cement (OPC). The report also identifies Noida International Airport (Jewar) as India’s first large-scale deployment of LC3.
Carbon capture, utilisation and storage (CCUS) is identified as a long-term solution for addressing process emissions that cannot be eliminated through conventional efficiency measures. The report notes that carbon capture costs typically range from US$ 40–120 per tonne of CO2, highlighting the need for supportive policies, shared infrastructure and investment. Emerging technologies such as mineralisers, fluidised-bed calcination, low-pressure-drop cyclones and high-efficiency classifiers are also identified as opportunities to further reduce energy consumption and emissions.

Conclusion
The report recommends a phased approach to decarbonisation, beginning with the scaling of composite cement, LC3, alternative fuels, renewable electricity and waste heat recovery between 2025 and 2030. The second phase, covering 2030–2040, focuses on higher alternative-fuel substitution rates, electric logistics fleets and emerging technologies such as oxyfuel kilns. The final phase, from 2040 to 2070, prioritises the deployment of CCUS and potentially green hydrogen to address residual emissions.
The study concludes that achieving India’s net zero ambitions will require coordinated action across the cement value chain, supported by technology development, investment, evolving standards and stronger policy frameworks. It also highlights the importance of market acceptance and demand-side measures, including green public procurement and low-carbon construction practices. By combining immediate efficiency improvements with long-term technological transformation, India’s cement industry can reduce emissions while maintaining competitiveness and supporting sustainable infrastructure growth.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds