Connect with us

Concrete

Beyond Despatch: Building a Strategic Supply Chain Process

Published

on

Shares

Dr SB Hegde, Global Cement Industry Leader discusses the imperative need for modern cement plants to recognise packaging and bag traceability as critical components of quality assurance and supply chain management.

In cement manufacturing, considerable attention is given to clinker quality, kiln operation, grinding efficiency and laboratory control. Yet the final stage of the process, cement packaging and despatch, often receives less strategic focus. The cement bag leaving the plant gate represents the final interface between the manufacturer and the customer. Even if clinker chemistry, fineness and strength development are well controlled, weaknesses in packaging, handling, or distribution can affect product quality before it reaches the construction site.
Operational experience from cement plants across different regions shows that packaging efficiency and bag traceability have a significant influence on product reliability, logistics performance and brand credibility. In modern cement plants, packaging systems are no longer viewed merely as despatch equipment. They are increasingly recognised as an important part of quality assurance, supply chain management and customer confidence.

Operational importance of packaging
Cement packaging systems must operate with high speed, accuracy and reliability to support efficient despatch operations. Rotary packers equipped with electronic weighing systems have improved packing accuracy and productivity in many plants.
However, maintaining operational discipline remains essential. Regular calibration of weighing systems, maintenance of packer spouts and proper bag application are important for maintaining consistent bag weights and preventing cement loss.
Operational benchmarks observed in many cement plants are summarised in Table 1.
Plants that improved calibration discipline and equipment maintenance have reported packing loss reductions of about 1 per cent to 1.5 per cent, which represents significant annual savings.

Quality assurance beyond the plant gate
Quality control in cement plants traditionally focuses on laboratory parameters such as fineness, compressive strength and chemical composition. However, the condition of cement when it reaches the customer is equally important.
Cement bags may travel through several stages including plant storage, transport vehicles, dealer warehouses and retail outlets before reaching the construction site. During this journey, cement may be exposed to humidity, rough handling and improper storage conditions.
Table 2 shows common factors that may affect cement quality during distribution.
Studies indicate that cement stored under humid conditions for long periods may experience 10 per cent to 20 per cent reduction in early strength. Therefore, maintaining proper packaging integrity and traceability is essential.

Role of cement bag traceability systems
Traceability systems allow manufacturers to identify when and where cement was produced and despatched. These systems connect packaging operations with production records and logistics data.
When customer complaints occur, traceability enables manufacturers to identify:

  • Production batch
  • Packing date and time
  • Plant location
  • Laboratory test results

Several technologies are used to implement bag traceability, as shown in Table 3.
Among these technologies, QR code authentication systems are becoming popular because customers can verify product authenticity through smartphones.

Digital transformation
Digital technologies are transforming cement packaging operations. Modern packing lines now integrate:

  • automated rotary packers
  • electronic bag counting systems
  • robotic palletising systems
  • ERP-based despatch management
  • digital supply chain monitoring

These technologies improve operational efficiency and transparency across the supply chain.
Such systems help manufacturers track cement movement across the distribution network and respond quickly to quality concerns.

Case Study: Digital Cement Bag Authentication
Several cement manufacturers in Asia and the Middle East have implemented QR code-based bag authentication systems to improve supply chain transparency.
In one integrated cement plant, QR codes were integrated into the rotary packing machine. Each cement bag received a unique digital identity linked to the production database.
The QR code contained information such as:
• plant location
• manufacturing date and time
• product type
• batch number

Customers and dealers could scan the code using a mobile application to verify product authenticity.
After implementation, the company reported:
• reduction in counterfeit bag circulation
• improved despatch data accuracy
• faster resolution of customer complaints
• better visibility of distribution networks

The system was also integrated with the company’s ERP platform, enabling real-time monitoring of production and despatch activities.

Future-Smart Packaging Systems
The future of cement packaging lies in the integration of Industry 4.0 technologies with logistics and supply chain management.
Packaging lines will increasingly become part of connected digital ecosystems linking production, quality control, despatch and market distribution.
Artificial intelligence and data analytics may also help detect abnormalities in bag weight variations, equipment performance and despatch patterns.

Global benchmark indicators
Global benchmarking of cement packaging operations highlights the increasing importance of efficiency, automation and digital traceability in modern cement supply chains. Leading cement plants are now focusing on key performance indicators such as packer availability, bag weight accuracy, packing losses, truck turnaround time and digital traceability coverage. Studies show that overall equipment effectiveness (OEE) in many industrial operations is still around 65 per cent to 70 per cent, whereas world-class plants aim for levels above 85 per cent, indicating significant scope for improvement in operational efficiency.
At the same time, the global cement packaging sector is expanding steadily, supported by growing infrastructure demand and increased emphasis on reliable and moisture-resistant packaging solutions. The cement packaging market is projected to grow steadily in the coming decade as companies adopt automation, smart packaging technologies and integrated logistics systems to improve despatch efficiency and supply chain transparency. In this context, benchmarking against global indicators helps cement plants identify performance gaps and adopt best practices such as automated bagging systems, QR-based traceability, ERP-linked despatch monitoring, and predictive maintenance of packing equipment.

Strategic Recommendations
To fully benefit from packaging and traceability systems, cement manufacturers should consider the following approaches.
• Packaging systems should be treated as an integral part of the manufacturing value chain rather than simply despatching equipment.
• Investments in modern packers, automated loading systems and digital traceability technologies should be encouraged.
• Industry associations may also promote standard traceability practices to reduce counterfeit products and improve transparency in the cement market.
Finally, continuous training of plant personnel in packaging operations and maintenance practices is essential for sustaining operational efficiency.

Conclusion
Cement packaging has evolved from a routine mechanical operation into a strategic component of modern cement manufacturing. Efficient packaging systems ensure that the quality achieved within the plant is preserved during transportation and distribution. Traceability technologies allow manufacturers to track cement movement, investigate complaints and prevent counterfeit products.
As the cement industry moves toward digitalisation and integrated supply chains, packaging and bag traceability will play an increasingly important role in quality assurance, operational efficiency and customer confidence. Ultimately, the cement bag leaving the plant carries not only cement but also the reputation and responsibility of the manufacturer.

References

  1. Hewlett, P.C., & Liska, M. (2019). Lea’s Chemistry of Cement and Concrete. Butterworth-Heinemann.
  2. Schneider, M., Romer, M., Tschudin, M., & Bolio, H. (2011). Sustainable cement production. Cement and Concrete Research, 41(7), 642–650.
  3. International Cement Review. (2023). Advances in cement packaging and logistics systems.
  4. World Business Council for Sustainable Development (2021). Cement Industry Supply Chain Innovation Report.
  5. Gartner, E., & Hirao, H. (2015). Reducing CO2 emissions in cement production. Cement and Concrete Research.
  6. ScienceDirect Industry Studies. (2024). Operational efficiency benchmarks and overall equipment effectiveness in industrial manufacturing systems.
  7. World Cement Association. (2022). Digital Transformation in Cement Manufacturing and Logistics. London.
  8. Towards Packaging Research. (2024). Global cement
    packaging market trends and technology outlook. Industry Market Analysis Report.
  9. Towards Packaging Research. (2024). Global cement
    packaging market trends and technology outlook. Industry Market Analysis Report.

About the author:
Dr SB Hegde is a Professor at Jain College of Engineering, Karnataka, and Visiting Professor at Pennsylvania State University, USA. With 248 publications and 10 patents, he specialises in low-carbon cement, Industry 4.0, and sustainability, consulting with cement companies to support India’s net-zero goals.

Table 1. Key Operational Parameters for Cement Packaging Systems

Parameter Typical Industry Range Recommended Target Operational Significance
Rotary packer capacity 2400–3600 bags/hr 3000–4000 bags/hr Improves despatch efficiency
Bag weight tolerance ±0.5 kg ±0.25 kg Reduces customer complaints
Bag leakage rate 1 per cent to 2 per cent <0.5 per cent Minimises cement loss Packing accuracy 98 per cent to 99 per cent >99.5 per cent Ensure compliance with standards
Truck loading time 30–45 minutes 20–30 minutes Improves logistics efficiency

Table 2. Causes of Cement Quality Degradation During Distribution
Factor Typical Cause Impact on Cement
Moisture exposure Poor storage or rain exposure Lump formation
Long storage duration Slow inventory turnover Loss of early strength
Bag damage Rough handling Cement loss
Improper stacking Excessive loading Bag rupture
Counterfeit bag reuse Refilling of empty bags Brand damage

Table 3. Comparison of Cement Bag Traceability Technologies
Technology Advantages Limitations
Printed batch code Low cost and simple Limited traceability
Barcode Fast scanning Requires equipment
QR code Smartphone verification Requires digital platform
RFID tagging Automated tracking Higher cost
Blockchain systems High transparency Complex implementation

Concrete

ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown

Published

on

By

Shares

ABB reconditions 25 drives at ACC’s Jamul cement plant, avoiding 16 tonnes of CO₂ emissions while improving reliability through predictive maintenance.
Chhattisgarh

ABB has signed a multi-year Motion OneCare service agreement with ACC Limited, part of the Adani Group, to modernise ageing industrial drives at its Jamul cement plant in Chhattisgarh, improving operational reliability while avoiding approximately 16 tonnes of carbon dioxide (CO₂) emissions without disrupting production.

Announced on 27 October 2026, the agreement combines scheduled drive reconditioning, digital condition monitoring and energy appraisals to extend equipment lifespan, improve plant uptime and optimise maintenance costs. The initiative marks a shift from conventional equipment replacement towards a more resource-efficient approach to industrial asset management.

The first phase, completed in April 2026, involved the on-site reconditioning of 25 ABB ACS800 variable speed drives without a major plant shutdown. By retaining the existing cabinets and restoring the drive modules rather than replacing entire panels, ABB helped ACC preserve capital investment, minimise material consumption and avoid approximately 16 tonnes of CO₂ emissions.

A second phase, covering an additional 25 ACS800 drive modules, is scheduled for the fourth quarter of 2026. The programme is designed to improve long-term equipment reliability while allowing maintenance activities to be aligned with the plant’s operational schedules.

The ACS800 drives, installed at Jamul in 2010, had delivered more than a decade of near-continuous service in demanding cement manufacturing conditions. However, ageing electrical components and changing fault patterns had begun to affect their ability to meet the plant’s reliability requirements.

Rather than opting for complete equipment replacement, ACC engaged ABB’s certified engineers to conduct a comprehensive asset health assessment. The evaluation found that the existing cabinets and enclosures remained structurally sound, making targeted reconditioning a technically viable and cost-effective alternative to full replacement.

Drawing on nearly two decades of experience with ACC’s equipment and operating requirements, ABB developed a maintenance framework tailored to the plant’s shutdown windows, budget cycles and production priorities.

The Motion OneCare agreement incorporates planned equipment restoration, condition-based monitoring and energy assessments, enabling ACC to adopt a more systematic approach to maintaining critical electrical infrastructure.

As part of the programme, ACC has implemented ABB Ability™ Digital Powertrain Insights to monitor drive performance and identify emerging operational issues before they result in equipment failures.

The digital platform provides continuous visibility into parameters such as temperature, current, vibration and fault patterns. These insights allow maintenance teams to detect early signs of equipment deterioration, schedule interventions more effectively and reduce the likelihood of unexpected downtime.

Amit Gupta, Local Division Manager, Motion Services, ABB India, said: “We know what unchecked wear costs over time: a small inefficiency that eats away at ROI for years. At Jamul, the evidence pointed clearly to assets with productive life still in them.”

“Our job was to restore them properly and give the team the tools to stay ahead of the next problem. At ABB, we don’t just fix what fails. We want to protect what works.”

The initiative also demonstrates the growing relevance of circular economy principles in cement manufacturing, where extending the service life of existing industrial equipment can reduce capital expenditure, material consumption and the environmental impact associated with manufacturing replacement components.

According to ABB, drive reconditioning can reduce lifecycle emissions by 50 to 80 per cent compared with complete equipment replacement. By preserving functional components and restoring critical modules, the process helps retain the economic and material value of existing industrial assets.

The addition of energy appraisals in subsequent phases will further expand the programme beyond equipment restoration, enabling ACC to assess drive performance, identify energy-saving opportunities and improve operating efficiency.

For cement manufacturers, variable speed drives play an important role in controlling motors and optimising energy consumption across production processes. Maintaining their reliability and efficiency is essential for minimising operational disruptions and managing electricity costs.

Vinod Bahety, CEO – Cement Business, Adani Group, said: “Moving from reactive firefighting to a structured maintenance plan was exactly what this operation needed. That kind of peace of mind doesn’t come easily. It comes from a partner that understands how your business runs.”

“We didn’t need a full system overhaul; we needed expert support, actionable insights, and a plan we could execute around our schedule. That’s what we got.”

The project supports ACC’s broader strategy to improve manufacturing efficiency through digital transformation, preventive maintenance and sustainable asset management.

ACC, a subsidiary of Ambuja Cements and part of the Adani Group, operates 20 cement manufacturing facilities and 119 ready-mix concrete plants across India. The company has been advancing initiatives focused on renewable energy, circular economy practices and technology-driven operational improvements.

Alongside Ambuja Cements, ACC is part of a large-scale building materials business committed to achieving net-zero emissions by 2050, with near-term and net-zero targets validated by the Science Based Targets initiative (SBTi).

The Jamul initiative aligns with these sustainability objectives by demonstrating how equipment life extension and digital monitoring can contribute to resource efficiency without requiring large-scale replacement of existing infrastructure.

ABB, a global technology company specialising in electrification and automation, brings more than 140 years of industrial expertise and employs approximately 110,000 people worldwide. Its Motion Services business supports industrial customers through equipment maintenance, modernisation, digital monitoring and lifecycle management solutions.

The agreement also reflects a wider shift in industrial maintenance practices, with manufacturers increasingly adopting predictive technologies to improve equipment availability, manage costs and reduce unplanned shutdowns.

With 25 drives already reconditioned and another 25 scheduled for restoration, ABB’s collaboration with ACC illustrates how targeted modernisation, digital monitoring and circular maintenance practices can extend the operational life of critical equipment while supporting more efficient and sustainable cement production.


Continue Reading

Concrete

ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K

Published

on

By

Shares

ABB deploys advanced process control at TCI MAX’s Srinagar cement plant to improve clinker quality, energy efficiency and sustainable manufacturing.

Kashmir 

ABB has deployed its advanced process control technology at TCI MAX Cement’s Srinagar facility in Jammu and Kashmir, marking the region’s first reported implementation of advanced process control (APC) in cement manufacturing and strengthening efforts towards more efficient, digitally enabled production.

Announced on 5 November 2026, the deployment of ABB Ability™ Expert Optimizer at the facility, operated by Trumboo Industries Pvt. Ltd., aims to improve process stability, clinker quality, energy efficiency and overall plant productivity. The implementation forms part of TCI MAX’s strategy to modernise its manufacturing operations through automation and digital technologies.

Following the integration of ABB’s advanced process control solution and supporting IT infrastructure, TCI MAX has reported improvements in operational productivity, product quality and sustainability-related performance indicators. The technology focuses on optimising the cement pyro process, a critical stage of production involving high-temperature processing and clinker formation.

Waseem Ahmed Trumboo, Director, Trumboo Industries Pvt. Ltd., said: “Introducing advanced process control at TCI MAX is an important step in how we are evolving our operations. Our focus is on improving the stability and efficiency of our processes while maintaining consistent clinker quality. We have been encouraged by the performance of the solution during commissioning and by the support from the ABB team, and we look forward to realizing its full potential.”

ABB Ability™ Expert Optimizer combines advanced process control, model predictive control (MPC) and artificial intelligence (AI) to continuously monitor and optimise manufacturing operations. By analysing process conditions, predicting operational behaviour and automatically adjusting key parameters, the system enables more consistent production while reducing process variability.

In cement manufacturing, maintaining stable pyro-processing conditions is essential for achieving uniform clinker quality and optimising thermal energy consumption. Fluctuations in operating parameters can affect fuel efficiency, production output and product consistency.

The deployment is designed to address these challenges through real-time process optimisation, helping operators maintain more stable kiln operations while improving the utilisation of fuel, electricity and raw materials.

Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries Division, ABB India, said: “Cement producers are increasingly looking to adopt digital technologies to achieve greater consistency and efficiency while addressing their sustainability priorities. ABB Ability™ Expert Optimizer brings advanced process control and deep cement process expertise together to help operators make their processes more stable and efficient. We are pleased to support TCI MAX as it takes this important step in its digital transformation.”

The technology also supports sustainability objectives by optimising fuel consumption, improving electrical energy efficiency and minimising process waste. More stable operations can contribute to lower energy intensity and reduced emissions associated with cement production.

For TCI MAX, the investment represents a move towards data-driven manufacturing, where automated control systems complement operator expertise to improve production performance and operational reliability.

The implementation is particularly significant for Jammu and Kashmir’s cement industry, as it introduces advanced process optimisation technology to a regional manufacturing facility. Its deployment could demonstrate the potential for wider adoption of digital automation across cement plants seeking to modernise their operations.

The project builds on ABB’s experience in delivering advanced process control solutions to cement manufacturers worldwide. Through the integration of industrial automation, predictive technologies and process engineering expertise, the company supports manufacturers in improving resource efficiency and maintaining consistent production quality.

As cement producers face increasing pressure to manage energy costs, improve productivity and reduce their environmental footprint, technologies such as AI-enabled process control and predictive optimisation are becoming important components of plant modernisation strategies.

ABB’s Expert Optimizer provides a platform for addressing these priorities by enabling automated adjustments based on changing process conditions, reducing reliance on manual intervention and supporting more efficient plant operation.

ABB, a global technology company specialising in electrification and automation, has more than 140 years of industrial experience and approximately 110,000 employees worldwide. Its Automation business employs around 26,000 people and provides technologies and services across process, hybrid and maritime industries.

The TCI MAX deployment reinforces ABB’s growing role in the digital transformation of cement manufacturing in India, where improving process efficiency and reducing energy consumption remain critical to the industry’s long-term sustainability.

With the advanced process control system now implemented at its Srinagar facility, TCI MAX aims to build on the initial operational improvements and further optimise production efficiency, clinker consistency and environmental performance.

Continue Reading

Concrete

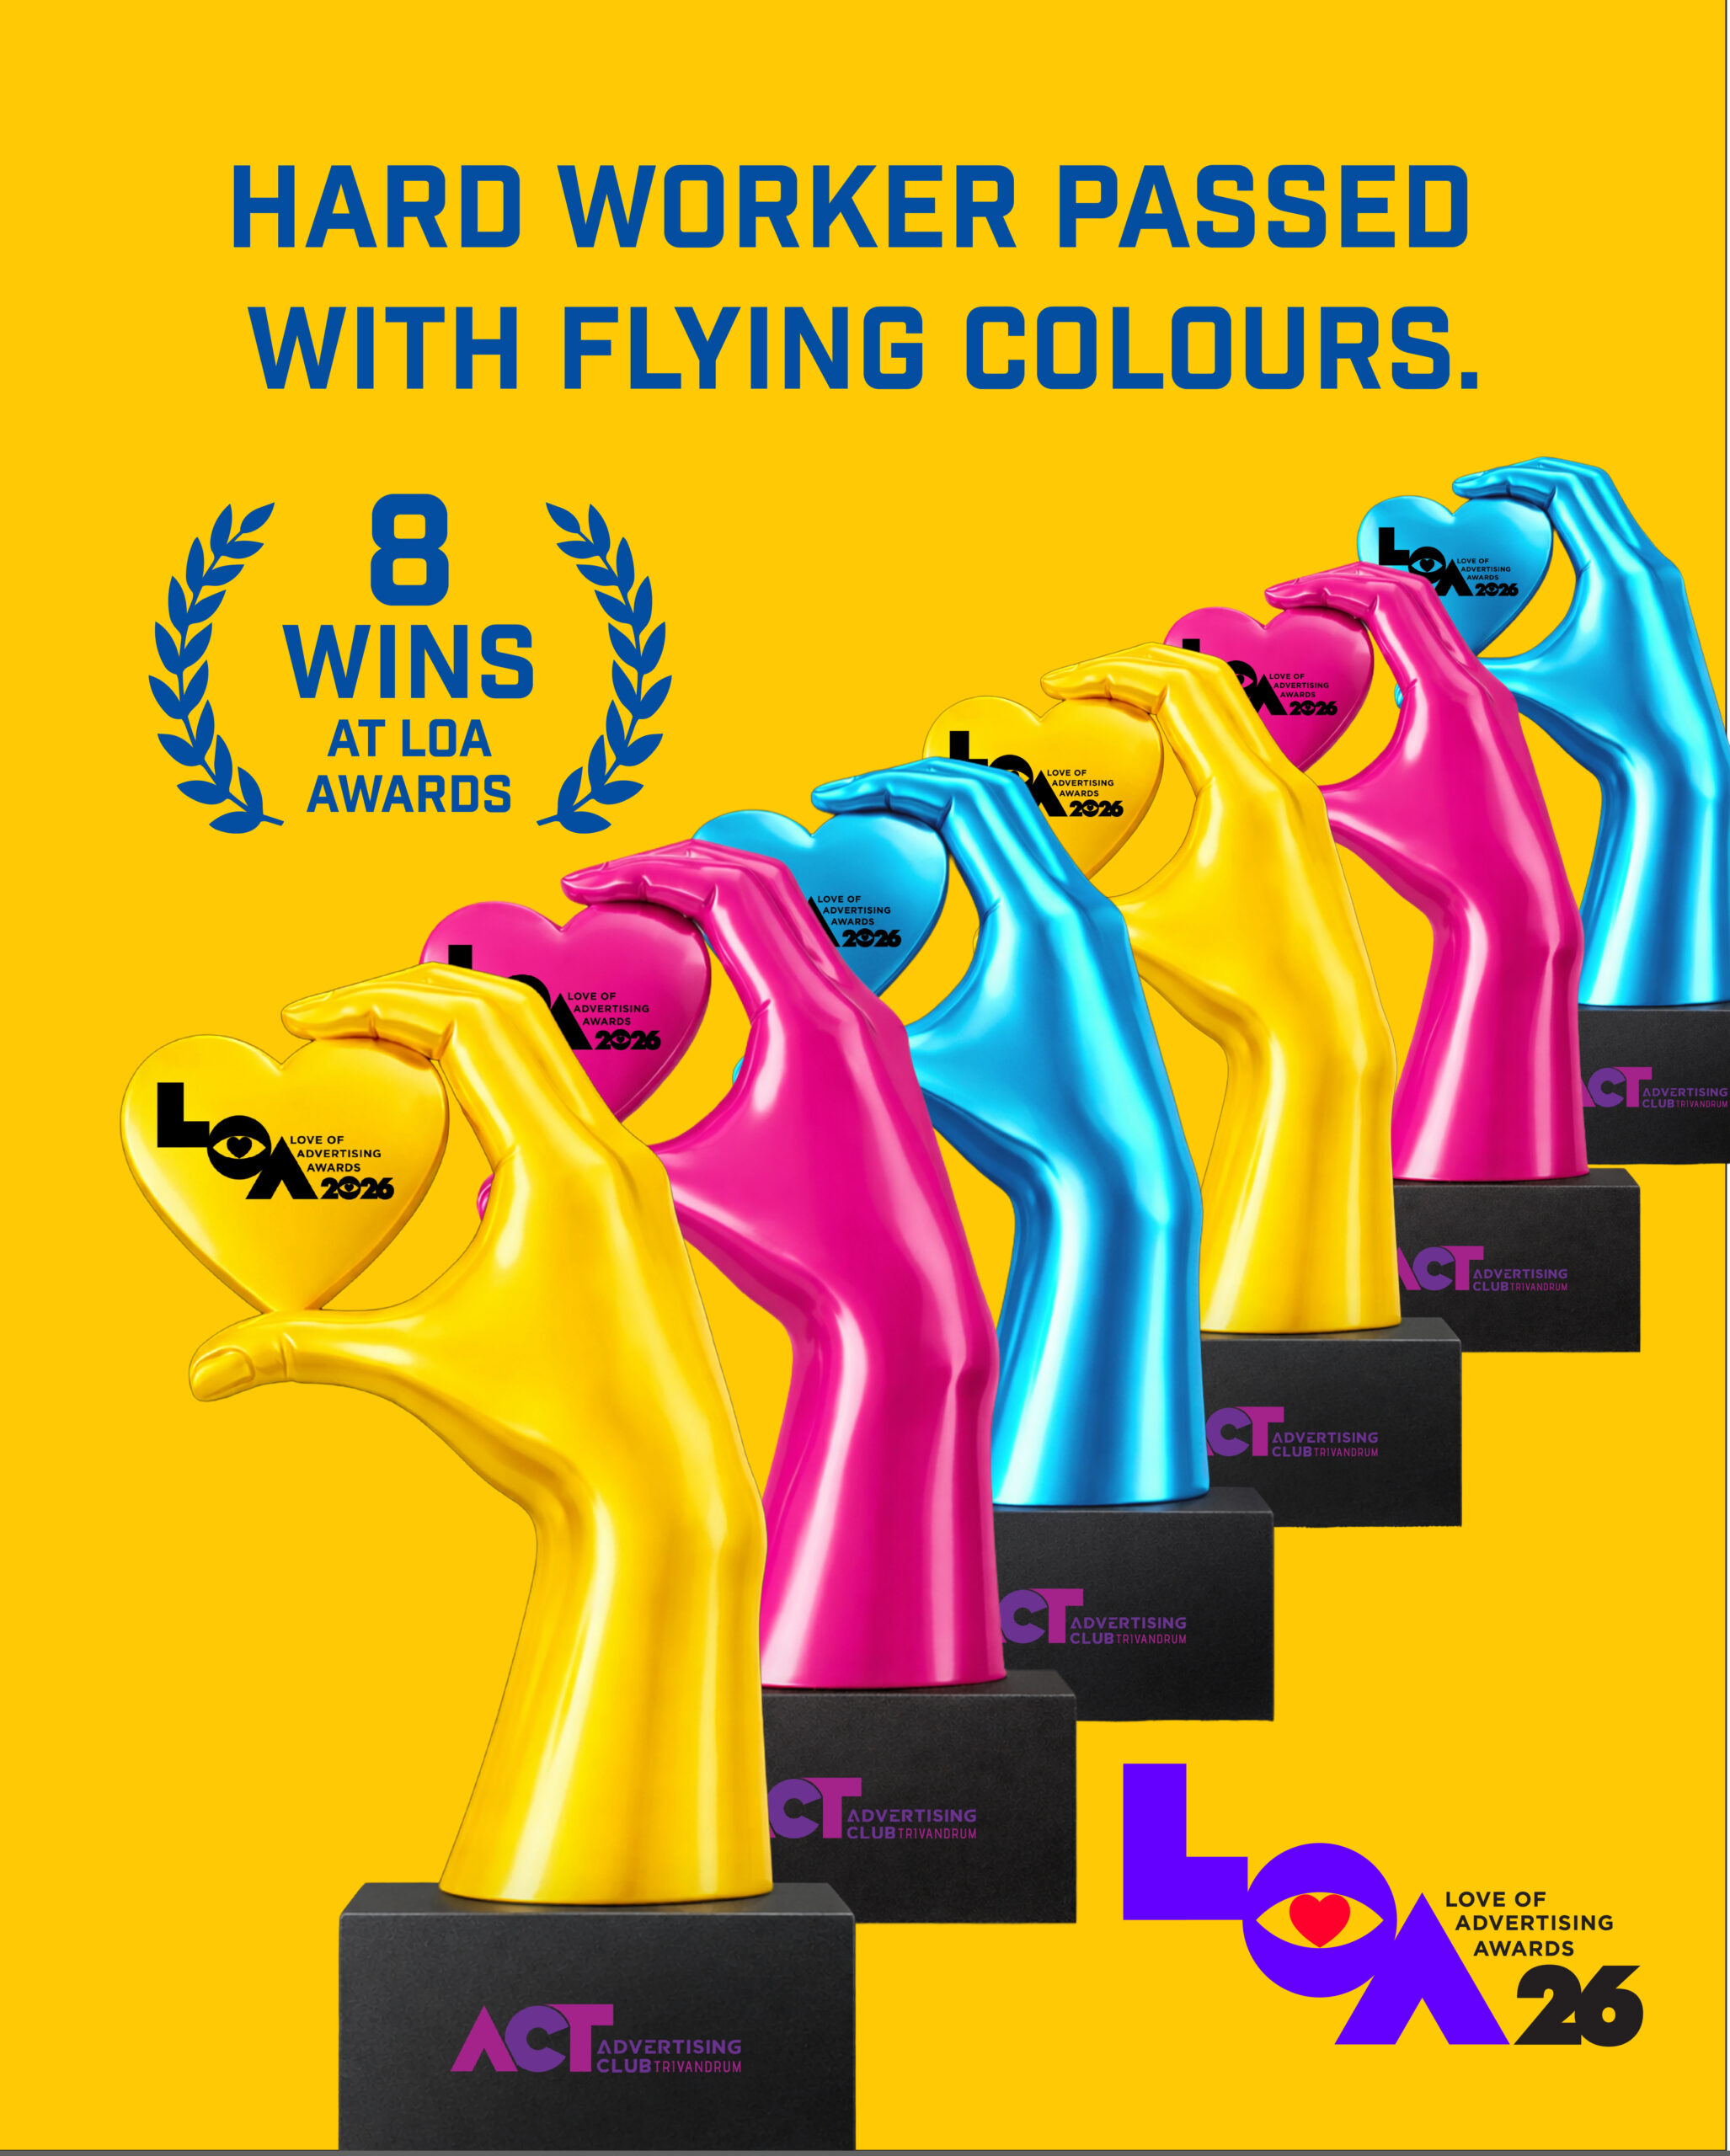
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’

Published

on

By

Shares

Ramco Cements’ Hard Worker brand wins eight awards for excellence in advertising, packaging and brand identity at the Love of Advertising Awards 2026.

Hyderabad 

The Ramco Cements Limited’s construction chemicals brand, Hard Worker, has secured eight awards at the Love of Advertising Awards 2026, recognising its creative excellence across television, digital advertising, packaging design and brand identity.

Organised by the Advertising Club of Trivandrum, the awards were presented at a ceremony held at The Leela Raviz, Kovalam, on 24 October 2026. The recognition highlights Hard Worker’s integrated marketing strategy and its efforts to establish a distinctive presence in India’s competitive construction chemicals market.

The eight awards span multiple creative categories, reflecting the brand’s approach to combining product-focused communication with engaging storytelling, humour and innovative design. Through its campaigns, Hard Worker has sought to simplify technical product benefits and make construction chemicals more accessible and relatable to consumers and construction professionals.

Built around the philosophy of “Hard-working products for hardworking people”, the brand focuses on communicating practical product advantages through memorable advertising narratives while maintaining a consistent identity across different marketing platforms.

Its campaigns for Ramco Hard Worker Eco Plaster and Tile Fix have been central to this approach. The Eco Plaster campaign highlights water conservation through the product’s self-curing properties, positioning it as a solution that supports more efficient construction practices. Meanwhile, Tile Fix promotes specialised tile-fixing solutions by presenting their practical benefits through relatable situations and creative storytelling.

Beyond advertising, Hard Worker has invested in distinctive packaging and brand identity development to improve product recognition and maintain consistency across customer touchpoints. This integrated approach has helped the brand differentiate itself in a category where marketing communication has traditionally focused on technical specifications and functional performance.

A V Dharmakrishnan, CEO, Ramco Cements, said, “Winning eight awards at the Love of Advertising Awards is a proud moment for Ramco Cements and the Hard Worker team. We believe that building a strong brand requires not only quality products but also the ability to communicate their value in a compelling and differentiated manner. Hard Worker’s journey reflects our commitment to combining product performance with innovative marketing to create meaningful connections with our customers and strengthen our presence in the construction chemicals market.”

The recognition comes as building materials manufacturers increasingly focus on brand differentiation, product awareness and customer engagement to strengthen their position in the construction chemicals segment.

By using humour and storytelling to explain product applications and benefits, Hard Worker aims to bridge the communication gap between technical construction solutions and the practical requirements of contractors, applicators and end-users.

Balaji K. Moorthy, Executive Director – Marketing, Ramco Cements, said, “Hard Worker was conceived to bring a fresh perspective to the construction chemicals category, where product communication has traditionally been functional and technical. Our endeavour has been to break through the clutter with distinctive ideas, humour and storytelling, while keeping the product proposition at the heart of every campaign. The recognition across TV and digital advertising, packaging design and brand identity design demonstrates our integrated approach to building the brand. These eight awards are an encouraging recognition of the creative thinking and collaborative effort behind Hard Worker’s marketing initiatives.”

The awards add to Hard Worker’s growing portfolio of creative recognitions and reinforce Ramco Cements’ emphasis on integrating product innovation with strategic marketing.

The brand’s communication initiatives also reflect a wider shift in the construction materials industry, where manufacturers are increasingly adopting consumer-focused marketing strategies to improve product understanding and strengthen relationships with construction professionals.

With its portfolio of construction chemicals, Hard Worker aims to address evolving requirements for durability, application efficiency and construction quality. Its marketing efforts seek to complement these product attributes by building stronger awareness and encouraging the adoption of specialised construction solutions.

Ramco Cements, one of India’s established cement manufacturers, operates across cement and allied building solutions. Through Hard Worker, the company is expanding its presence in the construction chemicals segment with products designed to enhance performance, quality and durability in modern construction applications.

The latest recognition strengthens Hard Worker’s brand visibility and underscores the growing importance of creative communication in promoting technical building materials. Ramco Cements intends to continue combining product development with distinctive marketing initiatives to support the brand’s growth in India’s construction chemicals market.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News