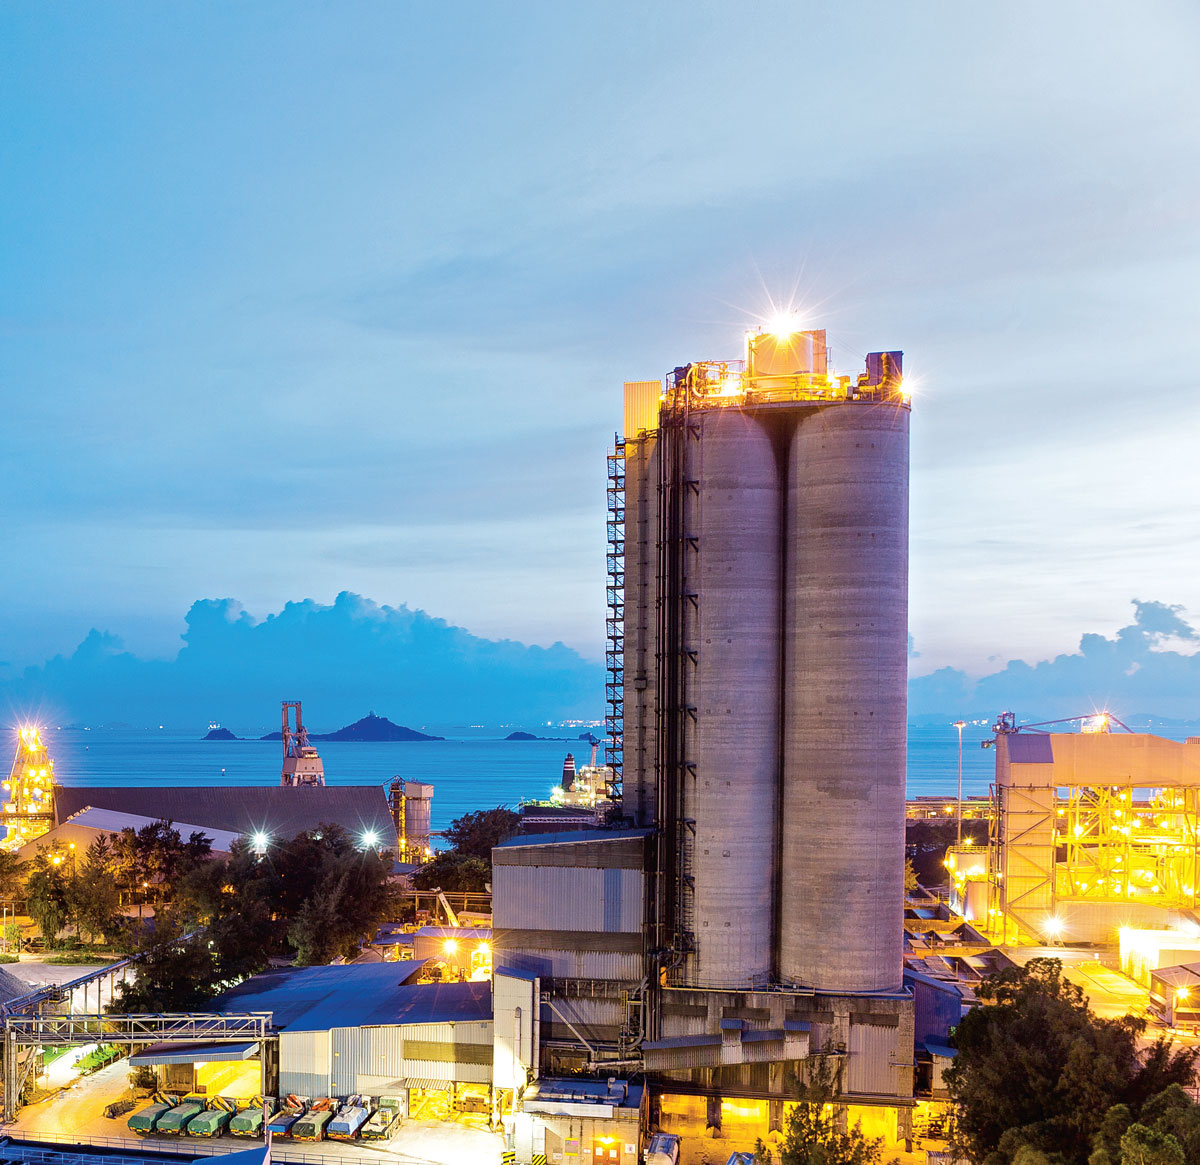
Cement plant modernisation is reshaping the industry through upgrades in
kilns, energy systems, digitalisation, AFR integration and advanced material
handling. We explore these technologies that improve efficiency, reduce
emissions, strengthen competitiveness, while preparing the industry for India’s
next phase of infrastructure growth.
India’s cement industry, the world’s second-largest, is undergoing a rapid transformation driven by infrastructure demand, decarbonisation targets and technological advancement. The sector’s installed capacity stood at approximately 668 million tonnes per annum (mtpa) in FY2025 and is projected to reach 915–925 mtap by 2030, supported by large-scale capacity expansions and infrastructure investment cycles, suggests CRISIL Intelligence Industry Report, 2025. At the same time, cement production remains highly energy intensive and contributes about 6 per cent to 7 per cent of India’s total greenhouse gas emissions, making efficiency improvements and modernisation critical for long-term sustainability as stated in CareEdge ESG Research, 2025. As a result, cement manufacturers are investing in advanced kiln technologies, digital monitoring systems, waste heat recovery, alternative fuels, and modern material handling infrastructure to enhance productivity while aligning with global decarbonisation pathways.
Need for modernisation
The need for plant modernisation is closely linked to the sector’s rapid capacity expansion and rising operational complexity. India’s installed cement capacity has grown significantly in the last decade and is expected to exceed 900 mtpa by 2030, driven by demand from housing, infrastructure and urban development projects, as per the CRISIL Intelligence Industry Report, 2025. However, increasing scale also places pressure on energy efficiency, logistics, and production stability. The report also suggests that the cement plants must upgrade equipment and processes to operate at higher utilisation rates, which are projected to reach 75 per cent to 77 per cent by the end of the decade, compared to around 72 per cent to 74 per cent in FY2026.
Environmental imperatives are another major driver of modernisation. Cement manufacturing is responsible for a significant share of industrial emissions because clinker production requires high-temperature processes that depend heavily on fossil fuels. According to CareEdge ESG research, the cement sector contributes 6–7 per cent of India’s total greenhouse gas emissions, with approximately 97 per cent of emissions arising from direct fuel combustion and process emissions in kilns. Consequently, plant modernisation initiatives now focus not only on productivity improvements but also on reducing emissions intensity, energy consumption, and reliance on conventional fuels.
“One of the most impactful upgrades implemented at Shree Cement in the last five years has been the adoption of advanced data management platforms that provide real-time visibility across major process areas. This digital advancement has strengthened plant automation by enabling faster and more accurate responses to process variations while improving the reliability of control loops. Real-time dashboards, integrated analytics and automated alerts now support quicker, data-driven decision-making, helping optimise kiln and mill performance, improve energy control and detect deviations early. By consolidating data from multiple systems into a unified digital environment, the company has enhanced operational consistency, reduced downtime and improved both productivity and compliance. This shift towards intelligent automation and real-time data management has become a key driver of operational excellence and future-ready plant management,” says Satish Maheshwari, Chief Manufacturing Officer, Shree Cement.
Kiln and pyroprocessing upgradation
The kiln remains the technological heart of cement manufacturing, and modernisation efforts often begin with upgrades to pyroprocessing systems. Many older plants in India operate with four- or five-stage preheaters, while modern plants increasingly adopt six-stage preheater and pre-calciner systems that significantly improve heat efficiency and clinker output. These systems enhance heat transfer, reduce fuel consumption, and stabilise kiln operations under high throughput conditions.
Professor Procyon Mukherjee suggests, “Cement manufacturing is, at its core, a thermal process. The rotary kiln and calciner together account for energy consumption and emissions. The theoretical thermal requirement for clinker production is around 1700–1800 MJ per tonne, yet real-world plants often operate far above this benchmark due to inefficiencies in combustion, heat recovery and material flow. Modernisation, therefore, must begin with the
kiln system, and not peripheral automation or
isolated upgrades. The shift from wet to dry process kilns, combined with multi-stage preheaters and precalciners, has already delivered step-change improvements, making dry kilns nearly 50 per cent more energy efficient.”
Recent investment programmes across the industry have included kiln cooler upgrades, advanced burners, and improved refractory materials designed to increase operational reliability and reduce specific heat consumption. Such upgrades are essential because cement production remains highly energy intensive, and continuous efficiency improvements are required to meet global decarbonisation targets. According to the International Energy Agency (IEA) Cement Tracking Report, 2023, the cement sector must achieve annual emissions intensity reductions of around 4 per cent through 2030 to align with global net-zero scenarios.
Energy efficiency and WHRS
Energy efficiency remains one of the most important areas of modernisation in cement manufacturing, given the sector’s heavy reliance on thermal and electrical energy. Modern plants deploy advanced process controls, efficient grinding systems, and improved combustion technologies to reduce specific energy consumption. The adoption of energy-efficient technologies is particularly important in India, where energy costs account for a large share of production expenses. As demand grows and plants expand capacity, improving energy performance becomes essential to maintain competitiveness.
Waste Heat Recovery Systems (WHRS) have emerged as a key solution for improving plant energy efficiency. During cement production, large volumes of high-temperature gases are released from kilns and coolers. WHRS technology captures this waste heat and converts it into electricity, thereby reducing reliance on external power sources. According to energy benchmarking studies for the Indian cement industry, installed waste heat recovery capacity in the sector has reached approximately 840 MW, with an additional potential of around 500 MW states the Green Business Centre, Energy Benchmarking Report, 2023. Several leading producers have already implemented large WHRS installations; for example, UltraTech Cement has deployed systems with around 121 MW of waste heat recovery capacity, reducing carbon emissions by nearly 0.5 million tonnes annually according to the Energy Alternatives India Case Study, 2024.
Integration of AFR
The integration of Alternative Fuels and Raw Materials (AFR) is another critical dimension of cement plant modernisation. AFR refers to the use of industrial waste, biomass, refuse-derived fuel (RDF), and other non-fossil materials as substitutes for conventional fuels such as coal and petcoke. Increasing the use of AFR helps reduce fossil fuel consumption while simultaneously addressing waste management challenges. According to the NITI Aayog Decarbonisation Roadmap, 2026, scaling the use of RDF and other alternative fuels could enable the sector to achieve thermal substitution rates of around 20 per cent in the coming decades.
However, integrating AFR requires significant plant modifications and operational adjustments. Waste-derived fuels often have inconsistent calorific values, higher moisture content, and heterogeneous physical properties compared to traditional fuels. As a result, modern plants invest in advanced fuel preparation systems, dedicated feeding equipment, and automated dosing technologies to ensure stable kiln operation. These upgrades allow plants to maintain consistent clinker quality while increasing the share of alternative fuels in their energy mix.
Digitalisation and smart plant operations
Digitalisation is rapidly transforming cement plant operations by enabling data-driven decision-making and predictive maintenance. Industry 4.0 technologies such as IoT sensors, artificial intelligence (AI), and advanced analytics are now used to monitor equipment performance, optimise process parameters, and anticipate maintenance requirements. These digital tools enable plant operators to detect early signs of equipment failure, minimise unplanned downtime, and improve operational efficiency. Predictive maintenance systems, for example, analyse vibration, temperature, and acoustic signals from rotating equipment to identify potential faults
before they escalate into major breakdowns. Digital twins and integrated control systems further allow operators to simulate plant performance under different scenarios and optimise production strategies. Such technologies are becoming increasingly important as cement plants operate at larger scales and higher levels of process complexity.
Maheshwari also adds, “Plant modernisation is also increasingly central to the global competitiveness of Indian cement manufacturers. As cost pressures rise across energy, logistics and regulatory compliance, modern plants offer the structural efficiency required to operate reliably and competitively over the long term. Technologies such as AI-driven Advanced Process Control (APC) integrated with real-time data systems are emerging as essential investments for the future. These platforms use predictive algorithms, machine learning and live process inputs to optimise kiln, mill and utility operations with greater precision than traditional control systems. By continuously analysing variations in feed chemistry, temperature profiles, energy demand and equipment behaviour, APC enables stable operations, lower specific energy consumption, reduced emissions and improved product consistency. As regulatory expectations tighten and plants pursue higher efficiency with lower carbon intensity, AI-enabled APC will play a crucial role in strengthening automation, enhancing decision-making and ensuring long-term operational resilience.”
Modern material handling and logistics
Material handling systems play a critical role in ensuring smooth plant operations and efficient logistics. Modern cement plants rely on advanced conveying systems, automated stockyards, and digital dispatch platforms to manage the movement of raw materials, clinker, and finished cement. Long-distance belt conveyors and pipe conveyors are increasingly replacing truck-based transport between quarries and plants, reducing fuel consumption, dust emissions, and operational costs. Automated stacker-reclaimers ensure consistent blending of raw materials,
which improves kiln stability and clinker quality. Meanwhile, advanced packing and dispatch systems equipped with high-speed rotary packers and robotic palletisers enhance throughput and reduce manual labour. These technologies allow cement plants to optimise logistics efficiency while supporting higher production capacities.
Emission control and environmental compliance
Environmental compliance has become a central focus of cement plant modernisation as regulators and investors place greater emphasis on sustainability performance. Modern plants deploy advanced emission control technologies such as high-efficiency bag filters, electrostatic precipitators, and selective non-catalytic reduction systems to reduce particulate matter and nitrogen oxide emissions.
Sine Bogh Skaarup, Vice President, Head of Green Innovation and R&D, Fuller Technologies says, “One of our key focus areas is decarbonisation. We help cement producers reduce CO2 and overall carbon emissions. We offer alternative fuel solutions and calcined clay technologies to enable the production of LC3 cement, which play a significant role in decarbonising the cement industry. By combining alternative fuels and calcined clay solutions, CO2 emissions can be reduced by up to 50 per cent, making this a highly impactful approach for sustainable cement production.”
Continuous emission monitoring systems are increasingly used to track environmental performance in real time and ensure compliance with regulatory standards. In addition to air pollution control, cement companies are also investing in water recycling systems, renewable energy integration, and carbon reduction initiatives. These measures are essential for aligning the sector with national climate goals and improving the environmental footprint of
cement manufacturing.
Economic benefits and future outlook
Beyond environmental and operational advantages, cement plant modernisation also delivers significant economic benefits. Energy efficiency improvements, digital process optimisation, and advanced material handling systems reduce operating costs and improve asset utilisation. Waste heat recovery and alternative fuels help lower fuel expenditure and reduce exposure to volatile fossil fuel markets. As the industry expands capacity to meet growing demand, modernised plants are better positioned to achieve higher productivity and maintain profitability. The long-term outlook for the sector remains positive, with India expected to continue large-scale infrastructure investments in roads, housing, railways, and urban development.
Milan R Trivedi, Vice President – Projects, Prod & QC, MR, Shree Digvijay Cement, says, “The main focus in case of modernisation projects drives through the investment decision, which is mainly based on IRR and impact on overall efficiency improvement, cost optimisation and improvement in reliability. However, there are certain modernisation, which has high impact on environmental impact, statutory requirements, etc. has higher priority irrespective of ROI or payback period.”
“The energy efficiency and reliability investment projects generally provide fast return on investment whereas strategic, digitalisation and environmental investment projects provide long term and compounded benefits. Typical modernisation investment projects are decided with IRR of about > 20 per cent, payback period of typically 2-3 years for fast-track projects,” he adds.
In this context, modernisation will remain a key strategic priority for cement manufacturers seeking to maintain competitiveness in an increasingly sustainability-focused market.
Conclusion
The modernisation of cement plants is no longer a purely technical upgrade but a strategic transformation that reshapes how the industry operates. As India’s cement sector expands capacity toward the next growth cycle, improvements in energy efficiency, digitalisation, alternative fuels and advanced logistics will determine the competitiveness of individual plants. Modern technologies allow producers to operate at higher productivity levels while simultaneously reducing energy consumption and emissions intensity.
Looking ahead, the pace of technological adoption will play a decisive role in shaping the future of
the cement industry. Companies that successfully integrate modern equipment, digital systems, and sustainable production practices will be better positioned to meet rising infrastructure demand while aligning with global climate commitments. In this evolving landscape, plant modernisation stands as the cornerstone of both operational excellence and environmental responsibility.
















 Concrete4 weeks ago
 Concrete4 weeks ago

 Concrete3 weeks ago

 Concrete3 weeks ago