

Concrete
Digital Transformation

Digitalisation is the way forward for the cement industry. Industry 4.0 brings with it tools that will help manufacturers in determining the desired product quality. ICR looks at the various channels through which cement companies can transform their processes to improve efficiency and sustainability.
The world is moving forward with technology and innovation and so is the Indian cement industry. It is increasingly embracing Industry 4.0 technologies to improve efficiency, reduce costs, and enhance product quality. Efficiency of a cement is the key to achieve the best production rate at the best cost. Costs of raw material, fuel and equipment are rising by the day. Thus, it is important to ensure accuracy through implementation of process controls and technical support. The cement industry globally is adopting Industry 4.0 technologies through automation, AI, data and more.
Automation is being used to optimise production processes, reduce downtime, and improve product quality. Automation is being used to control the entire production process, from raw material processing to finished product packing. Artificial intelligence is being used to analyse production data to optimise processes and reduce energy consumption. Indian cement companies are using machine learning algorithms to predict equipment failures and to optimise production schedules. Internet of Things (IoT) is being used to monitor equipment in real-time, enabling predictive maintenance and reducing downtime. It is also used to optimise logistics processes, including transportation and inventory management. Augmented reality is being used to improve safety and training. Indian cement companies are using AR to train workers and to improve safety by creating virtual simulations of hazardous scenarios. Big data analytics plays a key role to analyse production data, which in turn is used to optimise processes and improve product quality. Indian cement companies are using data analytics to identify the root cause of quality issues and to optimise production parameters.
Digitalisation has become a key factor to business success, encompassing physical assets, plants in multiple geographies, industry domains and regulatory frameworks. Early adopters can realise competitive advantages by leveraging digital technologies to identify and propagate best practice throughout their organisation, creating value for stakeholders.
ROLE OF AUTOMATION IN CEMENT INDUSTRY
Automation has a significant role to play in the cement industry. Here are some examples of how automation is being used in the industry:
Process control: Automation systems can be used to monitor and control various stages of the cement production process. This includes controlling the raw material feed, grinding, and blending of raw materials, and the kiln and clinker production process. By automating these processes, cement companies can improve product quality, reduce energy consumption, and increase production efficiency.
Quality control: Automation systems can be used to monitor the quality of cement at various stages of production. This includes monitoring the chemical composition of raw materials, the fineness of grinding, and the composition of the final product. By automating quality control, cement companies can ensure consistent quality and reduce waste.
Maintenance: Automation systems can be used to monitor the condition of equipment in real-time, enabling predictive maintenance. By using data to predict when maintenance is needed, cement companies can reduce downtime and optimise maintenance schedules.
Logistics: Automation systems can be used to optimise logistics processes, including transportation, storage, and distribution. By automating logistics processes, cement companies can reduce transportation costs, improve inventory management, and increase delivery efficiency.
“For the cement industry we primarily have bulk loading systems with an objective to reduce fugitive emissions that are generated while bulk loading. This means that we are trying to control dust at the cement plant,” says Venkatesh Ravula, CEO, DCL Bulk Technologies.
“We are the first organisation to bring this technology to the customers which makes us leaders in the field of dust emission control while bulk loading. Over a period of 4 decades, we have constantly upgraded our products and have made them better suited to the Indian requirements,” he adds.
Safety: Automation systems can be used to improve safety in the cement industry. For example, automated systems can be used to monitor the emission of pollutants, detect potential hazards, and improve emergency response times. By improving safety, cement companies can protect workers and reduce the risk of accidents.
Automation has a significant role to play in the cement industry. By automating processes and leveraging data, cement companies can improve product quality, reduce energy consumption, optimise maintenance schedules, improve logistics, and enhance safety.
EFFICIENCY FROM SOFTWARES AND MONITORING SYSTEMS
To achieve efficient and productive functionality in plants, multiple softwares, equipment, and monitoring systems are installed to ensure that production processes run smoothly, and equipment operates optimally.
management, and increase delivery efficiency.
Monitoring systems help ensure consistent product quality by providing real-time data on the production process. By monitoring production parameters, such as temperature and pressure, operators can quickly detect and correct any deviations that could impact product quality. They also help in identifying inefficiencies in the production process, such as equipment breakdowns, and can trigger automated responses to reduce downtime. This reduces the time and cost associated with maintenance and repair.
“We are an AI and IoT based predictive and prescriptive maintenance solution company. We predict the maintenance of equipment and save downtime for the plant which can cause millions of dollars to the organisation. We have an IoT device which can calculate six parameters like vibration, temperature, humidity, acoustic data, electric signals and the speed of the machine. Once this data is retrieved from the machine, the cloud systems analyses this data and comes up with analytics with its algorithm,” says Prashant Verma, Co-Founder and India Head, Nanoprecise Data Services.
Monitoring systems can help reduce operational costs by optimising energy consumption and reducing waste. By monitoring energy usage and production data, operators can identify opportunities for improvement, such as reducing the use of raw materials or optimising kiln temperatures. They also help improve maintenance operations by providing real-time data on equipment performance. This enables predictive maintenance, where maintenance tasks are scheduled before equipment failures occur. This reduces downtime, reduces the cost of repairs, and increases equipment lifespan.
“Our instruments are mainly used for the purpose of efficiency measurements. We have equipment that helps measure ultrasonic heat in the preheaters which helps detect any irregularity in the temperatures. This helps them take corrective action, thus, preventing damage or slowing down of the plant which leads to better efficiency. Similarly, we have multiple equipment that support the efficiency of cement plants,” says Piyush Patel, Head – Strategic Business, Testo India.
Monitoring systems help improve safety in the Indian cement industry by monitoring equipment for potential hazards and detecting potential safety risks. Automated responses can be triggered to prevent accidents, and operators can be alerted in real-time to potential issues. monitoring systems have numerous advantages for the Indian cement industry, including improved product quality, increased efficiency, cost reduction, enhanced safety, and improved maintenance. By investing in monitoring systems, Indian cement companies can become more competitive, sustainable, and efficient.
ensure consistent quality and reduce waste
SUSTAINABILITY WITH TECHNOLOGY
Technology can play a critical role in achieving sustainability in cement production by improving energy efficiency, reducing carbon emissions, reducing waste, and improving production processes through digitalization and data analytics.
To achieve Net Zero, it is essential to use alternative fuels and raw materials. Growing technology in the Indian cement industry can help in analysing and adjusting equipment of fuels and raw materials that can make a viable end product that serves the purpose and protects the planet.
Keyur Shah, Business Manager, SB Engineers, says, “As far as alternative fuels are concerned, petcoke, lignite, municipal wastes etc., are being used. When fuel type is changed, the burning process changes. The calculation with a different fuel is the quantity of fuel that needs to be pumped in to achieve the thermal balance in the burning zone area. It becomes more relevant to monitor and understand thermal knowledge in this scenario. Cement industry is using cementitious materials in their raw mix. Flyash or gypsum is mixed with clinker and then grinding is done. The percentage of this mix varies and grinding properties also change accordingly. What needs to be monitored is the particle size to understand if the process of grinding is giving an optimum output. Our equipment help monitor the changes in process when alternative fuels are used and when the raw mix has other cementitious materials in various proportions.”
Technology can help improve the energy efficiency of cement production equipment, such as kilns and mills. Advanced process control systems can optimise production parameters, such as temperature and pressure, to reduce energy consumption. Additionally, energy-efficient motors, variable speed drives, and heat recovery systems can help reduce energy usage.
“In the area of AFR, we are working on equipment and are one of the first ones to provide solutions for AFR when the equipment was newly installed and even spares were unavailable in the country. Many esteemed groups in the country use our solutions for AFR and life enhancement of these components. When it comes to heat, Vautid has always been working on areas where heat is an integral part of the process and leads to wear. Our products are designed in a manner to meet a combination of wear requirements, mostly to do with heat” says Anand Sundaram, Managing Director, Vautid India.
Newer technologies like carbon capture are slowly advancing in the Indian cement industry and can revolutionalise the decarbonisation mission of the industry. Similarly, data analytics can help optimise production processes by identifying areas of improvement, reduce energy consumption, and improve product quality. Digitalisation can also help improve supply chain efficiency, reduce logistics costs, and improve inventory management. Technology can also help cement companies recycle waste materials from the production process, such as slag or fly ash. This reduces waste and conserves natural resources. Additionally, technology can help companies optimise the use of water and reduce the amount of wastewater produced during the production process.
With the use of softwares, monitoring systems, better machinery, newer technologies and taking the digital route, the Indian cement industry is moving towards cost and energy effective cement manufacturing, which is going to benefit the industry with better production value in the long run.
-Kanika Mathur







Concrete
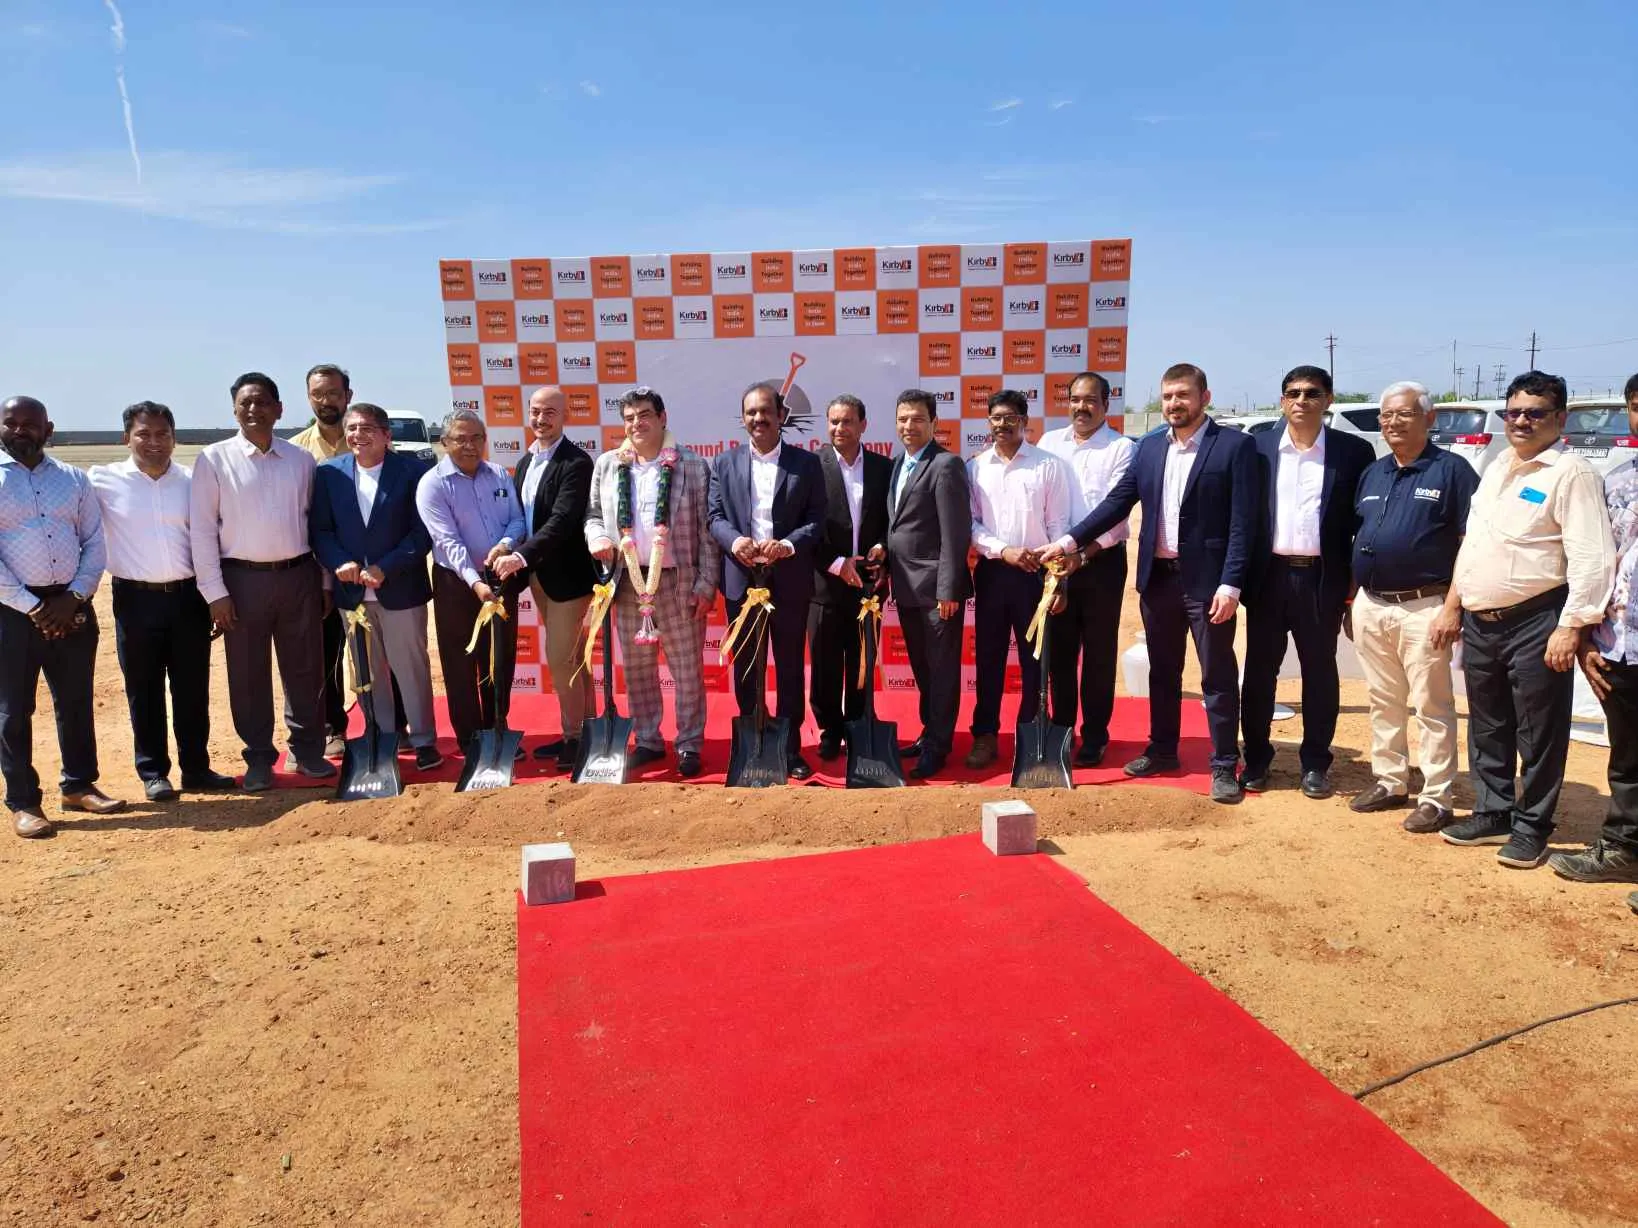
Kirby India Breaks Ground on Fourth PEB Plant in Tamil Nadu
New Manapparai facility will lift annual capacity to 400,000 tonnes by mid-2027

Concrete
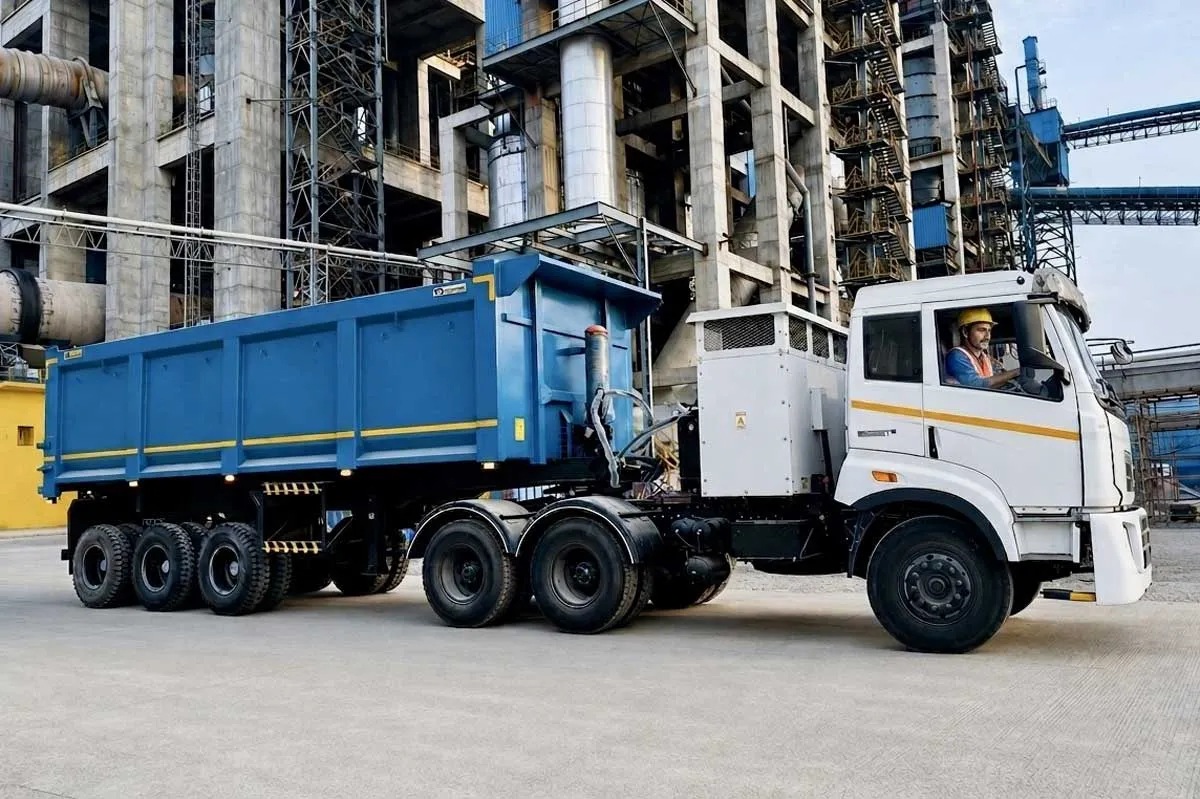
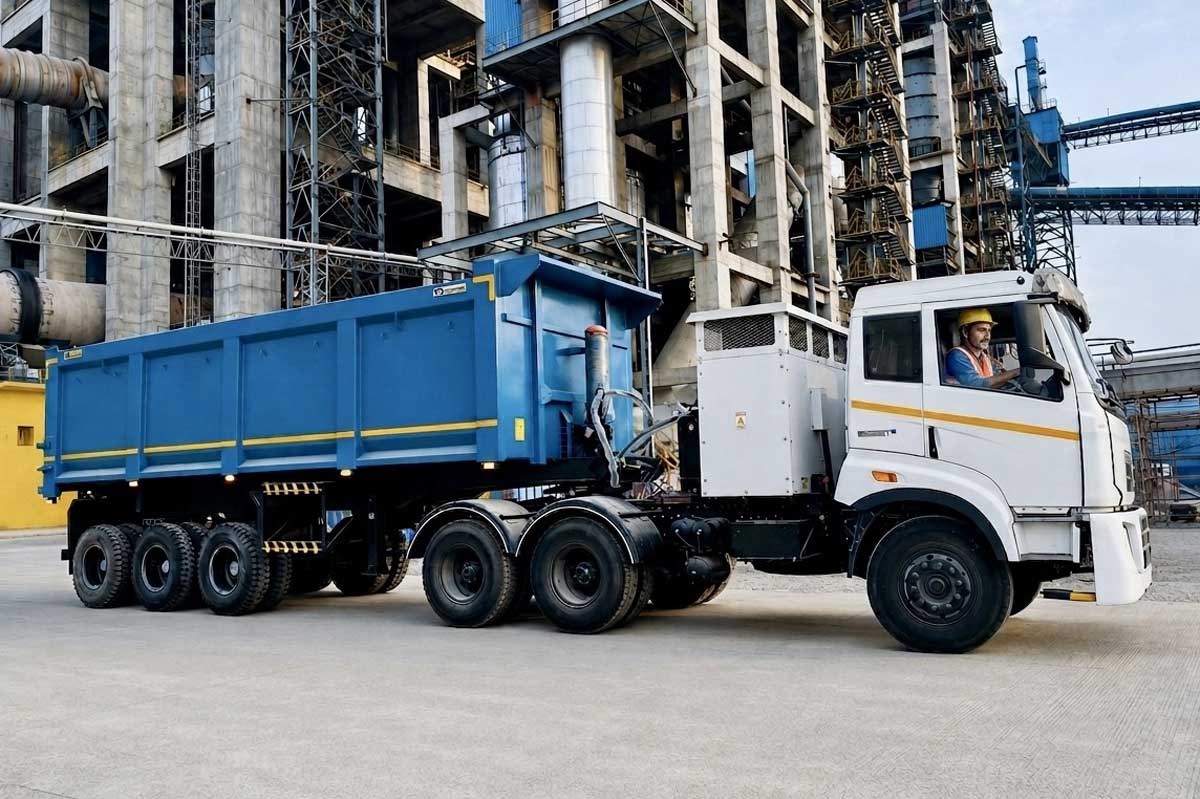
UltraTech to Deploy 600+ Electric Trucks by Dec 2026
Cement major expands green logistics to cut emissions across supply chain


Kirby India Breaks Ground on Fourth PEB Plant in Tamil Nadu

UltraTech to Deploy 600+ Electric Trucks by Dec 2026

UltraTech Cement expands green logistics with 600+ electric truck fleet

CarbonStrong Raises Rs 125 Million To Scale Low Carbon Cement Tech
Protect Your Margins
Kirby India Breaks Ground on Fourth PEB Plant in Tamil Nadu
UltraTech to Deploy 600+ Electric Trucks by Dec 2026
UltraTech Cement expands green logistics with 600+ electric truck fleet
CarbonStrong Raises Rs 125 Million To Scale Low Carbon Cement Tech

