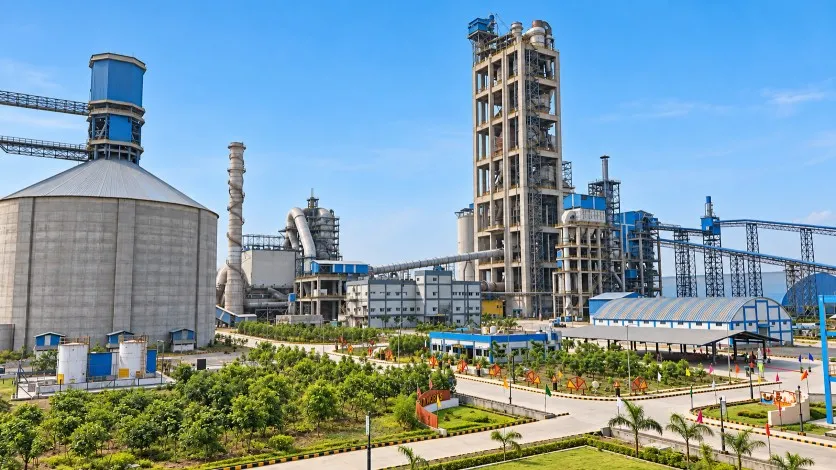
Girish Kumar, Plant Director, Riyadh Cement, outlines a disciplined, phased roadmap for cement plants looking to scale thermal substitution rates without sacrificing kiln performance or clinker quality.
As the cement industry accelerates its shift toward alternative fuels and raw materials (AFR), the gap between ambition and execution remains wide for many plant operators. Girish Kumar, Plant Director, Riyadh Cement, reveals why unstable baseline operations are the primary reason AFR programmes fail, and why scaling thermal substitution rates demands a cultural change as well as an investment in engineering.
How does process stability influence the success of AFR integration in cement plant operations?
As per my experience, process stability is the foundation of successful AFR integration to the clinker manufacturing, the most AFR failure are not because of fuel quality, the real issue is unstable baseline operation. AFR utilisation is only effective when the kiln and preheater systems are already operating in a stable condition. Unstable AFR operation often increases overall cost despite cheaper fuel. Within the process stability, the feasibility of AFR also depends on consistency in chemical and physical properties. Variations in calorific value, moisture, ash, volatile matter, alkalis, sulphur and chlorides directly impact pyro-process stability.
Stable operation enables the plant to absorb these variations through proper control of combustion, heat balance and gas flow. It also requires close alignment with raw mix design, as AFR ash influences key quality parameters such as quality moduli, PSD raw meal and burnability often requiring corrective raw materials. Additionally, improper control of volatile elements (chlorides, sulphur, alkalis) can lead to operational issues such as ring formation, coating instability, build-ups and cyclone blockages.
A stable kiln operation with controlled temperatures, draft, oxygen balance, and consistent feed chemistry creates the operating window required to absorb AFR variability. Without stable baseline operations, AFR becomes a disruption rather than an opportunity, increasing the risk of process disturbances, negatively impacting clinker quality, emissions and overall
plant KPIs.
What are the key operational disciplines required to scale AFR usage without compromising kiln performance and output quality?
As per my experience, scaling AFR usage is less about technology and more about discipline
on the shop floor with strict control of key operational parameters:
a. The AFR introduce in the system calorific value deviation should be less than 200 Kcal/kg of clinker.
b. Maintain higher oxygen levels at the preheater/calciner outlet (in some cases up to ~4 per cent) to ensure complete combustion of alternative fuels.
c. Control the temperature difference (?T) between gas and material in the preheater (typically <5°C) to ensure efficient heat exchange.
d. Optimise gas velocities in the riser duct and cyclones to ensure proper mixing, combustion, and heat transfer from minor to moderate level.
e. Maintain higher momentum at the main burner to stabilise the flame and accommodate variable AFR characteristics and in addition burner position is important to balance the alkalis sulphur cycle.
f. Ensure proper sulfur cycle balance by controlling firing sulfur input and effectively utilising kiln bypass (where available) to prevent build-ups and coating formation.
g. Ensure AFR quality control—particularly TDF/RDF utilisation then TDF size, moisture, and blending with biomass streams—which is critical for achieving higher substitution rates (up to ~50 per cent in calciner systems).
h. Apply proven co-processing strategies such as blending poultry waste and carbon black with coal (e.g., ~10 per cent to 15 per cent each), enabling stable feeding through the coal mill as practiced in regional markets.
i. Calibrated weigh feeders and dosing systems stable and the deviation in SHC < 180-200 Kcal/Kg and Temperature profile of the PH must have deviation of < 5*C.
j. If consider a new project scale, new PC designs with venturi’s are required for maximum heat transfer by venturi and more retention time by more PC height and volume.
These disciplines collectively sustain thermal efficiency, stabilise kiln operation, manage volatile cycles and protect clinker quality despite the inherent variability of AFR.
How can plants transition from opportunistic AFR usage to a structured, high-TSR operating model?
Transitioning from opportunistic AFR use to a structured, high Thermal Substitution Rate (TSR) model requires moving from ad-hoc fuel acceptance to a fully engineered and controlled system. This starts with defining a clear AFR strategy, including long-term fuel sourcing agreements, defined quality specifications, and a stable fuel basket instead of irregular inputs. Plants must then invest in dedicated pre-processing and feeding infrastructure to ensure consistent fuel size, moisture, and calorific value.
On the operational side, kiln systems should be stabilised at low TSR and then gradually ramped up through a controlled, stepwise approach. This must be supported by strict process control, particularly in oxygen management, volatile balance, and burner stability, to avoid operational upsets. Equally important is the development of skilled AFR-focused teams supported by process optimisation and R&D functions, ensuring continuous learning and plant-specific adaptation. Finally, digitalisation and AI-based optimisation tools should be deployed to enable real-time monitoring and decision-making, allowing the plant to manage variability while steadily pushing TSR to higher, stable levels.
What are the most common failure points when implementing AFR, and how can they be mitigated?
Failure point 1: Improper AFR selection and processing Inappropriate selection of AFR or poorly designed pre-processing systems (e.g., inconsistent particle size, high moisture, variable calorific value).
Mitigation:
• Conduct detailed feasibility studies (NCV, moistures, ash, chlorine, sulfur etc).
• Ensure proper pre-processing (remove toxic waste, shredding, drying, homogenisation).
• Prefer engineered solutions from experienced vendors or develop robust in-house systems with clear specifications.
Failure point 2: Lack of skilled operational expertise
Insufficiently trained kiln operators and absence of dedicated AFR/process optimisation teams.
Mitigation:
• Develop specialised AFR-trained operational teams
• Implement continuous training programmes
• Deploy advanced process control (APC) and real-time optimisation tools
Failure point 3: High variability in AFR quality
Significant fluctuations in AFR composition especially, in municipal solid waste (MSW), where high calorific fractions are often removed (as seen in regions like India), leading to low and inconsistent fuel quality.
Mitigation:
• Establish strict quality control protocols and
supplier agreements.
• Install online monitoring systems (e.g., CV analyser’s, moisture sensors).
• Blend multiple AFR streams to stabilise fuel characteristics.
Failure point 4: Process instability in kiln operation
In most plants, AFR failures are not due to one factor, but a combination of technical and organisational gaps. AFR introduction leading to unstable kiln conditions, including coating formation at kiln inlet, thick coating in upper transition zone, volatile cycles (Cl, S, alkalis), boulder formation and snowman formation at cooler.
Mitigation:
• Maintain stable thermal profile and oxygen levels
• Perform detailed volatile balance and adjust raw mix accordingly.
• Optimise burner settings and airflow distribution.
• Control AFR feed rate and feeding location (calciner vs kiln).
• Ensure proper kiln draft and gas velocities.
How do you align people, processes and technology to ensure consistent and reliable AFR utilisation on the ground?
Achieving consistent and reliable AFR utilisation requires strong alignment between people, processes, and technology, supported by a phased and disciplined implementation strategy.
For new plants or greenfield projects, alignment is relatively straightforward. Systems can be designed from the outset for high AFR substitution (50 to 100 per cent) by:
• Selecting suitable AFR streams based on long-term availability and quality.
• Installing properly engineered pre-processing and feeding systems.
• Integrating advanced AI-based process control and optimisation tools.
• Training operators specifically for AFR-based kiln operation.
For existing plants (brownfield transition), the challenge is significantly higher and requires a cautious, stepwise approach:
A) People alignment: Develop skilled, AFR-focused operational teams supported by dedicated process optimisation and R&D functions to ensure continuous improvement, stable operations, and efficient AFR utilisation. Provide continuous training on AFR handling, combustion behaviour and kiln impacts. Build a culture of confidence and accountability, as AFR transition often requires operational ‘courage’ and experience.
B) Process alignment
• Start with low AFR substitution rates and gradually increase to the optimum level.
• Establish strict quality control at the AFR source (moisture, CV, particle size, contaminants).
• Define standard operating procedures (SOPs) for feeding rates, kiln conditions and upset handling
• Continuously monitor and stabilise key parameters (O2, CO, temperatures, draft, volatile cycles).
C) Technology alignment
• Retrofit appropriate feeding and dosing systems for different AFR types.
• Ensure proper pre-processing (shredding, drying, homogenisation).
• Implement advanced control systems (APC/AI) for real-time optimisation.
• Use online analysers and monitoring tools to reduce variability impact.
Therefore, in brownfield plants, the biggest challenge is not technology, it is changing operator confidence and mindset.
What role does digitalisation and data-driven decision-making play in optimising AFR performance in real time?
Digitalisation and data-driven decision-making enable real-time decision-making through AI-based optimisation systems that continuously analyse process data and instantly adjust operating parameters. This helps maintain process stability, optimise combustion, and maximise AFR utilisation despite fuel variability. As a result, plants achieve higher substitution rates, fewer process disturbances, and consistent clinker quality through fast, predictive, and real-time control. Digital systems also help detect early signs of instability, allowing corrective action before it impacts kiln performance.
What would a future-ready cement plant look like with AFR fully embedded into its operational DNA?
The future plant will not adapt to AFR – it will be designed around it.
A future-ready cement plant will be designed to handle a wide spectrum of AFR, including low-calorific fuels (1500–2000 kcal/kg), through advanced pre-processing and flexible feeding systems. It will also integrate emerging fuels such as hydrogen as a supplementary or primary energy source for decarbonisation. An innovative method developed by Korean experts focuses on stabilising RDF quality and reducing calorific value (CV) variability by converting mixed waste streams into engineered fuel beads.
In this approach, materials such as poultry waste, sawdust, carbon black, biomass and sugar molasses are blended and processed into small, uniform beads (typically 4–6 mm). These engineered fuels offer a more consistent net calorific value (NCV) in the range of ~4500–5000 kcal/kg.
This pelletised/bead form improves:
• Fuel homogeneity and handling.
• Long-term storage stability.
• Controlled feeding and dosing.
• More stable combustion in the calciner.
As a result, such engineered AFR significantly reduces process fluctuations and enables higher, more reliable substitution rates compared to conventional RDF. The plant will feature high-efficiency, multi-fuel burners capable of stable combustion of diverse fuels, supported by optimised kiln design. AI-based control systems will enable real-time decision-making and process optimisation, while advanced chemical additives will help manage build-ups and coating formation.
Overall, it will be a highly digitalised, flexible and low-carbon operation capable of maximising AFR and alternative energy utilisation, without compromising performance or product quality.














 Concrete1 month ago

 Concrete4 weeks ago

 Concrete1 month ago

 Concrete3 weeks ago