Economy & Market
We aim to make sustainable practices more accessible
Published
1 year agoon
By
admin
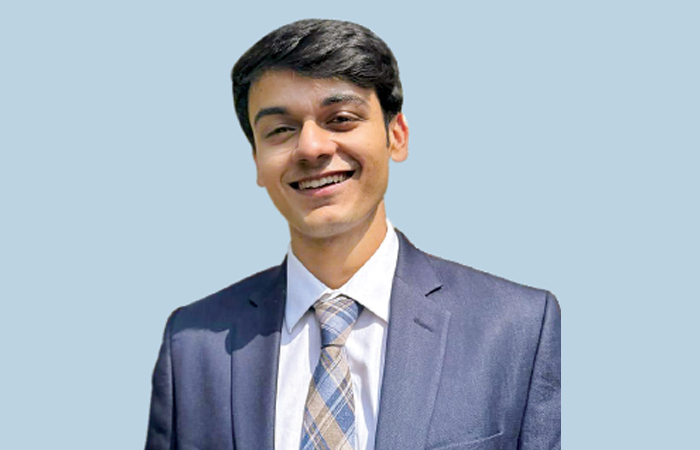
Raunak Singh Chatha, Business Development Manager, Alfa Therm, in conversation with Kanika Mathur about transforming waste into energy with cutting-edge shredding solutions.
Advanced shredding technology is playing a pivotal role in sustainable waste management in the cement industry. Technology-led companies are providing innovative solutions for alternative fuel processing. One such organisation is Alfa Therm, a leading engineering company with over 35 years of expertise. Ronak Singh Chaddha, Business Development Manager, takes us through their tailored industrial solutions that are designed to meet the unique challenges of waste handling and emissions control, in this interesting interaction.
How is Alfa Therm contributing to sustainable waste management and recycling in the cement industry through its advanced shredding?
Alfa Therm is a 35-year-old engineering company based in Gurugram, Haryana. Through its advanced shredding technology, Alfa Therm serves as a one-stop solution for the fuelling requirements of the largest cement groups in the country, and we are currently fulfilling this role successfully. With our state-of-the-art manufacturing facility, we ensure the highest quality standards and precision in our industrial solutions. Our manufacturing team comprises over 200 skilled professionals, supported by a highly advanced design team that helps us tailor our products to meet the unique needs of various industries.
Our product range includes incinerators for biomedical waste management, compost machines for organic waste processing, and shredders for producing alternative fuels. The most recent addition to Alfa Therm’s portfolio is pommels and material recycling facilities, which facilitate bio-remediation and land reclamation projects. These projects have been successfully executed across several sites in Delhi and the NCR region.
By combining engineering excellence with innovative technology, Alfa Therm continues to set high standards in sustainable waste management and recycling, making a positive impact on the cement industry and beyond.
With your state-of-the-art manufacturing facility, how does Alfa Therm ensure the highest quality standards and precision in its industrial solutions?
We have a manufacturing team of over 200 skilled professionals, supported by a highly advanced design team that helps us tailor our products to suit the specific needs of various industries.
Our offerings include incinerators for biomedical waste management, compost machines for organic feed processing, and shredders for producing alternative fuels. Currently, the most recent addition to AlfaTherm’s portfolio is pommels and material recycling facilities, which facilitate bio-remediation and land reclamation projects. AlfaTherm has successfully carried out these projects across multiple sites in Delhi and the
NCR region.
How does your expertise in processing materials like e-waste, rubber, and hazardous waste benefit the cement industry’s AFR strategies?
I would say that our greatest strength in processing materials like e-waste, rubber and hazardous waste lies in our extensive experience. The very first shredder we installed dates back to 1999, and it was assembled by my grandfather. Since then, AlfaTherm has had the privilege of working with a variety of industries across the country, including the tyre industry, the pharmaceutical sector, infrastructure, paper and pulp, and most recently, the cement industry over the last 6-7 years.
Over this period, AlfaTherm has gained valuable experience in processing diverse materials, which has helped us understand their potential. What may appear as regular waste material today could very well become a key resource to power an entire industry in the future. Our experience has allowed us to identify and harness this potential, giving us a significant edge in supporting the cement industry’s alternative fuel and raw material strategies.
What are the key innovations Alfa Therm has introduced in shredding and waste processing?
For cement manufacturers, innovation in shredding and waste processing is critical to enhancing efficiency and sustainability. However, as an engineering company, we believe that true innovation doesn’t emerge in isolation. It requires a thorough understanding of the market and the unique needs of the industry. We don’t just create solutions and hope they get adopted; we design solutions that industries are eager to embrace because they address real, pressing challenges.
Specifically for cement manufacturers, we focus on alternative fuels and raw materials (AFRs), particularly in the form of refuse-derived fuels (RDF). With India targeting its net-zero goal by 2070, cement plants—being some of the largest carbon emitters—must urgently adapt. This is where AlfaTherm plays a crucial role.
Our solutions empower cement manufacturers to enhance power generation and fuel efficiency. The largest cement groups in the country consume around 100-200 tonnes of fuel per day. Among our clients, some have managed to fulfill 15 per cent of their daily fueling needs through RDF. A few have achieved 20 per cent to 25 per cent, and we are proud to support some that have reached as high as 30 per cent of their daily fuel requirements through alternative fuels like RDF instead of conventional fossil fuels.
Our approach is to create machinery that not only addresses today’s requirements but also sets a foundation for the industry’s future. By developing advanced shredding and processing technology for RDF, we aim to make sustainable practices more accessible, efficient and impactful across the cement industry.
How does Alfa Therm customise its solutions to meet the specific challenges faced by cement plants?
When it comes to waste handling and emissions control, the biggest factors we consider are the capacities at which cement plants operate and the sources from which they procure their alternative fuels. These aspects play a crucial role in determining the customisation required for each cement plant.
For instance, if we consider RDF, it is essentially a grade of plastic. However, the quality and composition of RDF in the northern regions of India differ significantly from what is available in Tamil Nadu. As a result, the processing techniques required to handle these varying grades of RDF also differ.
At AlfaTherm, our manufacturing facility and dedicated design team ensure that our shredding solutions are tailored to the specific requirements of each cement plant, no matter where it is located in the country. Suppose a cement group has a daily requirement of 200 tonnes of RDF and sources its plastic waste locally in Tamil Nadu. In that case, our extensive research and experience over the past 6-7 years enable us to determine the precise level of treatment that this southern grade of RDF needs compared to a northern grade.
Additionally, we incorporate dust removal and ash handling systems to ensure compliance with environmental regulations, making the process as clean and sustainable as possible. Our goal at AlfaTherm is to continue being a one-stop solution for power plants across the country. Today, we serve the cement industry, but we hope to expand our expertise to more industries in the future.
You may like
-
Martin Engineering Appoints Ashwini Khunte as India General Manager
-
CII Calls for Greater Alternative Fuel Use in Cement Industry
-
Nuvoco reports 13.5% revenue growth in Q2 FY27
-
Nuvoco Marks 10 Years, Targets 35 MMTPA Capacity by FY28
-
JSW Cement commissions additional 1 MTPA grinding unit in Rajasthan
-
JSW Cement Boards Approve Proposed Shiva Cement Merger
Economy & Market
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
Published
3 hours agoon
October 30, 2026By
admin
Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.
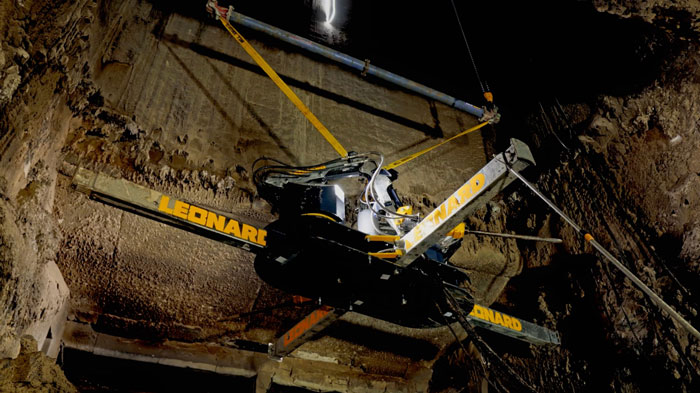
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.
Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.
Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.
Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.
According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.
First Deployment Demonstrates Shutdown Efficiency
The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.
Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.
Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”
Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.
The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.
“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.
“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”
Expanding Industrial Robotics Applications
Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.
Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.
Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.
The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.
Concrete
Martin Engineering Appoints Ashwini Khunte as India General Manager
Published
10 hours agoon
October 30, 2026By
admin
Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.
Pune
Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.
Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.
A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.
In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.
Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”
Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.
“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”
Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.
Concrete
Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26
Published
2 weeks agoon
October 19, 2026By
admin
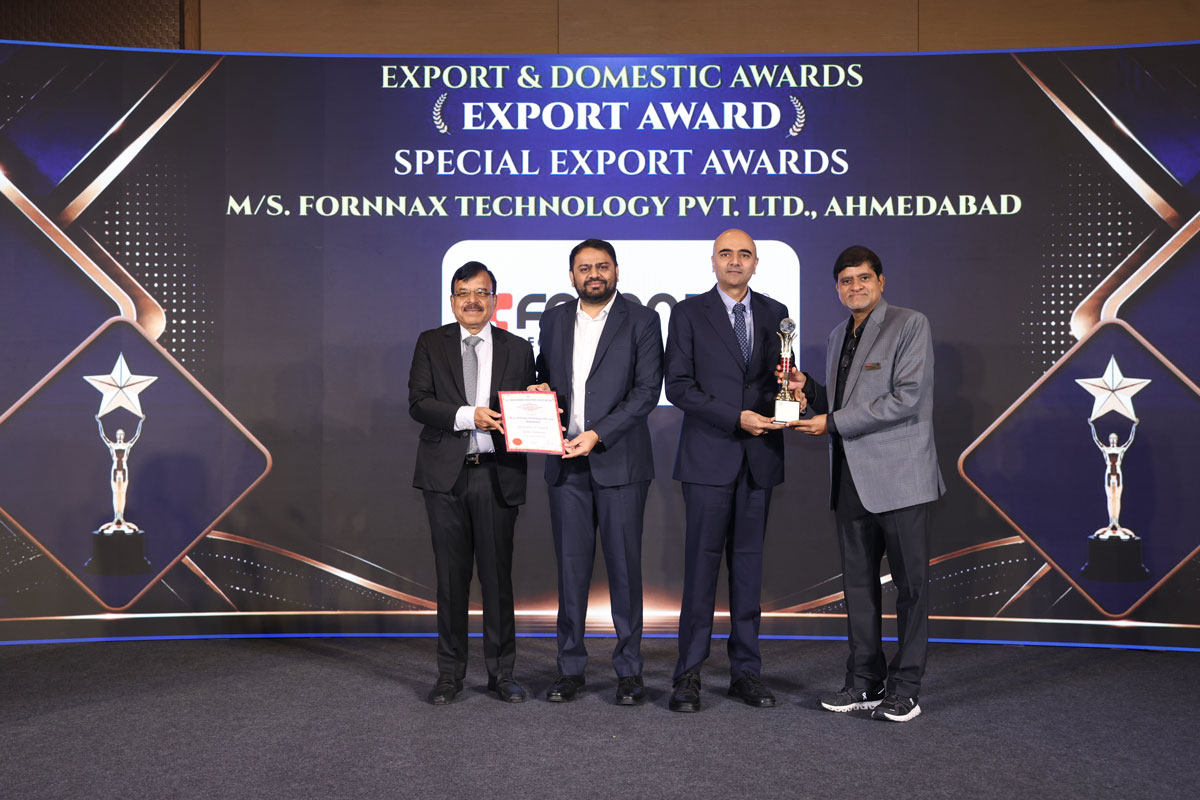
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.
With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.
The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.
Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:
“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”
Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.
The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.
Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.
For more information, visit: www.fornnax.com
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant
Martin Engineering Appoints Ashwini Khunte as India General Manager
CII Calls for Greater Alternative Fuel Use in Cement Industry
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant
Martin Engineering Appoints Ashwini Khunte as India General Manager