Alternative fuels reduce cement plants’ carbon footprint, but infrastructure challenges limit adoption. Technologies like the HOTDISC® Reactor help overcome these barriers.
Alternative fuels are a relatively straightforward and readily available means of reducing a cement plant’s carbon footprint. The technology is proven and well used worldwide, and with the right controls in place the switch from fossil fuels to waste-derived fuels does not impact the quality of the end product. In some countries, cement plants are achieving near 100 per cent substitution in the calciner and high levels of substitution in the kiln. However, this trend is not universal, and some countries are struggling to achieve a thermal substitution rate (TSR) of 25 per cent. In this article, we will look at the obstacles to alternative fuels use and the technology that is available to overcome them.
Advantages of alternative fuels
Alternative fuels offer three key environmental advantages.
1) A lower carbon alternative to coal or petcoke.
2) A pathway for waste that might otherwise be landfilled, including hazardous waste.
3) An alternative to waste incineration, which is typically done at lower temperatures where emissions tend to be higher.
In addition, the cost of alternative fuels can often be lower than fossil fuels and is not subject to the fluctuations of the energy market.
The sources of alternative fuels are many and varied – to the extent that the supply chain looks vastly different from one region to the next. For example, whereas India has abundant sources of biomass such as rice husk, in Western Europe there are plentiful supplies of refuse-derived fuel (RDF). This is partly a matter of industry and partly of infrastructure. But given the importance of reducing the cement industry’s reliance on coal, a lack of infrastructure must not prevent greater utilisation of alternative fuels – which is why FLSmidth Cement has for some time been developing alternative fuels solutions that reduce the burden of pre-processing and enable cement plants to more easily and more cost-effectively utilise a wide variety of waste streams.
A solution for all waste
Direct calciner injection may seem like the simplest way to replace fossil fuels with alternatives. However, it’s not always the best. The options for alternative fuels are limited by the necessity to pre-process fuel in preparation for burning, which, as stated, requires established infrastructure, or additional facilities at the plant.
Though the CAPEX cost of direct calciner injection is low, the calciner fuel substitution rate is also low, so this method doesn’t enable cement plants to optimise the potential for fuel replacement. Plant operators must also consider the impact on the process of direct injection, which doesn’t allow the long residence time that can be required to reduce process volatility. No plant wants to contend with greater instability or an increase in emissions from adding alternative fuels to the mix. Fortunately, direct calciner injection is not the only option. There are other ways of extracting energy from waste that require no pre-processing at all.
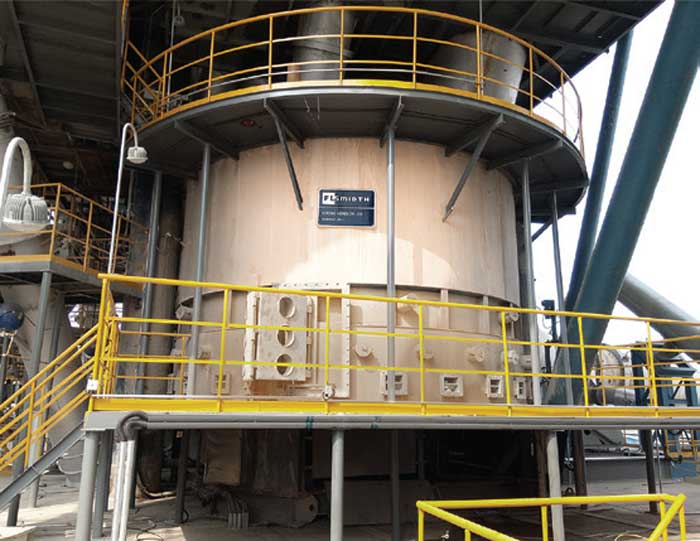
The HOTDISC® Reactor can handle a wide variety of solid waste in sizes up to 1.2m – from sludge or grains to whole truck tyres. There’s no need for expensive shredding or pre-drying, or any pre-processing, which removes one of the obstacles to adopting alternative fuels. The broad range of accepted fuel types also means cement plants are free to shop the market and not tied into one supplier. This makes it a very cost-effective solution because cement plants can select the lowest cost fuel without worrying about the quality.
How does the HOTDISC® work?
The HOTDISC® is a moving hearth furnace that is integrated into the pyroprocess below the calciner bottom and above the kiln riser. Coarse alternative fuels are fed onto a slowly rotating disc. Hot tertiary air is directed into the HOTDISC to provide an oxidising atmosphere for the alternative fuel to burn. As the alternative fuel slowly travels around approximately 270 degrees on the rotating disc, almost all of it fully combusts. Depending on the nature of the alternative fuel (size, heat content, moisture, etc.), the rotational speed of the HOTDISC can be adjusted to optimise the residence time (up to 45 minutes) and combustion rate. In addition, the temperature inside the HOTDISC is controlled by directing a portion of the preheated raw meal into the HOTDISC. The HOTDISC operation generates a controlled mix of hot gases, combustion residue (ash) and calcined raw meal that exits the HOTDISC. The combustion gases and finer materials are carried with the hot gases into the bottom of the calciner, while the coarser residues meet a scraper at the end of the 270 degrees rotation, where they are directed down into the riser duct. From there, this material falls into the kiln and is incorporated into the clinker.
The HOTDISC is designed to achieve a calciner substitution rate in the range of 50 to 80 per cent – or even higher – of the calciner fuel. Results vary by the specific plant conditions and fuel specification, but based on over 20 years of plant data it is possible to predict the substitution rate in each application.
The HOTDISC was originally designed for use with In-Line Calciners (ILCs), but new models are now available for use with Separate Line Calciners (SLCs), enabling the HOTDISC to be installed under the calciner and still deliver the same benefits. The HOTDISC-S is installed in the bottom part of the SLC calciner on the ground, the reject will be cooled and transported to a container or back into the system, gas flow and AF flow operates counter current.
For cement plants that wanted to utilise a wide range of alternative fuels, the HOTDISC®-S is a cost-saving solution that avoids the expense of changing the SLC to an ILC while enabling a high substitution of alternative fuels. Another model, the HOTDISC®-HMT (Hot Material Transport), enables quicker and easier installation of the HOTDISC in existing plants. Instead of directly integrating the exit of the HOTDISC reactor to the calciner and riser duct, the new layout allows the HOTDISC reactor to be mounted two to five metres away. It is then connected to the calciner and riser duct via a hot material transport chute for gas flows and combustion ashes.
Further advances in alternative fuels technologies
Low or varying quality alternative fuels can be another inhibitor to substitution, given the requirements of the relatively delicate cement pyro process. FLSmidth Cement has expended considerable R&D effort developing solutions that can accommodate a wide range of fuel types, knowing that this is the easiest path to greater substitution and ultimately the near-elimination of fossil fuels. The FUELFLEX® Pyrolyzer was one result of this effort and offers an exciting prospect for cement plants wishing to achieve near – 100 per cent substitution in the calciner and minimise NOx emissions.
The FUELFLEX® Pyrolyzer utilises hot meal from the lower preheater cyclones (yellow arrows) to dry and pyrolyze RDF or biomass. Either part or the full stream of hot meal from a lower preheater cyclone is admitted to the Pyrolyzer via the U-Lock (controlled by two dividing gates). The U-Lock fluidises the hot meal, forming a U-shaped gas lock that prevents pyrolysis gases from flowing backwards through the process. Subsequently the hot meal stream flows into the Pyrolyzer vessel, which also has a U-shaped lower aerated section to contain the hot fluidised meal. Fuel is pneumatically fed to the pyrolyzer vessel wherein through contact with the hot meal, it is dried, heated and pyrolyzed to form reactive gases and char. The gases push upwards into the main pyrolyzer vessels while the char falls down into the fluidised meal bed, before being reunited and fed as a very reactive stream into the calciner. Aeration panels are used to fluidise the hot meal and drain gates are used to drain out debris and meal from the pyrolyzer to the kiln system in a controlled manner. The reactive stream of pyrolysis products reacts with rotary kiln NO by so-called ‘re-burning’ reactions, utilising pyrolysis gases to convert NO into free N2 in the reduction zone prior to mixing with preheated combustion air in the calciner. In addition, the full fuel pyrolysis preceding the calciner helps limit calciner NOx formation by limiting access to oxygen when burning.
By using the FUELFLEX® Pyrolyzer, cement plants can achieve up to 100 per cent fossil fuel replacement in the calciner, with the following benefits:
- Reduced CO2 emissions, as net CO2 emissions from alternative fuels generally are lower than from fossil fuels.
- Increased utilisation of local waste streams, avoiding the need to dispose of or store this waste in other ways.
- Reduced fuel costs, especially in times of fluctuating energy prices.
- Reduced fossil fuel use saves the associated environmental impact of fossil fuel extraction and transport.
Conclusion
The challenge is on: cement plants must reduce carbon emissions now, and continue to do so for the next several decades until the target of net zero is met. While there are some solutions that are not ready yet – i.e. carbon capture – alternative fuels offer a valuable means of reducing the cement industry’s environmental impact immediately, with the added benefit of providing a controlled means of waste disposal. New and proven technologies will help the cement industry to overcome alternative fuel supply chain problems and achieve a dramatic reduction in fossil fuel use.
(Communication by the management of the company)














 Concrete4 weeks ago

 Concrete3 weeks ago

 Concrete4 weeks ago
 Concrete3 weeks ago