Connect with us

Concrete

Cement industry should look at real time data and not just data

Published

on

Shares

Keyur Shah, Business Manager, SB Engineers, gives a detailed account of how refractories can be made more efficient and sustainable, thereby making the manufacturing process more eco-friendly.

Tell us about the solutions you provide to cement companies to measure and monitor their processes.
We are partners with a company called Thermoteknix Systems Ltd, which is a UK-based company, located in Cambridge that has been providing thermal imaging solutions for the cement industry for over 30 years now. The thermal imaging solutions mainly are kiln shell scanning systems, the function of which is to monitor shell temperature of the rotating kiln.
We also have a burning zone monitoring system or burning zone CCTV and a clinker cooler monitoring system or clinker cooler CCTV.
These are the three major solutions in the thermal imaging area, which we have been providing to the cement industry.

How do your products help cement manufacturers optimise their processes?
Our first product category is the kiln shell scanning system, which very closely monitors the outer shell temperature of the rotating kiln. It gives information about what is the condition of the refractory inside, because there is the material passed through the kiln and the coating inside the kiln that keeps on building and collapsing. So, there is the thickness of the coating as well as thickness of the brick, which indirectly is reflected by the shell temperature of that kiln.
This system monitors the temperature and provides a reading for every single brick of the kiln. The first advantage of using this system is that it informs about the condition of the refractory. If it is too thin it gives you an early alarm to take action which helps avoid any sort of shut down. Shutdowns or any kind of breakdowns are a costly affair. Also, in parallel if there is an abnormality of temperatures along the length of the kiln or across the circumference of the kiln, which is caused by the uneven coating or the failure of the brick, there is an alert that sounds averting unwanted breakdowns, thus, saving cost.
Our second category is a kiln burning zone camera. Conventionally, the burning zone was monitored by installing a CCTV installed on the kiln, which allowed a process person to monitor what is happening in the burning zone, how the flame is doing and how the material is getting processed or condition of the material inside.
Typically for a cement plant approximately 40 to 45 per cent of the fossil fuel (coal) or any other fuel is burnt in this zone. A massive amount of money is being spent in this process of transforming raw material to clinker. The process person can only have an idea of what is happening but not any data.
Thermoteknix has introduced thermal imaging for monitoring the burning zone, as cement companies spend a lot of money in the process and having visual information is not sufficient for modern plants. Therefore, thermal imaging gives information about the temperature and at the same time gives the visual views and helps with the understanding of temperature, flame, temperature of outgoing clinker, temperature of nose ring, temperature of rising material etc. Any person monitoring this system can take appropriate action accordingly.
Data from this system gives better control to the plant and process monitoring. It allows for optimising processes. It helps with any adjustment of the fuel being pumped or to the burning zone, burner air, axil air or any other air, which is being provided to the burner. Available data also helps to make process improvements that helps optimise all critical processes at the cement plants.
Our third category is clinker cooler monitoring. Once the burning process is complete, the materials move out to cool into the clinker cooler to bring down the temperature. Conventionally, the cooler was monitored by a colour CCTV for the purpose of understanding visual aspects of cooling. This slowly became a bottle neck.
Modern cement plants, however, take hot air and feed it into the boiler for regeneration of power. In this case, if the thermal process of the cooler is monitored and the profile of the cooler bed and top are known, the pumping of the air or fan of the cooler can be controlled at the same time. The suction of air taking place from the cooler can be controlled for power generation, which in turn, helps optimise the cooler operations and the AQC boiler or cooler operations as well.

What is the impact of your solutions on the cost efficiency of cement manufacturing?
It is difficult to give a set number, but I will give the cost impact in general.
In the use of kiln shell temperature scanners, there are two aspects: to avoid breakdowns, which cost millions of dollars, and to enhance the service life of the refractory for one or two months, which again means huge money saving for the cement plants. This however, is difficult to quantify but is surely an amount that makes a difference.
Coming to the thermal imaging for burning zone monitoring system, let us say the plant can save only 0.5 per cent of the fuel being pumped or coal being pumped into the burning zone and optimise it by approximately 0.25 percent, that too is a significant amount of money.
Speaking about the cooler, when there is control on the energy given to the cooling fan and suction of air for regeneration of power is controlled, that saves a significant amount of money.

What are the major challenges you face in terms of the cement industry?
A major challenge as of now for us occurs because the cement industry is undergoing transformation from technically automation run plants to data driven running plants. This transformation furthering the adaptability of these new changes by the plant operators or by the plant operations team is a major challenge. But any transformation is painful and this transformation is slowly taking place. The challenge we face is the integration or collaboration of the plant in terms of offering them this solution and making sure it is used for effective purposes.

Are you working on any innovations that the cement industry can look forward to?
In addition to offering thermal imaging we also offer process improvement solutions and these are new and innovative solutions for the cement industry.
The particle sizing system is a measurement of the fineness of the cement by the cement plant. It was traditionally done or is still done by Blaine apparatus as an ISO requirement and is also being done on laboratory basis. We have introduced this as an innovative solution with an in-process particle sizing system, which means that the particle size of the final product is measured instantaneously and live data is available to the plant process team. They use this data for optimising their cement mill or even the raw mill.
It is said that 1 to 4 per cent of the world’s power is consumed for cement grinding. Through the use of automated systems, if this absolute power is improved by even 4 to 5 per cent, it contributes to a huge amount of cost saving for cement plants and allows to deliver consistent product quality. This is one of the most innovative solutions we have successfully introduced into various cement plants globally and in India.
Another most innovative solution we have introduced to the Indian cement industry is the gas flow measurement or the air flow measurement in a cement plant at various locations. Be it at the raw mill, tertiary duct, be it down comer, be it AQC duct, hot and dusty gas flows everywhere, which is laden with a lot of energy. This energy can be used in a modern cement plant for the generation of power.
The venturi system is a mechanical system, which is conventionally used in cement plants to measure dust in the flow of air and gas. It often gets clogged up and the results and readings are not accurate or satisfactory. We have joined hands with Promecon, a German company, and are offering a flow measurement system which works on a triboelectric system that does not involve mechanical devices. It is an electronic flow measurement system which does not require calibration, thus, giving reliable data repeatedly. This has also translated to bringing large cost savings to cement plants.
So, the cement industry should look at real time data and not just data. They used to have periodic data, laboratory data and a manual sample based collection data, and from there they should move to automated real time data, which can be used for process improvement. Going forward, this will become learning for good feeds of raw material, for machine learning and AI. These are likely to become trends in any cement plant.

-Kanika Mathur

Concrete

CII Calls for Greater Alternative Fuel Use in Cement Industry

Published

on

By

Shares

The Confederation of Indian Industry (CII), through its Green Business Centre and Energy Efficiency Council, inaugurated the 16th Conference on Alternative Fuel and Raw Material Usage (AFR) in Goa on 27 October 2026. The two-day conference brought together more than 350 industry leaders, policymakers, waste management experts and technology providers to explore strategies for accelerating alternative fuel adoption in India’s cement industry.

Held under the theme ‘Preparation for Net-Zero: Alternative Fuels & Raw Material in Cement Manufacturing’, the conference focused on reducing dependence on conventional fuels, improving waste utilisation and strengthening circular economy practices across cement manufacturing operations.

E R Raj Narayanan, Chairman, AFR Conference 2026, and Business Head and Chief Manufacturing Officer, UltraTech Cement, highlighted the industry’s progress in alternative fuel adoption. He emphasised the need to scale implementation, strengthen supply chains and extend circularity beyond fuel substitution to alternative raw materials through technological innovation and industry collaboration.

Harish Adconkar, Managing Director, Goa Waste Management Corporation, highlighted Goa’s progress in scientific waste management and refuse-derived fuel (RDF) production. He stated that approximately 765,000 tonnes of RDF had been supplied to cement plants, contributing to an estimated displacement of 320,000–560,000 tonnes of coal. He emphasised the importance of consistent RDF offtake and stronger coordination between urban local bodies, waste management agencies and cement manufacturers.

Dr L P Singh, Director General, National Council for Cement and Building Materials, identified AFR as an important opportunity for decarbonisation and resource efficiency. Drawing parallels with the industry’s successful utilisation of fly ash, he stressed the need to address quality, technological and economic challenges to expand alternative fuel adoption.

Dr Sharad P Kale, Special Advisor to the Chief Minister of Goa and former Head of Technology Transfer and Collaboration at BARC, emphasised treating waste as a resource. He highlighted decentralised biodegradable waste processing, reduced food waste and improved resource recovery as essential measures for minimising landfill dependence.

Kiran Ananth, Executive Director, Energy Efficiency, Renewable Energy and Green Entrepreneurship, CII-Green Business Centre, noted that India’s cement production reached approximately 491 million tonnes in FY2025-26, while the industry’s thermal substitution rate (TSR) stood at 7.5 per cent, with around 7 million tonnes of alternative fuels utilised annually.

He added that the industry had invested over Rs 12 billion in co-processing infrastructure during the past six years. Improving RDF supply reliability and quality assurance would be crucial to maximising the utilisation of existing infrastructure and accelerating industrial decarbonisation.

The conference also featured discussions on advanced AFR co-processing technologies, waste pre-processing solutions and industrial best practices for improving fuel substitution and resource recovery.

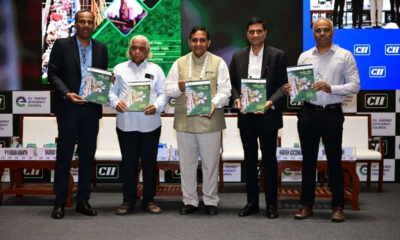
A publication titled ‘From Waste to Kiln: Scaling the Use of MSW-Derived RDF in Indian Cement Plants’ was launched during the inaugural session. The report identified inconsistent RDF supply and quality as major barriers to achieving higher thermal substitution rates.

According to the publication, many cement kilns already possess the technical capability to achieve higher alternative fuel substitution. However, variations in RDF availability, moisture content, particle size and calorific value continue to limit utilisation. The report emphasised the need to strengthen waste segregation, pre-processing and aggregation systems to establish reliable RDF supply chains.

The conference’s second-day agenda includes discussions on innovative domestic and industrial waste management solutions, alternative raw materials for low-carbon cement and strategies to increase alternative fuel utilisation across India’s cement manufacturing sector.


Continue Reading

Concrete

Sameera Group Enters Industrial and Logistics Real Estate

Rs. 1.5 bn project to support manufacturing and supply-chain firms

Published

on

By

Shares


Sameera Group has entered the industrial and logistics real estate segment with a 450,000 sq ft development in Sriperumbudur, Chennai. The group will invest Rs. 1.5 bn in the project, expanding beyond residential plotted developments into business-to-business real estate.

The proposed park will serve light manufacturing, e-commerce, third-party logistics and other supply-chain businesses. Building plan approvals have been secured, with construction expected to begin shortly. The development is scheduled to become operational within 12 to 15 months.

Sameera Group Managing Director and Chief Executive Officer Jayakumar Murugesan said the project marked the next stage of the company’s growth after nearly four decades in land acquisition and real estate development. He attributed the choice of Sriperumbudur to its industrial activity and growth prospects.

The Grade A development will include internal movement routes and shared infrastructure for modern manufacturing and logistics operations. The group is pursuing Indian Green Building Council (IGBC) Platinum certification and plans to provide rooftop solar readiness, rainwater harvesting, wastewater recycling, energy and water monitoring, and electric vehicle charging facilities.

The project is being developed amid increased demand for industrial and warehousing space in Chennai. Knight Frank’s India Warehousing Market Report 2026 recorded 8.3 mn sq ft of warehousing transactions in the city during 2025, up 42 per cent from the previous year, with manufacturing accounting for 59 per cent of demand. The Sriperumbudur-Oragadam cluster contributed 77 per cent of transactions.

Sameera Group plans to develop 5 to 6 mn sq ft across a larger industrial and logistics portfolio over the next five years, involving an estimated investment of Rs. 18 bn. Land has been acquired for projects in Chennai, Hosur and Bengaluru. Established in 1982, the group has developed more than 900 acres, sold over 13,700 residential plots, and currently has 35 projects under development and 28 in its pipeline.

Continue Reading

Concrete

UltraTech Cement Expands in Andhra Pradesh with Rs. 26.5 bn

Petnikota plant adds 3.6 MTPA cement dispatch capacity

Published

on

By

Shares


UltraTech Cement has expanded its manufacturing footprint in Andhra Pradesh with the commissioning of Petnikota Cement Works, an integrated cement plant built with an investment of around Rs. 26.5 bn. The facility is located in Petnikota village in Kolimigundla mandal of Nandyal district, in the Rayalaseema region.

Construction of the plant began in May 2025. The facility has a clinkerisation capacity of 3.3 MTPA and a cement dispatch capacity of 3.6 MTPA, strengthening the company’s production and distribution presence in the State.

The plant is expected to provide direct employment to 650 people and indirect employment to another 2,000. It has been designed to operate entirely on green energy and does not have a captive thermal power plant. The project also uses no groundwater, according to information released by the Andhra Pradesh Government.

Nara Lokesh, Andhra Pradesh Minister for Information Technology, said in the release that the facility was taken from groundbreaking to commissioning in 14 months. He described the project as a state-of-the-art addition to the company’s operations in the State and said it would create 2,650 direct and indirect employment opportunities.

Petnikota Cement Works adds to UltraTech Cement’s manufacturing capacity in Andhra Pradesh while supporting industrial activity in Nandyal district. The plant’s energy design and stated groundwater-use policy are also intended to reduce the environmental impact of its operations. The company has identified the facility as part of its continuing capacity expansion in the Indian cement market.

Continue Reading

Video Thumbnail
â–

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds