Connect with us

Economy & Market

Shree Cement: The New Sustainability

Published

on

Shares

Champion 10 factors that helped it make the gradeThere is a reason for putting Shree Cement on the cover in this issue. For an industry much maligned for its environmental impact, it is always welcome when members of this sector are honoured for their ability to practice innovative business solutions with sustainable development activities. The World Economic Forum (WEF) and Boston Consulting Group (BCG) by identifying and honouring Shree Cement as one of the 16 new Sustainability Champion Companies, has ensured that the sector will work even more zealously to earn more laurels for the sector.World Economic Forum (WEF) and Boston Consulting Group (BCG) have worked globally to identify New Sustainability Champion Companies that practice innovative business solutions with sustainable development objectives. As an initial part of this identification process, over 11 million projects / companies were screened. Following which, a few companies were further selected through a due diligence process, taking into consideration the sustainability aspect inculcated by them in their business. The top management personnel from around 200 of these short-listed companies were then engaged in a personal interview. They were interviewed on various related fields, considering their approach and work towards sustainability, innovation, scalability, geography and size. Based upon a detailed interview of Prashant Bangur, Executive Joint President of Shree Cement Limited (SCL), WEF identified SCL as one amongst 16 New World Sustainability Champions.Driving sustainabilityShree Cement inculcates sustainability in its business frame work based on the philosophy ‘Aah NA Bhadra: Kratavo Yantu Vishwatah’ (Let noble thought come to us from all over the world). The company’s sustainability policy aims to produce quality cement in in a socially responsible manner, with an eco-friendly, healthy and safe working environment approach, working toward continual improvement in the performance level."Our continual thirst to become steward in all spheres has led us to this reputed platform where we stand today," says Prashant Bangur, Executive Joint President of Shree Cement.The company has a 10-fold approach to ensure sustainability in all operations:Creativity and innovationShree Cement encourages its employees to think ‘Out of Box’, its "Jo Soche Wo Pave" scheme encouraged employees to provide innovative ideas and suggestions which are rewarded and communicated to spread the culture of innovative thinking."We believe that success comes through failure. Allowing failures encourage creative thinking and develop the attitude of creativity, risk taking and ultimately high performance," says Prashant Bangur.Employee creative ideas and innovations:

  • Developed synthetic gypsum to replace mineral gypsum for the first time in India.
  • Set a world record of commissioning a brown field clinkerization unit in a record time of 330 days.
  • Set a world record of commissioning a 46 MW of Waste Heat Recovery Based Green Power Plant in 17 months against the industry standard of 24 months.
  • Air lifted coal and raw mill from Germany to reduce the project execution time.
  • Installed the second largest waste heat recovery system in the world.

Resource and Energy ConservationA holistic view of Sustainability and care for the future generation through:

  • Conserving resources to ensure its availability for the future generation
  • Reducing emissions, cleaning environment and combating climate change

As an attempt to conserve fossil fuel, Shree Cement pioneered the use of petcoke as a replacement of fossil coal for the first time in India. Pet-coke has the properties of high sulphur, low volatile matter and harder grinding. Use of pet-coke came along with lots of constraints such as kiln jamming, low production and product quality but it also came as an opportunity to save precious fossil fuels. The company carried out extensive R&D and succeeded in pioneering its 100 per cent usage both in cement and power.Another initiative was to install India’s largest Air Cooled Condenser in its 2 X 150 MW power plant to replace the conventional water-cooled condensers, that ensured a current savings of 1 million KL water every year.One of the first process and cement manufacturing company in the world to obtain BS-EN 16001 Energy Management Certification, Shree Cement maintains one of lowest specific energy consumption for manufacturing its products.Environment FriendlinessThe company follows the philosophy of a Low Carbon Economy and work while following the maxim of clean and green is profitable. "They are members of various climate change initiatives like Cement Sustainability Initiative under the auspices of World Business Council of Sustainable Development (WBCSD)- Switzerland, GRI, TERI-BCSD etc.Waste UtilizationShree Cement began optimal use of fly ash in the cement manufacturing process in order to address the issues of fly ash disposal of power plants, while providing affordable cement to consumers and making planet better place. Use in cement makes the fly ash value added product thereby conserving limestone and fuels. The practice of using fly ash upto 35 per cent (which is maximum limit allowed by law), resulted in Shree Cement becoming the first cement manufacturing company in India to obtain CDM benefits for the same beginning July 2000.Similarly, the disposal of lead zinc slag was a serious problem for the zinc smelters. "However, our zeal to be opportunistic manufacturer provided us the threshold to utilise lead zinc slag, a waste of other industry thereby making us capable for laterite replacement from our operation. It also marked our "industrial ecologist" instinct. Besides, we have also demonstrated the use of agro-waste as a fuel replacement which is under validation for obtaining CDM benefits," says Prashant Bangur.The policy of Zero Disposals on LandMaintaining the lowest cost of production through:

  • Continual benchmarking with best achievements within Shree Cement and outside
  • Culture of challenging the established norms to find scope for further improvement
  • Focus on use of alternate raw material and fuels.

Empowering PeopleThe company empowers people by providing them with challenging roles, higher responsibilities, multi-skill jobs, faster career growth and healthy working practices; and encourage the youth.Engaging Local CommunityThe company promotes maximum employment from local community, in order to generate sustainable livelihood by assisting local community to engage in various livelihood creation activities. To ensure total prosperity in the community, it actively engages in initiatives focusing on infrastructure and water harvesting structure development, healthcare and women empowerment programs, educational awareness programs and plantation activities.Embracing New Technology"Our continuous focus is on technologies for enabling faster decisions through increasing speed and accuracy and releasing time which can be put to other productive uses," says Bangur. It is one of the first cement companies to implement ‘Operator Independent Truck Dispatch System’ at mines for automated truck dispatch. It also introduced remote surveillance system to track progress of projects on real time basis from office.Health and SafetyThe company’s facilities are certified to the OHSAS 18001:2007 standard. Committed to achieving its goal of becoming ‘Zero Accident Work Place’, Personal Protective Equipment is provided to all workers on the shop floor and their use is strictly enforced.Transparency and GovernanceThe company maintains an open door policy of inviting competitors and outsiders to visit its plants to interchange ideas. "We have highly analytical annual report covering detailed financial and non financial information. We are the first cement company to issue Corporate Sustainability Report based upon GRI guidelines," says Prashant Bangur.Successful implementation of some of the projects at SCL:-Thermal power plants have traditionally used Water Cooled Condenser (WCC) systems. Bearing in mind the location of our operations in one of India’s most water scarce regions, we operationalized the switch from a Water Cooled Condenser to Air Cooled Condenser system. Retrofitting of the old system to convert it to ACC was a challenging task requiring considerable skill; the retrofitting task was completed and the ACC was commissioned without any alignment problems.Implementation of air cooled condensers at its power plant in Beawar has enabled reduced water consumption by about 70 per cent.Waste heat utilization of Preheater & clinker coolerTwo major sources of heat rejection In a cement plant are pre-heater and clinker cooler hot gases. Waste heat recovery system installation in these two sources not only generates electricity also saves water for cooling down the gases. "Our earlier experience with the waste heat boiler in unit-I gave a strong background for installation of waste heat recovery system in other units with improved systems to generate electricity as well as to save the water used to cool down the gases," says Bangur. This has reduced water consumption by about 85 per cent in the power plant and 50 per cent in clinker production.

Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

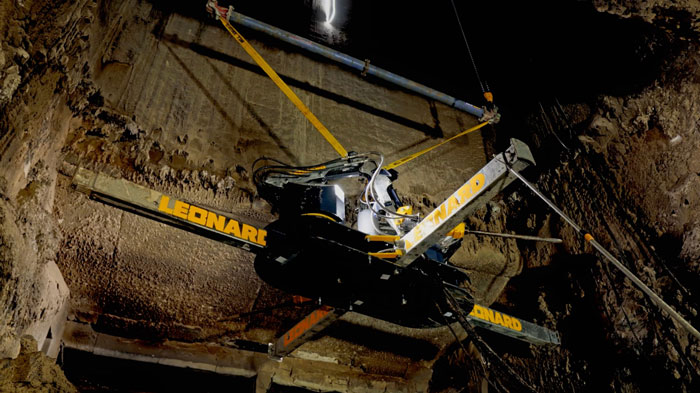
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.

Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

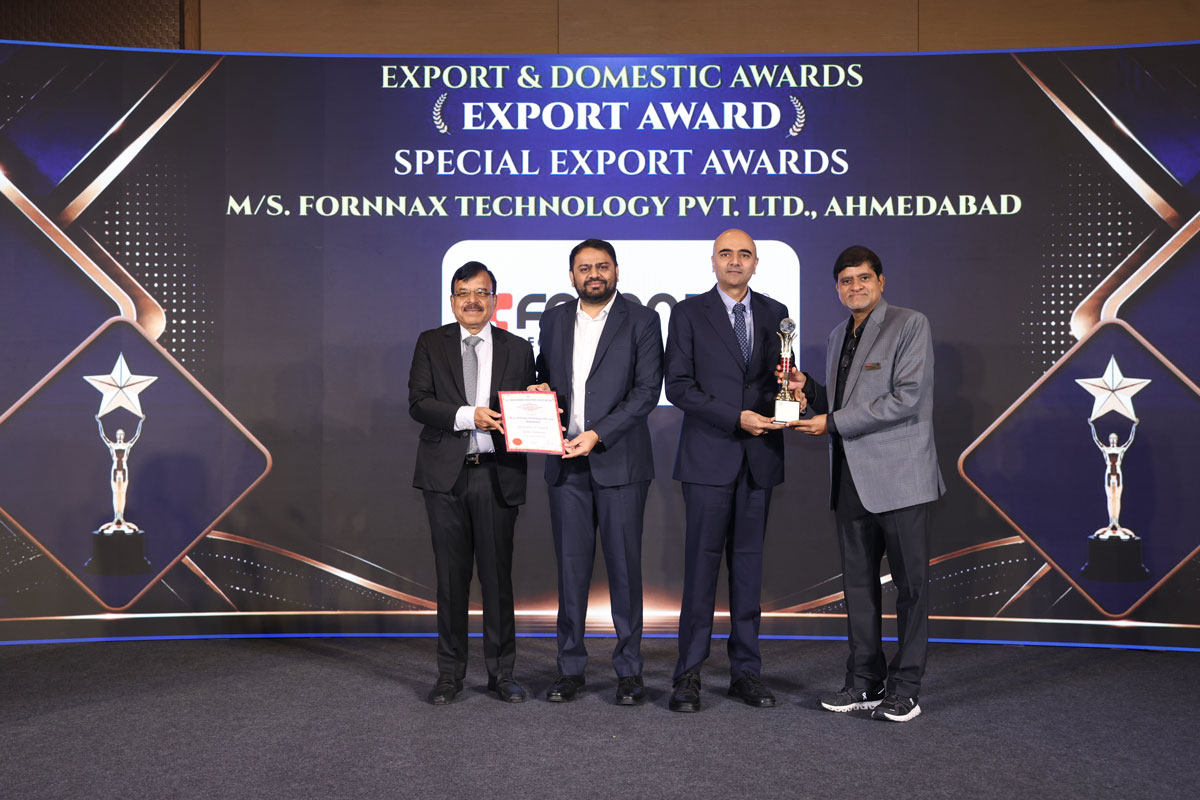
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    Economy & Market

    Shree Cement: The New Sustainability
    Published

    on

    Shares


    Champion 10 factors that helped it make the gradeThere is a reason for putting Shree Cement on the cover in this issue. For an industry much maligned for its environmental impact, it is always welcome when members of this sector are honoured for their ability to practice innovative business solutions with sustainable development activities. The World Economic Forum (WEF) and Boston Consulting Group (BCG) by identifying and honouring Shree Cement as one of the 16 new Sustainability Champion Companies, has ensured that the sector will work even more zealously to earn more laurels for the sector.World Economic Forum (WEF) and Boston Consulting Group (BCG) have worked globally to identify New Sustainability Champion Companies that practice innovative business solutions with sustainable development objectives. As an initial part of this identification process, over 11 million projects / companies were screened. Following which, a few companies were further selected through a due diligence process, taking into consideration the sustainability aspect inculcated by them in their business. The top management personnel from around 200 of these short-listed companies were then engaged in a personal interview. They were interviewed on various related fields, considering their approach and work towards sustainability, innovation, scalability, geography and size. Based upon a detailed interview of Prashant Bangur, Executive Joint President of Shree Cement Limited (SCL), WEF identified SCL as one amongst 16 New World Sustainability Champions.Driving sustainabilityShree Cement inculcates sustainability in its business frame work based on the philosophy ‘Aah NA Bhadra: Kratavo Yantu Vishwatah’ (Let noble thought come to us from all over the world). The company’s sustainability policy aims to produce quality cement in in a socially responsible manner, with an eco-friendly, healthy and safe working environment approach, working toward continual improvement in the performance level."Our continual thirst to become steward in all spheres has led us to this reputed platform where we stand today," says Prashant Bangur, Executive Joint President of Shree Cement.The company has a 10-fold approach to ensure sustainability in all operations:Creativity and innovationShree Cement encourages its employees to think ‘Out of Box’, its "Jo Soche Wo Pave" scheme encouraged employees to provide innovative ideas and suggestions which are rewarded and communicated to spread the culture of innovative thinking."We believe that success comes through failure. Allowing failures encourage creative thinking and develop the attitude of creativity, risk taking and ultimately high performance," says Prashant Bangur.Employee creative ideas and innovations:

    • Developed synthetic gypsum to replace mineral gypsum for the first time in India.
    • Set a world record of commissioning a brown field clinkerization unit in a record time of 330 days.
    • Set a world record of commissioning a 46 MW of Waste Heat Recovery Based Green Power Plant in 17 months against the industry standard of 24 months.
    • Air lifted coal and raw mill from Germany to reduce the project execution time.
    • Installed the second largest waste heat recovery system in the world.

    Resource and Energy ConservationA holistic view of Sustainability and care for the future generation through:

    • Conserving resources to ensure its availability for the future generation
    • Reducing emissions, cleaning environment and combating climate change

    As an attempt to conserve fossil fuel, Shree Cement pioneered the use of petcoke as a replacement of fossil coal for the first time in India. Pet-coke has the properties of high sulphur, low volatile matter and harder grinding. Use of pet-coke came along with lots of constraints such as kiln jamming, low production and product quality but it also came as an opportunity to save precious fossil fuels. The company carried out extensive R&D and succeeded in pioneering its 100 per cent usage both in cement and power.Another initiative was to install India’s largest Air Cooled Condenser in its 2 X 150 MW power plant to replace the conventional water-cooled condensers, that ensured a current savings of 1 million KL water every year.One of the first process and cement manufacturing company in the world to obtain BS-EN 16001 Energy Management Certification, Shree Cement maintains one of lowest specific energy consumption for manufacturing its products.Environment FriendlinessThe company follows the philosophy of a Low Carbon Economy and work while following the maxim of clean and green is profitable. "They are members of various climate change initiatives like Cement Sustainability Initiative under the auspices of World Business Council of Sustainable Development (WBCSD)- Switzerland, GRI, TERI-BCSD etc.Waste UtilizationShree Cement began optimal use of fly ash in the cement manufacturing process in order to address the issues of fly ash disposal of power plants, while providing affordable cement to consumers and making planet better place. Use in cement makes the fly ash value added product thereby conserving limestone and fuels. The practice of using fly ash upto 35 per cent (which is maximum limit allowed by law), resulted in Shree Cement becoming the first cement manufacturing company in India to obtain CDM benefits for the same beginning July 2000.Similarly, the disposal of lead zinc slag was a serious problem for the zinc smelters. "However, our zeal to be opportunistic manufacturer provided us the threshold to utilise lead zinc slag, a waste of other industry thereby making us capable for laterite replacement from our operation. It also marked our "industrial ecologist" instinct. Besides, we have also demonstrated the use of agro-waste as a fuel replacement which is under validation for obtaining CDM benefits," says Prashant Bangur.The policy of Zero Disposals on LandMaintaining the lowest cost of production through:

    • Continual benchmarking with best achievements within Shree Cement and outside
    • Culture of challenging the established norms to find scope for further improvement
    • Focus on use of alternate raw material and fuels.

    Empowering PeopleThe company empowers people by providing them with challenging roles, higher responsibilities, multi-skill jobs, faster career growth and healthy working practices; and encourage the youth.Engaging Local CommunityThe company promotes maximum employment from local community, in order to generate sustainable livelihood by assisting local community to engage in various livelihood creation activities. To ensure total prosperity in the community, it actively engages in initiatives focusing on infrastructure and water harvesting structure development, healthcare and women empowerment programs, educational awareness programs and plantation activities.Embracing New Technology"Our continuous focus is on technologies for enabling faster decisions through increasing speed and accuracy and releasing time which can be put to other productive uses," says Bangur. It is one of the first cement companies to implement ‘Operator Independent Truck Dispatch System’ at mines for automated truck dispatch. It also introduced remote surveillance system to track progress of projects on real time basis from office.Health and SafetyThe company’s facilities are certified to the OHSAS 18001:2007 standard. Committed to achieving its goal of becoming ‘Zero Accident Work Place’, Personal Protective Equipment is provided to all workers on the shop floor and their use is strictly enforced.Transparency and GovernanceThe company maintains an open door policy of inviting competitors and outsiders to visit its plants to interchange ideas. "We have highly analytical annual report covering detailed financial and non financial information. We are the first cement company to issue Corporate Sustainability Report based upon GRI guidelines," says Prashant Bangur.Successful implementation of some of the projects at SCL:-Thermal power plants have traditionally used Water Cooled Condenser (WCC) systems. Bearing in mind the location of our operations in one of India’s most water scarce regions, we operationalized the switch from a Water Cooled Condenser to Air Cooled Condenser system. Retrofitting of the old system to convert it to ACC was a challenging task requiring considerable skill; the retrofitting task was completed and the ACC was commissioned without any alignment problems.Implementation of air cooled condensers at its power plant in Beawar has enabled reduced water consumption by about 70 per cent.Waste heat utilization of Preheater & clinker coolerTwo major sources of heat rejection In a cement plant are pre-heater and clinker cooler hot gases. Waste heat recovery system installation in these two sources not only generates electricity also saves water for cooling down the gases. "Our earlier experience with the waste heat boiler in unit-I gave a strong background for installation of waste heat recovery system in other units with improved systems to generate electricity as well as to save the water used to cool down the gases," says Bangur. This has reduced water consumption by about 85 per cent in the power plant and 50 per cent in clinker production.

    Continue Reading
    Click to comment

    Leave a Reply

    Your email address will not be published. Required fields are marked *

    Economy & Market

    Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

    Published

    on

    By

    Shares

     Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

    Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

    Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

    Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

    Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

    According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

    First Deployment Demonstrates Shutdown Efficiency

    The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

    Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

    Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

    Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

    The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

    “The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

    “When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

    Expanding Industrial Robotics Applications

    Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

    Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

    Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

    The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.

    Continue Reading

    Concrete

    Martin Engineering Appoints Ashwini Khunte as India General Manager

    Published

    on

    By

    Shares

    Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

    Pune

    Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

    Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

    A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

    In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

    Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

    Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

    “Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

    Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.
    Continue Reading

    Concrete

    Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

    Published

    on

    By

    Shares

    Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

    With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

    The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

    Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

    “This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

    Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

    The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

    Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

    For more information, visit: www.fornnax.com

    Continue Reading

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds