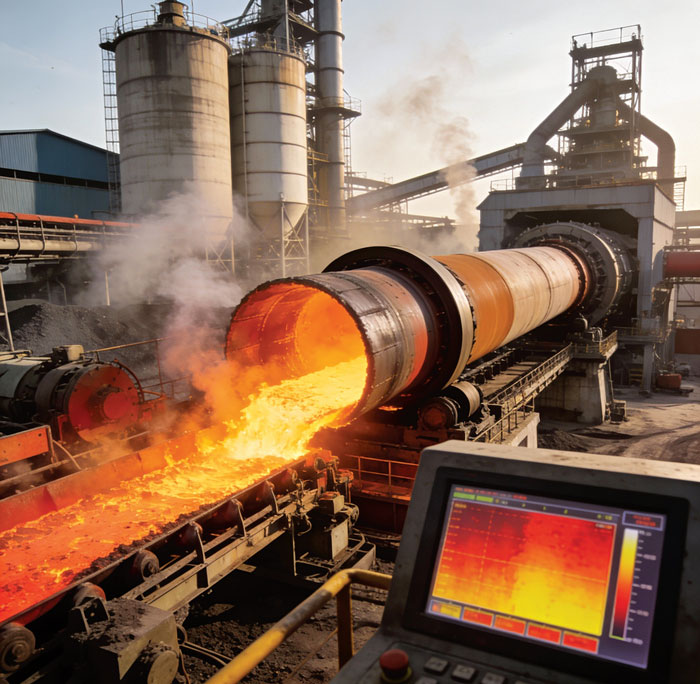
From AFR-driven chemistry shifts to digitalised kiln monitoring, refractory strategy has become central to operational stability and cost control. Plants that treat refractories as strategic assets and not consumables are redefining efficiency in the modern cement industry. ICR delves into the innovations in refractories and their repercussions on pyroprocessing efficiency in India’s cement industry.
Refractories form the quiet backbone of cement pyroprocessing—absorbing thermal shocks, resisting corrosive chemical attacks, and maintaining process continuity in the most extreme conditions of the plant.
While kiln drives, heat exchangers and burners often dominate conversations, the refractory lining allows a kiln to operate at 1,400–1,500°C daily without structural damage. According to the World Refractories Association, the cement sector accounts for nearly 30 per cent of refractory demand in construction materials industries, driven by the need for monolithic castables, high-alumina bricks and magnesia-based linings. Meanwhile, a report by the Indian Minerals Yearbook states that India is among the top refractory-consuming markets in Asia, driven by capacity expansions, debottlenecking and higher AFR substitution in integrated plants.
What makes refractories strategically important is their direct influence on clinker cost, fuel consumption and kiln efficiency. According to the Bureau of Energy Efficiency (BEE), thermal energy consumption in Indian cement plants ranges from 650–800 kcal/kg of clinker, depending on fuel mix, pyroprocessing stability and technology. Even minor refractory wear triggers cascading inefficiencies. A report by FLSmidth states that coating instability in the burning zone can increase energy use by 3 per cent to 7 per cent, raise free-lime variability and reduce kiln output by up to 10 per cent. These disruptions travel downstream—overloading coolers, damaging clinker granulometry, and affecting grinding systems. Refractory performance is not maintenance—it is margin protection.
Pyroprocessing, however, is evolving faster than ever. High AFR rates, aggressive calciner chemistry and stricter NOx/SOx limits have made “temperature-only” refractory selection obsolete. Modern plants demand linings resilient to thermal cycling, alkali infiltration, and abrasion. They also demand digital eyes inside the kiln, and installation methodologies that compress shutdown windows without compromising life. As India moves toward Net Zero, refractories and pyroprocessing systems are no longer supporting actors—they are the backbone of sustainability and competitiveness.
Kiln lining fundamentals
The rotary kiln remains the thermal heart of every cement plant. It is an environment where temperatures exceed 1,400°C and stresses are constant. The refractory lining is the sole shield between this world and a shell that must remain below 350–400°C to avoid structural failure. According to the World Refractories Association, refractories inside kilns endure 1,200–1,700°C, as well as chemical infiltration from sulphur, alkalis and volatile metals. Each zone brings unique threats: calcining zones see dust impingement, burning zones face clinker abrasion, and coolers battle high mechanical shock. Refractory selection must therefore be a zone-specific exercise balancing heat, chemistry and wear.
Material science underpins this design. A report by RHI Magnesita states that magnesia-spinel and magnesia-hercynite bricks deliver 15 per cent to 25 per cent higher resistance to clinker infiltration than traditional magnesia-chrome options, making them suitable where coating is unstable. According to the Indian Minerals Yearbook, high-alumina bricks, when paired with low-cement castables in transition zones, reduce spalling risk and extend lining life by 20 per cent to 30 per cent. Preheaters and coolers, meanwhile, respond better to abrasion-resistant alumina castables and silicon carbide. Effective refractory design maps these environments to the correct materials, ensuring kiln uptime and stable clinker output.
Beyond chemistry, three disciplines drive lining longevity: thermal elasticity, coating compatibility and installation. A lining that tolerates expansion without cracking, supports protective coating formation and is installed with proper anchoring will outperform a superior material installed badly. Treating refractory installation as a routine shutdown task invites wear, hotspots and premature relining. Modern refractories must work with the process, not merely endure it.
Preheater, calciner and cooler zones: unique refractory demands
Preheaters and calciners are the most aggressive wear environments in pyroprocessing. Fast gas velocities, thermal cycling and volatile chemistry punish linings relentlessly. According to the Portland Cement Association, gas velocities in preheater risers reach 18–22 m/s, with particle loading of 30–40 g/m3, creating intense erosion. Unlike kilns, preheaters rarely develop stable coating layers, making abrasion and thermal shock resistance more critical than temperature tolerance. Calciners intensify chemical stress: AFR combustion, sulphur oxidation and alkali vapours penetrate refractories, demanding low-porosity, chemically stable materials.
Material strategy in these areas differs. Silicon carbide, abrasion-resistant alumina and low-cement castables dominate because they survive dust, vibration and thermal cycling. A report by FLSmidth states that incorrect refractory choice in preheaters can increase pressure drop by 8 per cent to 12 per cent, raise exit temperatures and compromise calcination efficiency—pushing fuel load downstream. According to RHI Magnesita, refractory wear spikes sharply when SO3 in fuels exceeds 1.5 per cent, accelerating alkali-sulphate attack. Refractory strength alone is insufficient—it must align with the gas phase and fuel blend.
The clinker cooler poses a different battle: mechanical shock and direct impact. Abrasive clinker chunks repeatedly strike the lining, often destroying material faster than heat ever could. Abrasion-resistant castables, modular precast blocks or armour tiles are essential to maintain heat recovery and minimise downtime. Plants that treat these zones as extensions of the kiln overlook their unique physics—and pay for it in energy and throughput.
AFR revolution: How changing fuels reshape refractory strategy
Alternative fuels—biomass, RDF, rubber, industrial waste—have transformed kiln chemistry. According to the Global Cement and Concrete Association (GCCA), AFR usage has increased over 60 per cent in the last decade, with European plants reaching 60 per cent to 80 per cent thermal substitution versus 15 per cent to 20 per cent in emerging economies. AFR adoption improves emissions and cost profiles, but destabilises coating, introduces salt vapours and shifts heat profiles—each of which impacts refractory life.
Naveen Kumar Sharma, AVP – Sales and Marketing, Toshniwal Industries, says, “Our solutions are built around four core parameters: energy efficiency, yield loss reduction, product quality and environmental responsibility. These pillars drive our engineering decisions and define how our technologies support cement plants, especially as they adopt alternative fuels and raw materials (AFR). We strongly believe in energy conservation. Every product we offer—whether for thermal monitoring, kiln control or flame optimisation—is engineered to improve energy performance. Reducing yield loss is another principle deeply embedded in our solutions, because production interruptions and material losses directly affect plant profitability and clinker quality. We are also highly conscious of the end-product quality delivered by our customers to their markets. Consistency in burning, heat transfer, and thermal profiling directly influences clinker characteristics, and our instruments help maintain this stability. By optimising flame patterns, energy use, and pollution, our solutions deliver direct and indirect savings. Plants benefit from lower operational losses, reduced maintenance, and improved reliability, especially in pyroprocessing zones.”
Alkalis, chlorine and metals volatilise in hot zones and condense in cooler areas, infiltrating refractory pores. A report by the European Cement Research Academy (ECRA) states that chlorides from plastic-rich fuels reduce lining life by 30 per cent to 50 per cent in burning and preheater zones. According to the International Energy Agency (IEA), high AFR increases NOx/SOx and alkali-sulphate circulation, forcing plants to use higher-grade refractories. VDZ Germany research shows AFR kilns experience more coating instability, accelerating fatigue.
AFR requires moving from “high-temperature resistance” to “high-chemistry tolerance.” Magnesia-spinel and hercynite bricks help resist vapours; abrasion-resistant monolithics handle calciner dust. Plants that swap fuels without revising refractory strategy see premature failure. AFR is not a fuel choice—it is a process redesign requiring burner tuning, sulphur balancing and digital monitoring.
Failure modes and root causes
Refractory failure is rarely material—it is process. Alkali cycles deposit potassium and sodium deep into refractory pores, forming expansion phases. According to the European Cement Research Academy (ECRA), alkali-silica reactions reduce brick strength by up to 40 per cent. Combined with SO3 fuels, alkalis destabilise coating, induce spalling and trigger hotspots. Carbon monoxide damage is subtler. A report by the World Refractories Association states that 500–1,000 ppm CO exposure weakens refractory bonding, causing micro-cracks.
Sunil Kumar Gupta, Chief Project Officer, Star Cement, says, “Thermal profiling and digital monitoring have become essential predictive-maintenance tools for managing kiln and preheater performance. Online shell scanners now provide continuous thermography from inlet to outlet, helping teams assess coating behaviour and refractory health. Drone-based thermography is gaining popularity because it captures hotspots in areas manual checks cannot reach, especially inside cyclones and the calciner during shutdowns. Alongside kiln and cooler cameras, emerging instruments such as cooler-bed thickness sensors further optimise operation. Together, these technologies deliver better KPIs, more stable coating and improved refractory life. Digital data ensures that refractory life is maximised by maintaining stable thermal conditions.”
Thermal shock is mechanical: sudden temperature drops, often 100–150°C during start/stop, fracture high-modulus materials. According to VDZ Germany, uncontrolled thermal cycling shortens burning-zone lining life by 25 per cent to 35 per cent, even if the material is chemically sound. Plants rarely blame combustion or AFR shifts—they blame the brick. Refractories must be read as diagnostic tools, not just consumables.
Shaped vs monolithic refractories
Shaped bricks dominate burning and transition zones. Their dense microstructure resists abrasion and supports coating. According to the World Refractories Association, shaped refractories provide 10 per cent to 20 per cent higher abrasion resistance than castables above 1,400°C. Their modularity preserves shell geometry under load. A report by VDZ Germany states that brick linings withstand 50–60 coating collapse events annually, while monolithics lose strength under repeated instability. Monolithics excel in dynamic wear zones—cyclones, risers, coolers—where jointless continuity resists dust erosion. According to the European Cement Research Academy (ECRA), low-cement castables reduce cold-face heat loss by 8 per cent to 12 per cent and extend cyclone inlet life by 20 per cent to 30 per cent. Anchoring flexibility and rapid installation make monolithics ideal for modern operations.
Installation discipline and shutdown planning
Refractory success is determined at installation—not purchase. Joint thickness, curvature, anchor layout and heating curves matter more than material brochures. A report by the WBCSD–CSI states that poor installation causes over 50 per cent of global refractory failures. In India, compressed shutdowns amplify these risks. Outages carry direct and indirect cost. According to the International Energy Agency (IEA), unscheduled kiln shutdowns increase plant-wide energy consumption by 3 per cent to 6 per cent for 30 days. Plants that treat shutdowns as cross-functional engineering events—not maintenance—see longer lining life and fewer emergencies. Precision is a performance technology.
Digital monitoring, thermal profiling and predictive maintenance
Thermal cameras, shell scanners and kiln-eye systems have replaced intuition. According to the International Energy Agency (IEA), digital monitoring reduces refractory downtime by 20 per cent to 25 per cent. A report by ECRA shows that continuous temperature profiling predicts coating instability up to 48 hours earlier, enabling proactive intervention.
Professor Procyon Mukherjee explains, “Advanced refractory technologies are moving beyond material selection toward engineered performance systems. Next-generation monolithics and castables—enhanced with improved bonding chemistries, nano-modifiers and reduced alkali reactivity—extend campaign life and significantly reduce patch repair frequency. These materials also shorten shutdown windows because they cure faster and offer more predictable installation characteristics, directly lowering kiln downtime. 3D-printed refractory modules and prefabricated assemblies are now being used for burner blocks, riser ducts and throat geometries, allowing bespoke shapes that are difficult or risky to build onsite. Additive manufacturing enables tighter dimensional tolerances and faster installation in constrained spaces, where precise fitting is critical to avoid stress concentrations or mechanical wear.”
“A step further is the emergence of sensorised and embedded-monitoring refractories. Distributed fibre-optic lines, acoustic-emission sensors and integrated thermocouples provide real-time heat maps and detect micro-fracture initiation long before visual damage appears. These systems support condition-based maintenance instead of calendar-based shutdowns, enabling more informed decisions on when and how to intervene. Hybrid lining systems are also gaining traction—pairing high-performance bricks at the hot face with insulating monolithics behind them to optimise both cost and thermal reliability. Industry trials and publications from 2023–25 show early adoption of these technologies, with predictive analytics and sensor-embedded linings proving especially impactful in reducing unplanned outages and extending refractory life” he adds.
Predictive maintenance is the next frontier. According to ABB Industrial Analytics, AI systems cut unscheduled stoppages by 30 per cent to 50 per cent and extend refractory life. Plants that digitise pyroprocessing gain higher uptime, smoother ramp-ups and safer AFR adoption.
Retrofit pathways for older kiln lines
Older kilns are not obsolete—they are underutilised. According to the International Energy Agency
(IEA), targeted system upgrades improve clinker efficiency by 10 per cent to 15 per cent without new CAPEX. A report by GCCA states that retrofit optimisation reduces fuel by 3 per cent to 6 per cent. Retrofits begin with refractories: replacing chrome bricks, deploying abrasion monolithics, adding shell monitoring.
Their power is modularity. As per VDZ Germany, switching riser bricks to monolithics extends lining life by 20 per cent to 30 per cent and speeds installation by up to 35 per cent. Plants that treat old kilns as living systems—not legacy assets—win.
Towards Net Zero
Net Zero is a kiln stability challenge. GCCA claims that decarbonisation demands lower clinker intensity, higher AFR and efficiency—all refractory-dependent. A report by the IEA states that thermal improvements deliver 16 per cent to 20 per cent of total CO2 reduction, unattainable without coating stability and engineered refractories.
For India, incremental efficiency is everything. Proper refractory selection extends lining cycles by 25 per cent to 35 per cent, lowering shutdown emissions and volatility. Plants that view refractories as strategic assets—not consumables—achieve uptime, kWh/tonne improvement and real Net Zero momentum, according to VDZ Germany.
Conclusion
A new refractory philosophy is emerging in the cement industry—one where materials, process control, digital monitoring and shutdown discipline work together as a single ecosystem. Plants that still treat refractories as a replaceable commodity inevitably fall into cycles of premature wear, coating instability and soaring maintenance cost. But those that integrate material science with pyroprocessing logic—choosing the right brick for the right zone, using abrasion-resistant monolithics where needed, planning installations with precision, and upgrading older lines with smarter systems—are consistently outperforming their peers. In a market defined by tighter margins, unpredictable fuels, and rising sustainability expectations, refractories have become a lever of efficiency, not an afterthought.
The path forward is clear: engineered materials, digitalised diagnostics, predictive maintenance and intelligent retrofit strategies will shape the future of cement pyroprocessing. As AFR substitution grows, kiln loads intensify and environmental standards tighten, refractory solutions will evolve from passive armour to active enablers of reliability and emissions control. The plants that recognise refractories as strategic assets—rather than shutdown consumables—will unlock longer campaigns, lower kWh per tonne, greater clinker consistency and fewer disruptive outages. In that future, the kiln lining is not only a protective layer—it is the foundation on which India’s cement producers will build resilience, competitiveness and meaningful progress toward Net Zero.
– Kanika Mathur















 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago