Connect with us

Economy & Market

Predictive maintenance is a top priority in industrial IoT

Published

on

Shares

Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries, ABB India, discusses how advanced digital solutions are revolutionising the cement industry by enhancing operational efficiency, reliability, and sustainability.

How does ABB Ability™ Knowledge Manager help cement plants connect business KPIs to operations and optimise their performance?
ABB Ability™ Knowledge Manager (KM) is a true manufacturing operations management solution which, in a single platform, integrates data from operational, control, production, quality, downtime and business systems and converts data into actionable information.
At its core, ABB Ability™ Knowledge Manager offers industry-specific process and quality data warehousing, presenting information in a meaningful way. This single, powerful tool meets various needs: production information and downtime management, production scheduling, energy cost tracking and benchmarking, plant emissions monitoring and alarm analytics. Its user-friendly and intuitive statistical analysis tools boost both production and quality.
Statistical production analysis offers powerful tools to monitor quality-related process variables effectively. It helps verify if these variables are randomly scattered around the mean and normally distributed, and it detects variability and process changes to prevent instability. Some key tools we use include X charts (Shewhart), EWMA charts, CUSUM charts, histograms, and multivariable X-Y correlation graphs.
To enhance transparency across a plant or fleet of plants, our KM is available via a mobile app for smartphones and tablets. This allows plant and company managers to view operational performance anytime, anywhere. ABB Ability™ KM is highly scalable to meet customer needs, with flexibility for plant-level, regional, and enterprise-level deployment. It helps cement customers track processes, quality, operations, emissions, and downtime using standardised custom templates, IoT connectors and seamless ERP integration, all backed by excellent security policies.

How does ABB’s shift from reactive to predictive maintenance impact the operational efficiency and reliability of cement plants?
Predictive maintenance is a top priority in industrial IoT because it combines data, domain expertise, IoT platforms and AI. This combination allows manufacturers to predict anomalies in their plants. I believe, by using a modern asset optimisation system, cement manufacturers can shift from reactive to predictive maintenance strategies, avoiding unnecessary maintenance and reducing operating costs. This is achieved through the vast amount of data generated by smart devices connected in the plant, such as motor control centers, numerical relays, smart transmitters, and various asset models for motors, transformers, grinding circuits and conveyors.
ABB Ability™ Predictive Maintenance service leverages digital applications for quick detection of impending issues, root-cause analysis with recommendations, and assessment of severity levels and health indexes. It offers ready-to-use standard models that are easy to deploy and scale, helping to identify active conditions, assess health with severity and ensure easy deployment.

What are the key features of ABB’s AI-based Asset Performance Management (APM) suite, and how does it enhance asset optimisation in cement plants?
Predictive asset models can help cement plants operate with fewer workers, and to manage operations remotely. An APM solution, powered by predictive asset models, would give the remote teams full visibility into data that would tell them the health of all the assets in the plant. Think of AI-enabled APM as the most cost-effective way to extend the life of the aging (and newer) assets, to decide on the optimal timing for scheduled maintenance turnarounds (one of the biggest costs in a plant) and plan better. The new AI-based APM helps develop models, algorithms, dashboards and reports using a maintenance-oriented platform. It integrates with enterprise-level systems and evolves into digital strategic asset management. This makes transitioning from predictive to prescriptive maintenance and management possible.
ABB was approached by one of Asia’s largest manufacturers of grey cement, ready mix concrete and white cement. The customer has 19 integrated plants, one clinkerisation plant, 25 grinding units and seven bulk terminals. Working together with ABB domain experts, the company used maintenance-oriented algorithms that alerted the client to the potential failure of a particular part or electronic device, allowing it to perform predictive rather than reactive maintenance. Combined with a range of other digital solutions, including ABB Ability™ Expert Optimizer and ABB Ability™ Collaborative Operations, the customer was able to achieve ROI in eight months, a reduction in costs by 3-5 per cent and increase in the life cycle of assets. In this way, cement manufacturers can fully utilise the power of digitalisation to reduce energy usage and emissions, paving the way for the smart, sustainable and profitable cement plants of the future

With increasing digitalisation, how does ABB ensure the cybersecurity of cement plant operations and protect against potential cyber threats?
More and more cement producers on the digitalisation path would like to take a more proactive approach to cyber security. ABB’s analytics solutions and services continuously monitor, diagnose and resolve security issues, helping safeguard people, assets and reputation. Because technology and cyber threats can both change unpredictably, the strategy needs to be reviewed periodically, including performing simulations under different circumstances, like a major ransomware incident.
ABB realises that its customers are concerned about protecting against and minimising the risk of a cybersecurity incident. While asset owners have prime responsibility for any incident response procedures, ABB actively monitors for any cybersecurity threats that pose a potential impact to ABB control systems. All in all, ABB is well positioned as a systems integrator – a factor that is foundational to the company’s cybersecurity strategy in the industrial controls arena. There are two aspects to this. The first is that the customer can trust that implementation of a third party solution in ABB’s reference architecture will result in optimal value. The second is that the cement manufacturer can rest assured that if there is a failure or a problem with implementation, it will, in all probability, not impede the availability or safety of assets and will ease their recovery. ABB has been ensuring its customers by following the highest level of security policies during design, development, deployment and communications by adhering to the industry best practices.

– Kanika Mathur

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

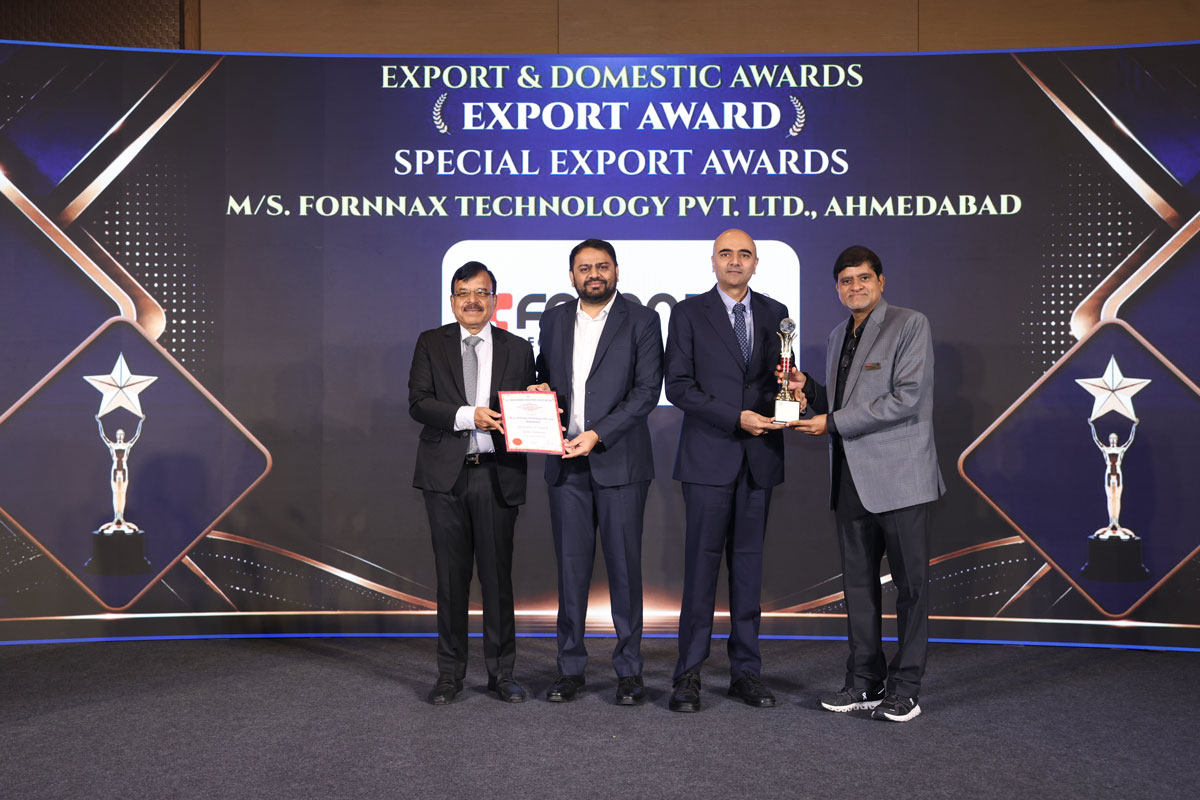
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Concrete

Wonder Cement appoints Mahesh Singh as VP Corporate Brand Communication 

Published

on

By

Shares

Singh brings 20+ years of brand and marketing experience, and will lead integrated corporate brand communication initiatives at Wonder Cement 

New Delhi

Wonder Cement, a leading cement manufacturer, has appointed Mahesh Singh as Vice President – Corporate Brand Communication. In his new role, he will oversee corporate brand strategy and communication, including digital and performance marketing, public relations, trade, events, exhibitions, sports and experiential marketing. 

Singh brings over two decades of experience across marketing and communications, with roles spanning the automotive industry, agencies and entrepreneurship. He spent more than a decade with Honda Motorcycle & Scooter India, working across integrated communication, media, digital, retail and consumer engagement. His stint also included helping build the company’s digital marketing capabilities. 

He moved to dentsu X India as Vice President – Strategy & Planning, working across categories such as automotive, auto components, electric vehicles, FMCG, consumer electronics, BFSI, apparel and brand consulting. His responsibilities included media and marketing strategy, product launches, content, performance marketing and consumer activations. 

Singh subsequently took an entrepreneurial route with Radiant Brands before joining Shriram Ltd (SPR Autotech) as Head – Marketing & Communications. There, his remit included brand and corporate strategy, communications, PR and ORM, retail identity, loyalty programmes and events. 

At Wonder Cement, Singh will be responsible for bringing together the company’s corporate brand communication initiatives across digital, performance marketing, PR, trade, sports and experiential platforms. The role will focus on creating an integrated approach to communication across consumers, trade partners and other key stakeholders. 

The appointment brings to Wonder Cement a marketer whose career has spanned the brand, agency and entrepreneurial sides of the communications ecosystem. 

Wonder Cement, part of the RK Group, is a cement manufacturer with roots in Rajasthan and a focus on quality, trust and transparency. The company has grown to six manufacturing plants, and a cement capacity of 21.5 MTPA. With more than 2,000 employees and a network of over 5,000 dealers, its operations span manufacturing, distribution and customer engagement, with a focus on consistent product quality and efficient execution. 

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds