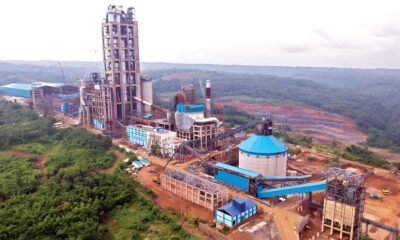
Tushar Khandhadia, Senior General Manager – Production, Udaipur Cement Works Limited (UCWL), elaborates on the benefits, challenges and future prospects of integrating environmentally friendly practices in the cement manufacturing process.
Tell us about the alternative fuels and raw materials used in your organisation.
Our organisation employs a variety of alternative fuels and raw materials (AFR) to enhance sustainability and reduce our carbon footprint. These include:
Alternative fuels: Waste-derived fuels such as municipal solid waste (MSW), tire-derived fuel (TDF), biomass, and industrial waste, waste mix for co-incineration LCV.
Alternative raw materials: Industrial by-products like fly ash, F.F slag, jarosite chemical gypsum, granulated slag, Bf dust, chemical sludge (waste water treatment, ETP sludge-solid, spent carbon, waste mix (solid).
What are the key parameters considered while selecting raw materials for the manufacturing of cement?
When selecting raw materials for cement manufacturing, we consider several key parameters:
Chemical composition: Ensuring the materials provide the necessary elements (calcium, silica, alumina, and iron) required for clinker production.
- Availability and consistency: Reliable supply chains and consistent quality to maintain production efficiency.
- Environmental impact: Minimising carbon footprint and environmental disruption.
- Cost-effectiveness: Balancing raw material costs with production costs to maintain economic viability.
- Regulatory compliance: Adhering to local and national standards and regulations.
How are the alternative fuels used by your organisation contributing to your decarbonisation goals?
The use of alternative fuels contributes to our decarbonisation goals by:
- Reducing fossil fuel dependency: Lowering CO2 emissions associated with traditional fossil fuels. In general, 65 per cent of CO2 generated during clinker formation is through process emission which comes from the calcination of limestone and 35 per cent is through burning of fuel. The AFR contributes to reducing the CO2 emitted from fuel combustion. Generally, at every 1 per cent increase in TSR, there is reduction of around 2kg CO2/T of clinker. As there is no substitute to the limestone for the clinker formation, increasing the TSR in clinker formation is
the only option to reduce CO2 emission during clinker formation.
- Waste management: Diverting waste from landfills and reducing methane emissions.
- Energy efficiency: Some alternative fuels have higher energy content, leading to more efficient combustion.
- If the hazardous waste is not co-processed in our cement kiln, then it’s diverted to an incinerator for disposal. Burning hazardous waste in an incinerator requires temperatures up to 1000oC, which occurs with the help of traditional fuels such as coal and this leads to further CO2 emissions into the atmosphere. So, cement industries are serving dual purpose for reduction in CO2 emissions in the cement manufacturing process itself as well as at the TSDF site.
What are the government regulatory and policy support that you get for the use of AFR?
We benefit from several forms of government regulatory and policy support, including:
- Regulatory frameworks: Policies that encourage the use of AFR in cement production.
- Research and development grants: Funding for innovation in sustainable materials and processes.
- Exemption in total energy count in PAT calculation.
- Permission for usage of hazardous waste in cement kiln by CPCB and SPCBs with regular monitoring protocol to controls emissions.
How do you ensure the quality and safety of alternative fuels and raw materials used in cement production?
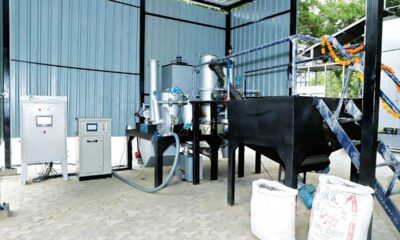
We have a state-of-art AFR lab in our plant for regular testing and monitoring of incoming AFR. In testing, we follow all important parameters required to maintain the quality of the product, safety of men and machines as well as environmental impact. We classify the incoming materials into solid, liquid and sludge and perform testing of moisture, ash, volatile matters, fixed carbon, ultimate analysis, grindability for solid, viscosity for liquid, flashpoints, etc.
Safety protocols are also strictly implemented. Comprehensive safety standards and training for handling and processing AFR include prohibition of mobile phones, barricading the area for only authorise person entry and proper earthing of the entire unloading vehicle along with the standard PPEs for all manpower dealing with AFR.
Have you faced any challenges or barriers when using alternative fuels and raw materials in cement production, and if so, how have you overcome them?
We have encountered several challenges when using AFR:
- Technical challenges: Variability in material properties, due to which CO2 generation and jamming issues are created inside the pyro system affecting production processes.
For this, we have installed a liquid AFR tank of 700kl for proper mixing of liquid AFR coming from different sources.
For each truck of AFR arriving at the plant, we take a sample, and only if the sample is within the permissible range, we accept the material for use.
We also use Karl Fischer titration machine from Metrohm for measuring bound water content and chloride.
The second challenge is the increase in the specific heat consumption as the high moisture content in the AFR needs more heat to evaporate the moisture. In general, at every 1 per cent TSR there is increase in the specific heat content by around 0.8-1.2 Kcal/Kg clinker.
- Supply chain issues: Ensuring a consistent supply of high-quality AFR. We overcome this by establishing long-term partnerships and diversifying our sources.
- Regulatory hurdles: Navigating complex regulations and obtaining necessary permits. We maintain active communication with regulatory bodies and advocate for supportive policies.
Do you collaborate with other companies or organisations to identify and implement best practices in the use of alternative fuels and raw materials in cement production?
Our organisation collaborates with various stakeholders to identify and implement best practices:
- Industry associations: Participating in industry forums and working groups.
- Academic partnerships: Collaborating with universities for research and innovation.
- Cross-industry initiatives: Partnering with other sectors to develop and share sustainable practices Like Hindustan Zinc, RSPL, PI industries, GEPIL, UPL, Phonix, Deccan, Cadila, Meghmani Speciality Che. LLP etc.
How do you see the use of alternative fuels and raw materials in cement production evolving in the future, and what role does your company play in this process?
We see a significant evolution in the use of AFR in cement production, driven by:
- Technological advancements: Improved processing technologies and material innovations.
- Stricter environmental regulations: Increasing pressure to reduce emissions and environmental impact.
- Circular economy models: Greater emphasis on waste valorisation and resource efficiency.
Our company aims to lead this transition by:
- Innovating continuously: Investing in R&D for new AFR and efficient production processes.
- Scaling sustainable practices: Expanding our use of AFR across all operations.
- Advocacy and leadership: Promoting sustainable practices within the industry and influencing
policy development.
Banned wastes for co-processing in cement kiln
Refuse the listed ‘banned wastes’
x Anatomical Hospital Wastes
x Asbestos-containing Wastes
x Bio-hazardous Wastes
x Electronic Scrap
x Entire Batteries
x Explosives
x High-concentration Cyanide Wastes
x Mineral Acids
x Radioactive Wastes
x Unsorted Municipal Garbage
Main Reasons for Waste co-processing
• Sustainable Development
• Economical Benefits
– Substitution of Fossil fuels or natural raw materials
– Income from co-processing service
• Environmental Benefits
– Reduction in CO2 emissions
– Safe and optimal waste disposal
– Reduction in extraction rate of natural materials
– Reduction in overall emissions
• Social Benefits
– Effective contribution to waste management at local / regional levels
– Regional job creation in waste collection and pretreatment etc.
– Saving of public funds in building alternative infrastructure.
Aspect HW Incinerator Cement Kiln
Temperature 850-1200 °C 1400-2000 °C
Residence Time >2 sec @>1200 °C 4-6 sec @>1800 °C
Turbulence Induced in SCC Induced in Kiln
Gas Cleaning Alkaline scrubbing Alkaline Env. in Kiln
Residues Ash / Fly ash In clinker product
Fuel Fossil fuel used Fossil fuel saved