

Concrete
Making durable concrete by using ternary blend


Cement, flyash, ground granulated blast furnace slag(GGBFS) are the key components in the ternary blend used to make concrete. Nagesh Veeturi and Sumanta Sahu of KEC International – Civil Business, shed light on reducing the carbon footprint of cement production by using supplementary cementitious materials.
Cement is prime ingredient in concrete. One tonne of cement produces around 0.8 to 1 MT of carbon dioxide. It’s worth noting that efforts are being made to reduce the carbon footprint of cement production by using supplementary cementitious materials such as flyash and GGBS in concrete. In case of ternary blended concrete, supplementary cementitious materials flyash and GGBS are used in addition to cement, sand, aggregate, water and admixture.
To evaluate the percentage of replacement of cement with flyash and GGBS, one needs to understand the properties of concrete mix with flyash and GGBS as ingredients, structure strength, stripping time and durability requirements.
Properties of Supplementary Cementitious Materials
Flyash
Pulverised coal is used in thermal power plants for electricity generation. A by-product of this combustion reaction is fly ash. The electrostatic precipitators (ESPs) used inside chimneys of the power plants remove flyash before ejecting out the combustion gases into the atmosphere. Fly ash is a very fine particle like residue, which has pozzolanic properties. Hence it is often blended with cement and also used as partial replacement of cement.
Fly ash consists of silica (SiO2), alumina (Al2O3) and calcium oxide (CaO) as its major components. Fly ash can be of two types – C type and F type. C type fly ash is rich in calcium oxide and possesses both cementitious and pozzolanic properties whereas F type fly ash is low in calcium oxide content and possesses only pozzolanic properties.
- Due to spherical shape of flyash, water demands in concrete is reduced, concrete becomes more cohesive.
- Silica in flyash reacts with calcium hydroxide released from cement to form CSH Gel, Formation of CSH Gel leads to increase in strength of concrete further and make the concrete dense and durable.
- 35 per cent of cement can be replaced with flyash according to IS specification. However, for mass concrete high volume flyash up to 50 per cent can be used.
- Early strength observed to be less for flyash concrete.
- Due to slow development of strength of concrete, stripping time gets delayed.

(Flyash produced from Thermal Power Plant)
Ground Granulated Blast Furnace Slag (GGBFS)
Blast furnace slag is a by-product of iron ore during iron extraction process. Amongst all mineral admixtures, blast furnace slag has the highest specific gravity (2.8 to 3.0). Typically, the slag fineness is slightly more than that of the cement.
There are various types of slag available like air cooled slag, expanded or foamed slag, granulated slag. Among these only the granulated slag is commonly used as a mineral admixture. It is a highly reactive form of slag and is usually quenched to form a hardened matter which is then grounded into particles of fineness almost same as that of cement. Hence the material is called as ‘ground granulated blast furnace slag’.
GGBFS possesses both cementitious and pozzolanic properties. An activator is needed to hydrate the slag.
- GGBFS increases the initial setting time of the concrete. But it does not alter the workability of the concrete much because its fineness is almost same as that of the cement.
- The early rate of strength gain in concrete is diminished by replacement of cement in the concrete with GGBFS.
- The final strength is improved by slag cement and also the durability of the concrete is increased.
- Concrete uses in marine construction are highly prone to chemical attack and corrosion. GGBFS as a concrete ingredient increases resistance against sulphate and chloride attack.
Normally concrete tends to segregate with GGBS as ingredient,
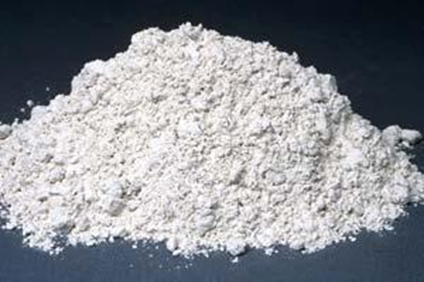

(GGBFS produced from Steel Plant)\
Concrete with flyash and GGBS as ingredients (Ternary Blend)
Ternary blended concrete is observed to be more cohesive and workable due to presence of flyash in concrete. Early strength gain can be achieved by using both Cement and GGBS in concrete. Concrete with ternary blend is win-win situation in terms of good product quality, optimising the cost of concrete, durability and resistance against chemical attack. Additionally, the use of SCMs in concrete can contribute to sustainability efforts by minimizing the cement content which is associated with significant carbon dioxide emission during its manufacturing process.
The hydration process of ternary blended concrete is divided into primary reaction by OPC and GGBS, pozzolanic reaction of GGBS and flyash as the secondary process. Both materials react with Calcium hydroxide produced by cement hydration to form CSH gel, which gives denser microstructure than conventional OPC concrete. The dense structure improves the durability properties of ternary blended concrete. Process yields to minimise penetration of aggressive chemicals such as sulphate, chloride as compared to conventional concrete mix.
Conclusion
Use of supplementary cementitious materials always improve the durability properties of concrete along with cost optimisation. Selection of supplementary cementitious materials, percentage replacement with cement is taken considering the strength and durability requirements of structure.

Concrete
Jammu Division Begins First Cement Rail Traffic to Anantnag
Cement Loading From Kathua for Anantnag to Begin on September 14

Concrete
Hard Worker Wins Three Honours at Kyoorius Design Awards
Ramco Cements’ brand secures Grand Prix and two Blue Elephant honours.

Concrete
Cement Firms to Invest Rs. 130 bn in Green Energy by FY28
Cement companies plan to expand clean energy capacity to 6 GW by FY28



Jammu Division Begins First Cement Rail Traffic to Anantnag

Hard Worker Wins Three Honours at Kyoorius Design Awards

Cement Firms to Invest Rs. 130 bn in Green Energy by FY28

Centre Defers Clearance for Limestone Mine Near Bustard Habitat

Telangana to Supply Subsidised Cement for Indiramma Houses
Jammu Division Begins First Cement Rail Traffic to Anantnag
Hard Worker Wins Three Honours at Kyoorius Design Awards
Cement Firms to Invest Rs. 130 bn in Green Energy by FY28
Centre Defers Clearance for Limestone Mine Near Bustard Habitat
Telangana to Supply Subsidised Cement for Indiramma Houses
-

 Concrete4 weeks ago
Predictive maintenance minimises the risk
-

 Concrete4 weeks ago
AI is solving longstanding challenges
-

 Concrete4 weeks ago
Fuller Technologies QCX® Lab Automation Systems
-

 Concrete4 weeks ago
Beyond the Gearbox: How a Holistic Lubrication Strategy Reduces Total Cost of Ownership in Cement Plants