Economy & Market
Leading the Green Revolution
Published
3 years agoon
By
admin
Ajay Kapur, CEO – Cement Business, Adani Group, explores India’s proactive measures, from embracing renewable energy and waste heat recovery to reducing clinker usage and innovatively repurposing industrial by-products, signaling a promising shift towards sustainable cement manufacturing.
Imagine a world without cement – it’s almost like picturing a skyline without its defining structures. As one of the most commonly used building materials, the manufacturing of cement faces significant challenges in decarbonising. Tackling this challenge goes beyond the ordinary, considering that the cement sector is a major player, contributing up to 7-8 per cent of global greenhouse gas emissions. The significance of this issue is particularly pronounced for India, as we currently hold the dual status of the world’s second-largest producer and consumer of cement. The production capacity of the Indian cement sector is poised to grow to more than 700 million tonnes (MT) over the next five years from around 570 MT now. Consumption on the other hand is also set to grow to 450 MT by 2027.
As the Indian economy expands and continues on this growth path to reach $5 trillion in GDP in the near term and emerge as the world’s third largest economy before the end of the current decade, the environmental challenges will also become more formidable.
Most large cement manufacturers in India have already committed to becoming carbon neutral sometime around the middle of this century and this is also going to contribute to India’s Net Zero ambition set for 2070. The road ahead for Indian cement manufacturers is very similar to what the energy sector faces. India’s economic turnaround that started in 1991 also brought home conversations around the rising and unprecedented levels of consumption of energy to fire up the economy, putting the country under the environmental spotlight, too. Cement production is not only energy intensive but also depends on natural mineral resources. The widespread adoption of well-understood and sustainable cement production practices has been a gradual process, gaining momentum over time. Today, the Indian cement sector is ready to meet sustainability challenges head-on through a whole range of measures that covers the entire value chain in cement manufacturing, leading all the way to increasing the share of green cement on the demand side.
Alternative fuel and raw materials
Being an energy-intensive sector, cement manufacturers have started investing in cleaner sources of energy like solar and wind as captive generation units to run their plants. This shift in no small measure is supported by the falling cost of renewable energy India. Between 2010 and now, the cost of solar modules in India have dropped by more than 80 per cent, making it one of the most sought after sources of clean energy for large industrial units including cement. Similar efforts are also on to move finished cement, packed and bulk on more sustainable or green logistics like soya extract-based biofuel powered shipping. Bulk terminals and grinding units along India’s long coastline can enable the movement of clinker and cement through the sea route at the lowest possible cost.
The share of green energy is further enhanced through investments in Waste Heat Recovery Systems (WHRS). These systems not only adhere to the principles of the circular economy but also result in fossil fuels savings. This not only nurtures a more cost-efficient process but also directly impacts the bottom line.
According to the Ministry of New and Renewable Energy (MNRE), the Indian cement Industry has the highest potential to adopt WHRS as an alternative to conventional sources of energy. WHRS installations will continue to grow along with the increase in capacity to manufacture cement, bringing it close to 1.3 GW at current production capacity levels. It is estimated that WHRS would help replace the energy requirement equivalent to 8.6 million tonnes of coal, resulting in emissions savings of 12.8 million tonnes of CO2 by the Indian cement manufacturers.
Cement manufacturers are also cutting down on the ‘clinker factor’ by replacing them with industrial by-products without compromising the quality (strength) of the cement. Cutting down the clinker factor offers two immediate benefits. One, it reduces energy consumption because clinker is produced at ~1400°C (from limestone etc.,) and two, it also softens the environmental impact of by-products like flyash, slag and silica fumes. Manufacturing a tonne of Ordinary Portland cement also releases around 800 kg of CO2. Investments are also made in recycling massive quantities of municipal waste into Refuse Derived Fuel or RDF through its pre- and co-processing facilities, which is then used as energy to run cement kilns. The impact of producing and using RDF not only saves on energy from conventional sources but also helps large cities manage municipal waste in a safe manner. Mega cities like Mumbai are now working with cement companies to manage municipal waste through a symbiotic relationship that benefits manufacturers and city administrators.
Red mud, a waste derived from aluminium production, is also now used in the cement manufacturing process as an alternative raw material. Again, this helps build a circular economy through utilisation of aluminium industry’s by-products in an environmentally sound manner. Other large industrial sectors like pharmaceuticals also tapped for zero residue of their process waste and ETP sludge. Similarly cement manufacturers are also able to process hazardous wastes released by the automobile and automobile ancillary sector such as chromium, zinc and paint sludge, oil residue and cotton waste.
Water management is yet another area that is making cement manufacturing in India more sustainable. Apart from becoming water positive (returning more water than what is consumed) from an operations point of view, a lot is also being done under the larger banner of CSR where cement manufacturers are now active participants in water conservation projects, working along with local rural communities including farmers. Large cement manufacturers in India are also working on conserving biodiversity in their areas of operations including large afforestation projects, which helps in strengthening the water table.
Conclusion
India today has a very robust legislative mechanism to ensure that industrial sectors like cement abide by environmental laws. But cement manufacturers, recognising the growing environmental consciousness among consumers, are actively pursuing higher benchmarks to minimise burden on environmental damage. With the growing consumer centricity that has moved cement from being a commodity to a branded consumer product, manufacturers are now able to offer sustainability as part of the brand value and appeal. Green cement as a product in India is still in its nascent stage with a miniscule share in the overall market. It is expected to grow in coming years as sustainability is an important factor for today’s buyers.
Today’s well-informed consumers also expect manufacturers to play a more responsible role in protecting the environment through sustainable manufacturing practices. The transformation of the Indian cement sector has only begun.
ABOUT THE AUTHOR:
Ajay Kapur, CEO – Cement Business, Adani Group has over 30 years of expertise in the cement, construction, power and heavy metals sector. He has been extensively involved in several business forums, such as CII, FICCI, and ASSOCHAM.
Economy & Market
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
Published
1 day agoon
October 30, 2026By
admin
Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.
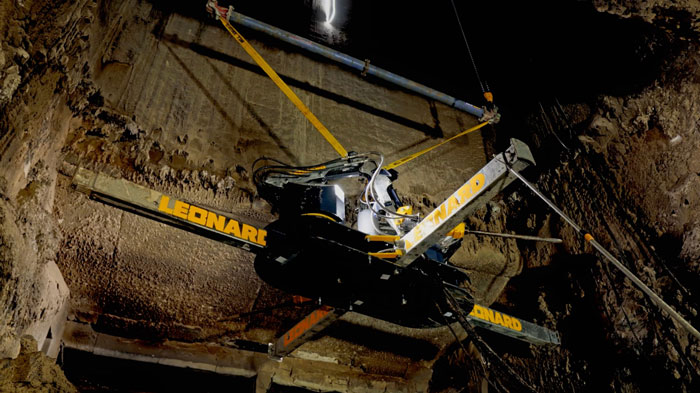
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.
Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.
Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.
Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.
According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.
First Deployment Demonstrates Shutdown Efficiency
The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.
Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.
Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”
Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.
The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.
“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.
“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”
Expanding Industrial Robotics Applications
Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.
Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.
Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.
The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.
Concrete
Martin Engineering Appoints Ashwini Khunte as India General Manager
Published
2 days agoon
October 30, 2026By
admin
Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.
Pune
Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.
Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.
A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.
In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.
Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”
Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.
“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”
Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.
Concrete
Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26
Published
2 weeks agoon
October 19, 2026By
admin
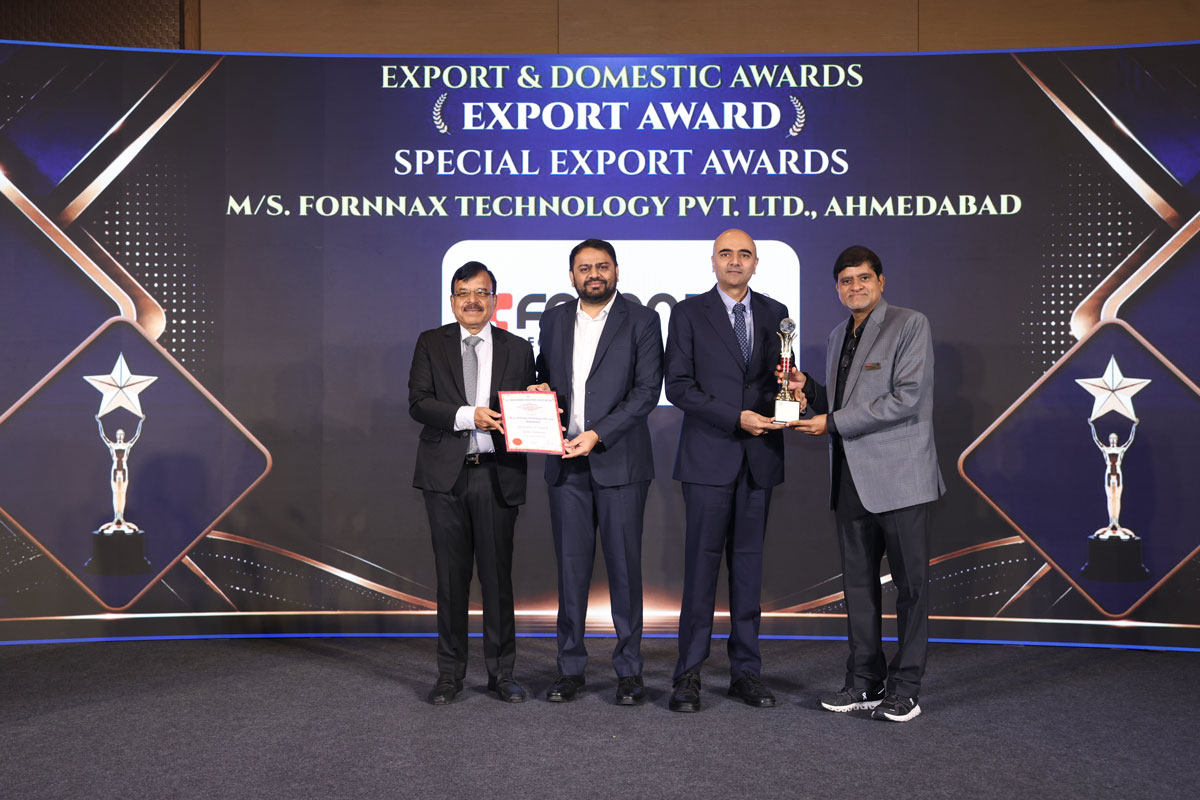
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.
With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.
The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.
Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:
“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”
Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.
The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.
Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.
For more information, visit: www.fornnax.com
JK Lakshmi Cement Begins Rs 110 Billion Assam Plant Project
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant
Martin Engineering Appoints Ashwini Khunte as India General Manager
JK Lakshmi Cement Begins Rs 110 Billion Assam Plant Project
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant