Connect with us

Economy & Market

Technology is the cornerstone of clinker cooling

Published

on

Shares

Madhusudan Rasiraju, Country Head, IKN India, talks about enhancing cement plant efficiency with energy-saving, reliable, and customised solutions while supporting sustainability through innovations like oxy-fuel plants and AFR adaptability.

Could you explain what IKN Engineering is, what the company specialises in, and share insights about your clinker cooling solutions?
IKN is a Germany-based company that specialises in providing advanced clinker cooling solutions to the cement industry. Our expertise lies in developing and supplying innovative cooling systems that focus on energy efficiency, durability and cost-effectiveness.
The clinker cooling process is a critical stage in cement production, as it significantly influences the energy efficiency of the entire plant. Our coolers are designed with cutting-edge technology to recuperate a substantial amount of heat from the clinker. This recovered heat is redirected back into the cement production process, enabling our customers to reduce their fuel consumption significantly. Moreover, IKN coolers are engineered for reliability. They are built to operate with minimal maintenance, which helps to lower operational costs and reduce downtime. By focusing on high performance and long-term reliability, we ensure that our solutions are both economically and environmentally beneficial.

How does IKN contribute to improving the efficiency of cement plant operations and supporting sustainability goals?
IKN plays a pivotal role in enhancing the operational efficiency of cement plants while aligning with global sustainability objectives. Historically, clinker coolers required frequent maintenance, with intervals as short as five to six months. This led to regular shutdowns, which disrupted operations and increased costs. With IKN’s advanced cooling solutions, cement plants can now operate their coolers for extended periods without significant maintenance. Our coolers are not only more reliable but also consume less power, which directly reduces energy costs. Additionally, the high heat recuperation efficiency of our systems ensures that less fuel is required for the cement-making process, contributing to a lower carbon footprint.
Sustainability is embedded in our solutions. By reducing energy consumption, optimising processes, and minimising maintenance, we help our customers achieve their operational goals while supporting their commitment to environmental stewardship.

What role does technology play in the clinker cooling process, and how does IKN leverage it to provide advanced solutions?
Technology is the cornerstone of clinker cooling and a driving force behind our innovative solutions at IKN. The cement industry’s needs are constantly evolving, and to stay ahead, we ensure our technologies remain dynamic and adaptable. We adopt a customer-centric approach, continuously collecting feedback from our clients to improve our systems. Every clinker cooler we supply is tailored to meet the specific requirements of the plant it serves. For instance, the physical layout, production capacity, and operational challenges of each facility are unique, and we ensure our solutions address these specific needs.
Moreover, our ongoing research and development efforts focus on enhancing reliability, improving heat recovery, and lowering energy consumption. By integrating the latest technological advancements, we make sure our coolers set new benchmarks in performance and sustainability.

Do you offer customised solutions for each cement plant, and how does the increasing use of alternative fuels (AFR) impact your clinker cooling solutions?
Absolutely, customisation is at the core of what we do at IKN. In the case of retrofits, every cooler is custom-designed to fit the specific layout and operational needs of the existing cement plant. For new installations, we collaborate closely with our clients to design coolers that are precisely sized and configured to meet their requirements.
Regarding alternative fuels (AFR), their increasing use in cement plants presents unique challenges. AFR often results in the production of finer clinker, which can be more difficult to handle during the cooling process. To address this, we optimise the operating parameters of our coolers, such as airflow density and cooler speed, to ensure they perform effectively with the type of clinker being produced. This adaptability ensures that our coolers remain efficient and reliable, even in plants using diverse and non-traditional fuels.

What challenges do you face in providing clinker cooling solutions, both from your operations and from the cement industry’s perspective?
Challenges are inevitable in any advanced technological field, and clinker cooling is no exception. One of the primary challenges we face is adapting to the changing demands of our customers. For example, frequent shifts in fuel types or the introduction of AFR can disrupt the cooling process. These changes often result in variations in clinker properties, requiring us to make adjustments to maintain optimal performance. Additionally, the grid surfaces in coolers may face increased wear and tear due to these changes. At IKN, we address such challenges by reinforcing the grid surfaces and fine-tuning our systems to handle these dynamic conditions.
From an industry perspective, there is an increasing emphasis on efficiency, sustainability, and cost reduction. Meeting these expectations while maintaining high performance is challenging, but it is a challenge we embrace through innovation, research, and collaboration with our clients.

What are your views on the net zero mission, and how is IKN contributing toward this goal?
The net zero mission is a vital initiative for energy-intensive industries such as cement, steel, and power. It requires a collective effort across the supply chain to achieve meaningful progress.
At IKN, we are committed to supporting this global goal. One of our key contributions is the development of oxy-fuel plants, which are designed to significantly reduce carbon emissions during production. We are also exploring innovative cooling methods, such as the use of nitrogen or other media, to further enhance sustainability. Currently, we have two oxy-fuel projects underway in Germany. These plants not only demonstrate our commitment to the net zero mission but also serve as examples of how advanced technology can drive sustainability in the cement industry. By focusing on durability, efficiency, and innovation, we help our clients reduce their environmental footprint while maintaining high operational standards.

– Kanika Mathur

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

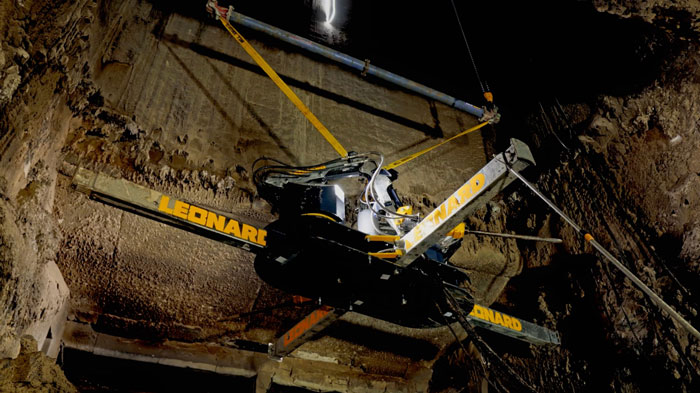
 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.


Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

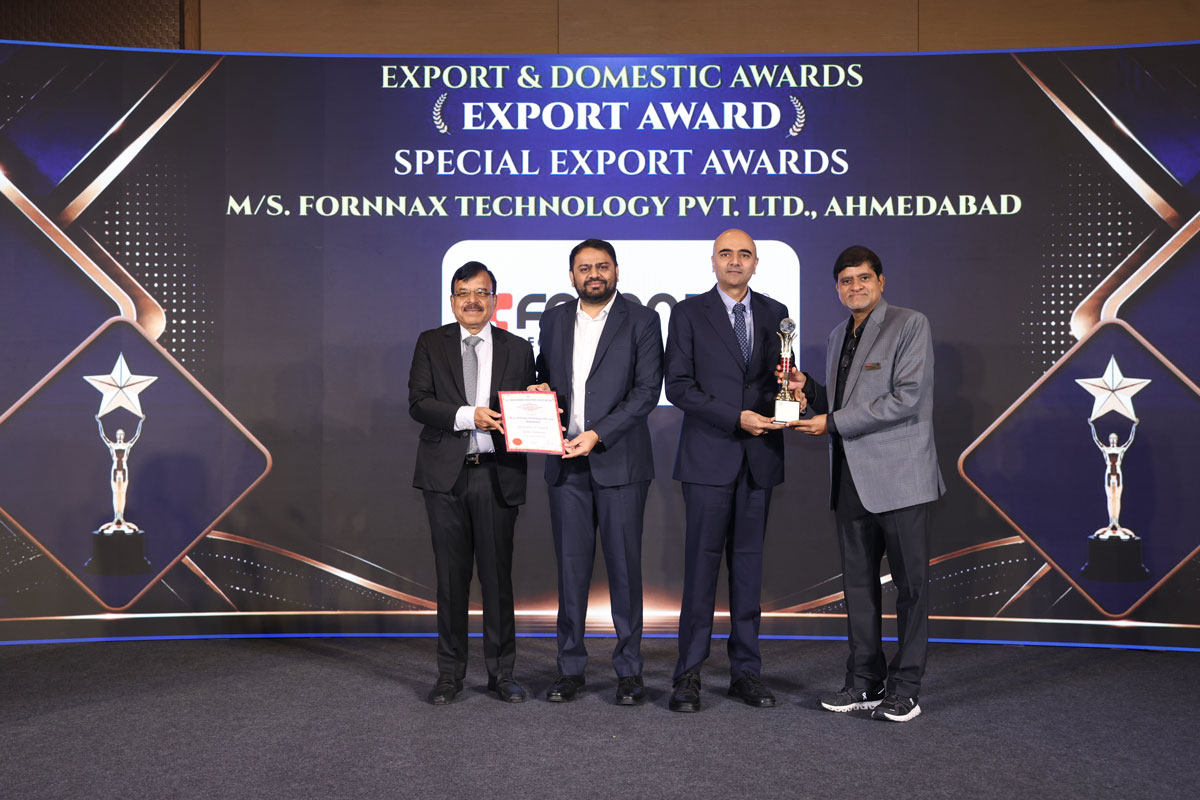
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News