India’s cement sector stands on the threshold of a green transformation — balancing rapid growth with deep decarbonisation. The journey ahead demands innovation across materials, fuels and processes, backed by strong policy and collaboration. ICR explores how industry stakeholders are looking at scaling sustainable solutions fast enough to build a truly Net Zero cement future.
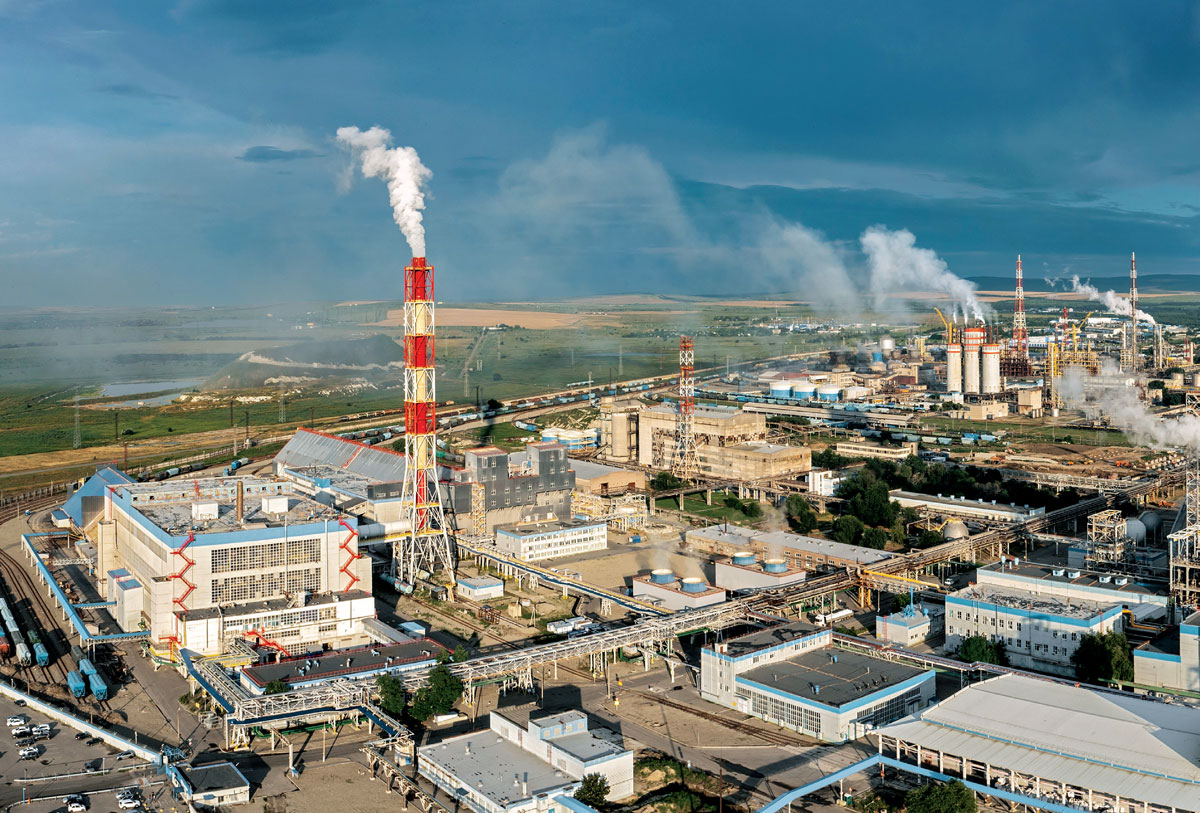
India’s cement industry stands at a pivotal crossroads. As the world’s second largest producer of cement, the country accounts for nearly 8 per cent of global installed capacity. A report by the India Brand Equity Foundation (IBEF) mentions that India’s cement production reached approximately 453 million tonnes in FY 2024–25, up from 426.3 million tonnes the previous year, reflecting steady growth driven by infrastructure and housing demand. This scale of activity underpins the nation’s development ambitions — yet it also magnifies the urgency of decarbonisation in a sector that is both energy and carbon intensive.
Globally, cement production is responsible for around 7–8 per cent of total manmade CO2 emissions. According to a 2024 report by the Global Cement and Concrete Association (GCCA), India’s cement sector contributes about 5.8 per cent of the country’s total CO2 emissions, primarily from the calcination process during clinker production and the use of fossil fuels in kilns. The same report notes that Indian producers are targeting a reduction in emission intensity from 0.68 tonnes of CO2 per tonne of cement in 2020 to 0.56 tonnes by 2030, with further improvements expected by 2047. These figures highlight the scale of transformation required even as domestic demand continues to surge.
At the same time, India’s market structure and resource base provide strong foundations for this transition. A report by IBEF highlights that nearly 98 per cent of India’s cement capacity lies in the private sector, supported by abundant limestone reserves and robust investment in new grinding and waste heat recovery capacities. However, achieving growth alongside sustainability will demand a deep shift — one that integrates smarter technology, low carbon material innovations, automation, and carbon capture at scale. The coming decade will test how effectively India can balance the ‘3 Cs’ of decarbonisation: Cut emissions, Cement innovations, and Carbon capture and utilisation.
The policy push
India’s industrial decarbonisation journey is gathering momentum, and the cement sector has become a key focus area. At the heart of the effort is the Perform, Achieve and Trade (PAT) scheme, a market-based instrument implemented under the National Mission for Enhanced Energy Efficiency (NMEEE). A report by the Cement Manufacturers’ Association (CMA) mentions that cement plants in PAT Cycle-I and Cycle-II overshot their energy savings targets by 81.6 per cent and 48.6 per cent respectively, signalling early success in improving energy efficiency.
Dr SB Hegde, Global Industry Expert, says, “Green hydrogen can transform cement production by eliminating the 32 per cent of emissions from burning coal in kilns, cutting ~0.32 million tonnes of CO2 annually for a one million tonne per annum (MTPA) plant (IEA, 2020). Combined with alternatives like fly ash for clinker and carbon capture, it could reduce emissions by 66 per cent to 95 per cent by 2050. Unlike biomass, which some plants use to cut emissions by 10 per cent but struggle with unreliable supply (UltraTech, 2024), hydrogen burns consistently at 1400–1500°C, like a steady flame in a gas stove. India’s National Green Hydrogen Mission (NGHM), targeting 125 GW of renewable energy by 2030, supports this shift (MNRE, 2023).”
In parallel, broader regulatory evolution is underway. According to an article by the Climate Policy Lab, India is set to replace the PAT scheme with the Carbon Credit Trading Scheme (CCTS) by 2026, covering nine industrial sectors including cement. This shift recognises that simply improving energy efficiency is not sufficient; the industry must move towards intensity and absolute emission targets, a step reinforced by India’s net zero commitment at COP26 for 2070.
Beyond regulatory mandates, industry led initiatives are driving the transition. The Global Cement and Concrete Association (GCCA) India and domestic trade bodies are collaborating to embed sustainability practices across the value chain, supporting innovations in blended cements, alternative fuels, and logistics decarbonisation. Such strategic initiatives amplify the policy push and help bridge the gap between regulation and action.
Cutting emissions at the source
In the race to decarbonise, the first frontier for the Indian cement industry lies in boosting energy efficiency across plant operations. Upgrading to six stage preheater kilns, optimising cooler and fan systems, and capturing waste¬ heat recovery (WHR) are all core tactics. A report by the Cement Manufacturers’ Association mentions that the theoretical energy demand for clinker production ranges between 1,650 to 1,800 MJ per tonne of clinker, while drying raw materials adds another 200 to 1,000 MJ per tonne. For manufacturers, that means every percentage point of thermal or electrical energy saved translates directly into lower CO2 emissions — a pragmatic and cost-effective route to ‘cut.’
MM Rathi, Joint President – Power Management, Shree Cement, says, “Innovation is transforming the way cement is produced and used, bringing efficiency, strength, and sustainability together. Modern high efficiency plants now run kilns capable of producing up to 13,500 tonnes of clinker per day. With advanced coolers and pyro systems, they achieve energy use as low as 680 kilocalories per kilogram of heat and just 42 kilowatt-hours of power per tonne of clinker. By capturing waste heat, these plants are also able to generate 30–35 kilowatt-hours of electricity per tonne, bringing the net power requirement down to only 7–12 kilowatt-hours—a major step forward in energy efficiency.”
Reduction of the clinker to cement ratio remains a strategic lever in lowering both process emissions (from limestone calcination) and thermal fuel consumption. In India, the average ‘clinker factor’ is estimated at about 0.73 (i.e., 73 per cent of cement is clinker) as per recent modelling. According to a study by the Council on Energy, Environment and Water (CEEW), India’s average clinker ratio stands at 0.73 compared with a global average of 0.77. If India’s cement sector can move towards ~0.56 by 2070 as envisioned in some roadmap scenarios, the implication for emissions reduction is substantial. This shift is supported by the increasing uptake of supplementary cementitious materials (SCMs) and innovative binder systems.
Alternative raw materials such as fly ash, slag and calcined clay offer meaningful pathways to absorb clinker substitution and lower embedded emissions. For instance, ternary blends that combine limestone with calcined clay or slag are gaining traction in India. One recent paper notes that a calcined clay limestone composite cement (LC3) can cut the CO2 footprint by around 30 per cent compared to conventional Portland cement. Moreover, the standards in India (for example IS 18189) now allow ternary blends with calcined clay limestone up to about 20 per cent replacement. These materials not only help reduce the clinker content but also align resource use and circular economy imperatives.
Dr Avijit Mondal, Scientist, NTPC Energy Technology Research Alliance (NETRA), states, “The cement industry’s decarbonisation journey is both a technological and policy challenge. A mix of regulatory frameworks, carbon pricing, green financing and stakeholder collaboration will be essential to accelerate adoption of the 3Cs. For India, which is expected to remain the second largest producer and consumer of cement, the 3Cs framework aligns with national goals of Net Zero by 2070. As power and cement sectors increasingly converge through ash utilisation, renewable integration, and CCU the scope for cross industry partnerships is immense.”
Finally, the intertwining of material and energy efficiency is mediated through smarter process controls, automation and digitalisation — especially in grinding, raw mix preparation and kiln operations. Real time monitoring of power, kiln stability, clinker quality and alternative fuel admixture enables plants to operate closer to their thermodynamic minima. While the technology and cost curve are improving, what remains critical is industry wide scale up of these practices across India’s 600 plus integrated and grinding only units. The challenge is to ensure that improved efficiency and lower clinker factors translate into tangible CO2 savings in the near term, rather than being deferred into ‘future promise’.
Alternative fuels and co-processing
The traditional reliance on coal and petroleum coke in kiln operations is giving way to more sustainable fuel streams, as the Indian cement industry embraces alternative fuels and co-processing of waste. Within the energy intensive process of cement manufacture, where combustion can account for 30 per cent to 40 per cent of CO2 emissions, substituting fossil fuels with refuse derived fuel (RDF), biomass and industrial byproducts offers a compelling route to ‘cut’. A recent industry overview notes that only around 4 per cent of total energy input in the Indian cement industry currently comes from alternative fuels — up from about 0.6 per cent in 2010. This underscores that while the option is technically proven, scaling remains a major hurdle.
Raju Ramchandran, Senior Vice President and Head Manufacturing – Eastern Region, Safety and Sustainability, Nuvoco Vistas, says, “The journey to decarbonise cement and concrete touches every link in the value chain — from sourcing raw materials to producing clinker, from pouring concrete on construction sites to rethinking design with reuse, recycling and 3D printing in mind. Each stage offers an opportunity to reduce emissions through innovation and collaboration.”
The practical application of RDF and biomass in kiln operations is increasingly supported by policy and infrastructure. For instance, in the State of Karnataka the updated waste management rules require that cement plants within a 400 km radius of an RDF facility meet at least 15 per cent of their fuel needs through RDF by 2031. This shift not only reduces dependence on imported fossil fuels but also converts municipal solid waste and non-recyclable combustible fractions into high value fuel inputs — advancing circular economy objectives. However, the path is not without challenge: the heterogeneity in waste fuel properties can disrupt feeding systems in kilns, and the logistics of sourcing, processing and transporting fuels remain complex.
Ulhas Parlikar, Director MRAI and Global Consultant, explains, “The co-processing strategy of AFRs in India supports national waste management goals such as reducing landfill, incineration of hazardous and municipal wastes, and enabling safe resource recovery. Cement kilns are uniquely positioned to help address the country’s growing urban and industrial waste challenge, aligning climate goals and circular economy priorities. Many plants manufacturing clinker in India that belong to Adani Group, UltraTech, Dalmia, Shree, JK, JK Lakshmi, Nuvoco Vista, Vicat, Heidelberg, Ramco, KCP, Nagarjuna, Chettinad and others are operating at a reasonable scale of AFR utilisation. Some of these plants have even achieved a TSR level of more than 35 per cent. Some of these cement plants that have reached the higher levels of chlorine have also set up the chlorine bypass systems.”
Beyond substitution, co-processing waste as fuel and raw material unlocks additional value. For example, industrial byproducts such as tyre derived fuel (TDF) or processed biomass residues may replace traditional coal-based energy inputs, while providing safe disposal routes for otherwise difficult waste. The dual benefit of waste to energy and emission reduction is clearly recognised in global industry studies. Nevertheless, tapping this potential at scale in India requires standardised fuel quality, consistent supply chains, and investment in pre-processing infrastructure — all of which are emerging priorities for the next decade.
Innovating low carbon binders
Global and Indian research and industry activity around low carbon binders has moved from laboratory curiosity to commercial pilot and early rollout. LC3 and other ternary blends are receiving particular attention because they offer substantial clinker substitution without compromising strength or durability. A report by the Global Cement and Concrete Association (GCCA) notes that new low carbon binders such as LC3 can reduce embodied CO2 by around 30 per cent to 40 per cent compared with ordinary Portland cement, and several Indian manufacturers have announced plans to commercialise these formulations. Complementary market studies also point to brisk growth in ‘green cement’ demand in India — the India green cement market was valued in the low billions of US dollars in 2024 and is projected to grow at a mid-single digit CAGR through the decade. These figures underpin why major projects and infrastructure clients are starting to specify low carbon cements as part of sustainability procurement.
Gaurav K Mathur, Director and Chief Executive, Global Technical Services, opines, “Energy consumption is a significant concern in cement production, with a substantial portion of it attributed to the friction and heat generated by moving components in machinery. Lubrication management plays a pivotal role in optimising energy efficiency within all manufacturing plants. Advanced lubricants with superior friction reducing properties contribute to lower energy consumption by minimising resistance in moving parts and ultimately play important role in machine reliability.”
Geopolymer cements and alkali activated binders present another promising avenue, particularly where industrial byproducts (fly ash, GGBS) are locally abundant. Recent Indian academic work has showcased geopolymer mixes that can cut CO2 emissions by a large margin — in some laboratory studies by as much as 50 per cent to 80 per cent relative to conventional OPC, depending on the precursor and activator chemistry. While these numbers are impressive, practical deployment requires overcoming standardisation, supply chain and curing practice barriers; nevertheless, pilot projects and institutional testbeds in India are accelerating technology readiness and building the case for wider acceptance in structural applications.
Jigar Shah, Head – Application Engineering, ACM SBU, Henkel Adhesive Technologies India says, “Ash buildup—especially in high humidity environments—is a recurring challenge for maintenance teams. It clings to the inner walls of hoppers and silos, chokes flow paths, and forces shutdowns that no one has time for. And when the monsoon rolls in, the problem only intensifies. Ash particles are fine, abrasive and hygroscopic. They absorb moisture from the air, especially during the rainy season, and form stubborn layers on metal surfaces. Over time, this buildup narrows flow paths, increases system pressure, and eventually brings operations to
a standstill.”
Technology innovation in formulations goes hand-in-hand with process and digital innovations on the plant floor. Automation, advanced process control (APC), and AI driven optimisation are enabling plants to maintain kiln stability with higher rates of alternative raw materials and fuels, while improving energy efficiency and reducing reject rates. According to the Cement Manufacturers’ Association, predictive maintenance and real time monitoring can recover 5 per cent to 20 per cent of productive capacity lost to poor maintenance and can materially reduce fuel and power consumption when integrated with WHR and kiln control systems. Likewise, industry consultancy analyses show that AI enabled predictive maintenance can cut downtime by 20 per cent to 30 per cent and trim maintenance costs by 10 per cent to 15 per cent, savings that translate directly into lower operational CO2 intensity.
Taken together, these technological strands — new binder chemistries, expanded use of SCMs, and smarter plant operations — create a mutually reinforcing pathway to lower carbon intensity. Yet scale up remains the central test: moving from pilot batches of LC3 and geopolymer concrete to sustained commercial production requires changes in standards, investment in calcination and grinding lines optimised for alternative blends, and digitised quality control regimes. If Indian producers can synchronise material innovation with automation and process control, the industry can materially bend the emissions curve while meeting the country’s infrastructure needs.
CCUS: The next frontier
Carbon capture is rapidly moving from theory to pilot scale reality for the cement sector, driven by a suite of technologies tailored to the industry’s unique emission profile. Options under active development include chemical solvent scrubbing (amine systems), oxy fuel combustion (which produces a CO2 rich flue gas stream), solid sorbents, calcium looping and indirect calcination that decouple calcination from fuel combustion — each with different energy, space and integration requirements for an existing kiln. Several international demonstration projects have shown the technical feasibility of these routes, and the Global Cement and Concrete Association (GCCA) places CCUS as a central lever that could account for a large share of sectoral emission reductions by mid-century.
Nathan Ashcroft, Director, Low Carbon Solutions Energy and Resources, Stantec, says, “Cement plants are built for durability and efficiency, not for future retrofits. Most were not designed with spare land for absorbers, ducting or compression units. Nor with the energy integration needs of capture systems in mind. Retrofitting CCS into these existing layouts presents a series of non-trivial challenges. Reliability also weighs heavily in the discussion. Cement production runs continuously, and any disruption has significant economic consequences. A CCS retrofit typically requires tie-ins to stacks and gas flows that can only be completed during planned shutdowns. Even once operational, the capture system must demonstrate high availability. Otherwise, producers may face the dual cost of capture downtime and exposure to carbon taxes or penalties, depending on jurisdiction.”
India has begun to pilot a variety of capture concepts and small-scale test sites to assess techno economic practicality and downstream utilisation pathways. Recent initiatives include five test sites announced in 2025 designed to capture CO2 from cement production for conversion into synthetic fuels, construction aggregates and other products, and government industry workshops have highlighted pilot projects such as amine based and biological capture trials (including photobioreactor approaches) under development at research facilities and industrial partners. A report by GCCA India and a NITI Aayog linked workshop note that Indian pilots remain modest in capacity but are important for building local data on capture efficiency, impurity handling and integration costs.
Dr Yogendra Kanitkar, VP R&D, Pi Green Innovations, explains, “Carbon Capture, Utilisation, and Storage (CCUS) technologies are emerging as a critical lever for achieving deep emission cuts, particularly since process emissions are chemically unavoidable. Post combustion amine scrubbing using solvents like monoethanolamine (MEA) remains the most mature option, with capture efficiencies between 90 per cent to 99 per cent demonstrated at pilot scale. However, drawbacks include energy penalties that require 15 per cent 30 per cent of plant output for solvent regeneration, as well as costs for retrofitting and long term corrosion management (Heidelberg Materials 2025). Oxyfuel combustion has been tested internationally, producing concentrated CO2 laden flue gas, though the high cost of pure oxygen production impedes deployment in India.”
Global experience — particularly from Europe and Japan — is shaping India’s deployment roadmap by underlining two lessons: first, CCUS for cement is capital intensive and needs coordinated value chain thinking (capture, transport, storage or utilisation), often requiring public support and cross sector infrastructure; second, technology selection is context specific. Large European demonstrations such as the Brevik project in Norway (where a cement plant was retrofitted with capture and linked to offshore storage under the Longship initiative) and Japan’s government backed “Advanced CCS” projects are instructive on financing models, regulatory frameworks and clustering opportunities for shared CO2 transport and storage. These projects show that commercial scale CCUS in cement is achievable but hinges on policy certainty, fiscal support and the emergence of CO2 transport and storage hubs — lessons India is already factoring into its pilot planning.
Green logistics
Efficient logistics is becoming a critical lever for decarbonisation in the cement sector. In India, road transport still dominates finished cement distribution, with approximately 71 per cent to 72 per cent of cement moved by road and only around 25 per cent by rail (with waterways making up about 3 per cent to 4 per cent). Emissions associated with distribution have grown — one study found that in 2018-19, road transport accounted for 87 per cent of distribution related CO2 emissions for cement despite carrying about 62 per cent of the load. By contrast, rail borne cement accounted for 35 per cent of tonnage but only 13 per cent of emissions. Shifting more freight to rail and bulk logistics (for example by using specialised wagons and terminals) therefore presents a clear pathway to lowering the carbon footprint beyond the plant gate.
Ashwini Khunte, Regional Head – Sales and Marketing, Martin Engineering, elaborates, “Even though the entire cement operation depends on conveyor performance, the importance of clean belts to overall productivity is rarely understood or prioritised by busy plant maintenance teams. Fortunately help is at hand, with specialists from Martin Engineering in available to help Indian cement producers to identify the root causes of their pain points and recommend innovative solutions that are proven to work.”
Beyond mode shift, the industry is also embracing bulk handling and efficient packaging systems to optimise supply chain carbon performance. Bulk cement movements (rather than bagged) reduce multiple handling, mitigate dust losses, and permit more efficient transport and storage. A trade body note highlights that bulk movement of cement in India grew at a compound annual rate of 15 per cent to 20 per cent between 2014-15 and 2019-20. By building more rail silo to plant configurations, deploying dedicated bulk terminals and investing in larger capacity rail tankers, the industry is better positioned to reduce per tonne logistics emissions.
Industry collaboration and circular economy
Collaboration between cement manufacturers, municipal authorities and waste management firms is rapidly becoming a cornerstone of circular economy practices in India. For example, the Confederation of Indian Industry (CII) has launched a Waste Material Exchange platform which enables cement plants to access industrial and urban waste streams as alternative raw materials and fuels.
Jignesh Kundaria, CEO and Director, Fornnax, says, “Based on extensive R&D and on-site analysis at numerous cement plants, we have identified and addressed the key bottlenecks hindering AFR adoption in India. These challenges include the absence of a standardised process layout, the difficulty of handling high moisture or contaminated waste and a heavy reliance on imported equipment that lacks customisation for Indian conditions. Other issues include long lead times for spares, high maintenance costs for imported secondary shredders and inconsistent output from equipment that performs only primary or secondary shredding.”
India’s cement sector is increasingly ‘diverting waste materials from landfill via partnerships and collaborations’ and thereby reducing both disposal costs and input material emissions. One study estimates that the Indian cement industry could reduce its dependence on virgin raw materials by up to 20 per cent to 30 per cent through systematic utilisation of waste derived feedstocks and byproducts under circular economy models. Such collaborative efforts not only cut resource extraction and emissions but also build a symbiotic industrial ecosystem where the waste output of one sector becomes the input for another.
Olli Hänninen, Owner and Co-Founder, Moviator Oy, states, “Decarbonising cement will not happen overnight. It will take imagination, cross sector collaboration and new standards that reward permanent carbon binding. But the tools are already here — from smarter slag processing to direct CO2 mineralisation. Moviator’s work in refining steel skulls and utilising slag demonstrates that circular, low carbon materials are not science fiction. They are emerging now, one pilot and partnership at a time.”
Despite the promise, the road to full circularity is paved with challenges that require coordination across multiple stakeholders. Material recovery infrastructure, consistent waste feedstock quality, and transparent liability frameworks need to be developed in tandem with policy incentives and industry buy in. A systematic review in 2025 emphasises that while interest in circular economy practices in the cement sector is ‘substantially increasing’ (with an annual publication growth of 23.4 per cent) it also warns that ‘scaling remains constrained by regulatory, socio-economic and logistical barriers. In response, a number of Indian cement companies have signed MoUs with local municipal bodies and waste management firms to secure streams of municipal solid waste, construction and demolition debris and industrial byproducts — signalling a shift from isolated pilots to ecosystem level collaboration.
Towards Net Zero cement
As the Indian cement industry charts its trajectory toward net zero emissions, the horizon offers both urgency and opportunity. By 2030, the global roadmap for cement envisages a reduction in CO2 intensity to roughly 0.45 tonnes per tonne of cement — a level that Indian producers, if aligned with the 3 Cs of decarbonisation (Cut emissions, Cement innovations, Carbon capture and utilisation), could realistically aim for. By 2050, the ambition in many roadmaps is to hit near zero operational emissions, with residual emissions offset or captured — a target that places technological adoption, scale up and financing at the heart of the transition.
Achieving these milestones will demand more than incremental change. Policy frameworks must strengthen carbon pricing or trading mechanisms that include cement, fiscal support for CCUS and alternative binder investments, regulatory push for low carbon procurement, and infrastructure for CO2 transport and storage are essential enablers. Simultaneously, private investment from both domestic firms and global players must flow into retrofits of vintage plants, digital and automation upgrades, large scale alternative fuel/coprocessing systems
and full-scale carbon capture installations. The confluence of innovation, structured finance and regulatory certainty will determine how smoothly the industry migrates from pilot phase ambition to full scale deployment.
Ultimately, intent and action must remain in sync. Indian producers possess competitive strength in large scale, strong domestic market growth, and a rich resource base. With the accelerating uptake of low clinker cements, automation across operations and strategic collaborations for waste to resource value chains, the critical ingredients are already in play. What remains is execution at pace and scale — delivering the decarbonised cement that India’s infrastructure vision demands, while ensuring that the industry contributes positively to the nation’s climate and sustainability goals.
– Kanika Mathur














 Concrete1 month ago
 Concrete1 month ago

 Concrete4 weeks ago

 Concrete4 weeks ago