Connect with us

Economy & Market

Controlling Dust at Critical Connections

Published

on

Shares

Jerad Heitzler, Training Manager, Martin Engineering, writes about controlling dust at conveyor transfer points to protect worker health and to extends equipment life and boost operational efficiency.

Transfer points are critical connections between key stages of cement manufacturing, but they are notorious as a source of fugitive dust. After all, whenever materials like crushed limestone, shale or clinker drop onto a moving conveyor, dust emissions are inevitable, aren’t they? Not necessarily.
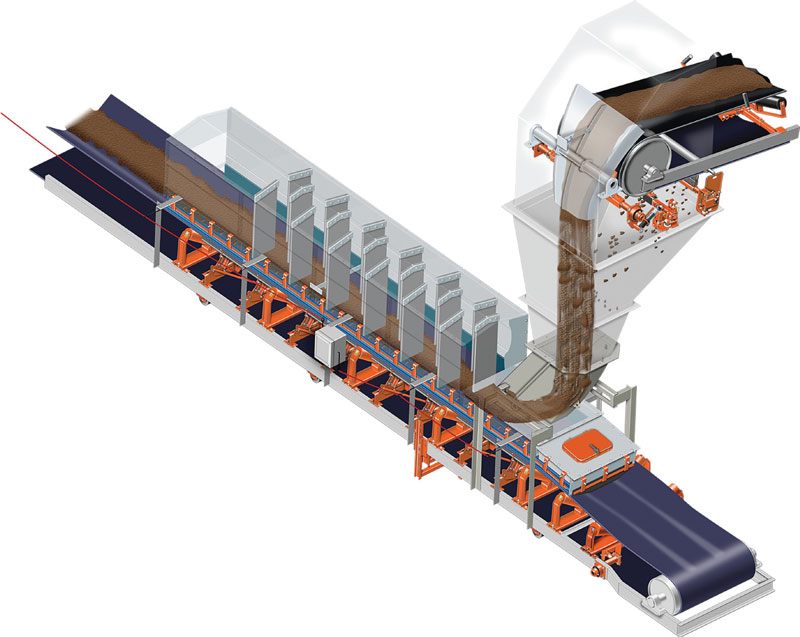
When loose materials hit a moving conveyor belt, the impact causes some of the cargo to disperse, particulates become airborne, and the subsequent air turbulence forces the dust toward the nearest opening. If the environment isn’t sealed, the dust-filled air creates a serious workplace health and safety hazard, a problem that’s exacerbated if dust is allowed to build up.
Dust emissions don’t just create a harmful environment for those working in the area. Abrasive particulates make their way into exposed machine parts and rolling components, causing them to wear quicker, seize and require replacement sooner. Particulates also clog air intakes of nearby equipment, further raising the need for maintenance and downtime. Then as it settles, dust builds up to cover walkways and stairs, engulfing control units, obscuring signage and, in some cases making access for maintenance impossible without a full shutdown and clean-up.
Often, the biggest issue is the team’s lack of understanding of the underlying sources of dust at transfer points. In fact, there are just three factors that cause dust in any minerals processing plant:
a. Material degradation from crushing and milling, as well as transfer and movement, which creates an abundance of fine particles that become airborne.
b. Air flow through the plant is a key factor in carrying airborne particulates and this can be controlled with the right design, considering material speed, volume and fall.
c. Transfer point design is one of the main causes of dust emissions and spillage on conveyor systems, often exacerbated due to desired increases in productivity.

Best practices for transfer point dust control

  • Avoid belt sag with impact cradle support. For each transfer point, support the belt the entire length of the chute wall so it doesn’t sag away from skirting. The pressure from air turbulence is enough to push dust and fines out of these gaps, causing excessive dust and spillage.
  • Use wearliners to increase system life. Modern chute designs raise the height of the chute, providing more room for dust to settle in the stilling zone and allowing space for an external wearliner. Without it, the rubber skirting takes the force of falling materials which lowers the equipment’s life.
  • Seal the environment with belt skirting. Single skirting should be cut to the belt’s trough angle for a tighter seal and mounted externally for easy and safe adjustment. Self-adjusting skirting has spring-driven latches that offer slight downward pressure for reduced maintenance. Dual skirting offers a single skirt with a rubber flap that provides a second layer of sealing and protection from spillage and emissions.
  • Use dust collection only when necessary – ‘Passive dust control’ uses engineered solutions such as controlled loading, wearliners, skirting, curtains and modular enclosures first. When there are length or space restrictions for chutes, which prevent an extended settling zone, dust bags and mechanical air cleaners are still effective, but they can require more maintenance, so sealing at source is better.
  • Slow the exiting air velocity. Some flow of air is still going to be exiting the system, but the key is slowing it to under 200 fpm (1 m/s), slow enough to allow for settlement happen. Adding a tail panel and curtains is essential to this but simply adding them at the ends does not accomplish the proper stilling environment required. Understanding the air flow and then strategic placement is the key to reducing exiting air velocity.

Conclusion
Improving workplace air quality in a cement plant seems like a challenge but eliminating dust delivers numerous benefits, notably in health and safety, housekeeping, efficiency, productivity and cost reduction. Of course, conveyor transfer points are not the only source of dust. However, as one of the most prevalent generators of particulate emissions in any bulk handling operation, addressing these is an excellent place to start.
By following best practices using modern and well-designed retrofitted components, and expert advice from experienced technicians, operators can tackle dust in a methodical way. Once the major dust sources are addressed, it becomes easier to identify emissions from other parts of the operation with the ultimate goal of a clean, efficient and
safe operation.

About the author:
As programme manager and lead instructor for Martin Engineering’s FOUNDATIONS™ Training Workshops, Jerad Heitzler is a leader in helping the industry learn how to make the handling of bulk materials cleaner, safer and more productive.

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

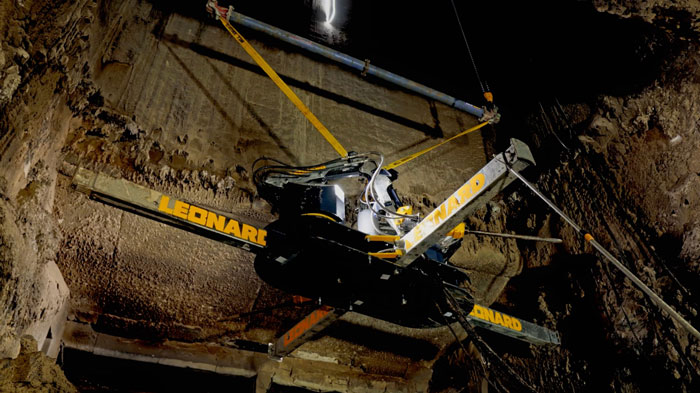
 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.


Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

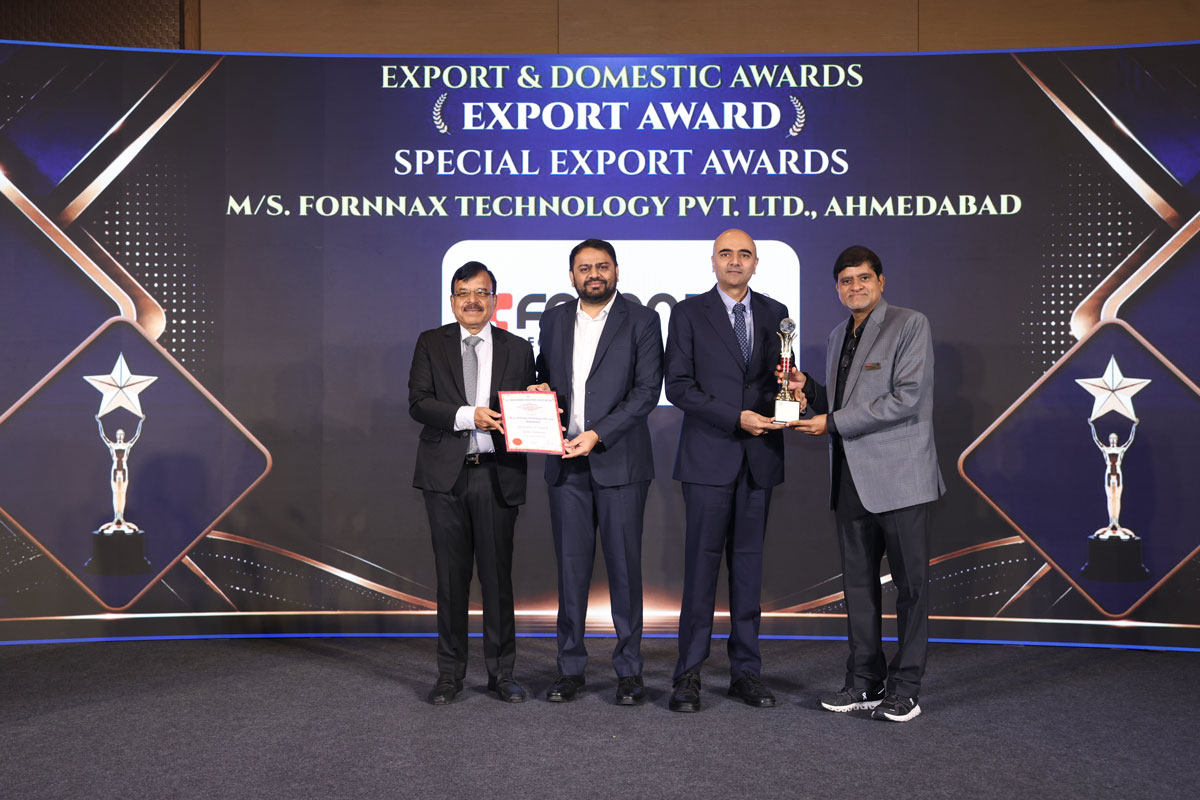
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds