

Concrete
Material Benefits


Supplementary cementitious materials are changing the way and the speed at which cement manufacturing is moving on the spectrum of environment sustainability. With large stakes on the line for achieving net zero targets, how is the Indian cement industry rising up to the challenge, finds out ICR.
Across the globe, cement is one of the most consumed and important materials for building all infrastructure. From homes, to factories, roadways or tunnels, everything would require cement in one form or the other. India especially is moving towards becoming infrastructurally strong with new projects in the works across the sub-continent. All infrastructural projects demand the consumption of concrete and cement, which has led to the rise of concrete requirement, thus, increasing the production of cement.

around 379 million tonnes in light of the country’s renewed focus on big infrastructure projects. Source: RBI Reports
India is the second largest producer of cement. Limestone is at the core of its production as it is the prime raw material used for production. The process of making cement involves extraction of this limestone from its quarries, crushing and processing it at the cement plant under extreme temperatures for calcination to form what is called a clinker (a mixture of raw materials like limestone, silica, iron ore, fly ash etc.). This clinker is then cooled down and is ground to a fine powder and mixed with gypsum or other additives to make the final product, cement.
Limestone is a sedimentary rock composed typically of calcium carbonate (calcite) or the double carbonate of calcium and magnesium (dolomite). It is commonly composed of tiny fossils, shell fragments and other fossilised debris. This sediment is usually available in grey, but it may also be white, yellow or brown. It is a soft rock and is easily scratched. It will effervesce readily in any common acid. This naturally occurring deposit, when used in large volumes for the cement making process is also depleting from the environment. Its extraction is the cause of dust pollution as well as some erosion in the nearby areas.
The process of calcination while manufacturing cement is the major contributor to carbon emission in the environment. This gives rise to the need of using alternative raw materials to the cement making process. The industry is advancing in its production swiftly to meet the needs of development happening across the nation.
Aligning Sustainability Goals
In one of its recent bulletins, owing to India’s announcement at the Glasgow Climate summit to reach net-zero by 2070, the RBI noted that with India aiming to reach half of its energy requirements from renewables and reduce the economy’s carbon intensity by 45 per cent by 2030, it ‘necessitates a policy relook across sectors, especially where carbon emission is high’ and ‘cement industry is one of them.’ However, it said, recent developments in green technologies, particularly related to reverse calcination, offer ‘exciting opportunities’ for the cement sector.
The RBI report noted that India’s cement production is expected to reach 381 million tonnes by 2021-22 while the consumption is likely to be around 379 million tonnes, in the light of the country’s renewed focus on big infrastructure projects like the National Infrastructure Pipeline, low-cost housing (Pradhan Mantri Awas Yojana), and the government’s push for the Smart Cities mission is likely to drive demand for the cement in future. On similar lines, according to the Eco-Business news portal report of April 2022, the India Energy Outlook 2021, which notes that most of the buildings that will exist in India in 2040 are yet to be built. Their projection suggests that urbanisation in the near future will demand an increase in infrastructure, which will ultimately lead to increase in the cement consumption.
With these forecasts in mind, RBI has recommended that there is a need to align India’s economic goal with its climate commitments by implementing emerging green tech solutions. It has also recommended an increase in finance towards green sustainable solutions through subsidised interest loans, proactive engagement with the leading research institutes and countries involved with green tech-related innovation in the cement industry.
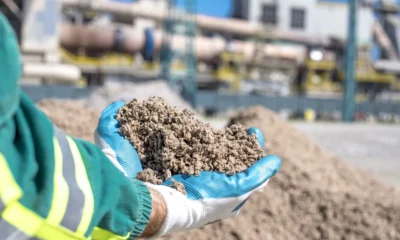
“When clinker is blended with other supplementary cementitious materials like fly ash, slag or both, products are called Portland Pozzolana Cement (PPC), Portland Slag Cement (PSC) and composite cement (CC) respectively. Blended cement products have a much lower carbon footprint than OPC. Since clinker manufacturing is the phase where most thermal energy is consumed and CO2 is emitted, reducing clinker factor in cement not only results in lowering the process CO2 but also the thermal energy and electrical energy requirements,’’ says Manoj Kumar Rustagi, Chief Sustainability and Innovation Office (CSIO), JSW Cement.

and lower greenhouse gas emissions are some of the
advantages of blended cement.
Alternative Raw Materials
Alternative cementitious materials are finely divided materials that replace or supplement the use of portland cement. Their use reduces the cost and/or improves one or more technical properties of concrete. These materials include fly ash, ground granulated blast furnace slag, condensed silica fume, limestone dust, cement kiln dust, and natural or manufactured pozzolans.
“Each material has its own composition and behaves differently during the burning process. In order to maintain the consistent clinker quality and stable clinkerisation process, we need to analyse these materials with respect to quality (during raw mix design) and also impact on the environment (if any harmful gases are released). There are certain materials which come in both ARM and cement additives like Ashes from coal fired thermal plants and slag from steel plants that have to be looked at from various angles,” says Gulshan Bajaj, Vice President (Technical), HeidelbergCement India.
The use of these cementitious materials in blended cements offers advantages such as increased cement plant capacity, reduced fuel consumption, lower greenhouse gas emissions, control of alkali-silica reactivity, or improved durability. These advantages vary with the type of alternative cementitious material.
Cement manufacturers are moving towards incorporating these supplementary cementitious materials in their raw material:
Fly Ash: Containing a substantial amount of silicone dioxide and calcium oxide, fly ash is a fine, light, glassy residue generated during ground or powdered coal combustion.
Ground Granulated Blast-furnace Slag (GGBS): It is a by-product of the iron and steel industry. In the blast furnace, slag floats to the top of the iron and is removed. GGBS is produced through quenching the molten slag in water and then grinding it into a fine powder. Chemically it is similar to, but less reactive than, Portland cement.
Silica Fume: It is a by-product from the manufacture of silicon. It is an extremely fine powder (as fine as smoke) and therefore it is used in concrete production in either a densified or slurry form.
Slag: It is a by-product of the production of iron and steel in blast furnaces. The benefits of the partial substitution of slag for cement are improved durability, reduction of life-cycle costs, lower maintenance costs, and greater concrete sustainability. The molten slag is cooled in water and then ground into a fine powder.
Limestone Fines: These can be added in a proportion of 6 to 10 per cent as a constituent to produce cement. The advantages of using these fines are reduced energy consumption and reduced CO2 emissions.
Gypsum: A useful binding material, commonly known as the Plaster of Paris (POP), it requires a temperature of about 150OC to convert itself into a binding material. Retarded plaster of Paris can be used on its own or mixed with up to three parts of clean, sharp sand. Hydrated lime can be added to increase its strength and water resistance.
Cement Kiln Dust: Kilns are the location where clinkerisation takes place. It leaves behind dust that contains raw feed, partially calcined feed and clinker dust, free lime, alkali sulphate salts, and other volatile compounds. After the alkalis are removed, the cement kiln dust can be blended with clinker to produce acceptable cement.
Pozzolanas: These materials are not necessarily cementitious. However, they can combine chemically with lime in the presence of water to form a strong cementing material. They can include – volcanic ash, power station fly ash, burnt clays, ash from burnt plant materials or siliceous earth materials.
Dr Sujit Ghosh, Executive Director – New Product and R&D, Dalmia Cement (Bharat), says, “Blended cements made using supplementary raw materials, have ‘additional’ activated silica (SiO2) and/or activated lime (CaO), which when co-processed with cement clinker, provide ‘additional’ cementitious gel paste (complex calcium-silica-oxide-hydrates) when mixed with water, that renders improved strength and durability to the cement-concrete structure.”
He adds, “With specialised processing and with the use of performance enhancers, blended cements using supplementary raw materials, provide acceptable rate of strength gains, comparable to pure-clinker cement and top-class long-term durability, with lower carbon footprints and at the same time effectively finding value-solution to other industry wastes!”
Besides having the advantage of lower emissions and better environmental conditions, use of supplementary cementitious materials also has a cost benefit. “Cost of production depends on the plant location, limestone and raw material quality. The source of alternative raw materials for some plants are significant and in some instances because of high logistic cost economics do not work out. For example, if a cement plant is located near the industry where chemical gypsum is generated, there will be a significant gain to that particular cement plant,” says Rajpal Singh Shekhawat Senior General Manager (Production and QC), JK Lakshmi Cement.
Bio Solutions
Researchers at the Indian Institute of Technology, Madras, are finding ways to use bacteria to develop bio-friendly cement and reduce carbon dioxide emission, as per a report in The Hindu earlier this year.
Professor GK Suraishkumar and assistant professor Nirav Bhatt in the Department of Biotechnology and Subasree Sridhar, a research scholar, are conducting the research. They have developed a mathematical model to produce an alternative to current cementation process. They have suggested the use of bacteria like S Pasteurii, which will microbially-induced calcite precipitation.
This bio cement will require temperatures in the range of 30 to 40 degrees as opposed to the traditional process that would require over 900 degrees for the calcination process. The emitted carbon dioxide will be negligible in this case and industrial waste like lactose mother liquor and corn steep liquor can be used as the raw materials for the bacteria, thus making the manufacturing of this cement more economical.
One of the most important ways of reducing carbon emission in cement manufacturing is the use of alternative raw materials from various other industries. This gives way to a circular economy, utilising waste from other industries and bettering the environment with reduced emission of harmful gases, especially carbon dioxide. It also helps the avoidance of landfills or ocean pollution, as waste of industries is utilised in manufacturing cement. Overall, new compositions of cement are the future.
-Kanika Mathur







Concrete
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement has deployed more than 70 EVs across its logistics network.





Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027

JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant

Martin Engineering Appoints Ashwini Khunte as India General Manager

CII Calls for Greater Alternative Fuel Use in Cement Industry
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant
Martin Engineering Appoints Ashwini Khunte as India General Manager







