

Economy & Market
Safety is at the centre of everything that we do

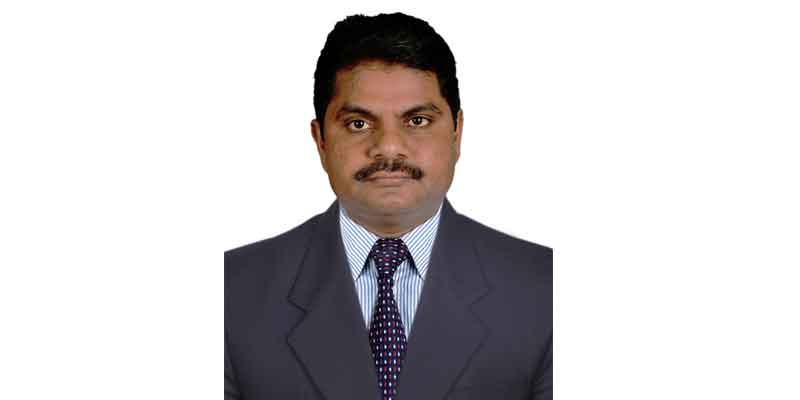
Perumal Jagatheesan, Safety Head, HeidelbergCement India and Zuari Cement, discusses the safety norms and standards at a cement plant, while underscoring the importance of training, safety protocols and practices and the use of technology at a cement plant.
How would you define a safe cement plant? What are the major areas of concern for safety in the cement work environment?
Safety in cement plant starts from its design itself, carrying out proper layout and machinery safety protection. It is designed to limit the risk to personnel for accident or injury. Different hazards involved in the process starts from extracting limestone from mines to dispatching the cement. Robust safety management system implementation is vital for safe cement plant to mitigate the hazards involved in blasting activity in mines, heavy mobile equipment, heavy crushing machineries, material transporting systems and clicker production.
Various hazards includes: blasting and mining of limestone, high temperatures in pre-heater tower (as high as 900 degrees centigrade), storage of coal in sheds, cement grinding, heavy inbound and outbound truck movements carrying all raw materials and the product from the plant etc.
Safety management system includes risk assessment and control measures for all the processing activities, well designed permit system, safeguarded machineries, firefighting systems, clean workplace, safety audit, trained and competent manpower are important elements to have safe cement plant. Major areas of concerns are the maintenance work in confined space, pre-heater cyclones and silos, work at height jobs, materials transportation systems, heavy mobile equipment and truck movement are major risks in a cement plant operation.
What are the key challenges in ensuring safety at a cement plant?
People in any industry do not appreciate to work in a hazardous work environment. Hence, our slogan “Someone in waiting for you at home” explains well about itself.
The manufacturing and distribution of cement is a high-risk enterprise but creating safe work environment in the cement industry is achievable. There are many causes of accidents in cement industry, however there are three major areas that can lead to serious incidents.
- Traffic and mobile equipment: Traffic is caused from inbound and outbound trucks. Mobile equipment are dumpers that bring limestone from mines to crushers. Rigorous intra and inter plant movement of traffic is an area of major risk.
- Fall from height and falling objects
- Moving/Starting Equipment
Some of other more serious hazards include working in confined spaces and working with hot materials in the pre-heater.
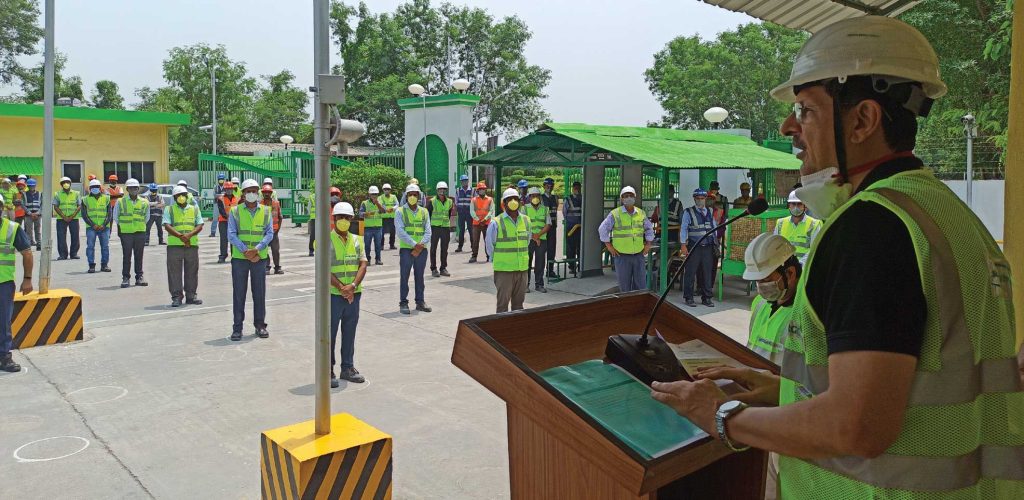
There are several key-factors to achieving sustainable safety in the cement industry we have implemented the following health and safety initiatives at all our HeidelbergCement India plants to keep the safety momentum and safety awareness throughout out the year. We have monthly safety gate meeting, monthly safety theme and communication, plant safety star award program which is once in four months, strict compliance of our safety cardinal rules, safety zone system, hazard identification and risk assessment control measures, work permits and procedures, safety inspections and audits, fire prevention and protection, accident and near miss incident reporting, and investigation to identify the root cause along with implementation of corrective actions with training on lessons learned across the HeidelbergCement India plants.
For example, of a near miss incident or any incident happened at any plant, incident learnings will be communicated across all HC India Plants to take appropriate corrective actions if similar unsafe situation exists in their plant.
Mock drill and emergency handling, safety induction and behavior safety training for workers at all our plants, award and penalty system, review of safety system for continual improvement, safety conversation with workmen by line managers, and monitoring implementation by inspecting and auditing controls to ensure they are working as expected by the company. Ensuring operating process and training materials are updated regularly and incase of any new process/system added in the plant. These are the various safety management systems to ensure safety in operation and maintenance of the plants.
What is your first response in case of hazard in the plant?
Our first response would be to immediately isolate the hazard, to prevent personal interference or people going in the proximity of the hazard.
Hazards can be classified into three categories that is low, medium and major.
When a major hazard occurs, we immediately stop the work and take the corrective action immediately. During such circumstances, the area is isolated, and the operational team is called to discuss and make corrective and preventive actions in the stipulated target time.
Tell us more about the personal safety equipment used in the plant by working professionals.
In safety management system, personal protective equipment (PPE) is the last line of defense to prevent injuries, but it is very essential and mandatory. In the hierarchy of most effective controls to least effective controls are, the first one is elimination, which means physically remove the hazard. Second one is substitution, which means replace the hazard. Third one is engineering controls, which means isolate people from hazard by providing guarding. Fourth one is administrative controls, that includes change the way people work. Last control is the personal protective equipment (PPE) which protect the worker. PPE will not prevent the accidents from happening, but certainly it will reduce the severity of injury.
We have mandatory PPE and job specific PPE. Mandatory PPEs are required for people entering the plant including the visitors. Mandatory PPEs are safety shoes, safety helmet with chinstrap, safety goggles and high visibility waist jacket. Then comes PPE for specific jobs, like for a worker working at more than 1.8 meters height should have a full body harness with shock absorber with a double lanyard. For gas cutting, safety goggles, apron, hand gloves. For welding work, welders face shield, apron, leg guard, hand gloves. Similarly, we have implemented specific PPEs for every work that is being done at our factory.
Do hazards often happen in a cement plant or are they a rarity?
In all our plants we have a plant safety advisor. When the plant is in operation, a process related hazard can happen in rare occasions, however, any individual can unknowingly initiate the unsafe act giving rise to an incident.
To perform any maintenance work, ‘Permit to Work’ needs to be obtained from the authorized personnel. Before closing the permit, it must be ensured that all equipment guards and Protections are in place. If that is missed, it can give rise to a hazard. If any safety cardinal rules violation observed in the plant, a warning letter is issued to the concerned engineer/manager to correct his behavior and to prevent repeat occurrence of similar major hazards in future.
What are major health concerns cement plant employees face as an occupational hazard?
Cement industry plays a vital role in development of the country and create employment opportunities. Adding to it, safe workplace in cement industry is also one of the important factors to prevent occupational health diseases.
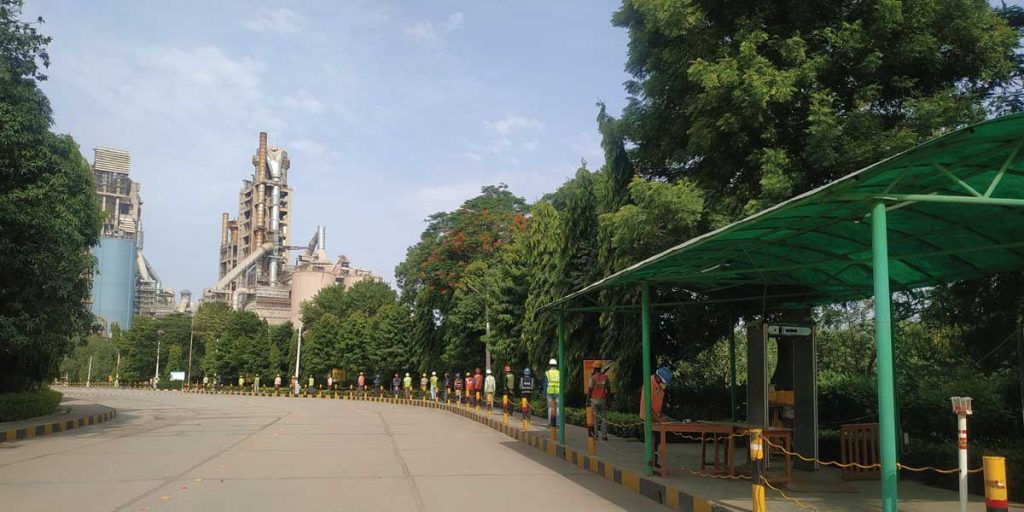
Cement plant workers are exposed to different types of hazards such as fume, gas, and dust which are risk factors to developing occupational diseases. The manufacturing units of a cement factory such as raw mill, preheater, kiln, coal mill, cement mill, cement storage silos, cement packaging section are point sources of pollution or dust emission. Exposure to cement dust leads to respiratory issues, also affecting skin and eyes. It also depends on the duration of a person exposed in the dust.
However, we as a responsible corporate ensure utmost care for our employees by ensuring proper use of PPEs along with installation of proper dust / fume / gas controlling equipment’s. We believe that all employees should come smiling to our establishment should go back home smiling.
Tell us about the key precautions one must take while working in the cement plants to avoid the occupational hazards.
We should have efficient dust control system at source to collect the dust (an engineering control method) i.e. baghouse dust collector, electrostatic precipitator (ESP) and a belt conveyer hood suppression system, water sprinkling on roads and ensuring good housekeeping on regular basis to control dust and to prevent occupational health diseases. These are some of the systems that all cement plants will have to prevent dust emission.
These must be maintained on regular basis to keep them in good working order and conduct air monitoring to measure worker exposures and ensure that controls are providing adequate protection to workers. Not only maintaining the system but we also have to measure the level of dust in the plant ensuring it is with in the statutory limit. If it exceeds the limit, actions must be taken to reduce the emission in the factory. As the last defense, we must provide and ensure the usage of suitable dust masks for all the workers for preventing the dust inhalation.
Can you tell us about a safety issue that occurred in any of your plants and how was it managed?
A workman used to stand on the top of the truck for doing tarpaulin to cover them post loading and removing the tarpaulin for unloading which bring raw materials to the factory. This involves risk of the workman slipping and falling from height. To eliminate this risk, we have provided safe access platforms with fall protection arrangement at all our plants. There would be a platform with a staircase, from where access is provided to the truck top, and from the center point we have given a lifeline across the truck with a full body harness to the workers.
What are the safety trainings provided to your employees? Could take us through
the process?
For all new employees and workmen joining the organization, we have a safety induction training module that covers all the safety rules and regulations of the plant. We also have a safety movie, shot in our own plant, that we show to our workers during safety induction training before issuing them a plant entry gate pass.
For work at height jobs, we conduct height phobia test to ensure that the worker doesn’t have a fear during working at heights. We have a mock structure where a workman is sent to a height and his blood pressure is checked before going up and after coming down. The doctor tells us with his blood pressure if they have passed the test. Those who pass are given the height work pass.
Training on safety behavior and training on lockout, tagout, tryout which is an electrical isolation work permit system, training on confined space, safety toolbox before starting the job, job specific training, firefighting training, training on safety standards etc. We have group safety standards for work at height, confined space work, electrical isolation (LOTOTO) and machine guarding.
Tell us about some of the good safety practices implemented in your HC India plants?
Occupational health and safety are the core value of our company and safety is at the center of everything that we do-from the daily routines in our plants. We are desired to conduct our business with “Zero Harm” to the people we work with and we strive to create a healthy and safe work environment for all our employees, contractors, and stakeholders. We believe that we are good in safety and we are good in
achieving new milestones in business. Safety is a critical success factor for all operational performance and is integrated in all business decisions including greenfield and brownfield projects and employee performance evaluation.
Safety cardinal rules
- There are “Safety Cardinal Rules” that all employees and contractors working with us must comply and follow:
- All personal protective equipment (PPE) required for a given task must be properly used.
- Equipment must be properly isolated from all inherent energy sources and must be tested to ensure it cannot start or move prior to conducting any task.
- Safeguards must be in place before the equipment is started or restarted.
- Entry into confined spaces is only allowed for competent persons and with a permit to work signed by the responsible superior.
- All occupational incidents are reported and investigated to identify the root causes and to set up corrective actions and lessons learned.
- Driving for the company is done in strict accordance with the local laws and company requirements.
Monthly safety theme
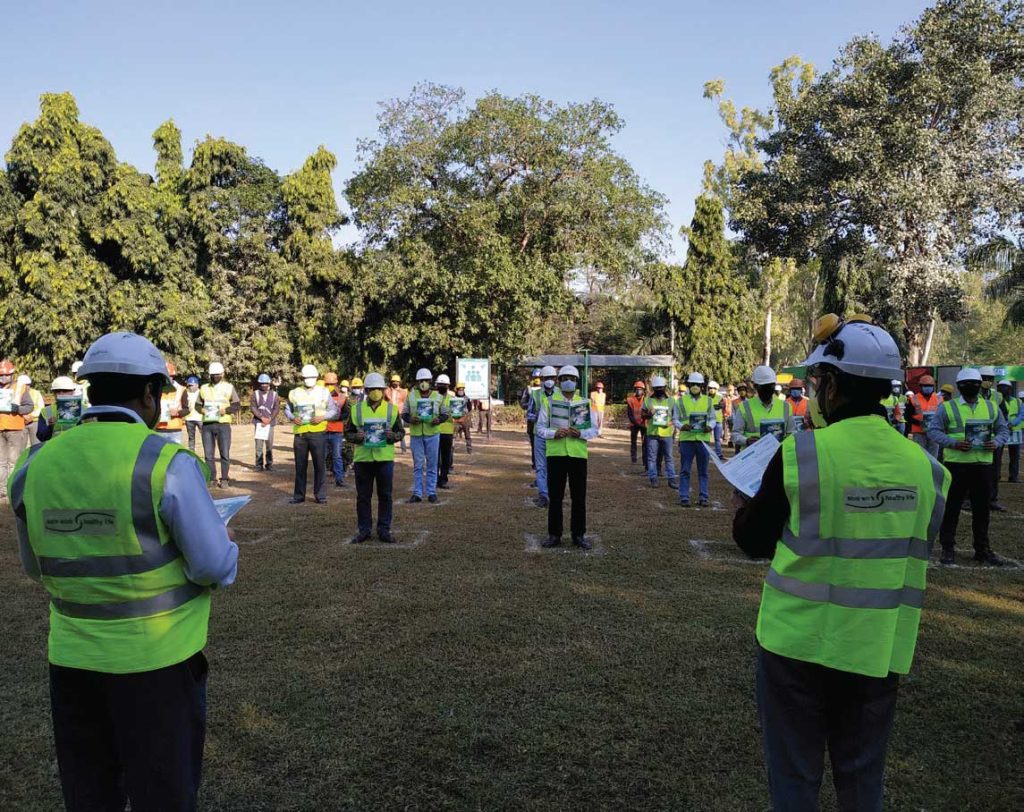
We have a monthly safety theme launching system. Across all plants, on the first day of each month, respective plant manager launches the theme for the month between a gathering of workers. The catalogue gives details of the risk, it causes, and mitigation measures is printed in a regional language and distributed to all workers. The aim is to see that every relevant worker gets covered and made aware of the risks and mitigating measures. Benefits noticed from the monthly safety theme program from all plants is rise in safety awareness among the workers on the potential risk and mitigation measures.
Plant Safety Star Award Programme:
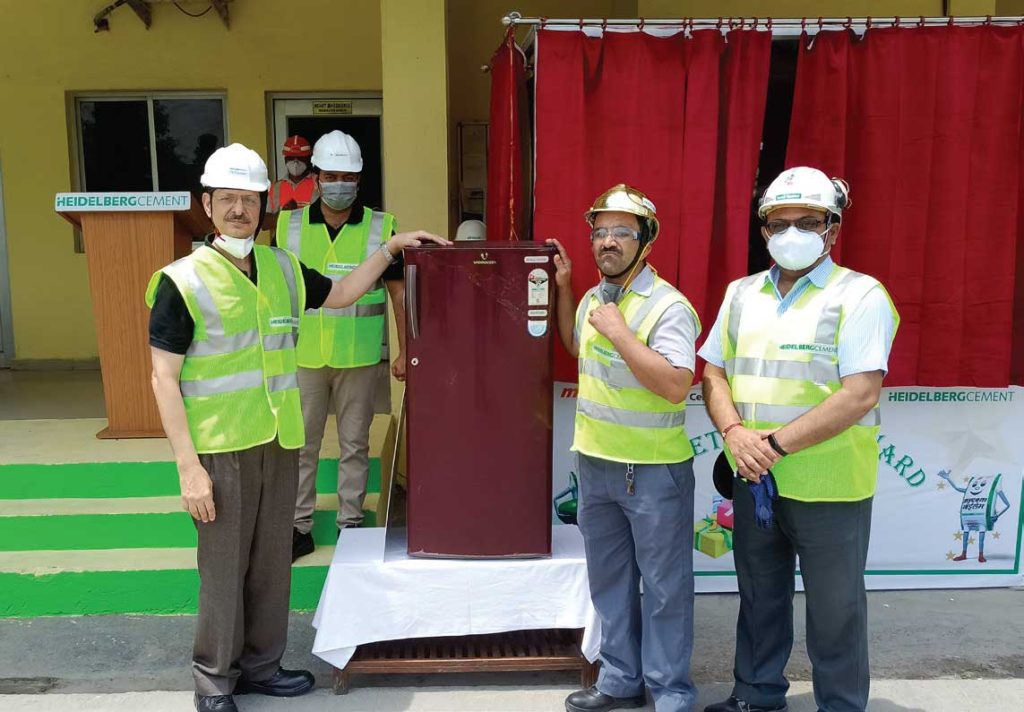
Plant Safety Star Award programme is unique to HC India initiated by the people and for the people. It identifies people having high regard for safety and are role models for others. Plant safety stars are selected from the workman level through the process of nomination followed by written examination covering topics related to health and safety rules and regulations. The nominations are done by fellow workman, and the one who secures maximum score is declared the Safety Star of the plant in the given trimester. Attractive gifts and award are presented to the winner by Managing Director and Director Technical in presence of all the workforce in the plant and address the gathering to motivate and enhancing the safety culture.
Safety zone system:
HC India encourages employee engagement where they achieve the sense of pride for having shouldered the responsibility of ensuring that everyone returns home safely to be with their loved ones. The entire plant is divided into zones depending on site conditions considering its layout, activities performed, ease of accessibility and monitoring. For each zone a head is chosen who selects representatives from all departments located in the safety zone headed by him. The area under each zone is further divided and allotted to each member responsible for specified section. By such divisions, communication will be more effective with a sense to communicate the hazards and risks to all the people in the zone. Increase the level of safety awareness and identify unsafe behavior to ensure compliance to best safety practices, highlight the near misses, incidents and share the learning, improve and sustain good housekeeping practices. So, the safety zone system is very effective in case of maintaining good housekeeping in the plant. Our tagline is, ‘Someone is waiting for you at home’.
What is the role of technology and automation in safeguarding the cement making process?
Considering the safety aspect, safety interlock switches are used to prevent machine operation or start up in an unsafe situation. Like, the guard is provided with interlock switch, equipment will stops working if the rotating part guard is open.
How frequently does you plant have safety audits and who does them?
All our manufacturing plants are certified under ISO 45001-2018 Occupational health and safety management system certified by TUV SUD South Asia Private limited. The safety audits are conducted by TUV external auditors once in a year and by an internal auditor once in 6 months. Also, in all the plants safety inspections are conducted by Head Safety once in three months. Daily, plant safety advisors carry out plant safety inspections in order to observe the physical conditions of work and the work practices / procedures followed by the workers. The safety advisors also render advice on measures to be adopted for removing unsafe physical conditions while at the same time preventing unsafe actions by workers and apprise the same to the factory manager on regular basis.
-Kanika Mathur










JK Lakshmi Cement Begins Rs 110 Billion Assam Plant Project

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027

JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant

Martin Engineering Appoints Ashwini Khunte as India General Manager
JK Lakshmi Cement Begins Rs 110 Billion Assam Plant Project
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant





