Connect with us

Economy & Market

March against asbestos

Published

on

Shares

Though its use is banned in most countries, the asbestos industry continues to thrive at the cost of putting millions of people at risk.

Asbestos has an uncanny habit of repeatedly making headlines. Recently, the Drug Controller General of India issued a show cause notice to Johnson & Johnson for its alleged use of asbestos in its talcum powder. In February this year, authorities imposed a fine of more than $40,000 after asbestos was found in the construction of a school in Michigan, usa. In New Zealand, a maternity home was demolished in March in Taupo District Council after officials detected asbestos materials. Asbestos has been used for different purposes since prehistoric times, but today the campaign against its use is building up, as exposure can lead to a wide range of diseases. When asbestos materials are damaged or broken during processing, the tiny fibres become airborne and can be easily inhaled at a significant rate. Once inhaled, asbestos fibres lodge in the lining of the throat, lung, or stomach, causing cells to mutate and become cancerous.

Well-documented effects
According to the World Health Organization (WHO), about 125 million people are directly exposed to asbestos in their workplace annually. More than one million workers die each year from an asbestos-related disease. In 2004, asbestos-related diseases such as lung cancer, mesothelioma and asbestosis from occupational exposure resulted in more than 1.5 million Disability Adjusted Life Years.

That’s why 60 countries have banned the use of this toxic material. Though the Supreme Court of India banned its use on January 21, 2011, it is still being widely used across India. The country uses about 3,50,000 tonnes of asbestos annually and the industry is growing by 12 per cent annually. More than 50 factories use chrysotile, also known as white asbestos, as an ingredient in cement roofing sheets, wall panels, pipes and other products. Asbestos deposits are found in Andhra Pradesh, Bihar, Jharkhand, Karnataka, Rajasthan and Manipur. Workers at cement factories in Ahmedabad, Hyderabad, Coimbatore and Mumbai are suffering from the lethal effects of asbestos. In these factories, the prevalence of asbestosis varies between 3 per cent and 5 per cent. Worse, India continues to import asbestos to be used in cement roofing sheets, cement piping, friction materials, textiles, insulation and even railways and armed forces. Moreover, asbestos products carry no health warning labels and trade unions have no mandate to prevent asbestos-related disease at workplaces. In fact, asbestos related-diseases are never diagnosed but simply labelled as tuberculosis or bronchitis. As long as the state governments and Union Territories have no mechanism to prove that lung cancer deaths and other severe conditions are being caused by asbestos exposure, the Indian asbestos industry could not care less about global efforts to completely eliminate this deadly material.

Trials continue
Russia remains the world’s largest producer of asbestos. The major mines are situated in Asbest, a city located on the eastern slopes of the Ural Mountains, once known as the "dying city" due to its high rate of lung cancer and other asbestos-related conditions. Russia provides most of the asbestos to the world market, including for the US.

Ironically, its use is legal in the US. "By allowing asbestos to remain legal, the Trump administration would be responsible for the flood of asbestos imports from Russia and other countries into the US, as well as the wave of illnesses and deaths that will continue for years to come," says Linda Reinstein, CEO and Co-Founder of the Asbestos Disease Awareness Organization, a non-profit based in California, USA. The legal claims for injuries from asbestos exposure in the US involve more plaintiffs, more defendants and higher costs than any other type of personal injury litigation. By the beginning of 2001, about 6,00,000 individuals had filed lawsuits against more than 6,000 defendants. The total amount that defendants and insurers have spent on resolving claims, including legal costs, is estimated to be $54 billion. The victims say they suffer from lung problems caused by repeated exposure to asbestos on their jobs.

The cases with the greatest potential liability involve mesothelioma and lung cancer. How much money can be awarded in a lawsuit depends on many factors, such as the medical evidence that confirms the diagnosis, the degree of injury, the actual and potential losses, and the financial resources of the company liable for the asbestos exposure.

Since the 1980s and continuing through the present, a number of companies who were defendants in asbestos litigation quickly sought to limit their losses by filing for bankruptcy protection. Specifically, this is a legal process which allows a company to re-organise in a bankruptcy proceeding, put money aside for present and future asbestos liabilities, and, then exit bankruptcy and continue to do business. For instance, Johns-Manville declared bankruptcy decades ago and set up a bankruptcy trust to pay victims of asbestos-related diseases. Soon the company exited bankruptcy and continued to operate as a business with products that can be seen in building supply stores across the country.

About ther auther Gregory A Cade is the principal attorney at US-based Environmental Litigation Group, PC, a law firm focused on asbestos exposure cases, toxic exposure cases and environmental cases)

(This article was first published in Down To Earth’s print edition dated April 1-15, 2019)

Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Concrete

ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown

Published

on

By

Shares

ABB reconditions 25 drives at ACC’s Jamul cement plant, avoiding 16 tonnes of CO₂ emissions while improving reliability through predictive maintenance.
Chhattisgarh

ABB has signed a multi-year Motion OneCare service agreement with ACC Limited, part of the Adani Group, to modernise ageing industrial drives at its Jamul cement plant in Chhattisgarh, improving operational reliability while avoiding approximately 16 tonnes of carbon dioxide (CO₂) emissions without disrupting production.

Announced on 27 October 2026, the agreement combines scheduled drive reconditioning, digital condition monitoring and energy appraisals to extend equipment lifespan, improve plant uptime and optimise maintenance costs. The initiative marks a shift from conventional equipment replacement towards a more resource-efficient approach to industrial asset management.

The first phase, completed in April 2026, involved the on-site reconditioning of 25 ABB ACS800 variable speed drives without a major plant shutdown. By retaining the existing cabinets and restoring the drive modules rather than replacing entire panels, ABB helped ACC preserve capital investment, minimise material consumption and avoid approximately 16 tonnes of CO₂ emissions.

A second phase, covering an additional 25 ACS800 drive modules, is scheduled for the fourth quarter of 2026. The programme is designed to improve long-term equipment reliability while allowing maintenance activities to be aligned with the plant’s operational schedules.

The ACS800 drives, installed at Jamul in 2010, had delivered more than a decade of near-continuous service in demanding cement manufacturing conditions. However, ageing electrical components and changing fault patterns had begun to affect their ability to meet the plant’s reliability requirements.

Rather than opting for complete equipment replacement, ACC engaged ABB’s certified engineers to conduct a comprehensive asset health assessment. The evaluation found that the existing cabinets and enclosures remained structurally sound, making targeted reconditioning a technically viable and cost-effective alternative to full replacement.

Drawing on nearly two decades of experience with ACC’s equipment and operating requirements, ABB developed a maintenance framework tailored to the plant’s shutdown windows, budget cycles and production priorities.

The Motion OneCare agreement incorporates planned equipment restoration, condition-based monitoring and energy assessments, enabling ACC to adopt a more systematic approach to maintaining critical electrical infrastructure.

As part of the programme, ACC has implemented ABB Ability™ Digital Powertrain Insights to monitor drive performance and identify emerging operational issues before they result in equipment failures.

The digital platform provides continuous visibility into parameters such as temperature, current, vibration and fault patterns. These insights allow maintenance teams to detect early signs of equipment deterioration, schedule interventions more effectively and reduce the likelihood of unexpected downtime.

Amit Gupta, Local Division Manager, Motion Services, ABB India, said: “We know what unchecked wear costs over time: a small inefficiency that eats away at ROI for years. At Jamul, the evidence pointed clearly to assets with productive life still in them.”

“Our job was to restore them properly and give the team the tools to stay ahead of the next problem. At ABB, we don’t just fix what fails. We want to protect what works.”

The initiative also demonstrates the growing relevance of circular economy principles in cement manufacturing, where extending the service life of existing industrial equipment can reduce capital expenditure, material consumption and the environmental impact associated with manufacturing replacement components.

According to ABB, drive reconditioning can reduce lifecycle emissions by 50 to 80 per cent compared with complete equipment replacement. By preserving functional components and restoring critical modules, the process helps retain the economic and material value of existing industrial assets.

The addition of energy appraisals in subsequent phases will further expand the programme beyond equipment restoration, enabling ACC to assess drive performance, identify energy-saving opportunities and improve operating efficiency.

For cement manufacturers, variable speed drives play an important role in controlling motors and optimising energy consumption across production processes. Maintaining their reliability and efficiency is essential for minimising operational disruptions and managing electricity costs.

Vinod Bahety, CEO – Cement Business, Adani Group, said: “Moving from reactive firefighting to a structured maintenance plan was exactly what this operation needed. That kind of peace of mind doesn’t come easily. It comes from a partner that understands how your business runs.”

“We didn’t need a full system overhaul; we needed expert support, actionable insights, and a plan we could execute around our schedule. That’s what we got.”

The project supports ACC’s broader strategy to improve manufacturing efficiency through digital transformation, preventive maintenance and sustainable asset management.

ACC, a subsidiary of Ambuja Cements and part of the Adani Group, operates 20 cement manufacturing facilities and 119 ready-mix concrete plants across India. The company has been advancing initiatives focused on renewable energy, circular economy practices and technology-driven operational improvements.

Alongside Ambuja Cements, ACC is part of a large-scale building materials business committed to achieving net-zero emissions by 2050, with near-term and net-zero targets validated by the Science Based Targets initiative (SBTi).

The Jamul initiative aligns with these sustainability objectives by demonstrating how equipment life extension and digital monitoring can contribute to resource efficiency without requiring large-scale replacement of existing infrastructure.

ABB, a global technology company specialising in electrification and automation, brings more than 140 years of industrial expertise and employs approximately 110,000 people worldwide. Its Motion Services business supports industrial customers through equipment maintenance, modernisation, digital monitoring and lifecycle management solutions.

The agreement also reflects a wider shift in industrial maintenance practices, with manufacturers increasingly adopting predictive technologies to improve equipment availability, manage costs and reduce unplanned shutdowns.

With 25 drives already reconditioned and another 25 scheduled for restoration, ABB’s collaboration with ACC illustrates how targeted modernisation, digital monitoring and circular maintenance practices can extend the operational life of critical equipment while supporting more efficient and sustainable cement production.


Continue Reading

Concrete

ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K

Published

on

By

Shares

ABB deploys advanced process control at TCI MAX’s Srinagar cement plant to improve clinker quality, energy efficiency and sustainable manufacturing.

Kashmir 

ABB has deployed its advanced process control technology at TCI MAX Cement’s Srinagar facility in Jammu and Kashmir, marking the region’s first reported implementation of advanced process control (APC) in cement manufacturing and strengthening efforts towards more efficient, digitally enabled production.

Announced on 5 November 2026, the deployment of ABB Ability™ Expert Optimizer at the facility, operated by Trumboo Industries Pvt. Ltd., aims to improve process stability, clinker quality, energy efficiency and overall plant productivity. The implementation forms part of TCI MAX’s strategy to modernise its manufacturing operations through automation and digital technologies.

Following the integration of ABB’s advanced process control solution and supporting IT infrastructure, TCI MAX has reported improvements in operational productivity, product quality and sustainability-related performance indicators. The technology focuses on optimising the cement pyro process, a critical stage of production involving high-temperature processing and clinker formation.

Waseem Ahmed Trumboo, Director, Trumboo Industries Pvt. Ltd., said: “Introducing advanced process control at TCI MAX is an important step in how we are evolving our operations. Our focus is on improving the stability and efficiency of our processes while maintaining consistent clinker quality. We have been encouraged by the performance of the solution during commissioning and by the support from the ABB team, and we look forward to realizing its full potential.”

ABB Ability™ Expert Optimizer combines advanced process control, model predictive control (MPC) and artificial intelligence (AI) to continuously monitor and optimise manufacturing operations. By analysing process conditions, predicting operational behaviour and automatically adjusting key parameters, the system enables more consistent production while reducing process variability.

In cement manufacturing, maintaining stable pyro-processing conditions is essential for achieving uniform clinker quality and optimising thermal energy consumption. Fluctuations in operating parameters can affect fuel efficiency, production output and product consistency.

The deployment is designed to address these challenges through real-time process optimisation, helping operators maintain more stable kiln operations while improving the utilisation of fuel, electricity and raw materials.

Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries Division, ABB India, said: “Cement producers are increasingly looking to adopt digital technologies to achieve greater consistency and efficiency while addressing their sustainability priorities. ABB Ability™ Expert Optimizer brings advanced process control and deep cement process expertise together to help operators make their processes more stable and efficient. We are pleased to support TCI MAX as it takes this important step in its digital transformation.”

The technology also supports sustainability objectives by optimising fuel consumption, improving electrical energy efficiency and minimising process waste. More stable operations can contribute to lower energy intensity and reduced emissions associated with cement production.

For TCI MAX, the investment represents a move towards data-driven manufacturing, where automated control systems complement operator expertise to improve production performance and operational reliability.

The implementation is particularly significant for Jammu and Kashmir’s cement industry, as it introduces advanced process optimisation technology to a regional manufacturing facility. Its deployment could demonstrate the potential for wider adoption of digital automation across cement plants seeking to modernise their operations.

The project builds on ABB’s experience in delivering advanced process control solutions to cement manufacturers worldwide. Through the integration of industrial automation, predictive technologies and process engineering expertise, the company supports manufacturers in improving resource efficiency and maintaining consistent production quality.

As cement producers face increasing pressure to manage energy costs, improve productivity and reduce their environmental footprint, technologies such as AI-enabled process control and predictive optimisation are becoming important components of plant modernisation strategies.

ABB’s Expert Optimizer provides a platform for addressing these priorities by enabling automated adjustments based on changing process conditions, reducing reliance on manual intervention and supporting more efficient plant operation.

ABB, a global technology company specialising in electrification and automation, has more than 140 years of industrial experience and approximately 110,000 employees worldwide. Its Automation business employs around 26,000 people and provides technologies and services across process, hybrid and maritime industries.

The TCI MAX deployment reinforces ABB’s growing role in the digital transformation of cement manufacturing in India, where improving process efficiency and reducing energy consumption remain critical to the industry’s long-term sustainability.

With the advanced process control system now implemented at its Srinagar facility, TCI MAX aims to build on the initial operational improvements and further optimise production efficiency, clinker consistency and environmental performance.

Continue Reading

Concrete

Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’

Published

on

By

Shares

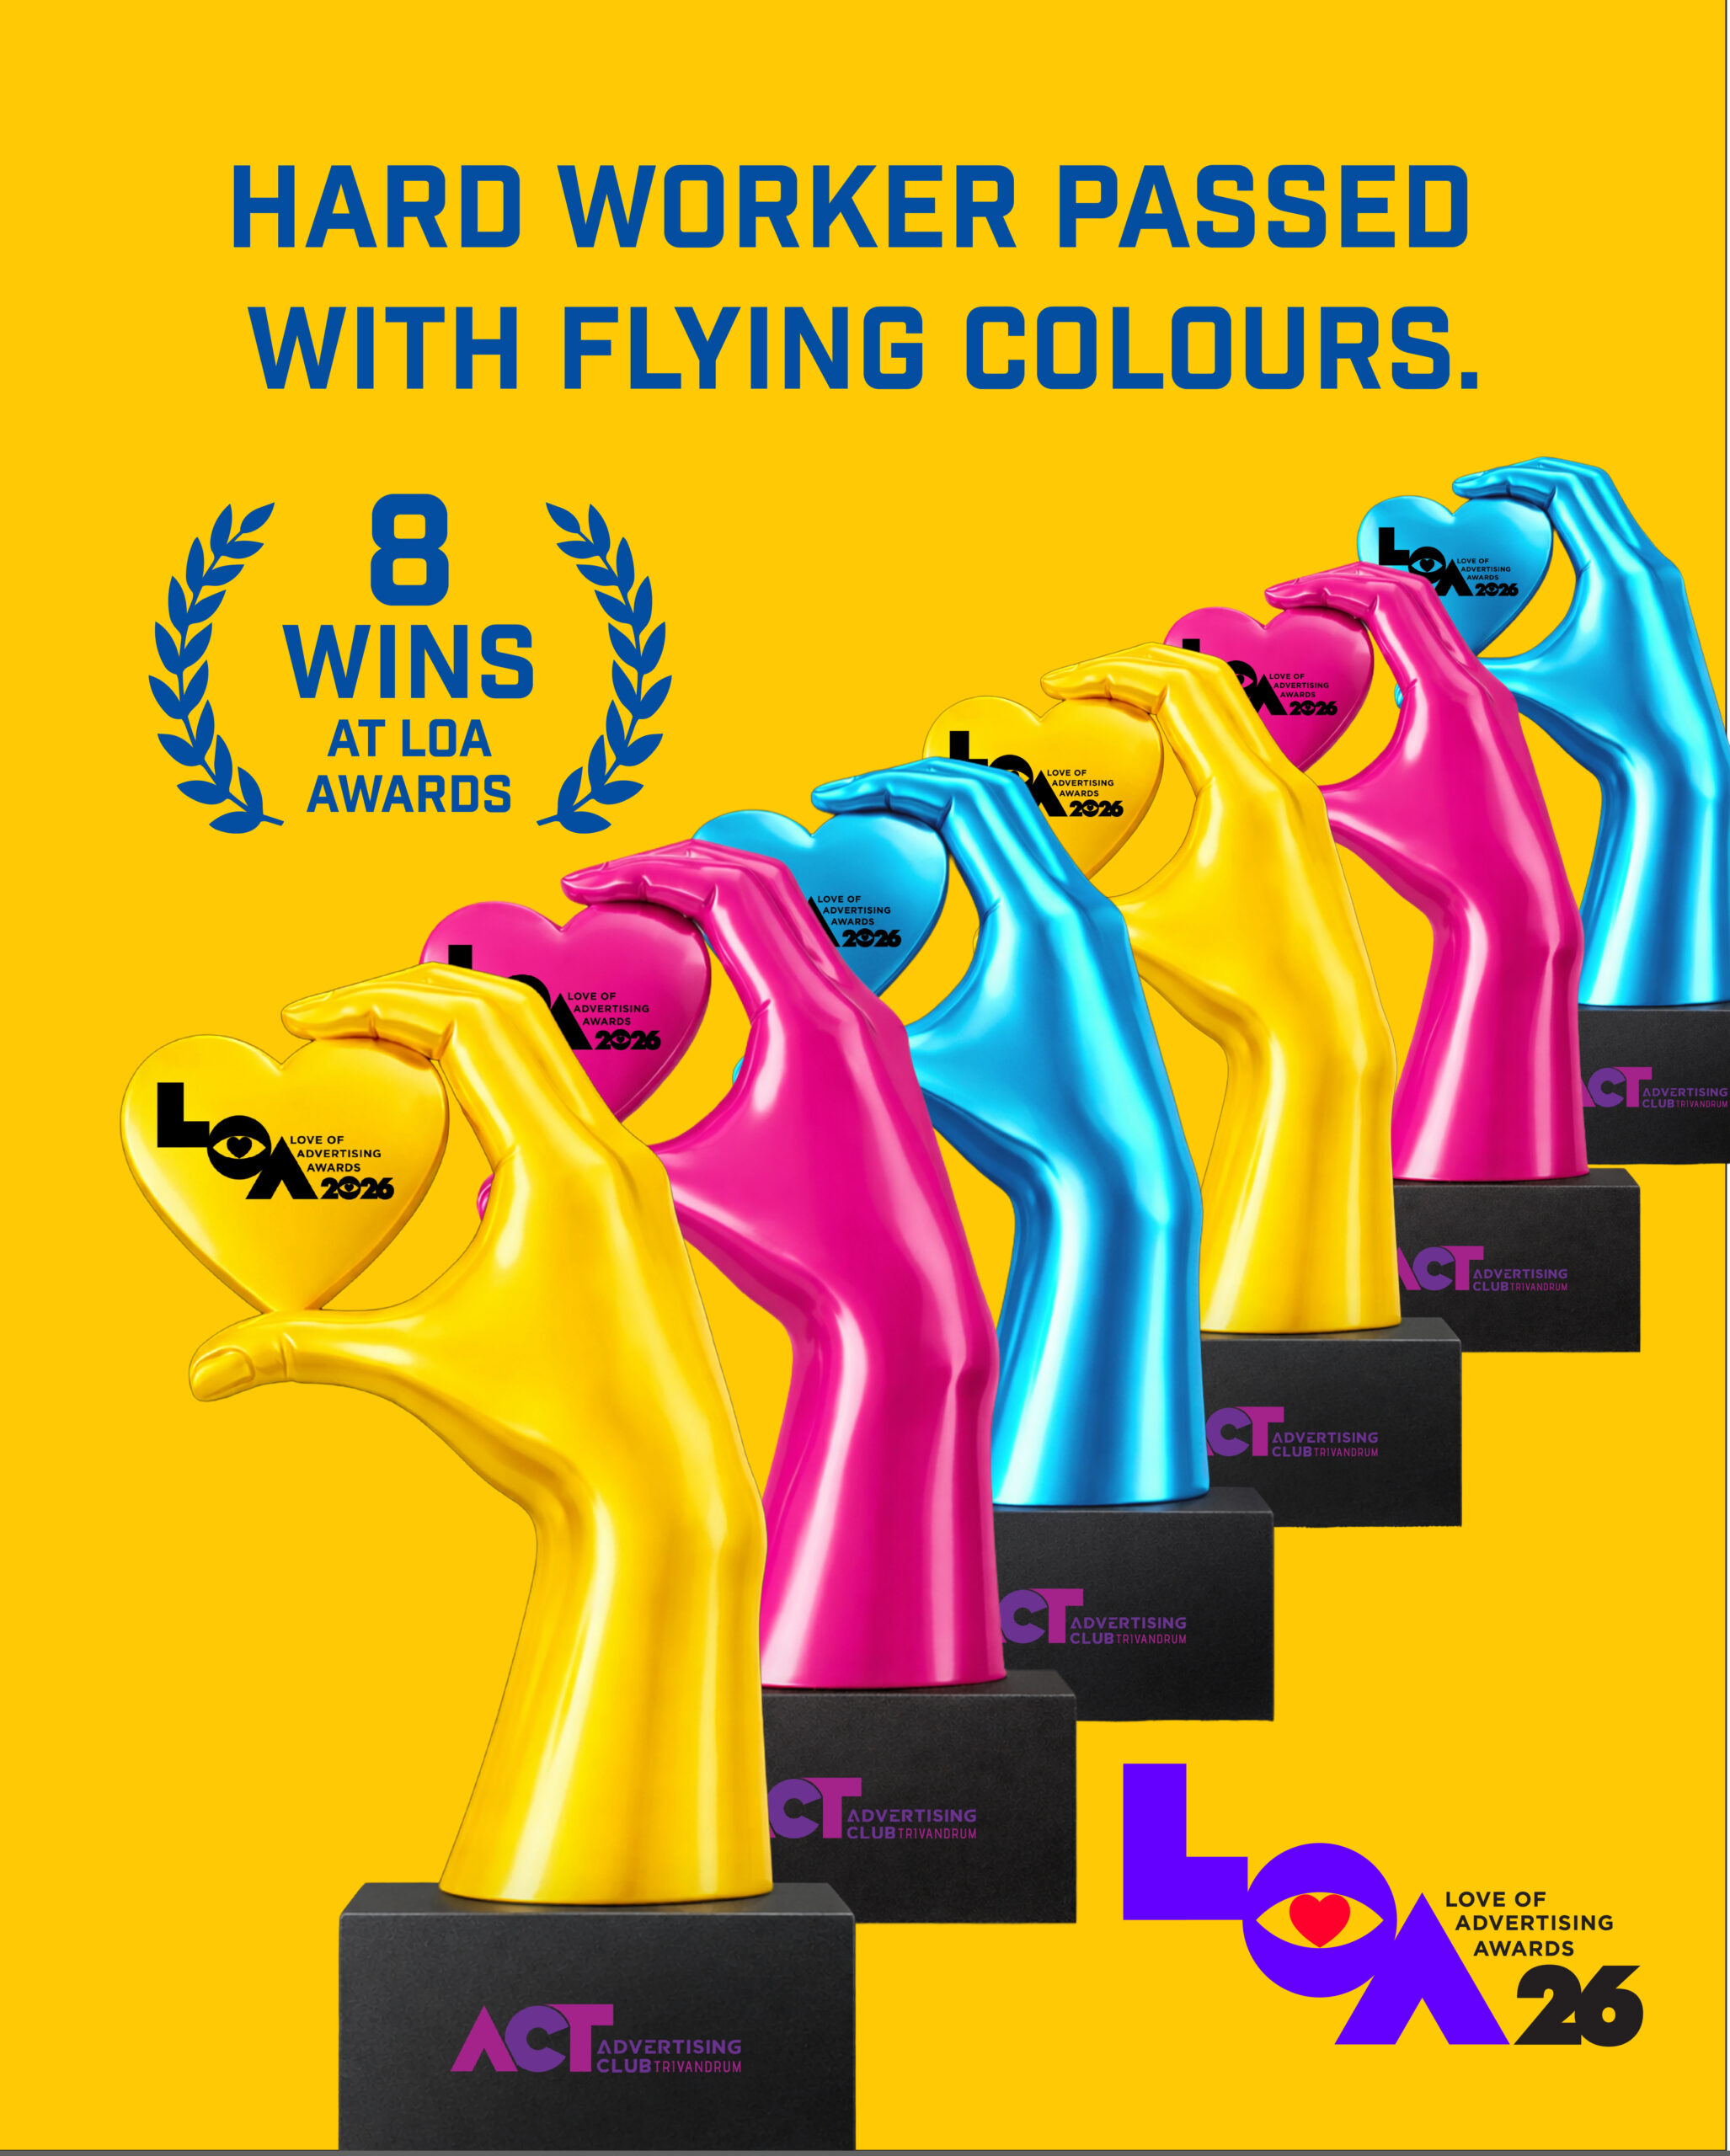
Ramco Cements’ Hard Worker brand wins eight awards for excellence in advertising, packaging and brand identity at the Love of Advertising Awards 2026.

Hyderabad 

The Ramco Cements Limited’s construction chemicals brand, Hard Worker, has secured eight awards at the Love of Advertising Awards 2026, recognising its creative excellence across television, digital advertising, packaging design and brand identity.

Organised by the Advertising Club of Trivandrum, the awards were presented at a ceremony held at The Leela Raviz, Kovalam, on 24 October 2026. The recognition highlights Hard Worker’s integrated marketing strategy and its efforts to establish a distinctive presence in India’s competitive construction chemicals market.

The eight awards span multiple creative categories, reflecting the brand’s approach to combining product-focused communication with engaging storytelling, humour and innovative design. Through its campaigns, Hard Worker has sought to simplify technical product benefits and make construction chemicals more accessible and relatable to consumers and construction professionals.

Built around the philosophy of “Hard-working products for hardworking people”, the brand focuses on communicating practical product advantages through memorable advertising narratives while maintaining a consistent identity across different marketing platforms.

Its campaigns for Ramco Hard Worker Eco Plaster and Tile Fix have been central to this approach. The Eco Plaster campaign highlights water conservation through the product’s self-curing properties, positioning it as a solution that supports more efficient construction practices. Meanwhile, Tile Fix promotes specialised tile-fixing solutions by presenting their practical benefits through relatable situations and creative storytelling.

Beyond advertising, Hard Worker has invested in distinctive packaging and brand identity development to improve product recognition and maintain consistency across customer touchpoints. This integrated approach has helped the brand differentiate itself in a category where marketing communication has traditionally focused on technical specifications and functional performance.

A V Dharmakrishnan, CEO, Ramco Cements, said, “Winning eight awards at the Love of Advertising Awards is a proud moment for Ramco Cements and the Hard Worker team. We believe that building a strong brand requires not only quality products but also the ability to communicate their value in a compelling and differentiated manner. Hard Worker’s journey reflects our commitment to combining product performance with innovative marketing to create meaningful connections with our customers and strengthen our presence in the construction chemicals market.”

The recognition comes as building materials manufacturers increasingly focus on brand differentiation, product awareness and customer engagement to strengthen their position in the construction chemicals segment.

By using humour and storytelling to explain product applications and benefits, Hard Worker aims to bridge the communication gap between technical construction solutions and the practical requirements of contractors, applicators and end-users.

Balaji K. Moorthy, Executive Director – Marketing, Ramco Cements, said, “Hard Worker was conceived to bring a fresh perspective to the construction chemicals category, where product communication has traditionally been functional and technical. Our endeavour has been to break through the clutter with distinctive ideas, humour and storytelling, while keeping the product proposition at the heart of every campaign. The recognition across TV and digital advertising, packaging design and brand identity design demonstrates our integrated approach to building the brand. These eight awards are an encouraging recognition of the creative thinking and collaborative effort behind Hard Worker’s marketing initiatives.”

The awards add to Hard Worker’s growing portfolio of creative recognitions and reinforce Ramco Cements’ emphasis on integrating product innovation with strategic marketing.

The brand’s communication initiatives also reflect a wider shift in the construction materials industry, where manufacturers are increasingly adopting consumer-focused marketing strategies to improve product understanding and strengthen relationships with construction professionals.

With its portfolio of construction chemicals, Hard Worker aims to address evolving requirements for durability, application efficiency and construction quality. Its marketing efforts seek to complement these product attributes by building stronger awareness and encouraging the adoption of specialised construction solutions.

Ramco Cements, one of India’s established cement manufacturers, operates across cement and allied building solutions. Through Hard Worker, the company is expanding its presence in the construction chemicals segment with products designed to enhance performance, quality and durability in modern construction applications.

The latest recognition strengthens Hard Worker’s brand visibility and underscores the growing importance of creative communication in promoting technical building materials. Ramco Cements intends to continue combining product development with distinctive marketing initiatives to support the brand’s growth in India’s construction chemicals market.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News