

Concrete
Ready Mix Concrete: A Better Choice

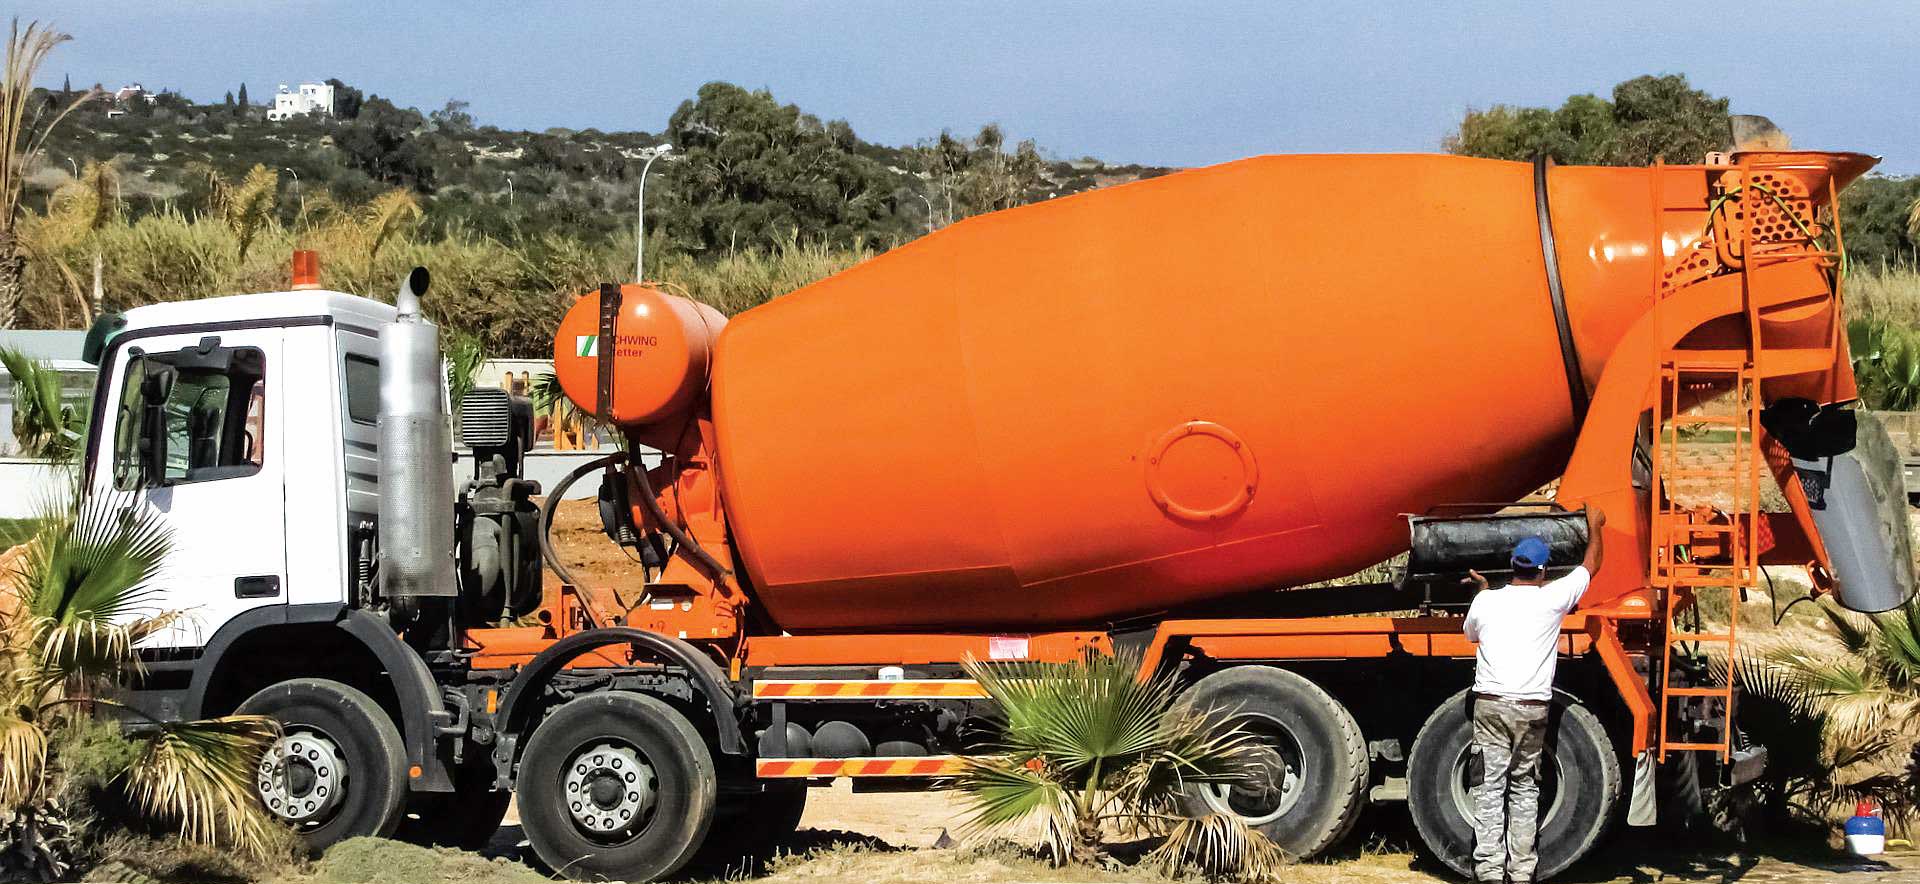
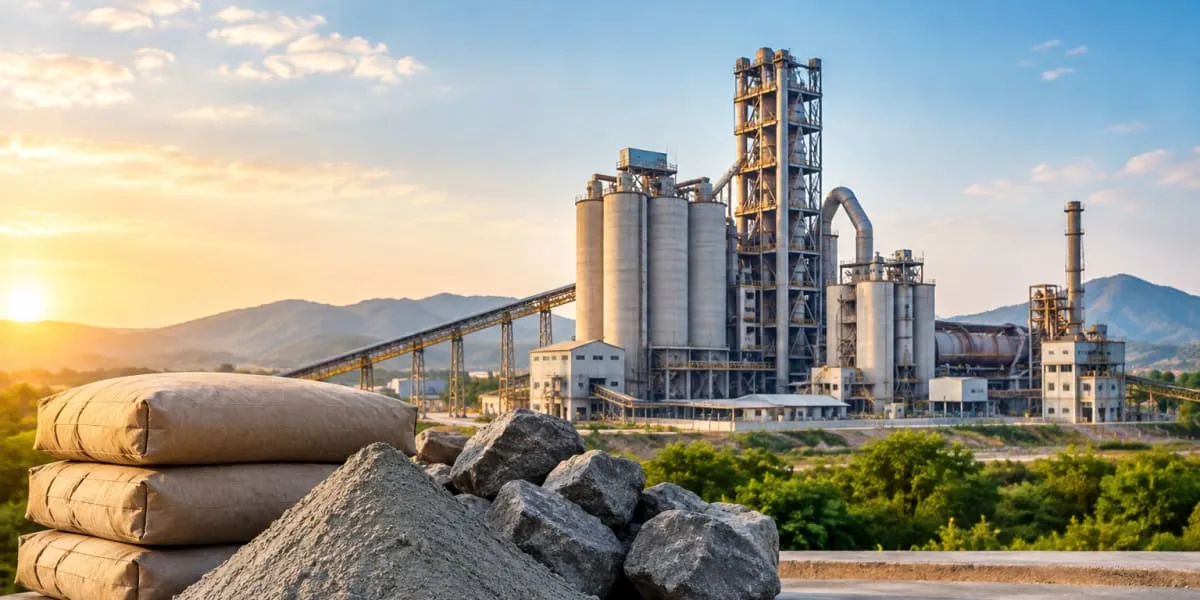
Its multiple benefits and cost effectiveness has given Ready Mix Concrete a preferred choice status in the construction industry. ICR attempts to understand its manufacturing processes and distinct features to evaluate its long-lasting impact on the industry.
The construction industry uses two main types of concrete – the ready mix concrete and site mixed concrete. They both have specific applications, functions, advantages and is advantages.
The ready mix concrete (RMC) is usually made in a factory or a batching plant and is delivered in an unhardened and plastic state, ready to use, to the construction site. It is the most preferred mix of concrete for large projects that require a high volume or when less space is available for storing and mixing the construction materials. It is also often preferred over on-site concrete mixes because the ready mix variety can be mixed using specialised equipment to get just the right mixture. It is like using a set recipe and delivering it to the site by trucks with in-transit mixers.
The story of the genesis of ready mix concrete – when it was first delivered or first made – is disputed. Some sources say that concrete was delivered by a horse-drawn mixer that used paddles turned by the cart›s wheels to mix concrete en route to the jobsite in 1909, while others suggest it was first made in 1913 in Baltimore and by 1929 there were over 100 plants operating in the United States. In 1916, Stephen Stepanian of Columbus, Ohio, developed a self-discharging motorised transit mixer that was the predecessor of the modern ready-mixed concrete truck. Development of improved ready-mixed trucks was hindered by the poor quality of motor trucks in the 1920s. During the 1940s, the availability of heavier trucks and better engines allowed mixing drum capacities to increase, which in turn allowed ready-mixed concrete producers to meet the high demand for concrete caused by World War II.
The Chemical Makeup
Cement is the core component of any ready mix concrete. It is then combined with water and other aggregates to make a ready to use mixture at construction sites. Water sets off a chemical reaction when it comes in contact with the cement. Aggregates, such as sand, gravel and crushed stones that are obtained from quarries or other sources, add 60 to 70 per cent volume to this mixture. Some solid or liquid additives, like retarders, are also introduced to ready mix concrete before or during preparation to increase its durability and shorten its setting time, giving allowance to the transportation and placing the time of the concrete.
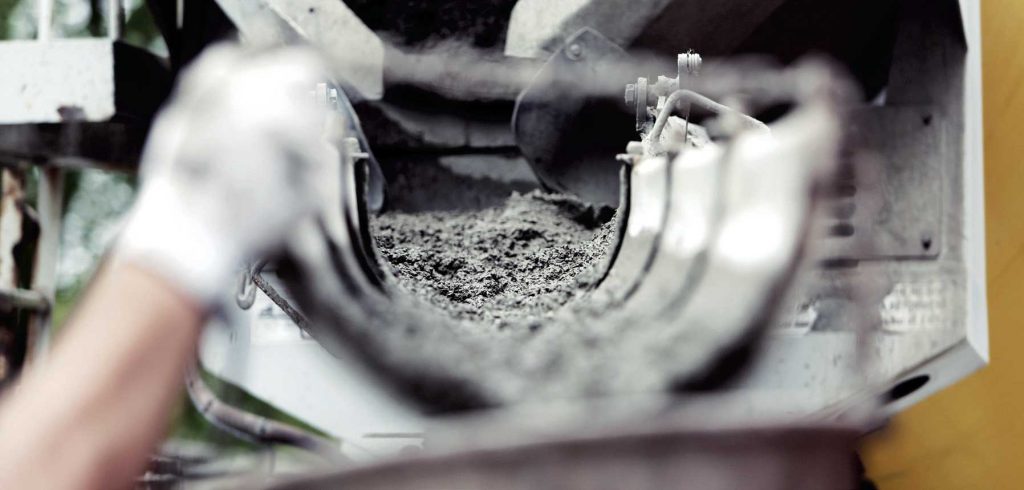
Each component of the ready mix concrete is manufactured separately. The proportions in which it is mixed are dictated by the requirement of its properties or the job that it is going to be used at. These components of the RMC are brought together in a rotating container, also known as the cement mixer and water is added to it. The proportions and measurements are carefully considered along with the time it will take to mix and travel to its destination. Once water hits the mixture, the cement mixer doesn’t stop rotating, even during the travel and rotates at approximately the speed of two to six rotations per minute.
Variety and Uses
There are mainly three types of ready mix concrete that are developed: Transit Mixed Concrete, Shrink Mixed Concrete and Central Mixed Concrete.
The Transit Mixed Concrete, also known as truck mixed concrete, has its materials batched at a central plant and are completely mixed in the truck in transit. Frequently, the concrete is partially mixed in transit and mixing is completed at the jobsite. Transit-mixing keeps the water separate from the cement and aggregates and allows the concrete to be mixed immediately before placement at the construction site. It is the most common type of ready-mix concrete used by building construction providers.
In Shrink Mixed Concrete, concrete is partially mixed at the plant to reduce or shrink the volume of the mixture and mixing is completed in transit or at the jobsite. The ingredients are added to the batching plants, and the required adjustments are made according to the strength requirements of the concrete. The ready-made concrete is then shifted through concrete pumps for transportation. The main purpose of this concrete is to increase the load capacity of the transporting vehicle. The balance mixing of the concrete is done during the transit time.
In this technique of the central mixed concrete, a stationary mixing unit is set and the concrete is mixed. It is followed by quality tests and is allowed to transport only after the tests are done and quality standards are met. It is also known as wet batch plants. However, the process is time-consuming and not always recommended.
RMC – Getting an Upper Hand
There are multiple advantages and disadvantages associated with the use of ready mix concrete.
The biggest advantage of using the same is the control on quality and ease of operations. RMC is mixed under quality controlled batch units, thus, the result and strength is assured and as per requirement. Another advantage is that it comes in a mobile mixture, so there is no need to store it at the construction site, thus reducing the handling and storing cost of the same. As the name suggests, ready mix concrete is a ready material to be used at construction sites and therefore, it accounts for reduced time of construction and accounts for no delays in completion of projects.
The quantities in ready mix concrete can be controlled and only that much can be ordered as much is required, which leads to reduced or no wastage. This is economically beneficial to the constructor as well as makes the same an environmentally friendly option.
Anil Bacchore, Managing Director, RDC, says, “Use of ready mix concrete at a construction site is cost efficient and has several advantages, making it a more viable and efficient alternative to site-mix concrete. It circumvents the messy and long-drawn task of producing the concrete on site. The consumption of required materials for making the concrete reduces by nearly 10 per cent to 12 per cent with better handling practices and proper mixing. RMC helps save on capital investments by not having to invest in plants and machinery for cement. The need to create storage facilities at the site of construction also reduces with ready mix concrete.”
“Faster pouring of concrete leads to less requirement of construction labours and makes the construction activity faster. Thus, RMC provides an alternative that reduces wastage of resources during the construction process. Furthermore, the responsibility of producing fresh concrete, its transportation, pumping and laying of concrete on the site lies with the RMC Players and their goal is to provide materials of the best quality with timely delivery, regardless of the size of the order,” he adds.
Precautionary measures
Some of the notable disadvantages of using ready mix concrete is that it requires an initial investment by the constructing party to order the required quantity of mix. Since the material is time sensitive, the readiness of the workforce becomes very important and labour at site must be ready to bring the material to use within its setting time.
The transport requirement of the same is also very specific. Special transport vehicles are required to bring ready mix concrete from batching plants to the site, which is again a monetary investment, and since the concrete is made ready to use at the plant, it becomes time sensitive to reach the site. Ready mix concrete must reach the site within 210 minutes from the batching plant. Any unforeseen delays or vehicle breakdowns can result in the onset of its setting and thus, resulting in wasted material and resources.

Fresh concrete has many applications and can be cast into circles, rectangles, squares and more. It can also be used for staircases, columns, doors, beams, lentils and other familiar structures. Concrete is made in different grades, including normal, standard and high-strength grades. These grades indicate how strong the concrete is and how it will be used in construction.
Raj Kamal Yadav, General Manager – Operations Strategy, Lodha Group, says, “The most widely used ready mix concrete in the industry is M30 and many of the experts shall agree to the same. M30 has proven to be a good design mix for low rise residential buildings and structures where the beams are of shorter span. M30 has also a wider usage in vertical members of a RCC structure. The choice of mix, however, changes depending upon the load on buildings. When we look at high-rise buildings, ready mix concrete grades like M40 and M50 are used in vertical and in many cases horizontal members as well. However, M30 becomes an obvious choice for structural members especially horizontal ones at higher levels of the building as loads on structure come down”.
“The choice of mix highly depends on the load (dead load or live load or wind load or earthquake), where the mix being used (foundation or columns or beams or slabs), methodology of construction and type of structure (framed or modular or precast or prestressed), other category of structure (bridge, dam, residential building, road, rail etc.) exposure of structure (windy, high moisture, marine), type of reinforcement and various other conditions. Having said that, M30 has a wide usage” he adds.
Manufactured Sand (M Sand)
Concrete is made with cement, water and aggregates. One of the most important aggregates is sand. However, owing to the shortage of naturally available sand, manufactured sand or M Sand is becoming a sustainable alternative for construction purposes as an aggregate for concrete.
Manufactured sand (M Sand) is artificial sand produced from crushing hard stones into small sand-sized angular shaped particles, washed and finely graded to be used as construction aggregate. An alternative to the naturally occurring river sand that is used in construction, manufactured sand is produced from crushing rocks, quarry stones, hard granite or larger aggregated pieces into sand-sized particles.
Sand is the world’s second most consumed natural resource after water. As urbanisation and infrastructure is rapidly growing, the demand for sand is also growing. This increasing need for sand as an aggregate for construction material is leading to an eventual exhaustion of natural sand resources. This also raises environmental concerns and thus, manufactured sand has emerged as a suitable and sustainable alternative to fine aggregate for the concrete mix.
The manufacturing process of M Sand involves crushing of stones or rocks of various sizes into aggregates using vertical shaft impact (VSI) crushers. This material is then fed into a Rotopactor for crushing the aggregates into sand to the desired grain size. This sand is then screened and further refined by removing fine particles and impurities through sieving
and washing.
Manufacturing Process
The production of manufactured sand is driven by the following factors advantages:
- Scarcity of natural sand is one of the key driving factors of manufactured sand production. Continuous mining of sand from river beds has led to its depletion and the need to have an alternative resource has become prominent.
- The aggregate particle size can be determined when the sand is artificially manufactured. Concrete creates its bulk with sand and other aggregates. They also determine certain properties which can be managed with manufactured sand.
- Natural sand pits that are licensed with the desired quality of sand may be located away from the site, which implies the cost of transport, various permissions and taxes. While manufactured sand solves this problem and becomes a cost effective solution, thus, the demand.
- Manufactured sand is a man-made aggregate that can be ordered as per required quantity. It is a processed material, free of impurities that allows concrete makers to reduce wastage as compared to that of natural sand.
- The use of manufactured sand in concrete making makes the batching process more efficient and productive as it is a quality controlled material, free of impurities.
While there are many advantages and drivers of manufactured sand, there are some disadvantages, too:
- M Sand is a coarser material and more angular than natural sand. Grains of natural sand are fine, almost spherical, that make it smooth due to natural gradation. The angular particles of M sand may lead to a higher water requirement to achieve its workability, which may add to some costs.
- At times, M Sand can contain larger amounts of micro fine particles as compared to that of natural sand. This also impacts the workability and strength of concrete.
- Manufactured sand is used for concreting,
- plastering and for brick or blockwork. It comes with its advantages and disadvantages but it has been proved to have economical and eco-friendly benefits for the concrete makers and construction activities. Ready mix concrete is a vital material in construction activities and is the preferred choice in the industry for multiple benefits and cost effectiveness it offers.
–Kanika Mathur










CII Calls for Greater Alternative Fuel Use in Cement Industry

Sameera Group Enters Industrial and Logistics Real Estate

UltraTech Cement Expands in Andhra Pradesh with Rs. 26.5 bn

Nuvoco reports 13.5% revenue growth in Q2 FY27

Meghalaya Cabinet Approves MCCL Closure, Writes Off Rs. 244.3 mn
CII Calls for Greater Alternative Fuel Use in Cement Industry
Sameera Group Enters Industrial and Logistics Real Estate
UltraTech Cement Expands in Andhra Pradesh with Rs. 26.5 bn
Nuvoco reports 13.5% revenue growth in Q2 FY27
Meghalaya Cabinet Approves MCCL Closure, Writes Off Rs. 244.3 mn
-

 Concrete4 weeks ago
Andhra Pradesh Clears Rs. 30 bn My Home Cement Plant
-

 Concrete4 weeks ago
Cement Prices Rise Rs. 7 per Bag in September; October Hikes Expected
-
 Concrete1 month ago
UltraTech Cement achieves 100% green energy milestone at Chhattisgarh plant
-
 Concrete1 month ago
Nuvoco Vistas, CleanMax Partner for Wind-Solar Hybrid Project in Rajasthan