ICR explores how India’s cement industry is redefining emission control through advanced filtration, digital process optimisation, and low-carbon innovation.
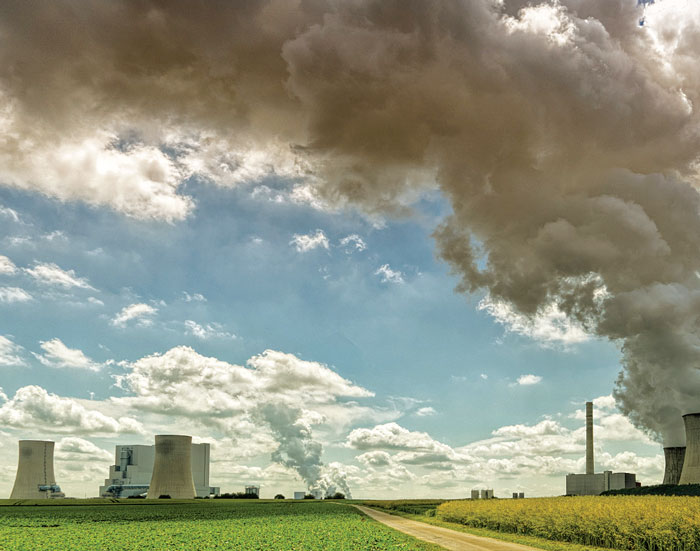
Cement plants emit four key pollutants—CO2, NOx, SOx, and particulate matter (PM)—each arising from different stages of production. Most CO2 stems from limestone calcination and kiln fuel combustion, and while the sector’s CO2 intensity has remained flat, it must decline by ~4 per cent annually by 2030 to align with net-zero goals, as mentioned in or a report by the IEA. In kilns, thermal NOx dominates due to high flame temperatures (~1,200°C), SO2 originates from sulphur in fuel and raw materials, and PM is released from raw mill handling and clinker grinding—as mentioned in or a report by the EEA Guidebook (2023). At the global level, cement accounts for 6 per cent to 8 per cent of total CO2 emissions, highlighting the need for integrated emission strategies, as mentioned in or a report by the GCCA. India’s installed capacity grew from ~510 MTPA (2019) to ~632 MTPA (2024), reflecting ~4.4 per cent CAGR, as mentioned in or a report by JMK Research (2024). National GHG emissions reached ~4.13 GtCO2e in 2024, with cement responsible for 6 per cent to 7 per cent, largely concentrated among top producers, as mentioned in or a report by CARE Edge ESG (2025).
India’s cement roadmap targets net-zero CO2 by 2070, with milestones tied to efficiency, alternative fuels, SCMs, and carbon capture, as mentioned in or a report by TERI (2025). Policy frameworks are evolving accordingly: Continuous Emission Monitoring Systems (CEMS) for PM, SO2, and NOx are mandated to strengthen compliance and transparency, as mentioned in or a report by the CPCB. Globally, the IEA’s Breakthrough Agenda Report (2025) emphasises that achieving real decarbonisation requires parallel progress in process control, AFR, SCMs, and CCS, since total CO2 emissions remain above 2015 levels and intensity gains have plateaued. For India, the path forward lies in combining strict regulatory oversight with accelerated technology adoption—ensuring each tonne of clinker produced moves closer to compliance, efficiency, and long-term net-zero alignment.
Modern filtration systems: The first line of defence
Cement plants are swiftly moving beyond legacy electrostatic precipitators (ESPs) to high-efficiency baghouses, hybrids, and smart filter media that achieve ultra-low particulate emissions with tighter control. India’s regulatory drive has been crucial—CPCB’s 30 mg/Nm3 PM limit (also enforced by Delhi DPCC) has accelerated retrofits and new installations, as mentioned in or a report by CPCB and DPCC. Modern systems often outperform these standards: a Thermax kiln-raw mill project guaranteed =25 mg/Nm3, while an ESP-to-baghouse conversion in Asia cut dust from 40 to 9 mg/Nm3 (—78 per cent), as mentioned in or a report by Thermax and a peer-reviewed study. Indian majors like UltraTech are scaling this approach—converting hybrid filters to pulse-jet baghouses and upgrading cooler ESPs to further reduce PM, as mentioned in or a report by the company’s environmental filings.
Performance gains now hinge on advanced filter media. Plants using ePTFE/PTFE-membrane bags achieve cleaner filtration and drops from ~50 to ~30 mg/Nm³, while maintaining stable pressure loss, as mentioned in or a report by Orient Cement’s compliance report and an ePTFE study. Nanofiber-laminated felts and electrostatically enhanced baghouses promise lower pressure drop, longer bag life, and reduced fan power, as mentioned in or a report by the US EPA baghouse compendium. Vendors like Intensiv-Filter Himenviro now offer baghouses achieving <10 mg/Nm3 under optimal design and maintenance. The trend is clear: pulse-jet baghouses with advanced membranes and selective ESP upgrades are providing India’s cement sector with the compliance flexibility, energy efficiency, and reliability needed to thrive under its tighter emission regime.
Advanced process optimisation
Digitalisation and AI-based process optimisation have emerged as key levers for emission reduction in cement manufacturing, addressing pollutants at their source rather than at the stack. Across global and Indian plants, AI-driven kiln control systems like ABB’s Expert Optimiser and Carbon Re’s AI for Pyroprocess are redefining precision by integrating real-time data from sensors and APC loops to stabilise combustion, optimise fuel use, and limit NOx and CO formation. As mentioned in or a report by ABB (2024), advanced process control has cut fuel consumption by 3 per cent to 5 per cent and CO2 emissions by up to 5 per cent, while as mentioned in or a report by Carbon Re (2024), European plants achieved 4 per cent lower fuel use and 2 per cent CO2 reduction through AI kiln optimisation.
Indian majors like UltraTech, Dalmia, and Shree Cement are piloting such hybrid models combining process, energy, and environmental data for smarter emission management.
Vijay Mishra, Commercial Director, Knauf India says, “India’s construction materials sector is making steady progress toward circularity, moving beyond the earlier focus on “green buildings” to now addressing lifecycle impacts and resource recovery. While global leaders, particularly in Europe, benefit from mature collection and recycling infrastructure for materials like gypsum, metals, and aggregates, India is still in the early stages of building that ecosystem—but the momentum and policy direction are clearly positive. The country’s massive construction pipeline presents a unique opportunity: even modest gains in material reuse and low-carbon manufacturing could yield enormous environmental benefits. The main challenge remains infrastructure—segregation at site level, recovery logistics, and recycling facilities—but as these improve, the economics of circular materials will become more compelling. Looking ahead, the next decade of emission-conscious manufacturing will be shaped by material circularity, manufacturing efficiency, and digital traceability—turning waste into value, cutting emissions at source, and ensuring every sustainable action can be measured and rewarded. For manufacturers, this balance between innovation and responsibility will define the future of India’s low-carbon construction movement.”
The benefits extend beyond combustion. Real-time monitoring and predictive analytics enable operators to anticipate emission spikes and recalibrate process parameters automatically. As mentioned in or a report by the CII–Sohrabji Godrej Green Business Centre (2023), India’s top plants operate below 70 kWh/t cement (electrical) and 690 kcal/kg clinker (thermal)—benchmarks sustained through digital oversight. Digital twins and AI-driven models now simulate NOx reduction and fuel substitution scenarios, cutting trial errors. As mentioned in or a report by the IEA (2025), digitalisation is among the top three global levers for industrial decarbonisation, capable of reducing cement CO2 emissions by up to 8 per cent by 2030. The future of emission control will depend less on end-of-pipe systems and more on intelligent, adaptive process control that keeps every second of kiln operation cleaner, stable, and efficient.
From capture to co-processing
The cement industry’s decarbonisation pathway now rests on two pivotal levers—Carbon Capture, Utilisation and Storage (CCUS) and Alternative Fuels and Raw Materials (AFR)—each addressing a distinct source of emissions. While process emissions from limestone calcination are unavoidable, CCUS provides a route to capture, reuse, or store CO2, whereas AFR mitigates combustion-related emissions by substituting fossil fuels with renewable or waste-derived alternatives. Together, they form the “dual engine” of deep decarbonisation, capable of reducing total CO2 emissions by over 40 per cent in advanced systems, as mentioned in or a report by the Global Cement and Concrete Association (GCCA, 2024). Globally, CCUS is moving from pilots to commercial reality—as mentioned in or a report by Heidelberg Materials (2024), the Brevik CCS plant in Norway will capture 400,000 tonnes of CO2 annually, while Holcim’s GO4ZERO project in Belgium aims for 1.1 million tonnes by 2029, establishing Europe as the proving ground for full-scale capture. As mentioned in or a report by TERI (2025), India is now developing its own CCUS roadmap, with Dalmia Cement and Carbon Clean partnering on a 500,000 tCO2/year project in Tamil Nadu—the country’s first commercial-scale cement CCUS initiative. Meanwhile, as mentioned in or a report by the NITI Aayog–GCCA policy brief (2024), frameworks are being designed for carbon capture finance corporations and shared storage clusters to accelerate deployment.
Raj Bagri, CEO, Kapture says, “Decarbonising cement production is crucial, but while the focus is often on the main kiln, the surrounding infrastructure, including essential diesel generators remains a source of carbon pollution. These generators provide crucial backup or primary power for on-site operations, contributing to a plant’s overall carbon footprint. Kapture addresses this with a cost- effective, easily retrofittable technology that captures CO2 directly from diesel generator exhaust. Kapture’s innovative approach transforms the captured carbon into a stable, solid byproduct. This material then closes the loop by being sequestered in concrete. By serving as a direct replacement for a portion of virgin clinker, Kapture’s. byproduct actively offsets the hard-to-abate process emissions that dominate the cement industry. This circular economy model provides a powerful solution. It immediately cuts combustion emissions from the auxiliary power source and simultaneously reduces the need for high-carbon raw materials in the concrete mix, Kapture offers the cement industry a pathway to both clean up their power and drastically lower the carbon intensity of their end-product.”
Parallel to carbon capture, the rise of AFR is redefining combustion efficiency and circularity across Indian plants. As mentioned in or a report by the CII–Sohrabji Godrej Green Business Centre (2023), India’s Thermal Substitution Rate (TSR) averages 6 per cent to 8 per cent, with leaders such as UltraTech, ACC, and Geocycle already achieving 15 per cent to 20 per cent through co-processing Refuse-Derived Fuel (RDF), biomass, and industrial waste. This transition reduces dependence on coal and petcoke while diverting thousands of tonnes of waste from landfills. The MoEFCC aims to raise TSR to 25 per cent by 2025, in line with India’s Circular Economy Action Plan, and as mentioned in or a report by the IEA (2023), such substitution can cut specific CO2 emissions by 12 per cent to 15 per cent. Although cost, scale, and infrastructure remain challenges, India’s combined progress in CCUS and AFR signals a powerful shift—toward a future where carbon is captured and reused, waste becomes a valuable fuel, and cement production evolves into a truly circular, low-emission system.
Instrumentation, data transparency, and continuous monitoring
Real-time monitoring has become central to emission management in cement manufacturing, replacing periodic sampling with Continuous Emission Monitoring Systems (CEMS) that track PM, SO2, and NOx continuously. As mentioned in or a report by the CPCB (2024), CEMS installation is now mandatory for all integrated plants in India, with live data streaming to regulatory servers for verification. These systems enhance transparency and allow operators to act before emissions exceed limits. Complementing them, IoT-based sensors for baghouse performance and draft fans are cutting downtime by up to 30 per cent, as mentioned in or a report by Frost and Sullivan (2024). Many states now mandate continuous online air-quality reporting, creating a real-time loop between regulators, operators, and technology providers. As mentioned in or a report by the GCCA (2024/25), leading producers are integrating digital emission platforms that combine CEMS data, process sensors, and ESG metrics, building both compliance and investor confidence. Globally, as mentioned in or a report by the IEA (2025), smart sensors and automated reporting can cut non-compliance events by up to 40 per cent while boosting efficiency. For India, scaling such data-driven frameworks will ensure emission control evolves from a reactive measure to a proactive, intelligence-led sustainability system.
Regulatory framework and global benchmarks
India’s cement industry operates under one of the most stringent emission control regimes among developing nations, with the Central Pollution Control Board (CPCB) setting specific stack emission limits for key pollutants—30 mg/Nm³ for particulate matter (PM), 800 mg/Nm3 for NOx, and 100 mg/Nm3 for SO2 from kiln and clinker cooler outlets, as mentioned in or a report by the CPCB (2024). These norms are comparable to the EU-Best Available Techniques (EU-BAT) reference levels, which stipulate 10–30 mg/Nm3 for PM, 200–800 mg/Nm3 for NOx, and 50–400 mg/Nm3 for SO2, depending on plant design and fuel type—as mentioned in or a report by the European Commission’s BAT Reference Document (BREF, 2023). Meanwhile, US-EPA’s National Emission Standards for Hazardous Air Pollutants (NESHAP) require PM to be maintained below 30 mg/Nm3 for new cement kilns, reinforcing global convergence toward tighter thresholds. India’s 2016 revision of cement emission norms marked a watershed moment, reducing permissible PM levels from 150 mg/Nm3 to 30 mg/Nm3, driving widespread retrofits of ESPs and installation of high-efficiency baghouses across major plants. As highlighted in a TERI policy paper (2025), nearly 80 per cent of India’s integrated cement capacity now complies with these upgraded standards, supported by Continuous Emission Monitoring Systems (CEMS) and regular digital reporting to state pollution control boards—placing India’s emission control framework among the most advanced and transparent in the Global South.
Building a low-emission, high-performance industry
India’s cement sector stands at a defining crossroads—where growth and sustainability must advance together. With production projected to exceed 600 million tonnes by 2028, as mentioned in or a report by JMK Research (2024), India’s leadership in emission control will shape global low-carbon manufacturing. Over the past decade, regulatory reform, CPCB’s 30 mg/Nm3 PM limits, continuous monitoring, and ESP-to-baghouse conversions have brought India close to EU and US benchmarks. The next leap requires integrated decarbonisation—linking AI-driven optimisation, renewable energy, alternative fuels, and carbon capture. As mentioned in or a report by the IEA (2025), digital technologies can reduce CO2 emissions by up to 8 per cent by 2030, while CCUS and AFR could cut process-related emissions by 40 per cent to 50 per cent. Meanwhile, R&D in LC³ and belite cements, combined with circular-economy co-processing, is reshaping both the chemistry and carbon profile of Indian cement. Policy incentives, carbon finance, and strong industry–academia collaboration will be key to making India a pioneer in green cement.
Ultimately, emission control is becoming a strategic advantage, not just compliance. The future cement plant will be a hybrid of automation, accountability, and adaptive design, where digital twins optimise processes and every gram of carbon is tracked. By coupling robust policy frameworks with investment in skills, digital infrastructure, and collaborative innovation, India can redefine sustainable heavy industry. The goal now is not incremental change but transformational adoption, where every avoided emission strengthens both the planet and profitability. With its evolving ecosystem of technology, regulation, and intent, India’s cement sector is poised to become a global benchmark for low-emission, high-performance manufacturing and a model for industrial decarbonisation.
Carbon Emissions in Ready-Mix Concrete
This case study, published in Case Studies in Construction Materials (Elsevier, Jan 2025) by Zuojiang Lin, Guangyao Lyu, and Kuizhen Fang, examines carbon emissions in C30–C80 ready-mix concrete in China and explores CO2 reduction through SCMs, transport optimisation, and manufactured sand use.
This study analyses the carbon emissions of C30–C80 ready-mixed concrete using a large-scale mix proportion dataset from across China. The research applies a life-cycle assessment (LCA) based on IPCC and ISO 14040 standards to calculate total emissions, covering raw material production, transportation, manufacturing, and concrete delivery. The findings reveal that average carbon emissions range between 262.61 and 401.78 kgCO2e/m3, with cement accounting for about 90 per cent of embodied emissions. The study establishes that emission variations primarily arise from differences in cement dosage and raw material composition rather than energy use in manufacturing or transport.
The study identifies Supplementary Cementitious Materials (SCMs)—such as fly ash, ground granulated blast furnace slag, and silica fume—as major contributors to CO2 reduction. By partially replacing cement, SCMs lowered total emissions by 5 per cent to 30 per cent while maintaining equivalent strength levels. However, around 11 per cent of samples showed negative reduction rates, indicating that improper SCM selection or inconsistent material quality can offset benefits. The relationship between SCM substitution rates and CO2 reduction was found to be positively correlated but weakly linear, with considerable data dispersion due to mix variability.
Transport distance was also evaluated as a significant but secondary factor influencing emissions. The study found that CO2 reduction benefits from SCMs remained stable until transport distances exceeded 4166 km, beyond which the gains were nullified. For every additional 100 km of SCM transport by truck, the carbon reduction rate decreased by only 0.45 per cent. Comparatively, long-distance transport of aggregates from 100 km to 500 km increased concrete’s carbon emissions by over 10 per cent. This highlights the higher sensitivity of total emissions to aggregate logistics than SCM transport.
Lastly, the study analysed manufactured sand (MS) as a substitute for natural fine aggregates (NFA). While MS reduces transport-related emissions due to shorter sourcing distances, it increases total production energy consumption and can reduce concrete strength. When 50 per cent to 100 per cent of NFA was replaced with MS, total CO2 emissions remained largely unchanged. The authors conclude that SCMs offer clear and stable low-carbon benefits, whereas MS requires technological optimisation to realise its potential. Overall, the research provides quantitative evidence supporting low-carbon labelling standards for China’s concrete industry and underscores the importance of balancing strength, sourcing, and sustainability.
Reducing CO2 in Cement Production
This case study, published in Industrial & Engineering Chemistry Research (ACS Publications, Sept 2024) by Franco Williams and Aidong Yang, investigates CO2 reduction in cement manufacturing through alternative clinker compositions and CO2 mineralisation, achieving up to 45.5 per cent energy and 35.1 per cent CO2 savings in simulations.
This study investigates strategies for reducing CO2 emissions in cement production, which currently contributes around 8 per cent of global anthropogenic CO2. Using Aspen Plus V12.1 process simulations, seven clinker production scenarios were analysed — including Ordinary Portland Cement (OPC), three variants of High-Ferrite Clinker (HFC), Belite-Ye’elimite-Ferrite Clinker (BYF), Calcium Silicate Cement (CSC), and a hybrid option combining OPC with a Supplementary Cementitious Material (SCM) produced via CO2 mineralisation. The objective was to quantify differences in energy demand and CO2 emissions under natural gas–fuelled conditions and assess the decarbonisation potential of each composition.
The simulations revealed that alternative clinkers significantly outperform OPC in both energy efficiency and carbon footprint. OPC clinker production required 1220.4 kWh/t, emitting 741.5 kgCO2/t clinker, while CSC clinker achieved the lowest total energy intensity at 665.1 kWh/t, corresponding to a 45.5 per cent energy reduction and 35.1 per cent CO2 reduction. This efficiency stems from CSC’s low CaCO3 input (989.7 kg/t clinker) and sintering temperature of 1250°C, compared to OPC’s 1271.5 kg/t and 1500°C. The BYF clinker followed with 31.3 per cent energy savings and 27.5 per cent CO2 reduction, while HFC variants achieved moderate reductions of 3.1 per cent to 6.4 per cent in CO2 emissions.
For the SCM + OPC scenario, 25 per cent of the clinker was replaced with SCM derived from CO2 mineralisation. Despite a higher total energy requirement (1239.6 kWh/t) due to capture and mineralisation energy, this option delivered the greatest CO2 reduction—up to 44.8 per cent relative to OPC. The benefit was attributed to CO2 absorption during mineralisation and reduced clinker mass. However, the study noted that the energy intensity of mineralisation (1.30 kWh/kg SCM) exceeded that of clinker production (1.22 kWh/kg), indicating that this strategy’s effectiveness depends on access to low-carbon electricity sources.
Geographical variations also influenced the overall carbon footprint. When accounting for electricity grid emissions, Brazil showed the lowest total CO2 output (482.7 kgCO2/t) for SCM-integrated cement due to its green energy mix, compared to 601.6 kgCO2/t in China and 556.1 kgCO2/t in the United States. For CSC clinker, total reductions were 35.7 per cent, 36.0 per cent, and 35.3 per cent respectively across these countries. This emphasises that decarbonisation gains are highly dependent on the carbon intensity of local power grids.
Supporting simulations demonstrated that lowering sintering temperatures alone (to 1350°C or 1250°C) could reduce total energy consumption by 7 per cent to 17.5 per cent and CO2 emissions by 1 per cent to 2.6 per cent. However, these results are modest compared to the full compositional changes in alternative clinkers, confirming that reducing CaCO3 content in the raw meal contributes more significantly to CO2 mitigation. The decomposition of CaCO3 releases 0.44 kg CO2 per kg CaCO3 and requires 179.4 kJ/kmol of heat; hence, formulations with reduced limestone and alite (C3S) contents inherently lower both emissions and energy demand.
In conclusion, the study establishes that Calcium Silicate Cement (CSC) is the most energy-efficient clinker alternative, while SCM-integrated OPC achieves the highest CO2 reduction potential under green-energy conditions. The authors highlight that the decarbonisation of electricity supply is crucial for maximising the benefits of CO2 mineralisation-based SCMs. These results underscore that altering clinker chemistry and incorporating CO2 utilisation pathways are practical, high-impact strategies for achieving deep decarbonisation in the cement industry and align with global net-zero goals.















 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete3 weeks ago

 Concrete1 week ago