Connect with us

Economy & Market

Digitalisation is pivotal in driving energy efficiency

Published

on

Shares

As energy costs continue to dominate the cement industry, efficiency and sustainability are proving to be vital components. MM Rathi, Joint President, Power Management, Shree Cement, explains the company’s long-term strategy is focused on cutting emissions while powering growth with renewable energy solutions.

Energy efficiency has always been a cost-saving lever for the cement industry. Today, it is the backbone of sustainability and competitiveness. Cement manufacturers are under growing pressure to optimise consumption, diversify power sources and align with decarbonisation targets. Shree Cement has been at the forefront of this transformation, significantly scaling up its green power capacity and embedding advanced technologies across operations. In this exclusive conversation, MM Rathi, Joint President – Power Management, Shree Cement, shares insights on the company’s approach to energy efficiency, challenges in brownfield modernisation and long-term strategies for achieving net zero alignment.

What percentage of your total operational cost is attributed to energy consumption?
At Shree Cement, energy is one of the most significant components of production cost, accounting for nearly 30 per cent to 40 per cent of total operational expenses. Within this, thermal energy typically contributes around 20 per cent to 25 per cent, while electrical energy forms about 10 per cent to 15 per cent. The exact share varies depending on factors such as the fuel mix (coal, pet coke or alternative fuels and raw materials), the power source (grid-based or captive like solar, wind or thermal), raw mix quality, and regional fuel and electricity price variations. This makes energy efficiency and the adoption of sustainable power sources a key focus area, both from a cost and sustainability perspective.

How has your company improved energy efficiency over the past five years?
Over the past five years, Shree Cement has consistently invested in enhancing energy efficiency across operations. Our green power capacity, covering wind, solar and Waste Heat Recovery (WHR), has more than doubled from 245 MW in 2020 to 592 MW in 2025. All grinding units are now equipped with biomass firing facilities, reducing dependence on conventional fuels. From the project stage itself, we prioritise efficiency by selecting advanced technologies such as six-stage kilns with integrated WHR, CFD-designed plants, and equipment fitted with VFDs, centrifugal compressors and high-efficiency fans. We also review and upgrade equipment systematically, replacing fans, compressors, blowers, pumps, boilers and turbines with more efficient options. This continuous approach has reduced costs while significantly advancing our sustainability journey.
What technologies or practices have shown the highest energy-saving potential in cement production?
WHR stands out as one of the most effective solutions, offsetting a significant portion of electricity required for clinker production. Hot air recirculation has also proven highly beneficial in reducing heat losses. Additionally, regular energy audits help us identify opportunities for improvement and implement corrective measures in daily operations. Together, these practices play a critical role in optimising energy efficiency and driving sustainable operations.

What are the key challenges in adopting energy-efficient equipment in brownfield cement plants?
The biggest challenge is the significant upfront investment required for upgradation. Retrofitting existing facilities often involves complex civil and structural modifications, which add costs and extend downtime. Integration is another hurdle, as new high-efficiency equipment may not align seamlessly with older kiln systems, fans, mills or automation setups. These factors make the transition in brownfield plants more resource-intensive and time-consuming compared to greenfield projects.

How do you measure and benchmark energy performance across different plants?
We track key performance indicators such as specific heat consumption and specific power consumption for each unit, benchmarking them against internal and external standards. Thermal Substitution Rate (TSR percentage) is another critical metric, measuring the share of alternative fuels in the thermal energy mix. Internally, we benchmark performance across plants to encourage best practice sharing. Externally, we compare against national averages and align with the Bureau of Energy Efficiency’s PAT (Perform, Achieve, Trade) scheme, which sets Specific Energy Consumption (SEC) baselines and targets for cement plants. This multi-layered approach ensures continuous monitoring, improvement, and industry leadership in energy efficiency.

What role does digitalisation play in achieving energy efficiency in your operations?
Digitalisation is pivotal in driving energy efficiency at Shree Cement. IoT sensors integrated with SCADA and DCS systems allow real-time monitoring of parameters like heat consumption and energy use, moving beyond periodic reports. Our digital platforms consolidate plant data, enabling management to compare metrics such as SPC, SHC, kWh per tonne and kcal per kg across units in real time. This visibility supports data-driven decisions, faster corrective actions, and higher operational efficiency.

How do government policies and incentives influence your energy-saving decisions?
Government policies and incentives strongly shape our energy-saving decisions. The Perform, Achieve, Trade (PAT) scheme sets plant-specific SEC targets. Non-compliance incurs penalties, while compliance earns tradable energy-saving certificates. This ensures energy efficiency is both cost-driven and regulatory. Additionally, subsidies and viability gap funding for renewable energy projects in wind, solar and AFR co-processing help reduce payback periods and make energy-saving investments more viable.

What is your long-term strategy for aligning energy efficiency with decarbonisation goals?
Our long-term strategy aligns energy efficiency with India’s net zero 2070 goals. Key levers include improving efficiency, expanding green electricity, producing more blended cement, and increasing alternative fuel use. Today, more than 60 per cent of our electricity comes from green sources such as solar, wind, and WHR, the highest in India’s cement industry. Our blended cement products, which reduce limestone and fuel consumption, further lower emissions. These products are certified under the GreenPro ecolabel by CII, validating our sustainability practices and environmental standards.

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

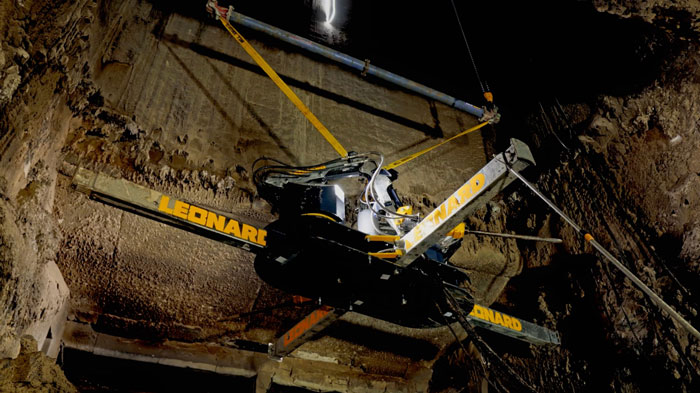
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.


Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

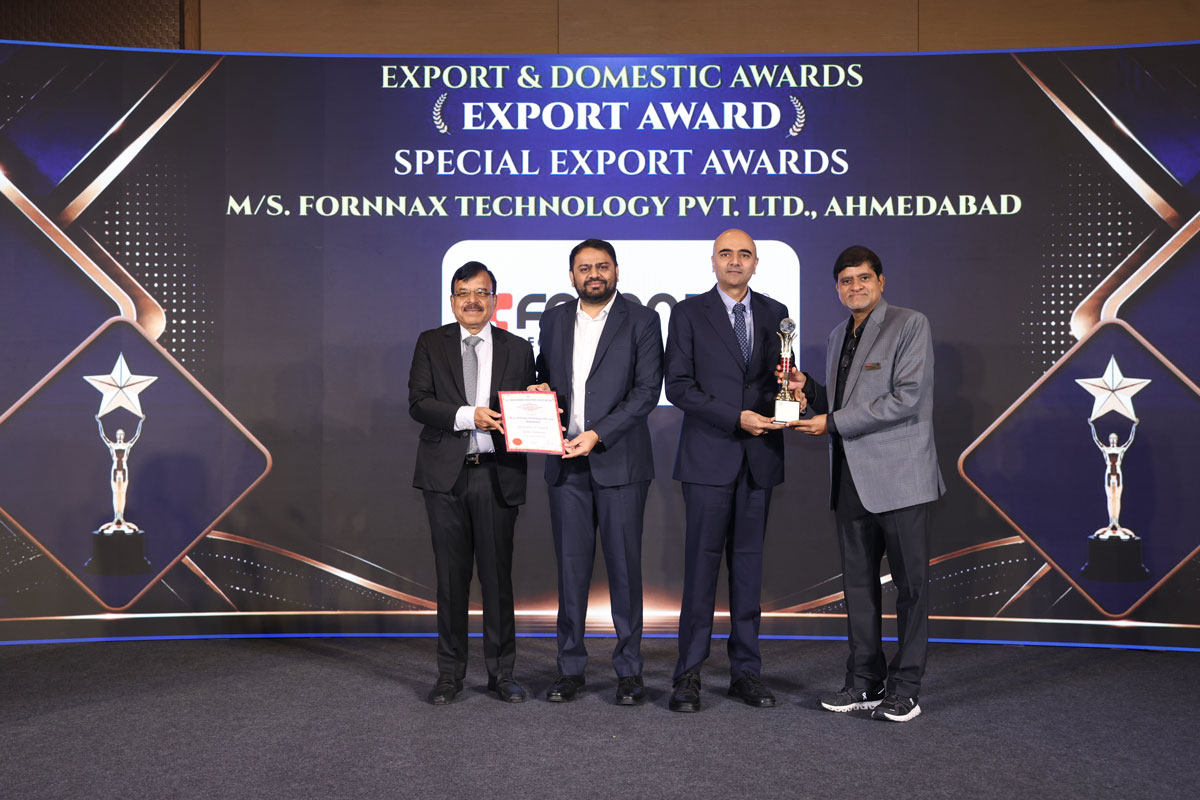
Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds