Connect with us

Economy & Market

Maximising AFR in Cement Manufacturing

Published

on

Shares

Shreesh A Khadilkar, Consultant and Advisor, and Former Director Quality and Product Development, ACC Ltd Thane, discusses the importance of optimising the use of alternative fuel and raw materials (TSR percentage) in cement production without affecting clinker quality, in part one of this two-part series.

Over the past decade or so, the Indian cement industry has made significant progress in terms of improvement in energy efficiency and productivity. However, the use of alternative fuel and raw material (AFR) to replace coal for thermal energy needs, remains an area where the Indian cement industry is yet to catch up with global benchmarks. Though a few cement plants co-process large quantities and varieties of AFR in their kilns, and are reported to reach a level of around 40 per cent Thermal Substitution Rate (TSR), many plants are still at much lower levels of TSR percentage.
Most of the cement plants have now installed co-processing facilities or are on the verge of having one. Some of the plants also have pre-processing facilities, which could include shredding, segregation, impregnation, foreign body removal etc., while some others source a pre-processed solid AFR (RDF, MSW, Industrial waste sludges, agro wastes etc.).
This article shares important aspects such as assessment of clinker quality in plant clinker quality optimisation, influence of alkalis, chlorides and SO3, effects of some important minor constituents and subsequently discusses the concept for maximising AFR (TSR percentage) without affecting clinker quality through with or without use of XRD technique for in process control. The author further recommends bi-hourly quality and in process dashboard for consistent kiln performance and consistent clinker quality.

Assessment of Clinker Quality
The clinker quality assessment can best be done by Lab Ball Mill grinding of day average clinker with mineral gypsum (with SO3 of the lab ground cement targeted at 2.2 to 2.4 with fixed grinding time to achieve Blaine’s of around 300-320 M2/kg with the residue on 45 microns of the cement in range of 18 per cent to 20 per cent, at this fineness, the clinker is observed to clearly depict changes in clinker reactivity in terms of changes in 1 Day strengths of cements (± 3 to 5 MPa). At lower grinding Blaine’s (of around 250 M2/kg), which is presently being practiced by many cement plants, one does not observe the changes in clinker reactivity, as the difference of 1 Day compressive strengths is only ± 1 MPa, which does not show the changes in clinker reactivity.
Typically, clinkers with good reactivity are observed to show 1 Day strengths in lab ground cements of 30 to 35 MPa. Higher values being observed when clinker alkali sulphates are high (especially with Petcoke as fuel), the achieved Blaine’s and quantity of nibs removed from the lab ground cement, in the fixed grinding time is also indicative of clinker grindability. Judicious raw mix optimisation with existing or alternative corrective materials (with the fuel mix used by the plant) can be attempted so as to have a clinker with improved reactivity/hydraulic potential. In a running plant the approach has to be by attempting small gradual changes to clinker composition and assessing the impact of the changes, on kiln performance and clinker quantity.
The changes to be attempted could be indicated through data analysis.
In each plant, the QC and process has detailed analysis data of the day average clinkers along with its lab ground cement test results. It is also suggested to test at least one spot clinker per day for chemical parameters and physical tests of lab ground cement. From the analysis data it could be observed that on some days the lab ground cements show much higher strengths. Why on some days or in some spot clinkers, the clinker reactivity is suddenly very good? Such clinkers should be preserved and evaluated by XRD, so as to identify the optimum clinker composition which shows higher reactivity. Such an evaluation could also indicate at times the impact of changes in fuel / sources of coal / proportions of coal and Petcoke (even source of Petcoke) / solid AFR usage levels.
Typically, the target clinker composition to give a good hydraulic potential would be with LSF of 93 to 95 with a bogues potential C3S of >55 per cent clinker (especially with Petcoke as main fuel in fuel mix), with C3A (6.5 per cent to 8.5 per cent) if the clinker is used for PPC/PSC and also for OPC (especially if OPC is supplied to RMX customers) and SM 2.2 to 2.4 A/F 1.2 to 1.4. In plants where clinker MgO is higher (> 4.5 per cent), besides having the LSF target of around 93 to 95, the minimum clinker lime targeted should be such to have C/S ratio of 2.95 to 3.1 for having good clinker reactivity in spite of high clinker MgO.
Co-Processing of AFR (Liquid AFR /Solid AFR)
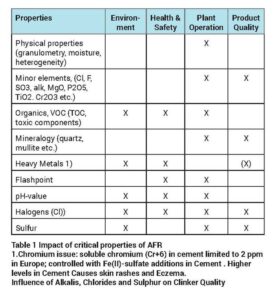
The properties of AF(R) co-processed in the calciner have an impact on environment, health and safety, plant operations and product quality as shown in Table 1:

  • Alkalis without sulphidisation: Formation of orthorhombic C3A, fast setting
  • Alkali sulphates (Na2SO4, K2SO4, 2CaSO4.K2SO4 or even Ca-langebnite): Increased early strength, usually shows decrease of later age strengths. Changes must be accounted for in gypsum optimisation
  • Excess of sulphur over alkalis
  • Integration of SO3 in C2S and/or formation of CaSO4
  • Possible reduction of final strength could be observed
  • Reduces the CaO availability for C3S formation
  • The clinker could be harder to grand
  • Changes the Clinker Liquid Characteristics which affects the phase formations
  • Chlorides tend to be higher in AFR liquid/solid, the control on chlorides is necessary to prevent inlet/cyclone jamming and to have < 0.06 per cent in clinker, so that the OPC has <0.04 per cent chlorides and is suitable for
  • RMC/structural concrete. To avoid problems of kiln inlet and cyclone jamming caused by SO3 and Cl. Preferably maintain the Hot Meal (2 Cl + SO3) < 3.5. The threshold value for a given plant needs to
    be assessed.

If the value goes above the plant threshold value, immediate actions of adding caustic soda for 2 to 3 shifts (in small polyethene bags) should be done to remove the depositions and avoid kiln stoppage.

Effects of some minor constituents on the clinker quality

Effects of ZnO

  • Zinc in clinker nearly distributes evenly between the silicates ad matrix phases (with preference to ferrite), trigonal C3S and ß C2S is stabilised by zinc.
  • Presence of zinc reduces the amount of aluminates in favour of alumino ferrite.
  • Each 1 per cent zinc reduces aluminates by
    1 per cent and increases alumino-ferrites by
    2 per cent.
  • Zinc is very effective flux and mineraliser, it lowers clinkerisation temperatures and accelerates lime combination. Knofel reports increased comp. strengths by up to 20 per cent and above at early ages.

Effects of TiO2

  • The clinker TiO2 should be <0.7 per cent, it should be noted that TiO2 is a viscous flux like Al2O3 and so for understanding the clinker liquid property for good C3S formation and based on the kiln conditions adjust the clinker Fe2O3 contents accordingly.
  • At higher TiO2, contents for improved kiln conditions the clinker Fe2O3 content needs to be much higher which is aggravated if clinker SO3 is higher (which also affects the viscosity of clinker liquid)
  • At high total liquid the clinker becomes silica deficient and so free lime tends to be higher (with clinker balls with calcined un sintered material inside)
  • In plants that use red mud especially with petcoke due to its higher alkalis, many sources of red muds also have TiO2, the plant should target Al2O3 + TiO2 as the viscous flux and then adjust the clinker Fe2O3 to get good kiln conditions as indicated above. Targeting higher liquid only increases the limestone LSF from mines and also affects clinker grindability.

Effects P2O5 sources

  • Many types of agriculture waste, biowastes, phosphate sludge, paint sludges, medical waste, RDF/municipal solid waste, expired detergent, cow dung cakes, etc.
  • Under Indian conditions of clinker phase composition, any increase of P2O5 contents can substantially affect clinker quality.
  • When higher P2O5 are present, the dicalcium silicate (C2S) is stabilised and inhibits formation of alite (C3S) i.e can decrease the percentage of C3S although bogue may show high percentage C3S.
  • When P2O5 present exceeds 0.4 per cent in the clinker it reduces the percentage of C3S by 10 per cent and 1 Day Comp. Strengths by around 5-6 MPa with negative effects on clinker reactivity and setting of cement.
  • Use of wastes containing phosphates in controlled manner so that P2O5 in the clinker (maximum limit in clinker is 0.25 per cent) can enhance the use of agricultural waste or use of other wastes with P2O5. It may be noted that in some regions limestone and laterite also have shown P2O5 contents.
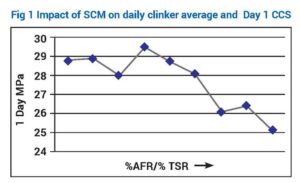
  • In some plants up to 5 to 7 per cent TSR there is no impact observed on quality or productivity, however as the TSR/AFR percentage is increased say above >8 per cent to 10 per cent, the kiln conditions get frequently disturbed with a very high dust generation and there is a drop in clinker reactivity/quality.

In the plants a judicious study of process conditions and understanding the burnability of kiln feed could help achieve productivity without affecting the clinker quality with increased AFR/TSR.

In one of my consultancy visits to an integrated plant, similar observations as above were reported. In a brainstorming discussions with the plant process, production and QC teams, it was noted that:

  • There was substantial variation in calciner outlet/kiln inlet material/C6 material temperature it fluctuated from around 920oC to as low as 860oC, these changes in temperatures nearly corresponded with the fluctuation in percentage of moisture and feed rate of solid AFR (SAFR), RDF and other solid wastes.
  • The kiln torque decreased below the desired levels, when the calciner outlet and kiln inlet material temperatures (in this case C6 material temperatures) were less than 890oC and the kiln performance showed high dust recirculation/generation.
  • The bi-hourly XRF analysis of clinker showed lower LSF/high free lime. The decrease in clinker LSF was understandable as the SAFR ash showed a higher percentage of ash.

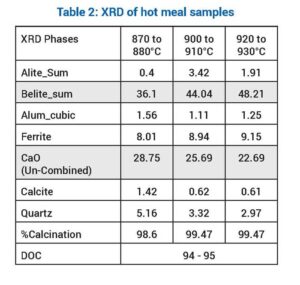
It was decided to collect hot meal samples 900oC to 910oC and 920oC to 930oC and also corresponding clinker samples collected after 40 minutes of the sample collection time of hot meal samples. The hot meal samples were analysed for XRD and clinker samples for XRF (Chemical analysis with free lime) and XRD (for clinker phase formation).
The XRD analysis of hot meal samples is shown in Table 2.
The XRD analysis indicates that:

  • The calcination percentage is much higher than the convention DOC of hot meal samples.
  • The un-combined CaO decreases with increase in temperature of collected sample.
  • The total belite increases with increase in temperature.

It was observed in the plant that when attempts were made to maintain the kiln inlet material temperature at 910oC to 920oC, the kiln torque showed an improvement and the kiln performance improved. The clinker quality showed improvements with lower free lime. However due to the fluctuations in ash percentage content of SAFR the clinker LSF showed lower values during the day. As a corrective action, lime sludge (available at the plant) was added on the SAFR conveyor. These corrective actions helped achieve a consistent improved clinker quality.

About the author:
With an MSc in Organic Chemistry from Jodhpur University (now JNV University), Shreesh Khadilkar joined ACC’s Organic Chemical Product Development Division in 1981 and later transitioned to the Cement R&D Division as a technical assistant. He took over as VP of R&D (Quality and Product Development Division) and retired as Director of the department in 2018, with over 37 years of experience in cement manufacturing and cements/cementitious products.
Concrete

ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown

Published

on

By

Shares

ABB reconditions 25 drives at ACC’s Jamul cement plant, avoiding 16 tonnes of CO₂ emissions while improving reliability through predictive maintenance.
Chhattisgarh

ABB has signed a multi-year Motion OneCare service agreement with ACC Limited, part of the Adani Group, to modernise ageing industrial drives at its Jamul cement plant in Chhattisgarh, improving operational reliability while avoiding approximately 16 tonnes of carbon dioxide (CO₂) emissions without disrupting production.

Announced on 27 October 2026, the agreement combines scheduled drive reconditioning, digital condition monitoring and energy appraisals to extend equipment lifespan, improve plant uptime and optimise maintenance costs. The initiative marks a shift from conventional equipment replacement towards a more resource-efficient approach to industrial asset management.

The first phase, completed in April 2026, involved the on-site reconditioning of 25 ABB ACS800 variable speed drives without a major plant shutdown. By retaining the existing cabinets and restoring the drive modules rather than replacing entire panels, ABB helped ACC preserve capital investment, minimise material consumption and avoid approximately 16 tonnes of CO₂ emissions.

A second phase, covering an additional 25 ACS800 drive modules, is scheduled for the fourth quarter of 2026. The programme is designed to improve long-term equipment reliability while allowing maintenance activities to be aligned with the plant’s operational schedules.

The ACS800 drives, installed at Jamul in 2010, had delivered more than a decade of near-continuous service in demanding cement manufacturing conditions. However, ageing electrical components and changing fault patterns had begun to affect their ability to meet the plant’s reliability requirements.

Rather than opting for complete equipment replacement, ACC engaged ABB’s certified engineers to conduct a comprehensive asset health assessment. The evaluation found that the existing cabinets and enclosures remained structurally sound, making targeted reconditioning a technically viable and cost-effective alternative to full replacement.

Drawing on nearly two decades of experience with ACC’s equipment and operating requirements, ABB developed a maintenance framework tailored to the plant’s shutdown windows, budget cycles and production priorities.

The Motion OneCare agreement incorporates planned equipment restoration, condition-based monitoring and energy assessments, enabling ACC to adopt a more systematic approach to maintaining critical electrical infrastructure.

As part of the programme, ACC has implemented ABB Ability™ Digital Powertrain Insights to monitor drive performance and identify emerging operational issues before they result in equipment failures.

The digital platform provides continuous visibility into parameters such as temperature, current, vibration and fault patterns. These insights allow maintenance teams to detect early signs of equipment deterioration, schedule interventions more effectively and reduce the likelihood of unexpected downtime.

Amit Gupta, Local Division Manager, Motion Services, ABB India, said: “We know what unchecked wear costs over time: a small inefficiency that eats away at ROI for years. At Jamul, the evidence pointed clearly to assets with productive life still in them.”

“Our job was to restore them properly and give the team the tools to stay ahead of the next problem. At ABB, we don’t just fix what fails. We want to protect what works.”

The initiative also demonstrates the growing relevance of circular economy principles in cement manufacturing, where extending the service life of existing industrial equipment can reduce capital expenditure, material consumption and the environmental impact associated with manufacturing replacement components.

According to ABB, drive reconditioning can reduce lifecycle emissions by 50 to 80 per cent compared with complete equipment replacement. By preserving functional components and restoring critical modules, the process helps retain the economic and material value of existing industrial assets.

The addition of energy appraisals in subsequent phases will further expand the programme beyond equipment restoration, enabling ACC to assess drive performance, identify energy-saving opportunities and improve operating efficiency.

For cement manufacturers, variable speed drives play an important role in controlling motors and optimising energy consumption across production processes. Maintaining their reliability and efficiency is essential for minimising operational disruptions and managing electricity costs.

Vinod Bahety, CEO – Cement Business, Adani Group, said: “Moving from reactive firefighting to a structured maintenance plan was exactly what this operation needed. That kind of peace of mind doesn’t come easily. It comes from a partner that understands how your business runs.”

“We didn’t need a full system overhaul; we needed expert support, actionable insights, and a plan we could execute around our schedule. That’s what we got.”

The project supports ACC’s broader strategy to improve manufacturing efficiency through digital transformation, preventive maintenance and sustainable asset management.

ACC, a subsidiary of Ambuja Cements and part of the Adani Group, operates 20 cement manufacturing facilities and 119 ready-mix concrete plants across India. The company has been advancing initiatives focused on renewable energy, circular economy practices and technology-driven operational improvements.

Alongside Ambuja Cements, ACC is part of a large-scale building materials business committed to achieving net-zero emissions by 2050, with near-term and net-zero targets validated by the Science Based Targets initiative (SBTi).

The Jamul initiative aligns with these sustainability objectives by demonstrating how equipment life extension and digital monitoring can contribute to resource efficiency without requiring large-scale replacement of existing infrastructure.

ABB, a global technology company specialising in electrification and automation, brings more than 140 years of industrial expertise and employs approximately 110,000 people worldwide. Its Motion Services business supports industrial customers through equipment maintenance, modernisation, digital monitoring and lifecycle management solutions.

The agreement also reflects a wider shift in industrial maintenance practices, with manufacturers increasingly adopting predictive technologies to improve equipment availability, manage costs and reduce unplanned shutdowns.

With 25 drives already reconditioned and another 25 scheduled for restoration, ABB’s collaboration with ACC illustrates how targeted modernisation, digital monitoring and circular maintenance practices can extend the operational life of critical equipment while supporting more efficient and sustainable cement production.

Continue Reading

Concrete

ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K

Published

on

By

Shares

ABB deploys advanced process control at TCI MAX’s Srinagar cement plant to improve clinker quality, energy efficiency and sustainable manufacturing.

Kashmir 

ABB has deployed its advanced process control technology at TCI MAX Cement’s Srinagar facility in Jammu and Kashmir, marking the region’s first reported implementation of advanced process control (APC) in cement manufacturing and strengthening efforts towards more efficient, digitally enabled production.

Announced on 5 November 2026, the deployment of ABB Ability™ Expert Optimizer at the facility, operated by Trumboo Industries Pvt. Ltd., aims to improve process stability, clinker quality, energy efficiency and overall plant productivity. The implementation forms part of TCI MAX’s strategy to modernise its manufacturing operations through automation and digital technologies.

Following the integration of ABB’s advanced process control solution and supporting IT infrastructure, TCI MAX has reported improvements in operational productivity, product quality and sustainability-related performance indicators. The technology focuses on optimising the cement pyro process, a critical stage of production involving high-temperature processing and clinker formation.

Waseem Ahmed Trumboo, Director, Trumboo Industries Pvt. Ltd., said: “Introducing advanced process control at TCI MAX is an important step in how we are evolving our operations. Our focus is on improving the stability and efficiency of our processes while maintaining consistent clinker quality. We have been encouraged by the performance of the solution during commissioning and by the support from the ABB team, and we look forward to realizing its full potential.”

ABB Ability™ Expert Optimizer combines advanced process control, model predictive control (MPC) and artificial intelligence (AI) to continuously monitor and optimise manufacturing operations. By analysing process conditions, predicting operational behaviour and automatically adjusting key parameters, the system enables more consistent production while reducing process variability.

In cement manufacturing, maintaining stable pyro-processing conditions is essential for achieving uniform clinker quality and optimising thermal energy consumption. Fluctuations in operating parameters can affect fuel efficiency, production output and product consistency.

The deployment is designed to address these challenges through real-time process optimisation, helping operators maintain more stable kiln operations while improving the utilisation of fuel, electricity and raw materials.

Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries Division, ABB India, said: “Cement producers are increasingly looking to adopt digital technologies to achieve greater consistency and efficiency while addressing their sustainability priorities. ABB Ability™ Expert Optimizer brings advanced process control and deep cement process expertise together to help operators make their processes more stable and efficient. We are pleased to support TCI MAX as it takes this important step in its digital transformation.”

The technology also supports sustainability objectives by optimising fuel consumption, improving electrical energy efficiency and minimising process waste. More stable operations can contribute to lower energy intensity and reduced emissions associated with cement production.

For TCI MAX, the investment represents a move towards data-driven manufacturing, where automated control systems complement operator expertise to improve production performance and operational reliability.

The implementation is particularly significant for Jammu and Kashmir’s cement industry, as it introduces advanced process optimisation technology to a regional manufacturing facility. Its deployment could demonstrate the potential for wider adoption of digital automation across cement plants seeking to modernise their operations.

The project builds on ABB’s experience in delivering advanced process control solutions to cement manufacturers worldwide. Through the integration of industrial automation, predictive technologies and process engineering expertise, the company supports manufacturers in improving resource efficiency and maintaining consistent production quality.

As cement producers face increasing pressure to manage energy costs, improve productivity and reduce their environmental footprint, technologies such as AI-enabled process control and predictive optimisation are becoming important components of plant modernisation strategies.

ABB’s Expert Optimizer provides a platform for addressing these priorities by enabling automated adjustments based on changing process conditions, reducing reliance on manual intervention and supporting more efficient plant operation.

ABB, a global technology company specialising in electrification and automation, has more than 140 years of industrial experience and approximately 110,000 employees worldwide. Its Automation business employs around 26,000 people and provides technologies and services across process, hybrid and maritime industries.

The TCI MAX deployment reinforces ABB’s growing role in the digital transformation of cement manufacturing in India, where improving process efficiency and reducing energy consumption remain critical to the industry’s long-term sustainability.

With the advanced process control system now implemented at its Srinagar facility, TCI MAX aims to build on the initial operational improvements and further optimise production efficiency, clinker consistency and environmental performance.

Continue Reading

Concrete

Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’

Published

on

By

Shares

Ramco Cements’ Hard Worker brand wins eight awards for excellence in advertising, packaging and brand identity at the Love of Advertising Awards 2026.

Hyderabad 

The Ramco Cements Limited’s construction chemicals brand, Hard Worker, has secured eight awards at the Love of Advertising Awards 2026, recognising its creative excellence across television, digital advertising, packaging design and brand identity.

Organised by the Advertising Club of Trivandrum, the awards were presented at a ceremony held at The Leela Raviz, Kovalam, on 24 October 2026. The recognition highlights Hard Worker’s integrated marketing strategy and its efforts to establish a distinctive presence in India’s competitive construction chemicals market.

The eight awards span multiple creative categories, reflecting the brand’s approach to combining product-focused communication with engaging storytelling, humour and innovative design. Through its campaigns, Hard Worker has sought to simplify technical product benefits and make construction chemicals more accessible and relatable to consumers and construction professionals.

Built around the philosophy of “Hard-working products for hardworking people”, the brand focuses on communicating practical product advantages through memorable advertising narratives while maintaining a consistent identity across different marketing platforms.

Its campaigns for Ramco Hard Worker Eco Plaster and Tile Fix have been central to this approach. The Eco Plaster campaign highlights water conservation through the product’s self-curing properties, positioning it as a solution that supports more efficient construction practices. Meanwhile, Tile Fix promotes specialised tile-fixing solutions by presenting their practical benefits through relatable situations and creative storytelling.

Beyond advertising, Hard Worker has invested in distinctive packaging and brand identity development to improve product recognition and maintain consistency across customer touchpoints. This integrated approach has helped the brand differentiate itself in a category where marketing communication has traditionally focused on technical specifications and functional performance.

A V Dharmakrishnan, CEO, Ramco Cements, said, “Winning eight awards at the Love of Advertising Awards is a proud moment for Ramco Cements and the Hard Worker team. We believe that building a strong brand requires not only quality products but also the ability to communicate their value in a compelling and differentiated manner. Hard Worker’s journey reflects our commitment to combining product performance with innovative marketing to create meaningful connections with our customers and strengthen our presence in the construction chemicals market.”

The recognition comes as building materials manufacturers increasingly focus on brand differentiation, product awareness and customer engagement to strengthen their position in the construction chemicals segment.

By using humour and storytelling to explain product applications and benefits, Hard Worker aims to bridge the communication gap between technical construction solutions and the practical requirements of contractors, applicators and end-users.

Balaji K. Moorthy, Executive Director – Marketing, Ramco Cements, said, “Hard Worker was conceived to bring a fresh perspective to the construction chemicals category, where product communication has traditionally been functional and technical. Our endeavour has been to break through the clutter with distinctive ideas, humour and storytelling, while keeping the product proposition at the heart of every campaign. The recognition across TV and digital advertising, packaging design and brand identity design demonstrates our integrated approach to building the brand. These eight awards are an encouraging recognition of the creative thinking and collaborative effort behind Hard Worker’s marketing initiatives.”

The awards add to Hard Worker’s growing portfolio of creative recognitions and reinforce Ramco Cements’ emphasis on integrating product innovation with strategic marketing.

The brand’s communication initiatives also reflect a wider shift in the construction materials industry, where manufacturers are increasingly adopting consumer-focused marketing strategies to improve product understanding and strengthen relationships with construction professionals.

With its portfolio of construction chemicals, Hard Worker aims to address evolving requirements for durability, application efficiency and construction quality. Its marketing efforts seek to complement these product attributes by building stronger awareness and encouraging the adoption of specialised construction solutions.

Ramco Cements, one of India’s established cement manufacturers, operates across cement and allied building solutions. Through Hard Worker, the company is expanding its presence in the construction chemicals segment with products designed to enhance performance, quality and durability in modern construction applications.

The latest recognition strengthens Hard Worker’s brand visibility and underscores the growing importance of creative communication in promoting technical building materials. Ramco Cements intends to continue combining product development with distinctive marketing initiatives to support the brand’s growth in India’s construction chemicals market.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds