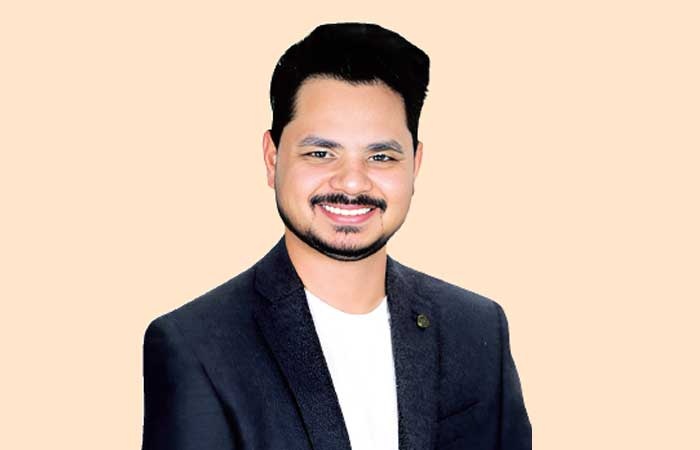
Prashant Verma, Co-founder and India Head, Nanoprecise Sci Corp, discusses the exponentially growing importance of technology and IT initiatives in all the processes related to cement production.
Tell us about the role of automation and technology in achieving efficiency in cement plants.
Technology has been playing a crucial role in transforming the operations of cement plants. It has paved the way for data-driven decision-making, which is now a hallmark of modern cement plants. The vast amount of data collected through automation systems is analysed to uncover operational inefficiencies and opportunities for process improvements. This data-driven approach enables plant personnel to optimise production schedules, increase productivity and stay ahead in a competitive market.
Technological evolution has also enabled the implementation of predictive maintenance solutions, which help identify potential equipment failures before they occur. The emergence of predictive maintenance solutions has revolutionised maintenance practices in cement plants. With real-time data from IoT sensors and AI-powered algorithms, these systems can predict faults in equipment well in advance, thereby preventing any unplanned down or catastrophic failure. This proactive approach optimises maintenance schedules, minimises downtime, and ultimately reduces maintenance costs. Moreover, automation and technology help maintenance teams to identify the energy consumption patterns of equipment sets, allowing them to implement energy-saving measures, leading to cost reductions and environmental benefits.
As the production of cement is moving towards Industry 4.0, how are you incorporating digitalisation in cement plants?
Embracing digitalisation is a key focus for a range of cement manufacturers across the country. Nanoprecise has been helping cement manufacturers incorporate state-of-the-art digital technologies to transform traditional cement plants into smart and connected facilities, for more than four years. One of our main efforts involves the deployment of Internet of Things (IoT) devices throughout the plant to monitor the health and performance of equipment in real time. These devices continuously collect data from the machinery, which is then transmitted to the cloud for analysis. The advanced signal processing algorithms parse through this complex machine health data to detect anomalies and predict potential equipment failures. This enables cement manufacturers to anticipate maintenance needs, helping plants optimise maintenance schedules, improve resource allocation, and avoid unplanned downtime.
How do you customise your solutions for each plant?
Customers generally have needs and requirements that are unique, and a one-size-fits-all approach may not meet their specific requirements. We are working with businesses across a wide range of sectors around the world, to deploy customised solutions that help them drive their digital transformation journey.
Customisation is an essential component of Industry 4.0 as each cement plant has unique operating conditions and equipment configurations. Our structured process involves conducting a comprehensive assessment of the plant, gathering real-time data using our ultra-low-power wireless sensors and analysing it using patented cloud-based software that detects even small changes in the machine performance and predicts the remaining useful life of any industrial asset. The solution can be customised to monitor a wide range of equipment including complicated machines like the roller press due to its ability to monitor low and ultra-low-speed applications with ease. It also allows for seamless integrations with various vertical and horizontal stacks. Moreover, the system can also be deployed on cloud or on-premise servers, thereby allowing for a simple plug and play, hassle-free deployment, without worrying about any extra IT infrastructure.
Tell us about AI-based machine productions? How does that help cement plants?
AI-based machine productions involve utilising artificial intelligence algorithms to optimise the cement production process. Through machine learning, AI algorithms can analyse historical production data, sensor readings, and other relevant factors to make accurate predictions and recommendations.
AI algorithms can monitor and analyse vast amounts of data pertaining to various production parameters to maintain consistent product quality. Moreover, by analysing data from various stages of production, AI can also identify inefficiencies and bottlenecks, suggesting optimisations to enhance overall process efficiency. Furthermore, AI can be applied to predict equipment failures and schedule maintenance activities, leading to minimal disruption and downtime. It can also optimise energy consumption by suggesting the most efficient operating conditions for equipment, thereby reducing energy costs and environmental impact.
What is the kind of data collected through automation systems? How does that help with cement operations?
Automated AI-based predictive maintenance solutions consist of 6-in-1 wireless sensors that measure the 6 most important parameters of Tri-Axial Vibration, Acoustics, RPM, Temperature, Humidity and Magnetic Flux. These sensors act as the vigilant eyes and ears of the manufacturing plants, continuously monitoring the vital indicators of the health and performance of machinery. The combination of these six vital parameters equips cement plants with a holistic view of their industrial assets, allowing for data-driven decisions to optimise operations and prevent costly downtime.
The collected data is then transmitted to the cloud through an encrypted and secured network for analysis. The AI analyses complex machine health data to discern subtle patterns, identify anomalies, and even predict potential equipment issues well in advance. This predictive capability is a game-changer for cement operations, as it empowers maintenance teams to take proactive measures before any critical failure occurs. By leveraging the power of automation and AI-driven analytics, the cement industry can reduce maintenance costs, enhance equipment reliability, and achieve higher energy efficiency, ultimately leading to improved productivity
and profitability.
Can costs and production be optimised or enhanced with the digitalisation of cement plants? If yes, how?
Digitalisation paves the way for implementing advanced digital solutions that can help maintenance teams transition from reactive to proactive maintenance strategies. Early detection of equipment issues enables planned maintenance, reducing costly unplanned downtime and minimising repair expenses. The state-of-the-art condition monitoring solutions available in the market, have the potential to revolutionise inventory management due to their predictive capabilities, thereby allowing for optimised resource allocation and reduced wastage of raw materials. This optimisation of inventory levels minimises carrying costs and mitigates the risk of overstocking or stockouts. Moreover, digitalisation allows for better monitoring of equipment’s energy consumption. By identifying the energy consumption patterns of equipment under faulty conditions, cement plants can take corrective actions to reduce energy wastage and carbon footprint, thereby achieving significant cost reductions over time.
What are the key skills required by plant personnel to transform them digitally?
Our automated solutions are designed to serve a wide range of end users, irrespective of their technical proficiency or department within the cement plant. The system generates real-time alerts that prompt the user to take necessary action, ensuring seamless and efficient operations. Moreover, our state-of-the-art dashboard and visualisation layer enables end-users and technical experts to view data from multiple dimensions, delivering an intuitive and user-friendly interface. The seamless integration of these features fosters streamlined and optimised operations within the cement plant.
Tell us about the major challenges you face in the execution of technology in cement plants.
Implementation of digital technologies such as predictive and prescriptive maintenance solutions is a challenging process in asset-intensive sectors like cement manufacturing. For instance, cement plants consist of various complex machines and equipment, each with its unique operating parameters and intricacies. Integrating and optimising technology solutions for such diverse machinery requires a deep understanding of the equipment and its operations. These plants operate in harsh and rugged environments, exposing the machines and equipment to extreme temperatures, dust, moisture and vibrations, which necessitates robust solutions that can withstand these conditions. Our solution comprises robust hardware that can monitor such machines, thereby bringing peace of mind to our customers. Our solutions undergo robust testing and validations to ensure their resilience in the rugged plant environment.
Secondly, the introduction of new technology is generally followed by an adoption curve, which is why we provide extensive customer support. We focus on gaining staff acceptance and support as that is vital to the successful implementation of technology solutions. We achieve this by conducting effective training programs that address staff concerns and promote acceptance of the new technology. Moreover, implementing technology solutions in large cement plants can be a time-consuming process. However, with our plug and play solutions, we closely collaborate with teams in these plants to streamline the implementation, allowing for hardware installation in less than five minutes and facilitating seamless integration of digital technology. This expedites the adoption of our solutions, minimising downtime and ensuring a smooth transition.
We ultimately strive to deliver technology solutions that excel in effectiveness and efficiency, ultimately optimising performance, enhancing reliability and fostering sustainable
growth in cement plants.
–Kanika Mathur














 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago