Connect with us

Economy & Market

We are aiming for a Rs 500 crore turnover by 2015 -16

Published

on

Shares

Y Srinivas Reddy, Managing Director, Bevcon Wayors.

Innovation is a continuous process at Bevcon and we have set a target to develop 10-12 new products every year. This year we are seriously focusing on the introduction of a sandwich conveyor for open cast mines for coal, says Y Srinivas Reddy, Managing Director, Bevcon Wayors. Excerpts from the interview.

How do you assess the current growth trends for bulk material handling equipment?

The current industrial situation in India is really unpredictable, ambiguous, uncertain, and we are not able to define clear strategies to meet day- to- day challenges. This has a larger impact on the bulk material handling sector, which depends on infrastructure development which in turn, is really in a shambles. Business opportunities have come down, competition is fierce, very low funds and cash flows as well as high interest rates are crippling the organizations` sustainability. In my view, there is no specific vertical that is doing well.

What is Bevcon’s strategies to bring in competitive costs, and to insulate the customer from higher costs?

The devaluation of the rupee has had a certain impact on the organisation bottom-line and there is no alternative except absorbing the extra cost, since most of the imports are in the process of transactions and as a policy, we don’t go back to our customers for extra claims. With regard to high cost funding, we are not affected at all since Bevcon Wayors is a debt- free organisation.

Effective implementation of operational excellence in every domain and close monitoring of budgets, most importantly out-of-the- box thinking and exploring new alternatives will make us more competitive and cost-effective.

Given the intense competition, what is Bevcon’s core focus on providing value addition to its customers?

Bevcon from its inception, has strongly believed in innovation in engineering, which will add greater value to the customer in terms of cost- effective and reliable solutions. We also lay much emphasis on the team’s collaborations, time-bound commitments, spreading our wings to source components from new associates, and the like.

What was Bevcon’s overall performance in 2012?

2012 was very good for Bevcon, we have not been effected by the slowdown since we could able to realise a few critical projects and sales were reasonable good. In fact, we have achieved the highest ever turnover in the last year.

Could you brief us on the Technology Development Group (TDG)? To what extent has Bevcon been able to leverage its strength?

Bevcon strongly believes that innovation is the lifeline for the organisation. To this end, we have formed an exclusive group called TDG. The core focus of the department is the development of new products, validation of products and cost- effective solutions for customer critical applications. The group consists of subject matter specialists from various domains who work collectively to get the ultimate results. We also approached DISR for recognition of as R&D hub and are hopeful that we will be through by the third quarter of this FY.

How strong is Bevcon in the cement sector and what are the major product lines for BMH?

Bevcon is competent in meeting almost all material handling needs of the cement industry, apart from supplying of conventional material handling equipment. Bevcon is in a position to provide cost- effective solutions to the industry with a series of new generation material handling equipment like steep angle conveyors, air-supported-belt and sandwich conveyors, etc. Recently, we implemented a revolutionary concept in one of the cement plants in India – conveying clinker from wagon unloading to silo storage – in the most cost- effective manner, with the lowest power consumption.

We offer end- to- end solutions from engineering to execution of various material handling equipment like conveyors, new generation equipment, bag filters, screens, feeders, storage sheds, stackers and reclaimers, pneumatic conveying systems, pipe and cross country conveyors, etc.

Brief us on the latest trends in the conveyors for raw material handling especially for the process industries.

As I see it, not many new technologies have come into material handling except in critical applications areas. But considering the environmental pollution challenges, there is a trend to use more pneumatic conveying systems than the mechanical conveying. Similarly, the storage shed concept covers the open storage of raw materials, protect them from the vagaries of the weather, as well as to reduce windswept and pollution.

What technology do you use for dense-phase pneumatic conveying systems?

Implementation of our new innovative technology Denseveyor (dense phase pneumatic conveying system) especially for the cement industry, will provide the most efficient, effective and bulk solid materials (raw meal and cement) for storage or to process the unit within a production environment.

The advantages of our system are less energy consumption, complete automated system which reduces lesser human interface, hundred per cent pollution-free, an unique system for replacement of existing FK and VP pumps, and the ability to convey material to greater distances with limited space for installation.

How environment friendly are the systems that Bevcon offers?

Bevcon gives utmost important to environment protection. A series of pollution controlling measures are in place from the stage of engineering itself; one additional advantage is that we being the manufacturers of pollution control equipment, we can create better synergy of technology from the concept so that the outcome of the commissioning of a project and product conforms to the expectations of environment protection.

How efficient is the bag type dust extraction system offered by Bevcon?

Our bag type dust extraction system is 99.9 per cent efficient, given that we use high quality sealing techniques to ensure no leakages of dust particles.

Yes, there is an automated system implemented to remove the dust load on filters at set readings and it helps reduce the resist of gas flow (pressure drop), it is amicroprocessor based panel.

A dust extraction system is available in cylindrical filters, cassette filters, cartridge type, snap band and flat collar (provided with rings).

Any new innovations from Bevcon?

Innovation is a continuous process at Bevcon and we have set a target to develop 10-12 new products every year. This year, we are seriously focusing on the introduction of a sandwich conveyor for open cast mines for coal.

Any more capex planned?

Yes, Bevcon strongly believes that organisation growth depends on infrastructure development of people, process, and in diversification.

We are putting up our third manufacturing plant this financial year at Hyderabad and have already started a new manufacturing unit strategically located in Raipur in the Chhattisgarh district about three months ago.

What are your long-term goals and your plans to achieve them?

We have clear vision goals defined for the future until 2015 -16 and a set target to reach Rs 500cr turnover; we also have plans to upgrade and put up a state- of-the- art fully automised idler manufacturing plant and develop a full-fledged manufacturing plant at Raipur.

Why should a customer come to Bevcon?

We always ensure the following aspects for every sale to create goodwill and confidence in our customers.

  • Equipment is reliable and efficient in operation.
  • Best in quality -manufactured at in-house ISO certified manufacturing units.
  • Cost- effective.
  • Innovative features in the products.
  • Low maintenance/low downtime.
  • Low wear costs.
  • Lowest product lifecycle cost.
  • Technology transfer from collaborations.
  • Customised product development to meet client needs.

Y Srinivas Reddy

  • Reddy is the founder and Managing Director of Bevcon Wayors is the first generation entrepreneur who started the business at the young age of 25 in 1990 with clear conviction of "People and Process" makes the difference to the organizations growth. In last two decades, Bevcon achieved rapid growth and delivered enterprises class engineering solutions to Global 2400 Customers.
  • His fervor for design engineering has lead to numerous innovations in Bevcon’s range of products while ensuring high quality and faster turnaround times. The company has achieved 185 crores revenue in last financial year. Mr. Reddy is an associate Member of "American Management Association" Professional Member of renewed social entrepreneurship organization "Net Impact".
  • He is also serving as the president of Uppal Industrial Association and chairman of Uppal IALA.
  • He has contributed immensely towards social causes as Founder & Managing director of IBeam Foundation, active social entrepreneurship not-for-profit Organization. He holds a bachelors degree in mechanical engineering from JNTU, Hyderabad.


Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

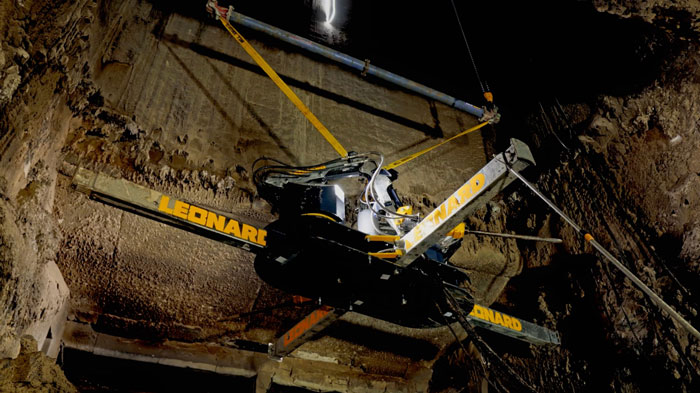
 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.

Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

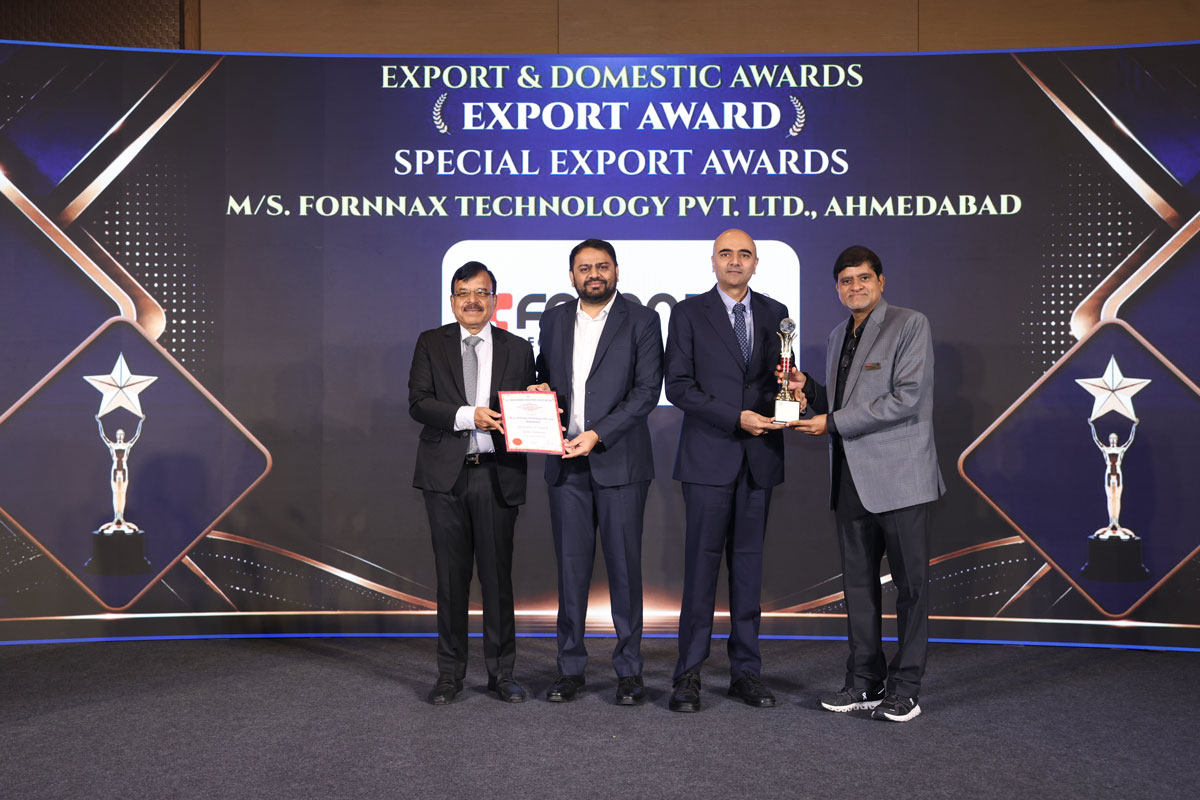
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds