Connect with us

Economy & Market

Advances in Cement Analysis

Published

on

Shares

Though Blaine analysis is a time tested method of measuring fineness of cement. Today Laser Diffraction technology scores over it mainly due to more accurate and real time measurement. Dr. Michael Caves, India ? Business Development Manager of Malvern AIMIL explains the advantages of laser based particle size analysers.

The final steps in cement manufacturing involve grinding (milling) and blending in order to produce the fine powder that is recognizable as cement. Every step in the manufacture of cement is checked by frequent physical tests, as is finished product, to ensure that it complies with all necessary specifications. Cement is ground to a particular fineness since the influence of particle size on the kinetics of cement hydration and development of strength is well known. A reduction in median particle size generally produces a higher compressive strength. Consequently the fineness of Portland cements has been increased over the years to improve properties such as higher early strengths. Nevertheless, other effects of increased fineness, such as higher water demands and more rapid heat generation in the concrete cannot be ignored. Despite the availability of instrumental methods of measuring particle size distributions, the classical method of air permeametry remains.

Understanding Blaine
Many plants control cement fineness using an air permeability apparatus to measure the Blaine number, a parameter related to the cement particle size. The Blaine surface area measurement has been used since the 1940s to determine cement quality and despite its longevity the limitations of this off-line technique are widely recognized. It is slow and suffers from poor reproducibility, which can lead to significant errors, including unnecessary or inaccurate changes to the classifier speed. Blaine analysis measures the specific surface area of a sample, the surface area per unit mass. Finer particle sizes have higher specific surface area: more area per unit mass, so Blaine is an indirect measure of particle size.

But, Blaine delivers just a single averaged figure. Figure 1 shows analysis of 2 cement samples using a Malvern Mastersizer Laser Diffraction system. Sample 2 contains more fines than sample 1 but also more coarse material. These two differences cancel each other out so average specific surface area remains the same, illustrating why two quite different samples can have the same Blaine. The more important question is ?do we need to know about the difference indicated by the particle size distribution??

Size Distribution Measurements
However two cement samples with identical Blaine figures can show different particle size distributions when measured by laser diffraction. Should we classify these two cements as different or the same?

For answers, we need to look at how the data are used. Cement manufacturers measure Blaine to quantify product quality. The hydration speed of cement particles is a function of particle size and determines the strength of the set cement. Generally, finer particles hydrate more quickly, giving greater strength, and within certain limits finer cement is better cement.

Returning to our samples, these materials will behave differently when used. Very fine cement particles, in the 2 – 3 micron range can cause exothermic cracking. Conversely particles over 50 microns may not hydrate, compromising product strength. Sample 1 contains less of both types of particles and consequently is a superior cement, even though Blaine ranks it the same as sample 2. So, the size distribution data are most certainly relevant.

Switching to laser diffraction
The practicalities of switching to laser diffraction are equally compelling. Laser diffraction, however, is fast and automated. In the lab this means greater productivity and better reproducibility. For processing it means on-line instrumentation and real-time measurement.

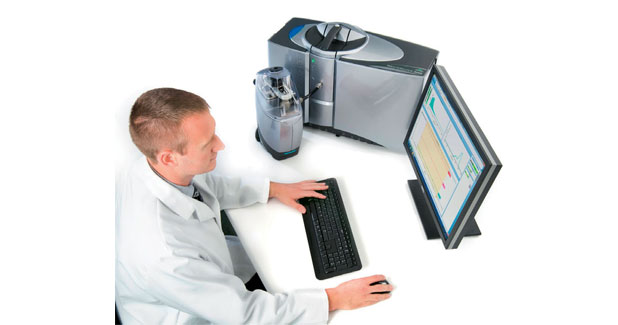
Malvern Mastersizer 3000 (Figure 2), which has a measurement range of 0.01 to 3500 microns, is an essential component of a high-quality cement laboratory. Finished products, as well as replacement material such as fly ash and blast furnace slag and fuels, have varying size distributions and so behavioral understanding and prediction requires Mastersizer analysis.

A vital element in successful laser diffraction particle size analysis is ensuring that samples are dispersed properly. In cement manufacture it is the primary particle size of a sample that is most usually the parameter of interest, rather than the size of any agglomerated material present. When using laser diffraction, samples can be dispersed and measured wet in the form of a suspension, or as dry powders. Dry dispersion, using dry compressed air, has a number of advantages, not least its obvious suitability for water sensitive material such as cement. It also avoids the need for solvent based dispersants and is rapid, thus increasing instrument productivity. The dry dispersion accessory, Aero S, available with Mastersizer 3000 has modular dispersion nozzles with different impaction surfaces. Keeping in mind that flow of abrasive material like cement for a prolonged period of time can cause damage to metal surfaces, there are options available for ceramic coated flow paths. It is worth highlighting the value of considering an analyzer that can switch easily between different samples with a minimum of fuss. Being able to change between different types of samples without fear of cross contamination, or to move simply or quickly from dry to wet measurement (or vice versa) as required, can make a real difference to analytical productivity, helping to maximize the return of investment in the system.

Finally, another important reason to switch to laser diffraction is the possibilities the technique offers for on-line analysis. Insitec systems deliver fully automated real-time analysis of cement particle size distribution from 0.1 to 2500 microns and can be configured to suit practically every process.

Conclusion
Whilst traditional Blaine measurements have served the cement industry well since the development of the Blaine method in the 1940s, the efficiency and quality of production of modern cements can be improved greatly by using Laser Diffraction technology. Efficient data acquisition, adaptable methods, and information-rich data explain the increasing use of the Malvern Mastersizer 3000 and Insitec range of systems in cement production around the world.

For more details, pls contact: Malvern Aimil Instruments Pvt. Ltd. Tel : 011-30810244 Fax : 011-26950011, Email : delhi@aimil.com


Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Concrete

Wonder Cement appoints Mahesh Singh as VP Corporate Brand Communication 

Published

on

By

Shares

Singh brings 20+ years of brand and marketing experience, and will lead integrated corporate brand communication initiatives at Wonder Cement 

New Delhi

Wonder Cement, a leading cement manufacturer, has appointed Mahesh Singh as Vice President – Corporate Brand Communication. In his new role, he will oversee corporate brand strategy and communication, including digital and performance marketing, public relations, trade, events, exhibitions, sports and experiential marketing. 

Singh brings over two decades of experience across marketing and communications, with roles spanning the automotive industry, agencies and entrepreneurship. He spent more than a decade with Honda Motorcycle & Scooter India, working across integrated communication, media, digital, retail and consumer engagement. His stint also included helping build the company’s digital marketing capabilities. 

He moved to dentsu X India as Vice President – Strategy & Planning, working across categories such as automotive, auto components, electric vehicles, FMCG, consumer electronics, BFSI, apparel and brand consulting. His responsibilities included media and marketing strategy, product launches, content, performance marketing and consumer activations. 

Singh subsequently took an entrepreneurial route with Radiant Brands before joining Shriram Ltd (SPR Autotech) as Head – Marketing & Communications. There, his remit included brand and corporate strategy, communications, PR and ORM, retail identity, loyalty programmes and events. 

At Wonder Cement, Singh will be responsible for bringing together the company’s corporate brand communication initiatives across digital, performance marketing, PR, trade, sports and experiential platforms. The role will focus on creating an integrated approach to communication across consumers, trade partners and other key stakeholders. 

The appointment brings to Wonder Cement a marketer whose career has spanned the brand, agency and entrepreneurial sides of the communications ecosystem. 

Wonder Cement, part of the RK Group, is a cement manufacturer with roots in Rajasthan and a focus on quality, trust and transparency. The company has grown to six manufacturing plants, and a cement capacity of 21.5 MTPA. With more than 2,000 employees and a network of over 5,000 dealers, its operations span manufacturing, distribution and customer engagement, with a focus on consistent product quality and efficient execution. 

Continue Reading

Concrete

JSW Cement commissions additional 1 MTPA grinding unit at Nagaur

Published

on

By

Shares

With this commissioning, JSW Cement’s total cement grinding capacity has increased to 25.10 MTPA, 
Mumbai

JSW Cement, one of India’s leading green cement producers and part of the diversified JSW Group, today announced the successful commissioning of an additional 1.00 MTPA cement grinding unit at Nagaur, Rajasthan. The commissioning marks another significant milestone in the Company’s growth strategy.

With this commissioning, JSW Cement’s total cement grinding capacity has increased to 25.10 MTPA, while its total clinker manufacturing capacity, including clinker capacity at its joint venture, JSW Cement FZC, stands at 9.74 MTPA.

JSW Cement had commenced operations in North India in March 2026 with the Nagaur Integrated Plant, comprising a 3.30 MTPA clinkerisation unit and 2.50 MTPA cement grinding unit. With the commissioning of the additional 1.00 MTPA cement grinding unit, the plant’s total cement grinding capacity has increased to 3.50 MTPA, enhancing the company’s ability to cater to the growing cement demand across Rajasthan, Haryana, Punjab and the National Capital Region (NCR). The expansion has been funded through a strategic mix of equity and long-term debt.

During the quarter ended 30th September 2026, JSW Cement has also commissioned the Alternate Fuel Handling System and the Waste Heat Recovery system (WHRS) at the Nagaur Integrated Plant.

Nilesh Narwekar, CEO, JSW Cement, said: “The commissioning of additional 1.00 MTPA grinding capacity at Nagaur is a key strategic priority for us and will accelerate JSW Cement’s expansion into North India. We look forward to servicing the growing needs of the region and contributing to the economic growth of Rajasthan, Haryana, Punjab and the NCR area. I am delighted to share that the company has commissioned this grinding unit within the expected timeline, showcasing our project execution capabilities. Further, the Alternate Fuel Handling System and the Waste Heat Recovery system (WHRS) are expected to substantially reduce our production costs going forward.”

Continue Reading

Concrete

UltraTech becomes first Indian cement firm to cross 2 GW green energy

Published

on

By

Shares

UltraTech Cement has crossed 2 GW of captive green energy capacity, with renewables and waste heat recovery meeting 48 per cent of its power needs.

Mumbai

UltraTech Cement Limited has surpassed 2 GW of installed green energy capacity for captive use, becoming the first cement company in India to achieve the milestone. The Aditya Birla Group company commissioned 116.55 MW of wind capacity at its Inter-State Transmission System-connected wind-solar hybrid project in Barmer, Rajasthan, along with 10 MW of Waste Heat Recovery System capacity at Sarlanagar Cement Works in Karnataka.

With these additions, UltraTech’s cumulative installed green energy capacity has reached 2,024 MW. This includes 1,580 MW of renewable energy capacity and 444 MW of waste heat recovery capacity, together meeting around 48 per cent of the company’s current power requirements.

The company said the milestone reflects the progress of its long-term energy transition strategy. In FY27 so far, nearly one-third of UltraTech’s 76 manufacturing units in India have maintained green energy utilisation above 50 per cent of their electricity requirements, while five units have crossed 95 per cent.

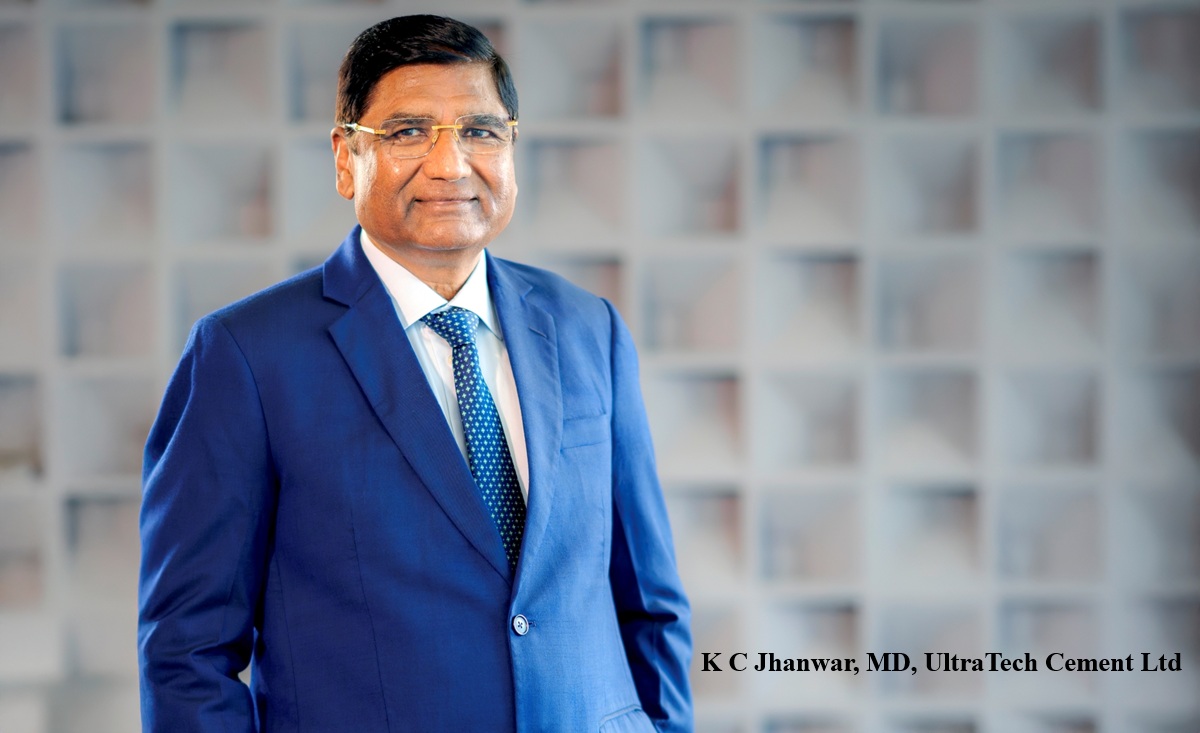
K C Jhanwar, Managing Director, UltraTech Cement Limited, said, “Crossing the 2 GW green energy milestone is the result of a strategy we have pursued consistently over the past decade. Cement is an energy-intensive, hard-to-abate sector, and showing that reliability and growth can go hand in hand with a rapid shift to green energy sets a benchmark for the industry. With nearly half of our power needs now met through green energy, we are significantly less exposed to fossil fuel supply constraints and power price volatility. As we scale up renewables, waste heat recovery and battery storage across our operations, we are building an energy foundation for stable, long-term growth.”

UltraTech commissioned 430 MW of green energy capacity in FY26 and continues to expand its renewable energy and waste heat recovery portfolio.

The company is also progressively integrating Battery Energy Storage Systems across its operations to improve renewable energy utilisation and supply reliability.

In 2025, UltraTech operationalised what it described as India’s first on-site hybrid round-the-clock renewable energy project at Sewagram Cement Works in Gujarat. The project combines solar, wind and battery storage.

As part of its decarbonisation strategy, UltraTech said it has not invested in new captive thermal power capacity for either greenfield projects or brownfield expansions at its integrated units for more than a decade.

The company said its expanding green energy portfolio is helping reduce dependence on conventional grid electricity and fossil fuel-based power, while lowering exposure to fluctuations in coal and electricity prices.

UltraTech aims to increase green energy’s share in its total power mix to 85 per cent by 2030. As a member of RE100, it has also committed to meeting 100 per cent of its electricity requirement through renewable sources by 2050.

UltraTech Cement, the cement flagship of the Aditya Birla Group, has a total grey cement capacity of 210.1 MTPA and white cement and putty capacity of 3.5 MTPA. The company is also a signatory to the GCCA Climate Ambition 2050 and has committed to the GCCA Net Zero Concrete roadmap.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds