Economy & Market
“The challenge is to move cement from the warehouse to the consumer?s site”
Published
12 years agoon
By
admin
Rohit Vohra Head Logistics, Reliance Cement
The total cost of logistics considering inbound and outbound movement can come up to 20 to 25 per cent of cement production cost. This is for companies having good infrastructure such as rail sidings, etc., and who transport 40 to 60 per cent product by rail. For companies that do not have such facilities, the cost can go as high as 30 per cent of the cement cost. Rohit Vohra highlights the challenges faced by cement companies in last mile deliveries. Excerpt from the interview.
How much is the cost contribution of logistical expenses to cement cost?
The cost of transporting cement via road comes to about Rs 1 to 3 /tonne/km. The wide range is due to the variation in lead distance, which can range from anywhere between 50-300 km. Longer the distance, lower is the cost of transport. Railway on other hand costs Rs 1.3 to 1.4/tonne/km. However, railway has additional fixed costs related to loading and unloading.
The handling cost is high for railways. So for a distance below 200 km rail is not viable. We generally outsource the unloading process to the C&F agents.
What are the losses experienced in cement transport via rail wagons?
Railways charge a fixed fare based on the number of wagons employed. If the wagon is not loaded completely, the company will still end-up paying for the entire wagon. One area where cement is lost is due to spillage from torn or damaged bags. Many a times the floor of the wagon is in bad constitution and may have sharp edges that damage the cement bags during transit. To minimise such loss we are using specialised packing material for our cement bags. These bags are not lifted using metal hooks. Instead the workers put a sort of wire loop around it and pick it up. Although the cost of loading and unloading too gets escalated with this, the end customer gets quality cement in quality packing.
What are the challenges faced by cement companies in last mile delivery?
The challenge in last mile delivery is that today we have lesser number of stockists. Now nobody wants to stock cement in warehouses. The rental charges of warehouses are too high for stocking a low margin product like cement. So dealers prefer ordering the material straight from the plant to the consumer site.
Now consumers require quick delivery, and on several occasions the delivery is to be made in congested city areas. These locations often have limitations on the size of trucks that could ply on the roads. Hence, we have to use smaller vehicles, which are cost inefficient. Companies then have to set up a very good network of warehouses close to the market so as to be able to reach the customer as quickly as possible. But again, setting up a warehouse means additional loading and unloading at the company?s expense. The moment you create an additional node in your supply chain, the cost of handling and distribution goes up. Plus, dispatch from these warehouses is also costly since transporters are moving material over short distances. So the cost of transport per tonne per km is high.
What are the constraints that you have to deal with in cement transport?
We put cement delivery process in two buckets. One is from plant to the warehouse and the other is where we transport cement from warehouse to the site. When we are moving cement from the plant to the warehouse we have the loading and unloading process and the associated cost in our control. The material is transported in multi-axle carriers with a capacity of around 27 tonnes. Mostly the approach road to the warehouse is good and the time required to load and unload is fixed and short. So here the costs are very much in the company?s control.
The challenge is to move cement from the warehouse to the consumer?s site. Many cities have restrictions on the size of trucks that can move round the clock. Cities like Nagpur, Bhopal, etc., do not allow trucks with more than 8-tonne capacity to ply on the roads. While at some places like Rajasthan, where highways are good we transport cement in 60-tonne trailers. Often the size of order placed by end consumers is small and we have to dispatch 4-5 tonnes of material.
Today the customers to want delivery of cement as and when required. They usually do not have space to store cement and other construction materials. Storing cement is a hassle and implies additional cost. Simply handling a cement bag costs Rs 2-3 and so everyone tries to avoid it. The traders to want the cement to be delivered directly from company warehouse to the site, not to the shop.
What can be done to cut down that cost?
We have a system where dealers can order at ex-warehouse price and can arrange for their own vehicle. That creates a synergy since the dealer can ship other items such as steel, paint, bricks, etc., in the same truck.
How about outsourcing this function?
We have been considering outsourcing this function. However, service providers do not find cement transport as profitable as they would find transporting high value retail products like electronic goods, etc. In cement the margins are low, and so it is less attractive to external logistics service providers.
Railways have plenty of surplus land, however they do not have clear policy for land allotment. Most major companies have their own cement siding. What the industry needs is rail side warehouses. We are looking for opportunities to set up terminals close to siding. Having a rail side warehouse minimises cost of product handling.
How to you manage the fluctuations in cement demand?
There are basically two types of fluctuations, the seasonal and the demand driven. Seasonal changes are seen in the trade segment while demand driven fluctuations are seen in non-trade segment. We have kept a balance of having trade to non-trade segment in 70:30 ratio. That stabilises the demand pattern.
The industry generally experiences good demand during the October-June period. This is the time when the company builds up reserve stock of cement at the plant. The industry experiences low demand during the July-August period. During this period we conduct operation and maintenance tasks at the plant.
Major fluctuations are taken care by the surplus stocks at the plant while minor fluctuations are dealt with at the warehouse level.
You may like
Concrete
ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown
Published
1 week agoon
November 12, 2026By
admin
ABB reconditions 25 drives at ACC’s Jamul cement plant, avoiding 16 tonnes of CO₂ emissions while improving reliability through predictive maintenance.
Chhattisgarh
ABB has signed a multi-year Motion OneCare service agreement with ACC Limited, part of the Adani Group, to modernise ageing industrial drives at its Jamul cement plant in Chhattisgarh, improving operational reliability while avoiding approximately 16 tonnes of carbon dioxide (CO₂) emissions without disrupting production.
Announced on 27 October 2026, the agreement combines scheduled drive reconditioning, digital condition monitoring and energy appraisals to extend equipment lifespan, improve plant uptime and optimise maintenance costs. The initiative marks a shift from conventional equipment replacement towards a more resource-efficient approach to industrial asset management.
The first phase, completed in April 2026, involved the on-site reconditioning of 25 ABB ACS800 variable speed drives without a major plant shutdown. By retaining the existing cabinets and restoring the drive modules rather than replacing entire panels, ABB helped ACC preserve capital investment, minimise material consumption and avoid approximately 16 tonnes of CO₂ emissions.
A second phase, covering an additional 25 ACS800 drive modules, is scheduled for the fourth quarter of 2026. The programme is designed to improve long-term equipment reliability while allowing maintenance activities to be aligned with the plant’s operational schedules.
The ACS800 drives, installed at Jamul in 2010, had delivered more than a decade of near-continuous service in demanding cement manufacturing conditions. However, ageing electrical components and changing fault patterns had begun to affect their ability to meet the plant’s reliability requirements.
Rather than opting for complete equipment replacement, ACC engaged ABB’s certified engineers to conduct a comprehensive asset health assessment. The evaluation found that the existing cabinets and enclosures remained structurally sound, making targeted reconditioning a technically viable and cost-effective alternative to full replacement.
Drawing on nearly two decades of experience with ACC’s equipment and operating requirements, ABB developed a maintenance framework tailored to the plant’s shutdown windows, budget cycles and production priorities.
The Motion OneCare agreement incorporates planned equipment restoration, condition-based monitoring and energy assessments, enabling ACC to adopt a more systematic approach to maintaining critical electrical infrastructure.
As part of the programme, ACC has implemented ABB Ability™ Digital Powertrain Insights to monitor drive performance and identify emerging operational issues before they result in equipment failures.
The digital platform provides continuous visibility into parameters such as temperature, current, vibration and fault patterns. These insights allow maintenance teams to detect early signs of equipment deterioration, schedule interventions more effectively and reduce the likelihood of unexpected downtime.
Amit Gupta, Local Division Manager, Motion Services, ABB India, said: “We know what unchecked wear costs over time: a small inefficiency that eats away at ROI for years. At Jamul, the evidence pointed clearly to assets with productive life still in them.”
“Our job was to restore them properly and give the team the tools to stay ahead of the next problem. At ABB, we don’t just fix what fails. We want to protect what works.”
The initiative also demonstrates the growing relevance of circular economy principles in cement manufacturing, where extending the service life of existing industrial equipment can reduce capital expenditure, material consumption and the environmental impact associated with manufacturing replacement components.
According to ABB, drive reconditioning can reduce lifecycle emissions by 50 to 80 per cent compared with complete equipment replacement. By preserving functional components and restoring critical modules, the process helps retain the economic and material value of existing industrial assets.
The addition of energy appraisals in subsequent phases will further expand the programme beyond equipment restoration, enabling ACC to assess drive performance, identify energy-saving opportunities and improve operating efficiency.
For cement manufacturers, variable speed drives play an important role in controlling motors and optimising energy consumption across production processes. Maintaining their reliability and efficiency is essential for minimising operational disruptions and managing electricity costs.
Vinod Bahety, CEO – Cement Business, Adani Group, said: “Moving from reactive firefighting to a structured maintenance plan was exactly what this operation needed. That kind of peace of mind doesn’t come easily. It comes from a partner that understands how your business runs.”
“We didn’t need a full system overhaul; we needed expert support, actionable insights, and a plan we could execute around our schedule. That’s what we got.”
The project supports ACC’s broader strategy to improve manufacturing efficiency through digital transformation, preventive maintenance and sustainable asset management.
ACC, a subsidiary of Ambuja Cements and part of the Adani Group, operates 20 cement manufacturing facilities and 119 ready-mix concrete plants across India. The company has been advancing initiatives focused on renewable energy, circular economy practices and technology-driven operational improvements.
Alongside Ambuja Cements, ACC is part of a large-scale building materials business committed to achieving net-zero emissions by 2050, with near-term and net-zero targets validated by the Science Based Targets initiative (SBTi).
The Jamul initiative aligns with these sustainability objectives by demonstrating how equipment life extension and digital monitoring can contribute to resource efficiency without requiring large-scale replacement of existing infrastructure.
ABB, a global technology company specialising in electrification and automation, brings more than 140 years of industrial expertise and employs approximately 110,000 people worldwide. Its Motion Services business supports industrial customers through equipment maintenance, modernisation, digital monitoring and lifecycle management solutions.
The agreement also reflects a wider shift in industrial maintenance practices, with manufacturers increasingly adopting predictive technologies to improve equipment availability, manage costs and reduce unplanned shutdowns.
With 25 drives already reconditioned and another 25 scheduled for restoration, ABB’s collaboration with ACC illustrates how targeted modernisation, digital monitoring and circular maintenance practices can extend the operational life of critical equipment while supporting more efficient and sustainable cement production.
Concrete
ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K
Published
1 week agoon
November 12, 2026By
admin
ABB deploys advanced process control at TCI MAX’s Srinagar cement plant to improve clinker quality, energy efficiency and sustainable manufacturing.
Kashmir
ABB has deployed its advanced process control technology at TCI MAX Cement’s Srinagar facility in Jammu and Kashmir, marking the region’s first reported implementation of advanced process control (APC) in cement manufacturing and strengthening efforts towards more efficient, digitally enabled production.
Announced on 5 November 2026, the deployment of ABB Ability™ Expert Optimizer at the facility, operated by Trumboo Industries Pvt. Ltd., aims to improve process stability, clinker quality, energy efficiency and overall plant productivity. The implementation forms part of TCI MAX’s strategy to modernise its manufacturing operations through automation and digital technologies.
Following the integration of ABB’s advanced process control solution and supporting IT infrastructure, TCI MAX has reported improvements in operational productivity, product quality and sustainability-related performance indicators. The technology focuses on optimising the cement pyro process, a critical stage of production involving high-temperature processing and clinker formation.
Waseem Ahmed Trumboo, Director, Trumboo Industries Pvt. Ltd., said: “Introducing advanced process control at TCI MAX is an important step in how we are evolving our operations. Our focus is on improving the stability and efficiency of our processes while maintaining consistent clinker quality. We have been encouraged by the performance of the solution during commissioning and by the support from the ABB team, and we look forward to realizing its full potential.”
ABB Ability™ Expert Optimizer combines advanced process control, model predictive control (MPC) and artificial intelligence (AI) to continuously monitor and optimise manufacturing operations. By analysing process conditions, predicting operational behaviour and automatically adjusting key parameters, the system enables more consistent production while reducing process variability.
In cement manufacturing, maintaining stable pyro-processing conditions is essential for achieving uniform clinker quality and optimising thermal energy consumption. Fluctuations in operating parameters can affect fuel efficiency, production output and product consistency.
The deployment is designed to address these challenges through real-time process optimisation, helping operators maintain more stable kiln operations while improving the utilisation of fuel, electricity and raw materials.
Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries Division, ABB India, said: “Cement producers are increasingly looking to adopt digital technologies to achieve greater consistency and efficiency while addressing their sustainability priorities. ABB Ability™ Expert Optimizer brings advanced process control and deep cement process expertise together to help operators make their processes more stable and efficient. We are pleased to support TCI MAX as it takes this important step in its digital transformation.”
The technology also supports sustainability objectives by optimising fuel consumption, improving electrical energy efficiency and minimising process waste. More stable operations can contribute to lower energy intensity and reduced emissions associated with cement production.
For TCI MAX, the investment represents a move towards data-driven manufacturing, where automated control systems complement operator expertise to improve production performance and operational reliability.
The implementation is particularly significant for Jammu and Kashmir’s cement industry, as it introduces advanced process optimisation technology to a regional manufacturing facility. Its deployment could demonstrate the potential for wider adoption of digital automation across cement plants seeking to modernise their operations.
The project builds on ABB’s experience in delivering advanced process control solutions to cement manufacturers worldwide. Through the integration of industrial automation, predictive technologies and process engineering expertise, the company supports manufacturers in improving resource efficiency and maintaining consistent production quality.
As cement producers face increasing pressure to manage energy costs, improve productivity and reduce their environmental footprint, technologies such as AI-enabled process control and predictive optimisation are becoming important components of plant modernisation strategies.
ABB’s Expert Optimizer provides a platform for addressing these priorities by enabling automated adjustments based on changing process conditions, reducing reliance on manual intervention and supporting more efficient plant operation.
ABB, a global technology company specialising in electrification and automation, has more than 140 years of industrial experience and approximately 110,000 employees worldwide. Its Automation business employs around 26,000 people and provides technologies and services across process, hybrid and maritime industries.
The TCI MAX deployment reinforces ABB’s growing role in the digital transformation of cement manufacturing in India, where improving process efficiency and reducing energy consumption remain critical to the industry’s long-term sustainability.
With the advanced process control system now implemented at its Srinagar facility, TCI MAX aims to build on the initial operational improvements and further optimise production efficiency, clinker consistency and environmental performance.
Concrete
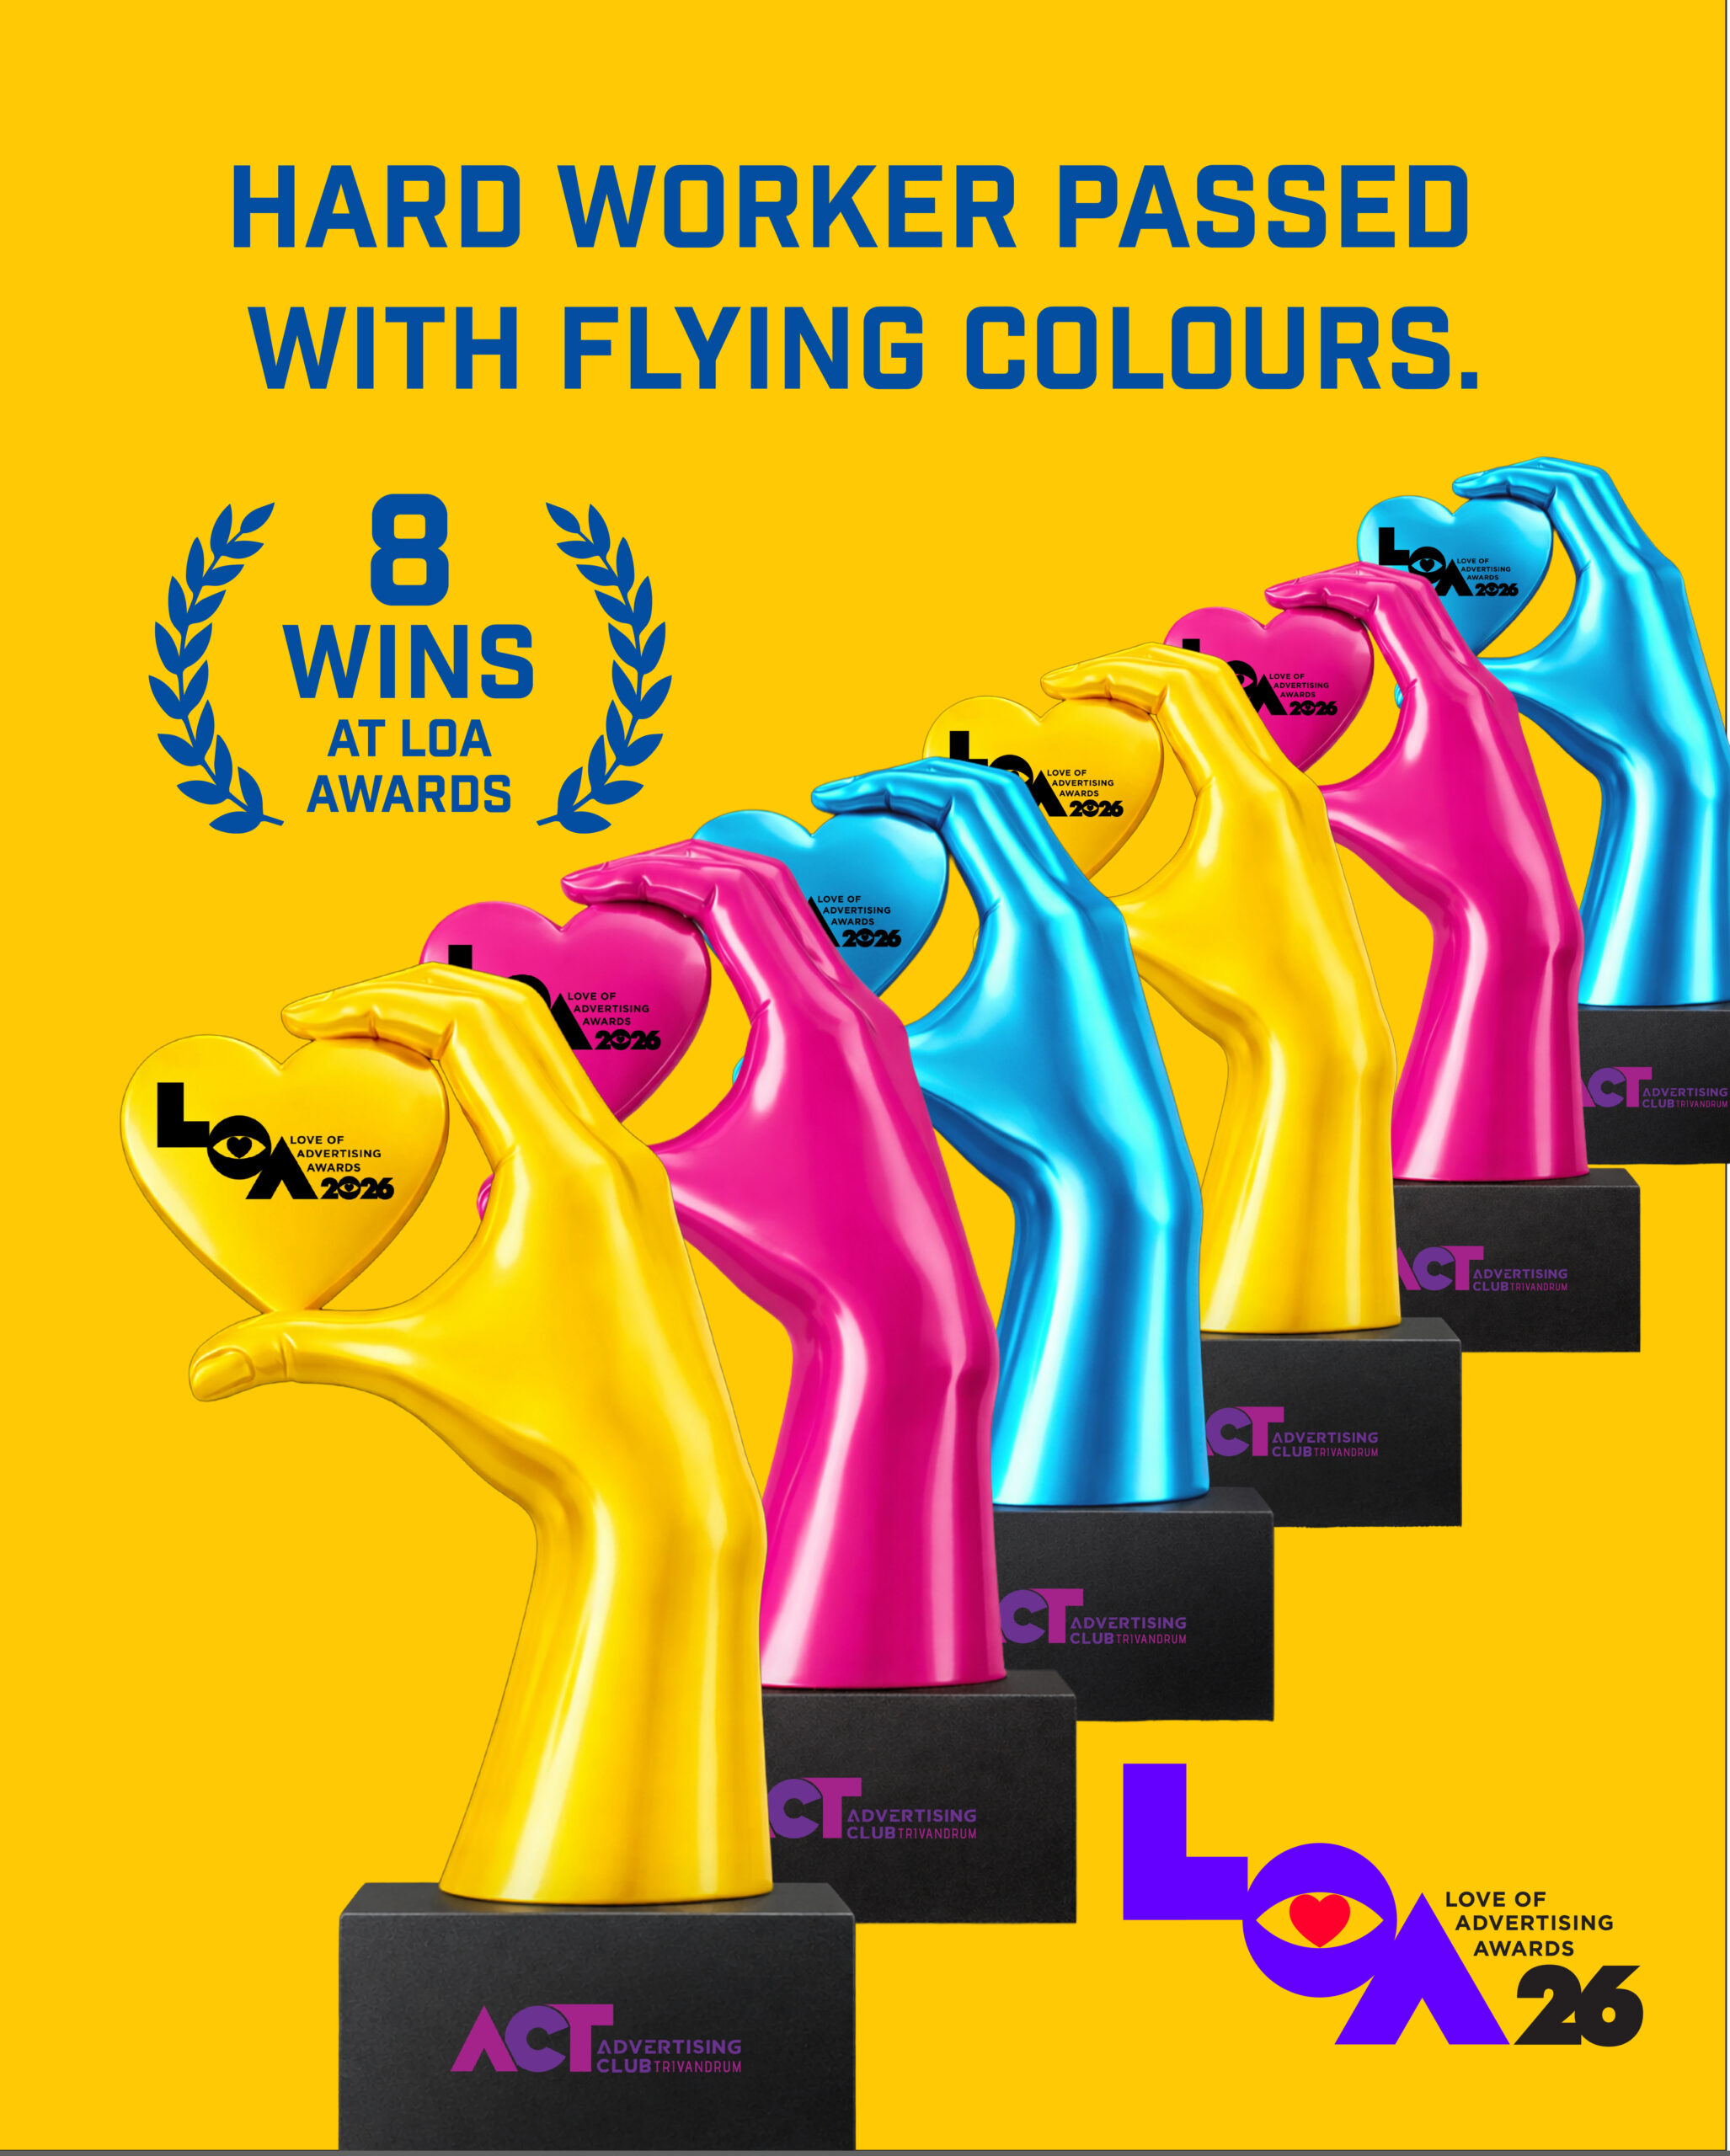
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’
Published
1 week agoon
November 12, 2026By
admin
Ramco Cements’ Hard Worker brand wins eight awards for excellence in advertising, packaging and brand identity at the Love of Advertising Awards 2026.
Hyderabad
The Ramco Cements Limited’s construction chemicals brand, Hard Worker, has secured eight awards at the Love of Advertising Awards 2026, recognising its creative excellence across television, digital advertising, packaging design and brand identity.
Organised by the Advertising Club of Trivandrum, the awards were presented at a ceremony held at The Leela Raviz, Kovalam, on 24 October 2026. The recognition highlights Hard Worker’s integrated marketing strategy and its efforts to establish a distinctive presence in India’s competitive construction chemicals market.
The eight awards span multiple creative categories, reflecting the brand’s approach to combining product-focused communication with engaging storytelling, humour and innovative design. Through its campaigns, Hard Worker has sought to simplify technical product benefits and make construction chemicals more accessible and relatable to consumers and construction professionals.
Built around the philosophy of “Hard-working products for hardworking people”, the brand focuses on communicating practical product advantages through memorable advertising narratives while maintaining a consistent identity across different marketing platforms.
Its campaigns for Ramco Hard Worker Eco Plaster and Tile Fix have been central to this approach. The Eco Plaster campaign highlights water conservation through the product’s self-curing properties, positioning it as a solution that supports more efficient construction practices. Meanwhile, Tile Fix promotes specialised tile-fixing solutions by presenting their practical benefits through relatable situations and creative storytelling.
Beyond advertising, Hard Worker has invested in distinctive packaging and brand identity development to improve product recognition and maintain consistency across customer touchpoints. This integrated approach has helped the brand differentiate itself in a category where marketing communication has traditionally focused on technical specifications and functional performance.
A V Dharmakrishnan, CEO, Ramco Cements, said, “Winning eight awards at the Love of Advertising Awards is a proud moment for Ramco Cements and the Hard Worker team. We believe that building a strong brand requires not only quality products but also the ability to communicate their value in a compelling and differentiated manner. Hard Worker’s journey reflects our commitment to combining product performance with innovative marketing to create meaningful connections with our customers and strengthen our presence in the construction chemicals market.”
The recognition comes as building materials manufacturers increasingly focus on brand differentiation, product awareness and customer engagement to strengthen their position in the construction chemicals segment.
By using humour and storytelling to explain product applications and benefits, Hard Worker aims to bridge the communication gap between technical construction solutions and the practical requirements of contractors, applicators and end-users.
Balaji K. Moorthy, Executive Director – Marketing, Ramco Cements, said, “Hard Worker was conceived to bring a fresh perspective to the construction chemicals category, where product communication has traditionally been functional and technical. Our endeavour has been to break through the clutter with distinctive ideas, humour and storytelling, while keeping the product proposition at the heart of every campaign. The recognition across TV and digital advertising, packaging design and brand identity design demonstrates our integrated approach to building the brand. These eight awards are an encouraging recognition of the creative thinking and collaborative effort behind Hard Worker’s marketing initiatives.”
The awards add to Hard Worker’s growing portfolio of creative recognitions and reinforce Ramco Cements’ emphasis on integrating product innovation with strategic marketing.
The brand’s communication initiatives also reflect a wider shift in the construction materials industry, where manufacturers are increasingly adopting consumer-focused marketing strategies to improve product understanding and strengthen relationships with construction professionals.
With its portfolio of construction chemicals, Hard Worker aims to address evolving requirements for durability, application efficiency and construction quality. Its marketing efforts seek to complement these product attributes by building stronger awareness and encouraging the adoption of specialised construction solutions.
Ramco Cements, one of India’s established cement manufacturers, operates across cement and allied building solutions. Through Hard Worker, the company is expanding its presence in the construction chemicals segment with products designed to enhance performance, quality and durability in modern construction applications.
The latest recognition strengthens Hard Worker’s brand visibility and underscores the growing importance of creative communication in promoting technical building materials. Ramco Cements intends to continue combining product development with distinctive marketing initiatives to support the brand’s growth in India’s construction chemicals market.
NCL Industries Approves Rs. 5.95 bn Solar-Wind Investment
Cement Makers See Margin Relief as Oil Prices Lower Fuel Costs
ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown
ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’
NCL Industries Approves Rs. 5.95 bn Solar-Wind Investment
Cement Makers See Margin Relief as Oil Prices Lower Fuel Costs
ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown
ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’
Trending News
-
Concrete4 weeks agoNuvoco reports 13.5% revenue growth in Q2 FY27
-
Concrete4 weeks agoUltraTech Cement Expands in Andhra Pradesh with Rs. 26.5 bn
-
Concrete3 weeks agoCII Calls for Greater Alternative Fuel Use in Cement Industry
-
Concrete2 weeks agoShree Cement Expands Bangur Concrete Network with Patna Plant