

Concrete
Evolving with Time


Concrete and precast shapes are playing an increasingly important role in the construction sector today. We look at the challenges and innovations in this segment.
The journey of precast concrete has been long. Joseph Aspdin patented the making of Portland cement in late 1700 and much later Joseph Monier was the first to use reinforced concrete in 1867. He went on to patent concrete pipes, basins, beams and panels. These panels proved to be the precursor to precast concrete production for construction. In 1905, city engineer John Alexander Brodie invented the first modern example of precast concrete in Liverpool, England. Although precast concrete forming of panels wasn’t popular in England, it flourished around the world.
Advances in the precast concrete industry continue to make the material indispensable. In addition to precast/prestressed concrete structural members that keep parking garages and bridges upright, it’s the concrete used underground that make it so valuable.
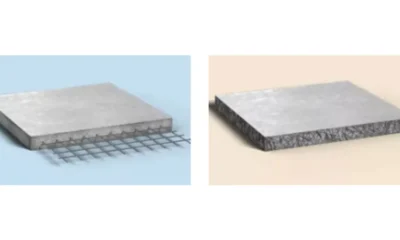
Precast concrete is a construction product produced by casting concrete in a reusable mould or ‘form,’ which is then cured in a controlled environment, transported to the construction site and maneuvered into place. Examples include precast beams, and wall panels for tilt-up construction. In contrast, cast-in-place concrete is poured into site-specific forms and cured on site. Recently lightweight expanded polystyrene foam is being used as the cores of precast wall panels, saving weight and increasing thermal insulation.
Precast concrete is employed in both interior and exterior applications, from highway, bridge and hi-rise projects to tilt-up building construction. By producing precast concrete in a controlled environment (typically referred to as a precast plant), it is afforded the opportunity to properly cure and be closely monitored by the plant employees. Using a precast concrete system offers many potential advantages over onsite casting. Precast concrete production can be performed on ground level, which maximises safety in its casting. There is greater control over material quality and workmanship in a precast plant compared to a construction site. The forms used in a precast plant can be reused hundreds to thousands of times before they have to be replaced, often making it cheaper than onsite casting in terms of cost per unit of formwork.
Precast concrete forming systems for architectural applications differ in size, function and cost. Precast architectural panels are also used to clad all or part of a building facade or erect free-standing walls for landscaping, soundproofing and security. In appropriate instances precast products – such as beams for bridges, highways and parking structure decks – can be prestressed structural elements. Stormwater drainage, water and sewage pipes as well as tunnels also make use of precast concrete units.
Precast concrete moulds can be made of timber, steel, plastic, rubber, fibreglass or other synthetic materials, with each giving a unique finish. In addition, many surface finishes for the four precast wall panel types – sandwich, plastered sandwich, inner layer and cladding panels – are available, including those creating the looks of horizontal boards and
ashlar stone. Colour may be added to the concrete mix, and the proportions and size aggregate
also affect the appearance and texture of finished concrete surfaces.
Some of the examples of precast concrete products and shapes are given below:
Precast concrete products for foundations
Isolated footings: They are commonly used for shallow foundations to carry and spread concentrated loads, caused for example by columns or pillars. Isolated footings can consist either of reinforced or non-reinforced material. These are used for smaller structures and residential buildings.
Pocket footings: They offer more strength to shallow foundations to carry and spread concentrated loads. They are used for commercial and
industrial buildings.
Combined footings: These concrete footings are usually rectangular and support two or more columns that are so close to each other their footings would overlap. They are used for commercial and industrial buildings.
Precast piles: They are prefabricated piles made of prestressed concrete that are driven into the ground using diesel or hydraulic hammer. The piles are made of prestressed concrete and have fixed dimensions. These piles are used for the most conventional foundation method.
RCC beams: These are structural elements designed to carry transverse external loads that cause bending moment, shear forces, and in some cases torsion across their length. RCC beams generally have concrete resisting on the compression region and steel resisting applied loads on the tension region. It can be classified as per size into- rectangular, T-Beam, I-Beam, Circular Beam and L-Beam. It is used to support the building’s floors, roof, walls
and cladding.
Prestressed beams: FRP-prestressed beams are greater than those of steel-prestressed beams.
It is very easy to install with reduced on-site labour needs and costs. It comes in a wide range of depths to meet exact building needs It provides much-needed reinforcement for multi-story buildings and industrial applications.
Shell beams: Shell beams are commonly used with precast floor systems to streamline building programmes and reduce on-site labour. Pre-stressed shell beam units, with the addition of a reinforcing cage and on-site concrete. Band depths of 290mm to 600mm and widths of 600mm to 2,400mm are possible.
RCC slabs: This type of slabs is used for support conditions in buildings. RCC slabs, with thickness that ranges from 10 to 50 centimetres, are most often used for the construction of floors and ceilings. Thin RCC slabs are also used for exterior paving purposes. In domestic and industrial buildings, a thick concrete slab, supported on foundations or directly on the subsoil, is used to construct the ground floor of a building. In high rises buildings and skyscrapers, thinner, precast concrete slabs are slung between the steel frames to form the floors and ceilings on each level.
Prestressed hollow core slabs: A hollow core slab, also known as a voided slab, hollow core plank, or simply a concrete plank is a precast slab of prestressed concrete typically used in the construction of floors in multi-story apartment buildings. The production of these elements is achieved using our Extruder and Slipformer machines that cast in one phase along a production bed without the need for any formworks.
Prestressed solid slabs: The solid slab is a customised, loosely reinforced, full concrete slab that is used in residential and industrial construction. Mounting parts, such as electrical outlets, wiring, openings, etc. or even heating conduits can be previously installed in the solid slab in the precast plant.
Double tee slabs: A double tee or double-T beam is a load-bearing structure that resembles two T-beams connected side by side. The strong bond of the flange (horizontal section) and the two webs (vertical members, also known as stems) creates a structure that is capable of withstanding high loads while having a long span. It can be applied in roofing, parking and bridges.
Precast concrete products for walls
Load bearing external walls: This wall is constructed to support the above slab or other building elements in a structure. These walls are generally 125 mm to 200 mm thick. The thickness depends on the load pattern.
Non-load-bearing walls: This wall holds up only itself as it carries only its own weight and may be any one of the types discussed under load-bearing walls. This type of wall is used to close in a steel or concrete frame building. It is usually carried by supports, normally steel shelf angles on each floor. These walls are generally 50 mm to 100 mm thick.
Precast joist roof
Precast joist roof is a building system in which precast reinforced cement concrete planks – rectangular slab elements – are placed on precast RCC joists. The roof gets completed with in-situ concrete poured over the haunches in planks and over the partially precast joists, thus ensuring monolithic action of individual precast elements.
Precast façade
Precast sandwich panels enable the strict requirements for thermal insulation to be met. Concrete structures have great insulation qualities, keeping the building warm in cold weather and cool when it is hot, stabilising the moisture and temperature inside. For the precast facade, a calculated age can be defined. One special feature of a precast façade is the panel joints
Glass Fibre-Reinforced Concrete (GFRC)
Glass fibre-reinforced concrete consists of high-strength, alkali-resistant glass fibre embedded in a concrete matrix. This is used especially for thin architectural cladding panels, but also for ornamental concrete such as domes, statues, planters and fountains. Recently, decorative concrete artisans have discovered the benefits of GFRC for decorative panels (such as fireplace surrounds), concrete countertops and artificial rock work.
Some of the advantages of precast concrete and shapes over in-situ concrete are as follows:
Simplified Material Inputs and Cost: Because precast products already contain the concrete, conduits and rebar needed, they eliminate the need to purchase and prepare these materials. Offsite casting also removes onsite casting needs, such as cardboard forms, from the equation. This simplifies the construction process to reduce hassle and
increase efficiency.
Reduced Installation Time: Precast concrete components are ready for immediate use upon delivery while cast-in-place concrete are not. This eliminates unnecessary time needed to set up cardboard forms, bend and position rebar, pour and vibrate concrete and then wait for the concrete to cure. The removal of these steps saves valuable time in terms of project duration and cost from labour needed.
Cost-effective for Large Projects: When compared to cast-in-place concrete, the cost associated with precast concrete decreases as project scale increases. Large-scale projects that require repeatable concrete components, such as installing airport taxiway lighting, are great candidates for precast concrete products, as the setup and install time required to hand pour all concrete would quickly increase project cost. Precast concrete is truly an economy of scale, which makes it ideal for businesses and contractors of large-scale construction projects.
Stronger than Cast-in-place Concrete: Precast concrete is often stronger than cast-in-place concrete. Not only are precast concrete products already reinforced with steel rebar, but the controlled curing process also ensures that the concrete will set correctly under ideal conditions for maximised strength. Precast concrete can also be stress-tested before being delivered to the final job site.
Higher-quality Control: Another advantage of precast concrete is its higher standard of quality control. Because precast concrete forms are created offsite, all products are inspected for defects before shipping out. The controlled process also eliminates unknowns related to temperature, humidity and imprecise tools.

However, there are some challenges as well that must be taken care of as follows:
Higher Upfront Costs: The good news is precast concrete makes up for the high initial costs in the long run. Because concrete is so strong and durable, there is typically very little maintenance over the life of the precast concrete fence.
Transportation: If your project site is located far away from our plant, the transportation can take a while and cost more. Precast concrete isn’t fine China. Some bumps and bruises aren’t going to hurt it. But you will need to be prepared when installing the precast shapes.
Hard to Modify: Precast concrete has a ton of options during design phase but once designed and built it is not possible to modify in part or whole.
The market for precast products and shapes have been growing very fast and because of the nature of customisation possibilities it is likely to be the product of choice for not only government projects but also for residential construction.
-Procyon Mukherjee







Concrete
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement has deployed more than 70 EVs across its logistics network.





Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027

JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant

Martin Engineering Appoints Ashwini Khunte as India General Manager

CII Calls for Greater Alternative Fuel Use in Cement Industry
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027
JK Lakshmi Cement Breaks Ground on Rs 110 bn Assam Plant
Martin Engineering Appoints Ashwini Khunte as India General Manager







