Sanjeev Arora, President – Motion Business & IEC LV Motors Division, ABB India, discusses efficient drive powertrain technology for cement manufacturing, which is powering India’s next phase of sustainable growth.
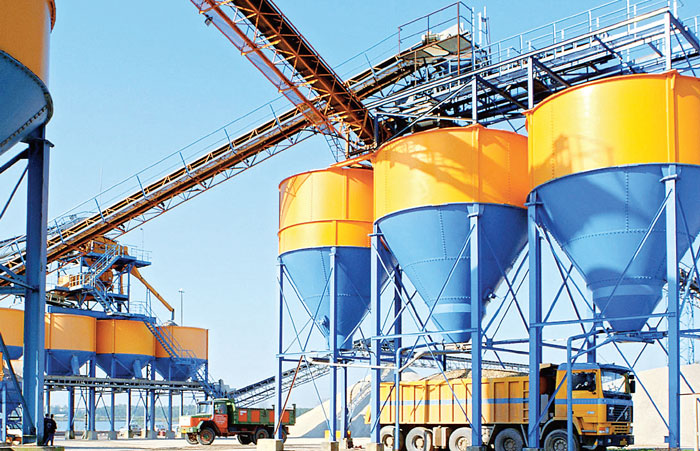
India’s growth story is being written at an unprecedented scale. From highways and airports to smart cities, metros, renewable energy parks and industrial corridors, infrastructure development is accelerating rapidly. At the heart of this transformation lies one of the country’s most foundational industries – cement. India is already the world’s second largest cement producer, and demand is expected to rise significantly over the next decade as investments in urbanisation, housing, manufacturing and public infrastructure continue to expand. However, the cement industry also finds itself at a defining crossroads. It must scale production while simultaneously reducing emissions, improving efficiency, strengthening reliability and ensuring operational excellence.
This is where technology will play a decisive role. For decades, motors and drives have quietly powered every stage of cement manufacturing, from crushers, kilns and conveyors to mills, fans and packing units. They have become strategic enablers of sustainability, digitalisation, safety and profitability. The future of cement manufacturing will be defined by plants that are not only more productive, but also more intelligent, energy efficient and resilient.
In many ways, the journey toward a leaner and cleaner cement industry begins with how motion systems are designed, monitored and optimised.
Decarbonising cement
A substantial share of electricity consumption within a cement plant comes from motor driven systems such as fans, pumps, compressors, conveyors and grinding mills. Globally, electric motors account for nearly 45 per cent of the world’s electricity consumption in industrial applications. This makes energy efficient motor systems one of the fastest and most impactful levers available for decarbonisation.
In India, where industrial energy demand continues to grow alongside economic expansion, improving motor efficiency can create meaningful environmental and business outcomes. Replacing IE2 motors with high efficiency IE4 and IE5 motors, combined with variable speed drives (VSDs), can significantly reduce energy consumption while improving process control. ABB’s latest generation of IE5 ultra-premium efficiency motors and synchronous reluctance motor technologies are helping industries achieve substantially lower energy losses compared to conventional systems.
Compared to the commonly deployed IE2 motors, IE5 motors can achieve nearly 50 per cent lower energy losses across several operating ranges, making them particularly relevant for energy intensive sectors such as cement where motors operate continuously at scale. In large scale industrial applications, it is estimated that upgrading to IE5 motor systems can deliver energy savings significant enough to enable payback periods of nearly one to two years, depending on operating hours and load conditions.
The impact goes beyond energy bills. Lower energy consumption directly contributes to reduced carbon emissions and supports India’s broader sustainability ambitions, including the country’s commitment toward net zero pathways and industrial decarbonisation. At ABB in India, our installed base of motors and drives has already contributed to significant annual energy savings across industries. According to our estimates, ABB motors and drives installed over last 12 years, save nearly 20 TWh of electricity annually in India, equivalent to roughly half of Delhi’s annual electricity consumption.
Rise of the digital plant
As cement plants become larger and more automated, operational continuity has become critical. Unplanned downtime in a cement facility can lead to significant production losses, supply chain disruptions and maintenance costs. This is driving a major shift toward digitally connected operations.
The next generation of motors and drives is embedded with intelligent monitoring capabilities that enable real time visibility into equipment performance, energy consumption and operating conditions. Combined with Industrial IoT, advanced analytics and predictive maintenance solutions, plant operators can now move from reactive maintenance to proactive asset management. In practical terms, this means maintenance teams can detect anomalies such as overheating, vibration imbalances or bearing degradation long before equipment failure occurs.
Predictive maintenance technologies are especially important in cement manufacturing because of the extreme conditions in which equipment operates. Dust, vibration, fluctuating loads and high ambient temperatures place enormous stress on rotating equipment. Digital condition monitoring systems can continuously assess equipment health, identify performance deviations and help optimise maintenance schedules, reducing downtime, extending equipment life and improving operational reliability.
As cement manufacturers navigate fluctuating energy prices, changing market demand and sustainability targets, intelligent motor systems provide the flexibility needed to optimise production dynamically.
Toward total cost of ownership
One of the most significant shifts taking place in industrial decision-making today is moving away from evaluating equipment based solely on upfront capital cost toward understanding total cost of ownership (TCO). In a typical motor system, the purchase price often represents only a small fraction of the total lifecycle cost however energy consumption, maintenance requirements, downtime and operating efficiency account for the vast majority of long-term operational expenses. For cement manufacturers operating in highly competitive markets, this distinction is critical.
A high efficiency motor paired with an appropriately configured variable speed drive may require a higher initial investment, but the long-term benefits are substantial. Reduced electricity consumption, lower maintenance needs, longer service intervals and improved process stability can deliver faster payback and stronger profitability over time.
In addition to reducing energy use, optimised drive powertrain also minimises mechanical stress on equipment. This improves reliability and reduces wear on bearings, couplings and connected systems.
As sustainability reporting and energy benchmarking become increasingly important
across industries, forward looking cement manufacturers are recognising that investments in efficient drive powertrain create both operational and environmental value.
Engineering reliability
Cement applications demand robust insulation systems, superior thermal management, advanced sealing technologies and durable mechanical construction. ABB’s heavy-duty motors and drives are engineered specifically to withstand these extreme operating environments while maintaining efficiency and performance.
Equally important is the ability to maintain serviceability over long operating lifecycles.
In sectors such as cement, where plants are expected to operate continuously for decades, lifecycle support becomes a strategic consideration. Modernisation, retrofitting and service solutions are therefore playing an increasingly important role in helping operators improve efficiency with minimal upgradation and without requiring complete infrastructure replacement.
ABB’s Motion Services portfolio supports customers through predictive maintenance,
performance optimisation, digital diagnostics
and lifecycle management solutions designed to maximise uptime and equipment longevity. Reliability in cement manufacturing is no longer simply about avoiding breakdowns. It is about ensuring continuity, protecting productivity, enabling operational confidence and excellence.
Safety-productivity connection
Industrial safety and operational productivity are deeply interconnected. As cement plants become more automated and digitally integrated, modern motor and drive technologies are also contributing to safer work environments. Remote monitoring capabilities reduce the need for personnel to physically inspect equipment in hazardous or hard to access areas. Intelligent systems can provide alerts, diagnostics and performance insights remotely, improving both safety and maintenance response times.
Advanced drive technologies also support safer operations through smoother start-and-stop, controlled acceleration and reduced mechanical shocks. These capabilities not only protect equipment but also reduce operational risks for plant personnel. Additionally, digitally enabled systems improve visibility into operational conditions, helping teams respond more effectively to potential safety issues before they escalate. In many ways, the modern cement plant is evolving into a more connected and collaborative ecosystem where automation, digital intelligence and motion technologies work together to improve both human safety and operational excellence.
India’s infrastructure ambitions
The cement industry is entering a transformative phase. As India advances toward becoming a global manufacturing and infrastructure powerhouse, the sector will need to balance growth, competitiveness and sustainability simultaneously. It is an opportunity for us to help industries outrun leaner and cleaner. By combining energy efficiency, digital intelligence and engineering innovation, the cement sector can accelerate its transition toward a more sustainable and resilient future while continuing to power India’s growth ambitions. And that journey has already begun.
About the author
Sanjeev Arora, President – Motion Business & IEC LV Motors Division, ABB India comes with nearly three decades of experience in industrial motion technologies, energy-efficient motor systems, and driving sustainable industrial transformation across India and the Middle East & Africa.