Connect with us

Concrete

Bringing About a Green Change

Published

on

Shares

VN Balasubramanian, Director – Head BU Polysius India, thyssenkrupp Industries India (tkII), discusses the various factors challenging Indian cement sector’s fight against carbon emissions and the role technology partners play in the larger scheme of things.

BU Polysius has been in existence for over 150 years and has grown from a family-owned brand to a conglomerate. The philosophy of the Polysius group has always centred on quality, reliability and performance. India is a very price sensitive market, but as a group, thyssenkrupp Polysius is driven by the quality and ruggedness of German machinery. Their products may not be the cheapest in terms of price, but are amongst the best in quality. They do not believe in slashing their prices and compromising quality.
Major cement players from the Indian cement industry have relied on thyssenkrupp Polysius and have added multiple lines over the years. In addition, several new customers have also placed orders on Polysius in the recent past. Between 2010 and 2020, tkII Polysius have built 22 Pyro lines, which is a testimony to the reliability, quality of the equipment and service focus for the customer.

Reducing Carbon Footprint
Carbon footprint reduction in the Indian cement industry is not yet a mandatory norm like in the west but the mandates are round the corner. The Indian cement industry has strict guidelines on noise and dust emissions, which they have admirably complied with. There are guidelines on SOx and NOx emissions but no penalties yet for carbon emissions. But the awareness has surely increased. Outside India, BU Polysius have come up with a lot of green technology initiatives for reduction in use of fossil fuels, utilisation of activated clay etc. There are plants in Europe operating on 100 per cent alternative fuel and raw materials (AFR) with equipment supplied by BU Polysius. This has twin advantages of reduction of carbon emissions as well as operational cost advantages to the customers. Polysius offers a complete solution for AFR handling from the collection point to feeding in the calciner with assurance of total substitution rate (TSR) and throughput. The solution is field proven, with several operating references and highly beneficial to the customer and of course, the environment in the larger scheme of things.
In India, the AFR usage is around 15-25 per cent and is very fragmented. The main hurdle in achieving higher TSR rates is the supply chain to ensure continued availability of the waste of the right quality. Secondly, many plants are not AFR ready. However, this trend is changing for the better now with customers insisting on designing AFR-ready plants.
Apart from the standard ISO specifications that they adhere to and following the DIN standards for designs that are based out of Germany, all their equipment are initially designed in Germany and horizontally deployed in India. Hence, the thyssenkrupp India team does not copy, only improvise/ modify to match Indian conditions, get their approvals for BU Polysius and move forward. The vetting is a mandatory process for maintaining standards and reason for higher costs of their products. Every big and small equipment is DIN standard specified and over a period they are vetted. tkII workshops are approved by BU Polysius Germany Quality experts, who also carry out periodic inspections to ensure quality standards.
Customer Complaints at tKII are accorded top priority and resolution within a fixed period is an absolute must. They have a standard four-eyed principle for offer and design submission, vetted by a minimum of two people to avoid any errors.
thyssenkrupp BU Polysius India Global Engineering Centre is one of the two centres in the world, catering to plant design for BU Polysius Germany for their global projects. It comprises handpicked designers trained by Polysius Germany to deliver top class quality on rigid timelines. To maintain the high standards, German experts constantly evaluate and upgrade the skills of the team.

Role of Automation and Technology
Operating costs are constantly on the rise. The goal is to reduce the production cost to the best possible extent for the customers. In the former days, there used to be about 800 people working in a cement plant and today it has been reduced to less than 250 in India. Similar plants overseas operate with less than 100 personnel. This has been possible largely due to digitalisation and automation. The trend is gradually gaining pace in the Indian cement industry as well. Manual intervention in inspection and operation not only increases the cost but also the probability of errors. Today automation is not just a buzzword but the need of the day.
For example, their R&D Centre in Germany can evaluate the real time performance of a Polysius plant in India or any corner in the world without physically visiting. It, of course, comes at a price but with proper planning in the early stages of the project, the cost is negligible. It is possible even in operating plants of any make. The cost incurred vis-à-vis advantages of an automated solution is a no brainer.
Developing a digitalised solution for improving operational efficiency is a challenge, and there are many players in the market but with thyssenkrupp Polysius, the added advantage is the knowledge
of process technology that comes along. Thus, the output from their automation solutions are more precise and accurate, which are accompanied by precise recommendations.
Regarding polab® laboratory automation, Polab stands for POLYSIUS Laboratory. It is one of the most automated and reliable products in the market today. It is a step towards the future where it cuts out personal and human intervention. With the POLAB, samples are collected automatically from every stage of the production line, transported to the lab and results delivered within a few minutes and correction is carried out online.
Earlier cement plant laboratories used to have 6-8 people in a shift and at least 10-12 in the lab for the physical and chemical testing. Now, the POLAB carries out the tests automatically with a robot that does all the testing, and usually operates with just one person per shift to oversee the operation. The total design and supply of crucial components are from Germany. Another USP is the assembly and trial of the entire system in our R&D centre in Germany before being shipped out to the plant location. thyssenkrupp BU Polysius specialises in this kind of automation.
In India, Wonder Cement has four pyro processing lines from BU Polysius through tkII. The association started with the first line and with each new Pyro line, modules added subsequently. The entire system is fully integrated and operational. The key components in all lines are manufactured and assembled in Germany. The quality control at every stage is excellent and very precise. It contributes to the image of Wonder cement. The return on investment is high in this scenario. There are other players also in the market but very few bring with them the technology that is akin to BU Polysius.
polab® is yet another equipment that the company is proud of. They are thinking of steps to further indigenise some components to optimise costs and work on the lines of ‘Make in India’ initiative so that over a period of time, it becomes more affordable for all cement players in India, without any compromise on quality. For the past two years, India has been one of the most fiercely expanding economies and top of the order in terms of capex investments in the cement sector.
A few years ago, thyssenkrupp India used to execute 2-3 pyro lines in a financial year. But in the past couple of years, they are executing on at least five pyro lines with 10-12 raw grinding units simultaneously without any big-time increase in headcount. This has been possible due to the proactive support from the parent organisation in Germany and excellent work of the young and exuberant team in the BU Polysius India. It would not have been possible without them.
With the tremendous thrust on infrastructure in the recent budgets, the Government of India has opened floodgates of opportunity for the cement sector. Hence, the bullish trend should continue for a few more years but will continue to be severely price competitive. Hence, the key lies in optimising design and cost without compromising quality. Indian cement plants are amongst the most efficient worldwide in terms of fuel and power consumption but we are not yet there in terms of emissions and cost competitiveness.
The Government of India and the cement industry are putting efforts in that direction. But, given the size of India and its diversities, the task is daunting. They are optimistic that change will happen soon and tkII BU Polysius with the technology back up is prepared to partner the cement makers to bring this green change to cement manufacturing, which will not only help the current generation but also the future generations.

–Kanika Mathur

Concrete

CII Calls for Greater Alternative Fuel Use in Cement Industry

Published

on

By

Shares

The Confederation of Indian Industry (CII), through its Green Business Centre and Energy Efficiency Council, inaugurated the 16th Conference on Alternative Fuel and Raw Material Usage (AFR) in Goa on 27 October 2026. The two-day conference brought together more than 350 industry leaders, policymakers, waste management experts and technology providers to explore strategies for accelerating alternative fuel adoption in India’s cement industry.

Held under the theme ‘Preparation for Net-Zero: Alternative Fuels & Raw Material in Cement Manufacturing’, the conference focused on reducing dependence on conventional fuels, improving waste utilisation and strengthening circular economy practices across cement manufacturing operations.

E R Raj Narayanan, Chairman, AFR Conference 2026, and Business Head and Chief Manufacturing Officer, UltraTech Cement, highlighted the industry’s progress in alternative fuel adoption. He emphasised the need to scale implementation, strengthen supply chains and extend circularity beyond fuel substitution to alternative raw materials through technological innovation and industry collaboration.

Harish Adconkar, Managing Director, Goa Waste Management Corporation, highlighted Goa’s progress in scientific waste management and refuse-derived fuel (RDF) production. He stated that approximately 765,000 tonnes of RDF had been supplied to cement plants, contributing to an estimated displacement of 320,000–560,000 tonnes of coal. He emphasised the importance of consistent RDF offtake and stronger coordination between urban local bodies, waste management agencies and cement manufacturers.

Dr L P Singh, Director General, National Council for Cement and Building Materials, identified AFR as an important opportunity for decarbonisation and resource efficiency. Drawing parallels with the industry’s successful utilisation of fly ash, he stressed the need to address quality, technological and economic challenges to expand alternative fuel adoption.

Dr Sharad P Kale, Special Advisor to the Chief Minister of Goa and former Head of Technology Transfer and Collaboration at BARC, emphasised treating waste as a resource. He highlighted decentralised biodegradable waste processing, reduced food waste and improved resource recovery as essential measures for minimising landfill dependence.

Kiran Ananth, Executive Director, Energy Efficiency, Renewable Energy and Green Entrepreneurship, CII-Green Business Centre, noted that India’s cement production reached approximately 491 million tonnes in FY2025-26, while the industry’s thermal substitution rate (TSR) stood at 7.5 per cent, with around 7 million tonnes of alternative fuels utilised annually.

He added that the industry had invested over Rs 12 billion in co-processing infrastructure during the past six years. Improving RDF supply reliability and quality assurance would be crucial to maximising the utilisation of existing infrastructure and accelerating industrial decarbonisation.

The conference also featured discussions on advanced AFR co-processing technologies, waste pre-processing solutions and industrial best practices for improving fuel substitution and resource recovery.

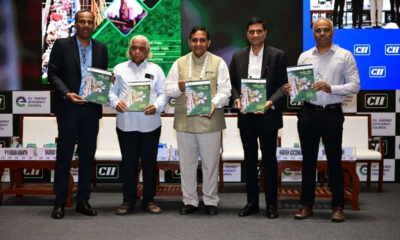
A publication titled ‘From Waste to Kiln: Scaling the Use of MSW-Derived RDF in Indian Cement Plants’ was launched during the inaugural session. The report identified inconsistent RDF supply and quality as major barriers to achieving higher thermal substitution rates.

According to the publication, many cement kilns already possess the technical capability to achieve higher alternative fuel substitution. However, variations in RDF availability, moisture content, particle size and calorific value continue to limit utilisation. The report emphasised the need to strengthen waste segregation, pre-processing and aggregation systems to establish reliable RDF supply chains.

The conference’s second-day agenda includes discussions on innovative domestic and industrial waste management solutions, alternative raw materials for low-carbon cement and strategies to increase alternative fuel utilisation across India’s cement manufacturing sector.


Continue Reading

Concrete

Sameera Group Enters Industrial and Logistics Real Estate

Rs. 1.5 bn project to support manufacturing and supply-chain firms

Published

on

By

Shares


Sameera Group has entered the industrial and logistics real estate segment with a 450,000 sq ft development in Sriperumbudur, Chennai. The group will invest Rs. 1.5 bn in the project, expanding beyond residential plotted developments into business-to-business real estate.

The proposed park will serve light manufacturing, e-commerce, third-party logistics and other supply-chain businesses. Building plan approvals have been secured, with construction expected to begin shortly. The development is scheduled to become operational within 12 to 15 months.

Sameera Group Managing Director and Chief Executive Officer Jayakumar Murugesan said the project marked the next stage of the company’s growth after nearly four decades in land acquisition and real estate development. He attributed the choice of Sriperumbudur to its industrial activity and growth prospects.

The Grade A development will include internal movement routes and shared infrastructure for modern manufacturing and logistics operations. The group is pursuing Indian Green Building Council (IGBC) Platinum certification and plans to provide rooftop solar readiness, rainwater harvesting, wastewater recycling, energy and water monitoring, and electric vehicle charging facilities.

The project is being developed amid increased demand for industrial and warehousing space in Chennai. Knight Frank’s India Warehousing Market Report 2026 recorded 8.3 mn sq ft of warehousing transactions in the city during 2025, up 42 per cent from the previous year, with manufacturing accounting for 59 per cent of demand. The Sriperumbudur-Oragadam cluster contributed 77 per cent of transactions.

Sameera Group plans to develop 5 to 6 mn sq ft across a larger industrial and logistics portfolio over the next five years, involving an estimated investment of Rs. 18 bn. Land has been acquired for projects in Chennai, Hosur and Bengaluru. Established in 1982, the group has developed more than 900 acres, sold over 13,700 residential plots, and currently has 35 projects under development and 28 in its pipeline.

Continue Reading

Concrete

UltraTech Cement Expands in Andhra Pradesh with Rs. 26.5 bn

Petnikota plant adds 3.6 MTPA cement dispatch capacity

Published

on

By

Shares


UltraTech Cement has expanded its manufacturing footprint in Andhra Pradesh with the commissioning of Petnikota Cement Works, an integrated cement plant built with an investment of around Rs. 26.5 bn. The facility is located in Petnikota village in Kolimigundla mandal of Nandyal district, in the Rayalaseema region.

Construction of the plant began in May 2025. The facility has a clinkerisation capacity of 3.3 MTPA and a cement dispatch capacity of 3.6 MTPA, strengthening the company’s production and distribution presence in the State.

The plant is expected to provide direct employment to 650 people and indirect employment to another 2,000. It has been designed to operate entirely on green energy and does not have a captive thermal power plant. The project also uses no groundwater, according to information released by the Andhra Pradesh Government.

Nara Lokesh, Andhra Pradesh Minister for Information Technology, said in the release that the facility was taken from groundbreaking to commissioning in 14 months. He described the project as a state-of-the-art addition to the company’s operations in the State and said it would create 2,650 direct and indirect employment opportunities.

Petnikota Cement Works adds to UltraTech Cement’s manufacturing capacity in Andhra Pradesh while supporting industrial activity in Nandyal district. The plant’s energy design and stated groundwater-use policy are also intended to reduce the environmental impact of its operations. The company has identified the facility as part of its continuing capacity expansion in the Indian cement market.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds