Connect with us

Economy & Market

Green Agenda

Published

on

Shares

The new environmental norms which the power sector has to adhere to come with their own set of technological challenges. For the first time ever, schools have been shut in the first week of November 2016 in New Delhi and citizens are rushing to buy air purifiers as sensors show alarming levels of air toxicity. Why has the situation come to such a pass?
The heavy concentration of particulate matter is greatly affected by meteorological conditions. In winters, cool air causes ‘inversions’ that make the air stagnant and trap pollution close to the ground. Air flow patterns from Afghanistan and Pakistan pick up emissions as they move over the densely urbanised regions of Punjab and Haryana where farmers burn straw in their fields and pull this pollution into Delhi.
Pre-monsoon dust storms also contribute to air pollution in the region. These are some of the opinions expressed by environmentalists. Ref. Figure 1
The role played by thermal power plants is significant in worsening air quality. The Ministry of Environment, Forest & Climate Change (MoEF & CC) announced the revised standards for controlling pollution in December 2015, considering the deterioration of ambient air quality. The proposed standards are strict, but can be achieved if the compliance plan is executed correctly. The revised standards, which are quite comparable with international standards, aim to cut emissions of particulate matter (PM), sulphur dioxide (SO2), oxides of nitrogen (NOx), and mercury. In addition, the new norms also require power plants to sharply curtail the use of water.
In December 2015, MoEF & CC announced standards for coal-based thermal power plants, which are given below. Ref. Table 1
There are commercial implications of executing the change. The most important one being of finance for the investment required and cost recovery through tariff. The time lines issued by the ministry are tight, but achievable.
In case any additional time is required for implementation of the change, this permission may be granted on a case-to-case basis. Plants under construction need to change the design and plans to meet the new norms from 1st January 2017, which would be a challenge. Technology options
Investments in plants/units that have exceeded their design life of 25 years must be made carefully, considering their efficiency and availability, post revamp. A majority of such plants will have to be shut down. Basic up-gradation targeting mainly PM control may, however, suffice in the interim. Plants with good operating performance, low cost of generation and recent repairs & maintenance that would have extended remaining life may be allowed to invest so that they can meet the new standards. Particulate matter (PM)
Units commissioned between 1990 and 2008 may need to upgrade the electrostatic precipitator (ESP) to meet the PM norms of 100 and 50 mg/Nm3.
In some cases, it may involve adding fields in series or parallel or increasing the height of the ESP. The units installed after 2008 are required to meet PM norms of 50 mg/Nm3. Therefore, a basic performance revamp may suffice for these units. However, some units are required to meet 100-150 mg/Nm3 and others are poorly performing – these units may require huge investment.
Power plants under construction should be able to meet the 30 mg/Nm3 PM standard with a combination of ESP and FGD (flue gas desulphurisation) In fact, an integrated design would mean that the ESP size can be made smaller than a standalone one for meeting the norm.Sulphur dioxide (SO2)
Units of size less than 500 MW installed between 1990 and 2016 need to meet the SOx norm of 600 mg/Nm3. These units may choose options such as partial FGD or sorbent injection.
Units of size 500 MW and more, installed between 1990 and 2016, have to install limestone-based wet FGD or lime-based dry FGD, depending on raw material and water availability. FGD is a mature technology for controlling SOx. It is used in many countries and has been shown to be effective for a wide range of coal qualities and operating conditions. China has installed FGD in over 91.4 per cent of its fleet in recent years. Upcoming units can meet the SOx standard by installing FGD.Oxides of nitrogen (NOx)
Minimal measures are needed to meet emissions of less than 600 mg/Nm3. Some units are already meeting these levels. The units installed after 2003 have to reduce emissions to 300 mg/Nm3. Manufacturers, including BHEL, have already been supplying boilers that meet these emissions. Those plants whose emissions exceed the norms will need to choose from several options including burner modification, over fire air supply (OFA) etc., depending on the base level of emissions and technical constraints.
Upcoming units need to meet the NOx emissions of 100 mg/Nm3 SCR (Selective Catalyst Reduction) and SNCR (Selective Non-Catalyst Reduction) technologies, which have been used globally to cut NOx to these levels. Some industry players, however, feel that the technology’s effectiveness needs to be established for Indian coal (high ash, chemical composition and physical characteristics). NTPC will run five pilot programmes to assess the technology. Suppliers are confident that the technology will work with possibly minor tweaks.
The coal-based power sector is in the midst of a major transition across the world. China, for instance, has decided not to build new coal-fired plants after 2030. India, on its part, has put in place tighter environmental standards and hiked its coal cess by eight times within two years. Says Chandra Bhushan, Deputy Director-General of Centre For Science and Environment (CSE), New Delhi, "The world is faced by relatively newer challenges, including that of a changing climate – this means countries need to have flexible, nimble energy policies."
In addition to the monitoring of individual parameters, the power plants will have CEMS(Continuous Emission Monitoring System). Developed countries such as the US, EU and Japan as well as a few emerging economies like Brazil and China have already adopted CEMS. The Central Pollution Control Board will be the authority that will drive the implementation.
Priyavrat Bhati of CSE adds, "Some basic requirements for successfully implementing CEMS – such as skilled laboratories and human power or comprehensive guidelines for device selection, etc., are still lacking in India." This creates multiple implementation challenges which must be urgently resolved. While CEMS has been initiated as pilots in three states, fundamental issues are yet to be resolved. For instance, manufacturers express their concern over the unavailability of standards in India for getting themselves certified as accredited device manufacturers. It goes without saying that the changes are equally applicable to captive power plants irrespective of their capacity to generate power.

Table 1: Standards (in mg/Nm3)


Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

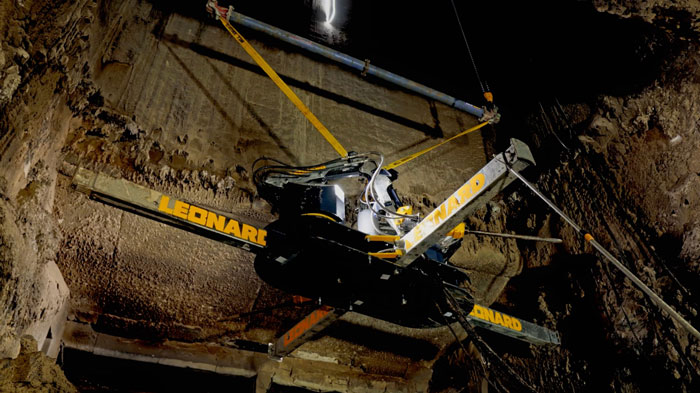
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.

Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

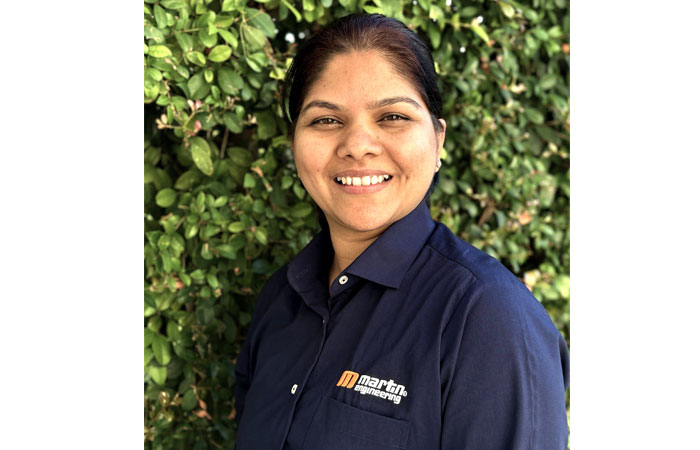
Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

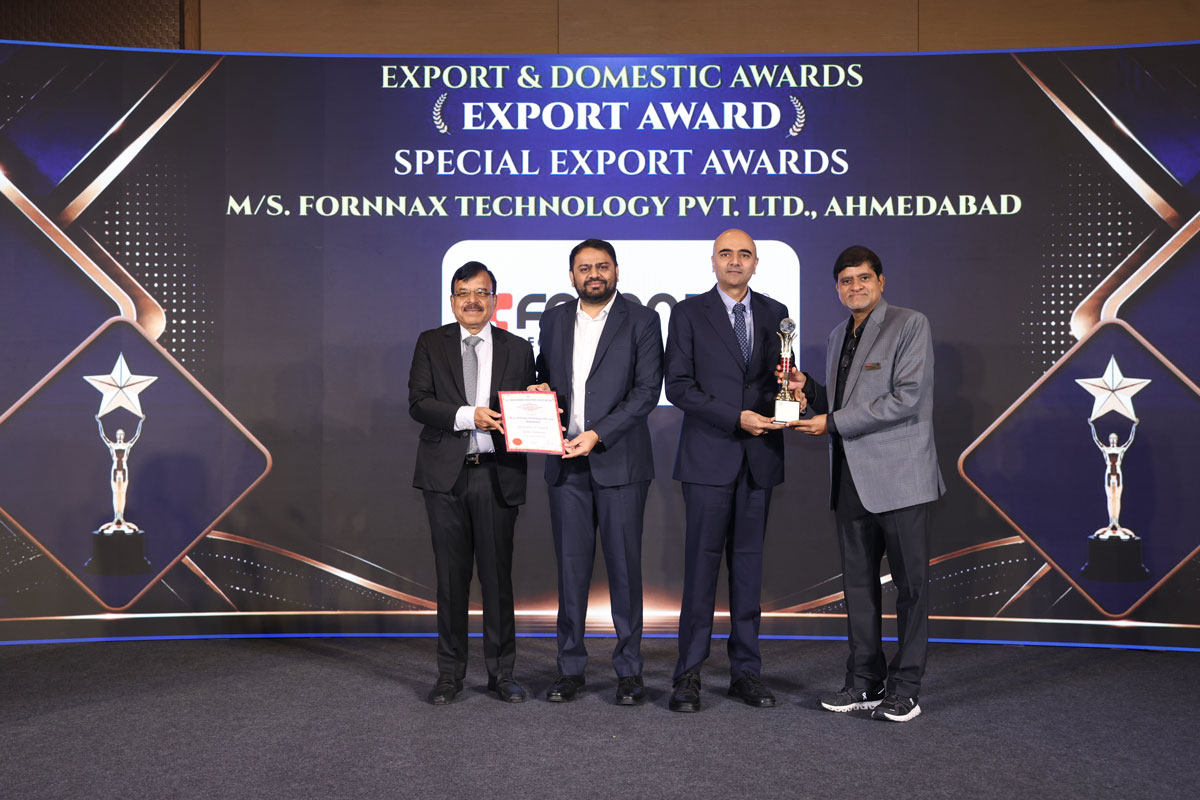
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds