After the ready-mixed concrete industry?s successful journey of 20 long years in India, the new era concrete has to perform many applications apart from achieving strength and workability. The article outlines some new developments in the field.
Water plus cement plus aggregates; the formula seems mighty simple, but in reality concrete manufacturing is a far more complex process. As India builds its infrastructure, the ready-mixed concrete industry is steadily gaining pace as the most viable option to speed up construction.
Various properties such as sustainability, easy flow, colourful, lightweight, high early strength, durability, etc., need to be attained to meet the requirements specified by the construction industry. A deft designing of concrete is done to achieve these properties. All such need-based concrete products are often tailor-made and as always, have proved to be value for money.
High volume Fly Ash/High Volume GGBS concrete
Supplementary Cemetitious Materials (SCMs) such as fly ash, GGBS (Ground Granulated Blast Furnace Slag) in concrete are in use for a reasonably long period due to the overall economy in their production as well as their improved performance characteristics in aggressive environments. High Volume GGBS and HVFA concrete is a major breakthrough as compared to conventional concrete due to cement savings, cost savings, environmental and social benefits offered by it. So it?s wide spread usage should be encouraged in extending the lifespan of structures.
Usage of High Volume GGBS and HVFA significantly reduces the risk of damages caused by Alkali-Silica Reaction (ASR), provides higher resistance to chloride ingress by making the concrete more impermeable and reduces the risk of reinforcement corrosion and also provides higher resistance to sulphate attacks and other chemicals. The resulting product has a much lower level of embodied CO2 than if OPC or ordinary cement replacements were used. With the increase of specific surface area and content of GGBS/HVFA, the repulsion between cement particles increases, improving the workability of the HVGGBS and HVFA incorporated concretes. To obtain maximum benefits, the optimum substitute content of HVFA is 50 per cent in standard and high grades; similarly optimum substitute content of GGBS is 70 per cent in standard and high grades of concrete.
Temperature controlled concrete
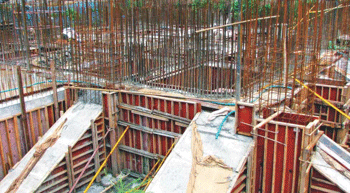
Cracking in mass concrete structures is undesirable as it affects the water-tightness, durability, appearance, and overall integrity of the structures. Cracking in mass concrete will normally occur when tensile stresses that surpass the tolerance limit of concrete are developed. These tensile stresses may occur due to imposed loads on the structure, but they more often occur because of the restraint against volumetric change. Largest volumetric change in concrete mass arises from change in temperature. The hydration of a concrete mixture is a process that liberates heat and the rate of heat generation is accelerated with the rise in concrete temperature. Concrete is a poor conductor of heat, and the rate of heat evolution due to the hydration process is much greater than the rate of heat dissipation. Development of high concrete temperatures can cause a number of effects that are detrimental to the long-term concrete performance such as:
- Thermal stresses and thermal cracking
- The tendency for drying shrinkage cracking
- Decreased long-term concrete strengths and durability as a result of cracking
- Loss of structural integrity and monolithic action, and
- Permeability.
Steel fibre reinforced concrete
Concrete is strong in compression but weak in tension and hence, in structural applications this shortcoming of concrete is overcome by providing steel reinforcing bars to bear the tensile forces once the concrete has cracked. In reinforced concrete, the tensile failure strain of the concrete is significantly lower than the yield strain of the steel reinforcement and the concrete cracks before any significant load is transferred to the steel(1). Short, discrete steel fibres provide discontinuous three-dimensional reinforcement that pick up load and transfer stresses at micro-crack level. This reinforcement provides tensile capability and crack control to the concrete section before the establishment of visible macro cracks, thereby endorsing ductility or toughness.
Steel fibres modify concrete properties as follows:
- Improve mix rheology or cracking characteristics in the plastic stage
- Improve the tensile or flexural strength
- Improve the impact and abrasion resistance
- Control cracking and the mode of failure by means of post-cracking ductility, and
- Improve durability.
The functions of steel fibres and conventional concrete reinforcement are clearly different. Steel fibres are added to concrete mainly to influence the way in which concrete cracks as it fails. Micro-cracks form when concrete is loaded. Fibres bridge cracks during loading and hence, influence mechanical performance.
Steel fibres have a tensile strength typically 2-3 times greater than traditional fabric reinforcement and a significantly greater surface area (for a given mass of steel) to develop bond with the concrete matrix(2). The average fibre pull-out length is l/4, which for the longest 60mm fibres, is only 15mm. This length is insufficient to allow efficient use to be made of the high tensile strength of drawn wire unless devices such as bends, crimps or flattened ends are used to improve anchorage efficiency(3).
Factors that influence performance of steel fibres in concrete are:
- Bond and anchorage mechanisms (e.g., straight or deformed shape, end conditions, cones or hooked ends)
- Aspect ratio (the fibre length and diameter)
- Dosage (kg/m3)
- Fibre count (number of fibres per kg of fibres), which is a function of fibre size and dosage
- Tensile strength, and
- Elastic modulus
Depending on the service life and exposure conditions, steel fibres by virtue of their disconnected nature and small diameter eliminate corrosion and associated spalling damage compared to steel rebar and enhance resistance to chloride and carbonation induced corrosion. Unlike synthetic macrofibres, they are not affected by elevated temperatures.
Reference
1.Technical Report No. 63, Guidance for the Design of Steel-Fibre-Reinforced Concrete, 2007, p 1
2.Technical Report No. 63, Guidance for the Design of Steel-Fibre-Reinforced Concrete, 2007, p 4
3. John Newman and Ban Seng Choo Advanced Concrete Technology, Processes, 2003, p 6/9
Technologies from RMC Readymix (India)
Environprotectcrete
In an era of growing environmental consciousness, more and more customers are adopting Green Building Certifications such as LEED? India developed by Indian Green Building Council (IGBC) or Green Rating for Integrated Habitat Assessment (GRIHA) developed by The Energy Resource Institute (TERI). Environprotectcrete? provides desired levels of consistence and the compressive strengths at various ages, depending upon client requirements and enables the customers to earn more points, thus facilitating the process of obtaining certification and enhancing the ratings.
Thermocrete
It is chilled concrete that gives control over the temperature differential between the core and surface of the concrete, thereby mitigating thermal tensile cracks. It also prevents delayed ettringite formation, which may occur in certain concretes of particular chemical makeup exposed to temperatures over about 70?C during curing stage.
FRCcrete
This product incorporates steel fibres, based upon expected loading and sub-base conditions, and completely does away with reinforcement bars in ground supported slabs.
RMC Readymix (India)
The company is a division of Prism Cement Limited, and is one of the largest ready-mixed concrete manufacturers in India. Established in 1996, the company operates 90 ready-mixed concrete plants in 37 cities and towns across the country. The company has always been one of the leaders in setting standards for plant and machinery, production, quality systems and product services in the ready-mixed concrete industry.








 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago