Economy & Market
AAC production in cement plant
Published
12 years agoon
By
admin
Cement companies can manufacture AAC blocks and can compete with stand alone AAC units in the country.
The raw materials required for AAC production are readily available in any cement manufacturing plant. The process does not require installation of a steam boiler or a power plant and can utilise the waste-heat from the clinker cooler exhaust gases for steam curing of aerated concrete. The method also earns carbon credits not only for the green product being made, but also for waste-heat utilisation. Although, there are more than 35 standalone AAC manufacturing units in India, very limited attempts have been made to manufacture AAC by the cement plants. One reason behind this is the lack of awareness about the new technologies that were developed recently in this field. DS Venkatesh elaborates on the technology offered by Cemeng for AAC production in a cement plant.
What is AAC
AAC is lightweight autoclaved aerated concrete, which is completely cured, inert and stable form of calcium silicate hydrate. It is a structural material, approximately one quarter in weight of the conventional concrete. It is composed of minute cells/air pockets, which give the material its lightweight and high thermal insulation characteristics. It is available as blocks and as pre-cast reinforced units for building floors, roofs, walls and lintels.
Raw material
Raw materials for AAC vary with the manufacturer and the location. The kinds of materials that could be used are detailed in the ASTM C1386 specifications. They include some, or all, of the following: fine silica sand; Class F fly ash; hydraulic cements; calcined lime; gypsum; expansive agents such as finely ground aluminium powder or paste; and water.
AAC is produced by mixing quartz sand and/or pulverised fly ash (PFA), lime, cement, gypsum/anhydrite, water and aluminium and is hardened by steam-curing in autoclaves. The silica is obtained from silica sand, fly ash (PFA), crushed silica rock and/or stone. It is possible to obtain silica as a by-product coming from other processes such as foundry sand or burgee from glass grinding; although, it can be used only if the levels of alkali or other impurities are not too high. The calcium is obtained from quick lime, hydrated lime and cement. Gypsum acts as a catalyst and enhances the properties of AAC. Careful regulation of the amount of aluminium powder gives accurate control over the density of the final product.
Cement with the least per cent of clinker would be the cheapest and suitable, e.g., Portland limestone cement. If milling of siliceous material is required, Cemeng suggests grinding of a composite mix of siliceous materials together with cement clinker, lime and gypsum/anhydrous. The ground material can be stored in a single bin. It also eliminates the need for multiple handling of individual constituents and weigh batchers. Cemeng employs a PSRG mill function in open circuit to produce the desired fineness of the composite mix.
Process flow
Cemeng has simplified the process flow to minimise the number of equipment and material handling requirements in mini AAC plants. The process gets rid of ?wet cutting? the green cake as it is possible only if the plant is involved in exclusive production of smaller blocks. Other AAC products with or without reinforcement certainly require ?dry milling? of cured cakes for profiling. Cemeng moulds for AAC are wheel-mounted units with a base plate and sliding sidewalls. There is no need for rotation or dismantling and re-assembling of side plates. Loaded moulds are transferred directly into the autoclaves for steam curing. Cemeng autoclaves generate the required steam in the autoclave itself. Separate boiler is not required. For mini AAC plants, Cemeng suggests after-cutting/milling of cured blocks for economic benefits.
The important unit operations involved in AAC production are gravimetric proportioning and mixing of constituents with water to form the slurry. This is followed with secondary mixing with expansive agents, pouring the slurry into casting moulds and then allowing sufficient time for initial hydration. Once the material is hydrated it gains enough strength to support its own weight and can undergo de-moulding/cutting. The cakes are then transferred into autoclave for high pressure steam curing. Once cooled, the autoclaved blocks are ready for after-cutting/milling as per the required profile. The AAC cost depends mainly on the cost of mineral binders and the expansive agents used. The cost of silica can vary from location to location.
Cement plant and Cemeng mini AAC production line
Cemeng mini AAC production line can be installed in an existing cement plant. Cement plants are already processing and handling both siliceous and mineral binder constituents, except for lime and sand. Also, ground raw meal, preheater ESP dust, pre-calcined meal from bottom most stage of preheater can partially or wholly replace lime. Sand may be replaced by ground slag and cinder. Clinker dust from cooler ESP and gypsum can replace cement. Besides, clinker cooler exhaust air may be effectively utilised for production of steam required for autoclaving, thus eliminating the need for a separate boiler set up.
AAC production capacity, on a thumb rule basis, can be considered as twenty cubic meter per day for every 100 tpd production capacity of the clinkerisation unit. This is based on steam production using gases only from the from clinker cooler exhaust.
Manufacturing process
To make AAC, sand is ground to the required fineness in a ball mill and is stored along with other raw materials. The raw materials are then batched by weight and are delivered to the mixer. Measured amounts of water and expansive agent is added to the mixer to prepare a cementitious slurry.
Preparation of slurry
Slurry preparation is a batch process. When AAC is being made from dry constituents, Cemeng employs separate weighbin augur dosers for each constituent the Cemeng weighbin augur doser, which uses a combination of weight and volumetric filling. A vertical auger looks like a corkscrew. The auger rotates in the hopper filled with lose powder. As it turns, it drives the powder through the bottom of the hopper into a narrow tube, where the powder is drawn down by a turning screw. The auger runs through the narrow tube, creating a tight fit. As the screw turns, it pulls the prescribed amount of powder down the tube. The agitator keeps the feed flowing to the centre of the auger. You can control the amount of powder delivered by setting the number of revolution made by the auger.
The augur screw discharges into a tubular disc conveyor for conveying and transferring directly into the AAC mixer. Subsequently, aluminium paste is added, secondary mixing is carried out and the final slurry is discharged into the AAC moulds.
Casting in moulds
Steel moulds are prepared to receive fresh AAC. If reinforced AAC panels are to be produced, steel reinforcing cages are secured within the moulds. After mixing, the slurry is poured into the moulds. The expansive agent creates small, finely dispersed voids in the fresh mixture, which increases the volume by about 50 per cent within three hours. The moulding of AAC in the mould box, holding for initial strength and de-moulding prior to autoclaving is an important step in reducing the material handling. Conventionally, the base of the moulds-box and three sides are welded together with only one side plate of mountable type. This calls for mould rotation to load the green mould on to the mountable side plate.
Cemeng moulds for AAC are trolley-mounted units with a base plate and sliding sidewalls. During casting, the sidewalls are slided inwards to form a box holding the slurry. The sidewalls keep space all around the green cake for the passage of steam. No rotation or dismantling of the side plates and reassembling are required. After curing in autoclaves, the cake is picked up by a grab and is transferred to the trolley.
Cemeng also offers ?FlexiMold? wherein rectangular shaped pre-stitched permeable cloth bags with open top are held at the base of the trolley. The flexibag is filled half with slurry and the top half is left empty to allow for expansion. As the green cake attains strength, it attains the shape of the flexibag. The telescopic brackets are then lowered. The bracket is held in its lowest position when the trolley is moved into the autoclave. The green cake along with FlexiMold is left undisturbed. After curing, the trolley is moved out and the cured cake in the moulding bag is lifted and transferred to storage. FlexiMold serves as a protective cover for cured block and it is also disposable. The size of the green cake can be set as required and several green cakes can be mounted on a single trolley.
Autoclaving
Autoclaving is steam curing at high temperature and pressure. It is required to achieve the desired structural properties and dimensional stability. The chemical reactions that produce the final calcium silicate hydrate structure happen in the autoclave. The process takes about eight to 12 hours under pressure of about 174 psi (12 bar) and a temperature of about 360?F (180?C), depending on the grade of material produced. Preferably, two autoclaves are used with the casting and precuring section in between. The mixing station is located near the discharge end of the autoclave. The thermic fluid reservoir is located at the feed end of the autoclave. This permits the precuring shed to store the cast moulds for the required duration. The waste heat from grate cooler exhaust is utilised for the heating the thermic fluid in a simple heat exchanger. It is estimated that at least 350-400 kg/hr of steam could be generated per 100 tpd production capacity of clinkerisation unit. To initiate the curing cycle, the thermic fluid, heated to 205?C, is passed through the coils in the reservoir at the bottom of each autoclave to generate steam. The hot steam pressure rises up to 1.75Mpa.
After-cutting/milling of cured AAC Blocks
Steam cured AAC blocks can be transported directly to the marketing yards. After-cutting can be carried out by the stockists or at the construction site itself. Existing granite/stone cutting and polishing units at different cities in the marketing zone can be used to saw the AAC blocks to the required size/dimensions. It is always possible to saw cut the large size AAC blocks to the required size at the construction site. Any broken pieces could be used as lightweight filler, thus nothing is wasted.
Conclusion
Every cement plant has to take green initiatives to safeguard sustainability. Using waste-heat for steam generation is highly cost effective and adds to the profits of AAC production. Besides, the plant will also be a captive consumer of cement. Every cement plant can produce AAC at considerably lower cost and can compete with standalone AAC units. AAC products can save time, labour, cement and sand during construction.
References
Eco-Care Building products: www.primeaac.com
Raw material formulae: Dearye Brick machine
Silica, calcium joined in premium products, by Sandy Herod Pit and Quarry Dec 1987 Pg.72 – 74
Brick manufacture in a Cement Plant by DS Venkatesh, Cemtec Engineering, Secunderabad. Indian Cement Review May 1989, Pages ICR-19 to ICR-25 Green Concrete by Yuvraj Patil, Flycrete. Indian Cement Review, May 2014 ?Let us employ PSRG Milling Technology? by DS Venkatesh, Indian Cement Industry Desk Book, March 2014. www.victoryenergy.com
DS Venkatesh,
Freelance Industrial Consultant
Email: dsvenkatesh40@gmail.com
Former CEO and Director of Cemtec Engineering at Secunderabad, DS Venkatesh is currently working as a freelance industrial consultant. He started as a Design Engineer at ACC and later had a long stint at Holtec-India holding several responsible positions. He has been one of the lead consultants to many rotary based mini cement plants and expansions.
DS Venkatesh has provided technical know-how, design and manufacturing drawings for cement production machinery to many Indian machinery manufacturers. Re-engineering and retrofitting of plant/machinery for enhanced productivity is his forte. His work has helped in enhancement of PSRG milling technology applied in media grinding.
You may like
Concrete
Nuvoco Vistas, CleanMax Partner for Wind-Solar Hybrid Project in Rajasthan
Published
21 hours agoon
September 29, 2026By
admin
The project – comprising 20 MW of wind and 26.4 MWdc of solar capacity – will support Nuvoco’s cement operations with cleaner power while strengthening its renewable energy and decarbonisation strategy.
Mumbai, September 29, 2026
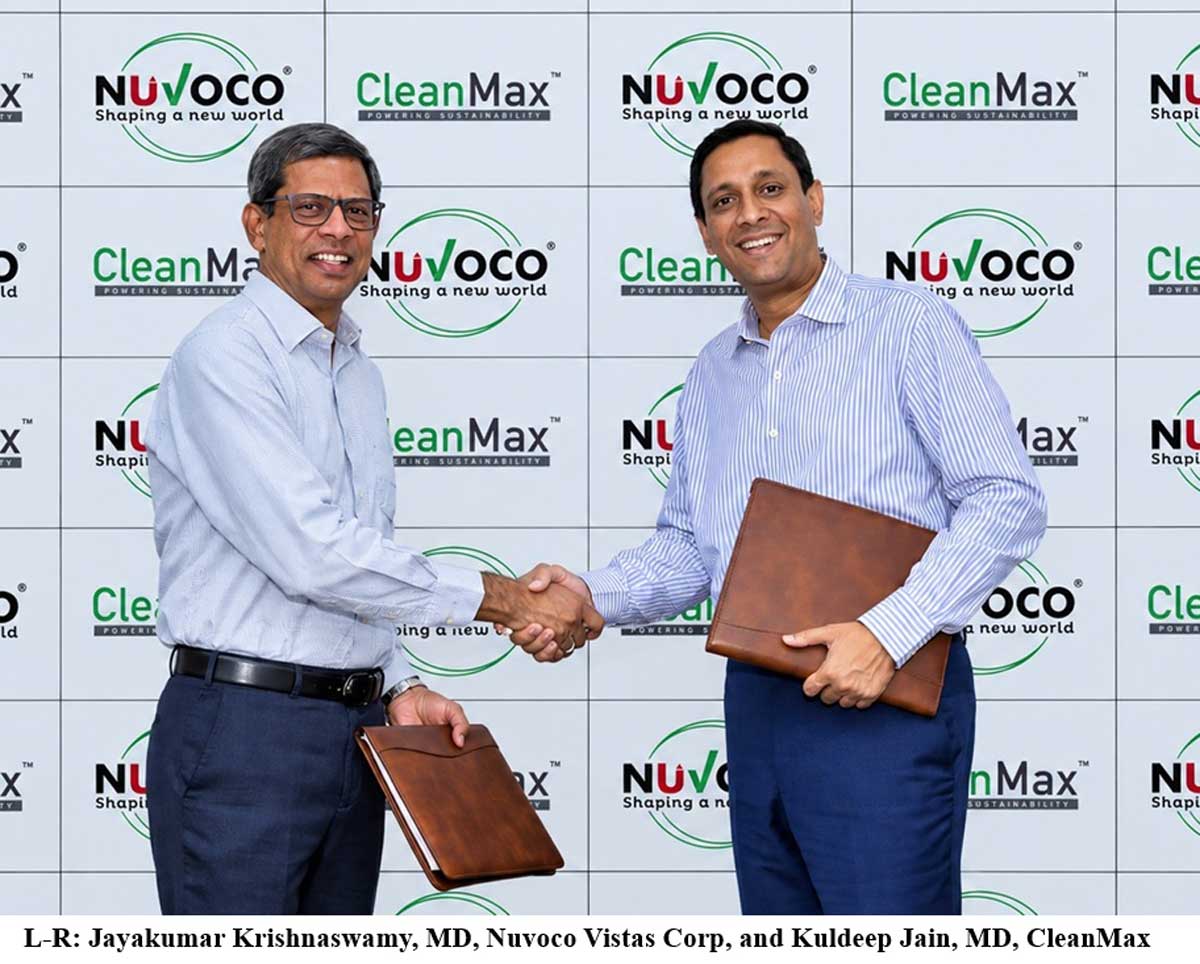
Nuvoco Vistas Corp Ltd, part of Nirma Group and one of India’s leading cement companies, has partnered with Clean Max Enviro Energy Solutions Limited (CleanMax), a renewable energy solutions provider for the commercial and industrial (C&I) sector, to develop a 46.4 MW wind-solar hybrid renewable energy project in Rajasthan.
The project will support Nuvoco’s cement operations with cleaner power while strengthening its renewable energy and decarbonisation strategy. It is expected to increase the share of renewable energy in Nuvoco’s power mix, reducing fossil fuel consumption and associated emissions.
Developed by CleanMax, an Independent Power Producer (IPP), at Bhikamkhore, Rajasthan, the project will comprise 20 MW of wind capacity and 26.4 MWdc of solar capacity, along with a 2-MWh Battery Energy Storage System (BESS). Power generated from the facility will be supplied to Nuvoco through the State Transmission Utility (STU) Open Access network.
The hybrid project is expected to generate approximately 100 million units (MU) of renewable electricity annually and help avoid around 1,25,485 tonnes of CO₂ emissions every year across Scope 1 and Scope 2 emissions.
The initiative supports Nuvoco’s ongoing efforts to reduce the carbon intensity of its manufacturing operations through renewable energy adoption, Waste Heat Recovery Systems (WHRS), energy-efficiency measures and increased use of alternative fuels. It also aligns with the company’s DIRE (Digitalisation, Innovation and Renewables) agenda, which focuses on climate action, renewable energy transition, water stewardship, circularity and biodiversity conservation across its manufacturing ecosystem.
Commenting on the initiative, Jayakumar Krishnaswamy, Managing Director, Nuvoco Vistas Corp Ltd, said, “This marks an important step in advancing Nuvoco’s journey towards more sustainable and resilient operations. Our collaboration with CleanMax will increase the share of renewable energy across our Rajasthan operations, strengthening our energy mix while improving long-term cost efficiency and reducing our dependence on conventional power sources. Initiatives such as these reinforce our commitment to operational excellence and responsible growth, while supporting our vision of Building a Safer, Smarter and Sustainable World.”
Kuldeep Jain, Founder and Managing Director, CleanMax, said, “Cement plants run continuously, so the power behind them has to be dependable for decades, not years. We’re seeing manufacturing industries view clean energy as an integral part of their core operations and long-term strategy. Our partnership with Nuvoco reflects that shift, and we’re pleased to support its decarbonisation journey. This wind-solar hybrid project is designed to deliver long-term cost certainty while supporting the Company’s transition to cleaner power.”
Nuvoco has been advancing its sustainability initiatives through renewable energy, operational efficiency and technology-driven solutions. The company operates across Cement, Ready-Mix Concrete (RMX) and Modern Building Materials (MBM) segments, with a presence across East, North and West India.
The company began operations in 2014 with a greenfield cement plant in Nimbol, Rajasthan, and later acquired Lafarge India Limited, which entered India in 1999, along with Emami Cement Ltd in 2020 and Vadraj Cement Limited in April 2025. With planned expansion initiatives, including a new grinding mill at the Arasmeta Cement Plant and multiple debottlenecking projects, Nuvoco aims to achieve a cement capacity of 35 MMTPA.
The company reported total income of Rs 113.62 billion in FY 2025-26, reflecting its continued growth trajectory. Its cement portfolio includes Concreto, Duraguard, Double Bull, PSC, Nirmax and Infracem brands, while its RMX business offers products under Concreto, Artiste, InstaMix, X-Con and Ecodure brands. Nuvoco also provides construction solutions under its Zero M range of modern building materials.
Concrete
UltraTech Cement achieves 100% green energy milestone at Chhattisgarh plant
Published
23 hours agoon
September 29, 2026By
admin
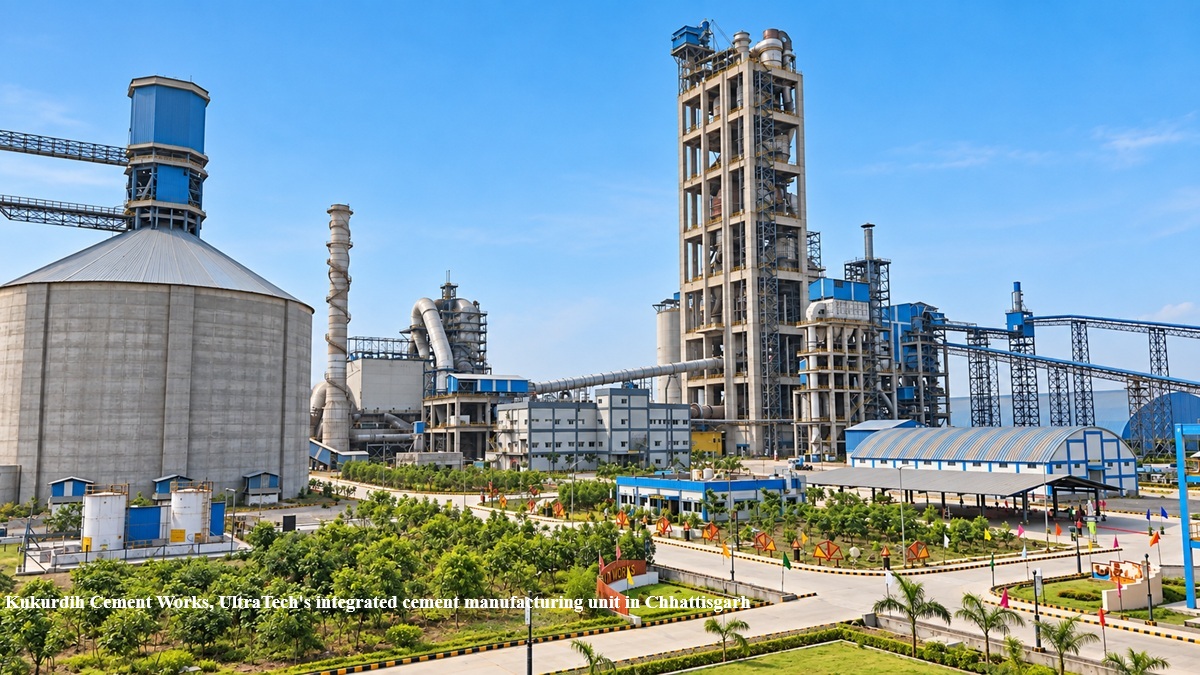
UltraTech Cement’s Kukurdih Works becomes its first integrated unit to meet 100 per cent electricity needs through green energy every month.
Raipur (Chhattisgarh)
UltraTech Cement Limited, the world’s largest cement company outside China, has achieved a significant decarbonisation milestone, with its Kukurdih Cement Works integrated unit in Chhattisgarh meeting 100 per cent of its electricity requirement through green energy every month since April 2026.
Commissioned in 2024, Kukurdih Cement Works has an installed grey cement capacity of 3.3 million tonnes per annum. The unit achieved this milestone through a combination of renewable power sourcing and Waste Heat Recovery Systems (WHRS), which now collectively meet its entire electricity demand while ensuring operational reliability.
Since April 2026, nearly one-third of UltraTech’s 76 manufacturing units in India have maintained green energy utilisation above 50 per cent of their electricity requirements. Five units, including Kukurdih, have exceeded 95 per cent green energy utilisation. The company is also progressively deploying Battery Energy Storage Systems (BESS) across its network to enable deeper renewable energy integration.
As part of its decarbonisation strategy, UltraTech has not invested in additional captive thermal power capacity for greenfield projects or brownfield expansions at its integrated units for over a decade.
As of Q1FY27, the company’s captive green energy capacity stood at 1,897 MW, comprising 1,463 MW of renewable energy capacity from solar, wind and hybrid sources, along with 434 MW of WHRS capacity. Under its RE100 commitment, UltraTech aims to increase the share of green power in its total energy mix to 85 per cent by 2030 and achieve 100 per cent by 2050.
UltraTech Cement Ltd, the cement flagship company of the Aditya Birla Group, is a $10-billion building solutions company and the largest cement producer globally by sales volume outside China. The company has a total grey cement capacity of 210.1 MTPA and white cement/putty capacity of 3.5 MTPA. It is a signatory to the GCCA Climate Ambition 2050 and has committed to the Net Zero Concrete roadmap announced by GCCA.
Praveen Vashistha, Founder, Gxpress Solutions, speaks about building a holistic logistics network that encompasses latest technology and current challenges faced by logistics service providers.
Logistics may seem to only entail transporting a package from one location to another. However, there is more to this term than just that. Logistics refers to the entire process of controlling all movement, transfers and decisions in the correct way at the right time and cost and with the desired level of visibility.
People nowadays want to receive more than just the delivery. They want quick, efficient, reliable and transparent logistics service. On the other hand, companies are facing higher operating costs, broken supply chains, congested cities, changing habits of consumers and growing complexity of logistics services. In this situation, a full logistics package is gaining importance not only as a competitive advantage but also as a necessity for a successful business.
The main challenge lies in uniting the first mile, the middle mile and the last mile into one seamless process.
The journey begins before the package moves
First-mile logistics may be the least recognised part of the logistics chain, but they have a crucial influence on all that follows.
This stage starts from the moment the shipment leaves the manufacturer, supplier, farm, warehouse or distribution centre. Depending on the industry, first-mile logistics may involve grouping shipments from multiple suppliers, compiling paperwork and checking the inventory before sending the shipments to a central hub.
Flaws in first-mile logistics produce effects later down the supply chain. Delays in cargo pickup can affect warehouse operations; improper packaging can damage goods in transit; and incorrect inventory information may cause stockholding or unnecessary replenishments.
This is why building a reliable network involves simplifying the operations done at the beginning of the supply chain.
Companies require accurate demand forecasts, supplier visibility, standard procedures, and software to capture information from the moment a shipment enters the supply chain. Route planning and fleet management are also important at this stage, especially as it may involve contacting multiple suppliers.
The main goal is simply to make the first mile predictable.
The middle mile: Where scale meets complexity
When products leave the original site, they travel through the ‘middle mile,’ which connects fulfilment centres, warehouses, sorting centres, and regional distribution points. In this phase, logistics networks begin operating on a large scale. A shipment can pass through several facilities before reaching the final destination. Each additional transfer entails the risk of delay or damage and information losses. Accordingly, the ideal solution is not to minimise the number of transfers but rather to optimise them. The use of hub-and-spoke networks, regional distribution centres, and strategically placed distribution centres can help companies shorten transportation routes and optimise distribution costs. Besides, data can be used to determine the optimal placement of inventories.
For instance, a retailer may find that it takes more time and is more expensive to deliver goods to customers if everything is stored in a central warehouse. Meanwhile, regional distribution helps meet the customer’s needs quicker and more efficiently.
The last mile is where the customer judges you
When it comes to the logistics experience, the customer experience comes down to the delivery. While the last mile might comprise a small part of the entire journey in actual distance, it could also entail expensive and difficult processes. Delivery runs through densely populated cities, through traffic jams, through unsuccessful delivery attempts, and through changing consumer preferences and narrowed time frames.
Customers want to have control over their delivery. Delivery means that customers expect to know the exact moment when their order is delivered. They need to receive current updates about their orders and the ability to decide whether they want scheduled deliveries, or whether they want their order to be dropped off at a designated location far from their house.
As a result, last-mile logistics must incorporate both efficiency and experience. The technology may be used to ensure timely and accurate delivery, through such products as route optimisation and real-time delivery tracking.
However, technology is not enough to guarantee success in terms of last-mile delivery. Knowledge of the local area is still an important aspect that contributes to successful delivery.
One network, not three separate operations
First, the common mistake that organisations can make is treating the first mile, the middle, and the last mile separately.
An effective first mile of logistics does not matter much if the shipment waits in a hub for many hours. A perfectly working warehouse does not make a happy customer if the last-mile delivery fails. Therefore, even the fastest last-mile delivery can become an expensive operation if the supply is not well geographically positioned.
The three moments should work together as one whole system.
This implies having a common view on inventory, transport capacities, shipment statuses and demand. The Transportation Management System, Warehouse Management System and order management system should give information to each other instead of acting like separate islands.
That is where real-time information comes into play!
If something happens, such as a vehicle gets delayed, the company has to know that from the start. If not, someone from Customer Service should be informed about the situation.
Visibility is the new infrastructure
Previously, companies had to rely on physical assets, such as warehouses, trucks, and sorting facilities, to create their logistics networks. Today, they have an additional layer of technology providing visibility.
Command-and-control systems now include GPS tracking, Internet of Things devices, bar-coding, RFID, cloud computing, artificial intelligence, and analytics, which allow companies to know what the goods are doing, how well they are doing, and what is going to happen next.
Predictive analytics reveal possible delays. AI-powered forecasting increases availability. Digital dashboards enable the manager to monitor all operations in one place. The efficiency of such technologies is not measured in the amount of information they gather, but rather in their capability of converting data into knowledge.
Logistics managers should be able to answer the following questions: Where is it? When is it supposed to arrive? What causes the delay? What impact does it have? Can it be delivered some other way? How much will it cost?
The sooner the answers are given, the more resilient the logistics system is.
Resilience must be designed into the network
The events of recent years have highlighted the vulnerability of interconnected supply chains. Geopolitical tensions, bad weather, a lack of labour, poorly developed infrastructure and an unexpected spike in demand are some events that can cause problems for logistics systems without prior notice. Thus, companies should create an end-to-end network not just for normal times but also capable of functioning quickly in problematic situations. In order to create such a network, it is necessary to find alternative suppliers, use several means of transportation, create several routes of delivery, and establish inventory. It is also important to use scenario planning to define what to do if the main hub becomes unavailable or any means of transportation is blocked.
Sustainability: Part of the delivery equation
The future of logistics will also be shaped by environmental considerations.
As delivery volumes rise, businesses are under increasing pressure to reduce emissions without compromising service. Better route planning, load optimisation, electric vehicles, alternative fuels, renewable-energy-powered warehouses and consolidated deliveries can all contribute. The most sustainable shipment is often the one that does not require unnecessary movement in the first place.
Better demand forecasting and inventory placement can reduce empty miles and avoid repeated transportation. Consolidating deliveries can improve vehicle utilisation. Reverse logistics can ensure that products, packaging and materials return efficiently instead of becoming waste.
Sustainability, therefore, should not be treated as a separate initiative. It should be incorporated into network design itself.
The future belongs to connected logistics
An end-to-end logistics network ultimately seeks to close existing gaps between various processes.
Every mile of the process should be interconnected with the other miles. Warehouses should be aware of the restraints imposed by transportation. Delivery crews should be able to know at every moment the inventory at their disposal. Clients must have access to this useful information.
Companies that will be successful in this area will not necessarily be the ones with the biggest fleets or the most warehouses. They will simply be the ones that can employ their resources in the most effective manner.
The future of logistics will be represented by an ecosystem consisting of the combination of the physical aspect, digital intelligence, and personnel decisions. Every mile in the process of delivery is important. However, the key advantage here is getting those miles to work together.
For companies, it means having minimal resistance, enhancing their efficiency and improving customer care. For clients, it means simply having the right product delivered at the right time.
About the author: Praveen Vashistha, Founder, Gxpress Solutions,

Nuvoco Vistas, CleanMax Partner for Wind-Solar Hybrid Project in Rajasthan
UltraTech Unit Runs Entirely on Green Energy
UltraTech Cement achieves 100% green energy milestone at Chhattisgarh plant
Assam Cabinet Approves Rs. 110 bn JK Lakshmi Cement Investment
JSW Cement Receives Rs. 2.3 bn GST Demand Notice
Trending News
-
Concrete4 weeks agoUltraTech to Deploy 600+ Electric Trucks by Dec 2026
-

Concrete4 weeks agoUltraTech Cement expands green logistics with 600+ electric truck fleet
-

Concrete3 weeks agoKirby India Breaks Ground on Fourth PEB Plant in Tamil Nadu
-

Concrete3 weeks agoAditya Birla Group Launches Ultravolt Wires And Cables Business