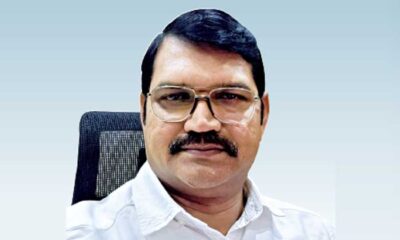
Gautam Sinha, Vice President, Sales & Marketing, Process Industries, ABB India, on the changing role of automation from a productivity tool to a cohesive operating ecosystem.
The conversation around automation in cement has shifted. It is no longer about replacing manual tasks or improving line efficiency. It is about building plants that learn, adapt and self-optimise in real time. In this interview, Gautam Sinha, Vice President, Sales & Marketing, Process Industries, ABB India, explains how predictive intelligence is solving problems that have resisted the industry for decades. He underscores the importance of cybersecurity, electrification and carbon capture as components of a single transformation that the cement industry can no longer afford to sequence.
How is automation evolving from a productivity tool to a strategic enabler of sustainability, resilience and profitability in the cement industry?
The cement industry is witnessing a shift where automation is no longer viewed solely as a productivity tool, but as a strategic enabler of sustainability, resilience, and profitability. By integrating various operational areas and leveraging advanced technologies, companies are better equipped to address key industry challenges. This integration allows for the promotion of higher usage of alternative and renewable energy sources and the real-time optimisation of asset performance, which are crucial for sustainability.
Digitalisation and automation are key to reaching environmental sustainability targets, not just by reducing emissions but also by optimising energy consumption and management. This creates immediate benefits for operating costs and margins, enabling new business models for high-tech, low-CO2 cements. For example, advanced process control (APC) solutions can improve SO2 emissions control while reducing hydrate consumption, directly impacting both environmental performance and profitability.
Furthermore, predictive asset models can help cement plants manage operations remotely, ensuring business continuity. By predicting asset failures and optimising maintenance schedules, automation minimises downtime and reduces one of the biggest costs in cement plants, thereby boosting profitability.
As cement plants accelerate digital transformation, which technologies do you believe will deliver the next breakthrough in operational performance?
As cement plants accelerate their digital transformation, several technologies are poised to deliver the next breakthrough in operational performance. Artificial Intelligence (AI) and Machine Learning (ML) are at the forefront of this transformation. These technologies enable advanced data analytics and smart optimisation, from raw materials to dispatch, which is a game-changer for many cement producers. To fully leverage these insights, robust data management systems like Knowledge Manager (KM) solutions, are essential, as they consolidate plant-wide data to connect equipment, processes, and personnel to an unprecedented. This unified intelligence creates a single source of truth, making the concept of a highly efficient, autonomous plant an achievable reality.
The concept of an autonomous plant is becoming a reality through the use of digital and automation technologies that connect equipment, processes, and people to an unprecedented degree. By learning from a plant’s historical energy usage and production schedules, these forecasting tools deliver accurate predictions that help plants reduce peak demand charges on electricity bills. Technologies such as ABB Ability™ Knowledge Manager and Expert Optimiser are already helping cement plant owners achieve business results and meet decarbonisation targets. For example, ABB Ability™ Expert Optimizer for cement helps to optimise operations and reduce energy consumption.
Significant developments are also emerging from technologies that enable process electrification, fundamentally changing how cement is produced. Innovations in electrically powered heating solutions for high-temperature processes like clinkerisation, and the use of electric plasma to replace fossil fuels in calcination, offer pathways to production with lower emissions. When combined with essential technologies like Carbon Capture, Utilisation, and Storage (CCUS), these electrification strategies are a critical part of the plan for the future of the cement industry.
With AI becoming integral to industrial operations, how do you see predictive intelligence reshaping process control, quality assurance and energy optimisation in cement manufacturing?
AI-powered solutions gather data from multiple sources like smart sensors and databases to enable algorithms to evolve and improve their predictions. In process control, AI is moving traditional Advanced Process Control (APC) solutions towards adaptive APC. While traditional APC addresses thermal efficiency and fuel switching, AI-driven analytics will enable automatic re-modeling and tuning, optimising additional variables and allowing systems to operate at peak performance. In the future, AI systems will interact with control system history data to learn from patterns, recommend optimal parameters, and even write new setpoints directly to the control system.
For quality assurance, AI is solving longstanding challenges like cement quality prediction. Traditionally, cement strength is measured after 28 days, which is too late for process corrections. ABB is leveraging ML with data-driven soft sensors to predict 28-day strength on the day of sampling, allowing for immediate process adjustments and reducing the need to ‘overdeliver’ on product specifications. In energy optimisation, AI-based anomaly detection can learn a plant’s “normal” energy usage patterns and use adaptive setpoints to detect unusual behavior. By triggering alerts on energy consumption deviations, operators no longer need to set manual setpoints or deal with notification overload. The system can also learn from a plant’s energy
usage and production schedules to deliver accurate forecasts, helping to reduce peak demand charges on electricity bills.
Cybersecurity is becoming inseparable from automation; how should cement manufacturers strengthen digital resilience while expanding connected operations?
As automation and digitalisation become more integrated into cement manufacturing, building
strong digital resilience is crucial. To achieve this
while expanding connected operations, cement manufacturers should adopt a proactive and AI-driven approach to cybersecurity.
Strengthening digital resilience involves several key strategies. Manufacturers can leverage AI-powered analytics solutions to continuously monitor, diagnose, and resolve security issues, which helps in safeguarding personnel, protecting assets, and preserving the company’s reputation. Given the unpredictable and evolving nature of both technology and cyber threats, it is essential to periodically review and update security strategies. This includes conducting simulations for various threat scenarios, such as a major ransomware attack, to test the robustness of the defense systems. Furthermore, data analytics can be employed to run “what-if” scenarios, allowing plants to anticipate potential vulnerabilities and fortify their digital infrastructure accordingly. This forward-thinking, analytical approach enables cement producers to not only connect their operations but also secure them effectively against the dynamic landscape of cyber threats.
What will define the ‘cement plant of the future,’ and what role will companies like ABB play in enabling that transformation?
The cement plant of the future is defined by the seamless integration of digitalisation, automation, electrification, and decarbonisation. Operating as a highly connected, increasingly autonomous ecosystem, it relies on real-time data integration, digital twins, and remote monitoring to run processes on “autopilot”. Crucially, the future plant is deeply sustainable—minimising its carbon footprint through the adoption of alternative fuels, electrified high-temperature processes, and carbon capture technologies.
ABB plays a pivotal role in this transformation by providing the essential automation, digital infrastructure, and electrification technologies. Through tools like ABB Ability™ Expert Optimizer and Knowledge Manager, ABB uses AI, neural networks, and model predictive control to stabilise kiln operations, optimise energy consumption, and maximise alternative fuel usage. Additionally, ABB secures these highly connected environments with proactive, AI-driven cybersecurity, while pioneering sustainable innovations like Electric Arc Calcination to help manufacturers transition to net-zero, highly resilient digital operations.
















 Concrete3 weeks ago

 Concrete3 weeks ago
 Concrete1 month ago

 Concrete3 weeks ago