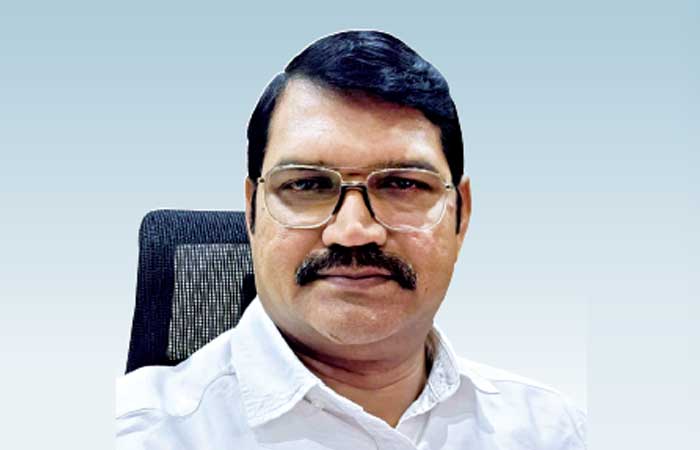
Girish Kumar, Group Manufacturing Director, Riyadh Cement, backs the case for speedy integration of low-carbon clinker chemistry, AI-driven digitalisation and alternative fuel systems.
In this interview, Girish Kumar, Group Manufacturing Director, Riyadh Cement, covers the full breadth of the challenges that cement companies are facing with regards to innovation. He points out that sustainability and industrial competitiveness are not competing priorities but the same objective pursued through better science, smarter data and more disciplined execution.
How is innovation helping the industry improve efficiency while reducing environmental impact?
Producing one tonne of cement generates approximately 0.6 to 0.9 tonnes of CO2 making cement responsible for around 8 per cent of global CO2 emissions, one of the largest shares of any single industrial process. The industry is responding on multiple fronts simultaneously.
Hydrogen co-firing is now being introduced in cement kilns and separate calciners alongside conventional fuels, directly reducing CO2 per tonne of clinker. In India, plants are integrating coastal wind turbines, solar PV systems, and waste heat recovery (WHR) systems to reduce grid dependency. Electric calciners are approaching commercial availability. In European plants, carbon capture systems are already deployed, with captured CO2 converted into methanol for reuse as fuel. Alternative fuels from municipal solid waste and agricultural biomass further curtail fossil fuel dependency.
These innovations demonstrate conclusively that sustainability and industrial competitiveness are not in conflict. They reinforce each other.
What role does R&D play in driving innovation strategy in the cement industry?
R&D is the bridge between ambition and commercial reality. Its role extends well beyond laboratory testing. It must validate new materials, optimise formulations, assess long term durability, support product certification and confirm that innovations can be produced consistently at industrial scale.
Implementation of ISO 56002:2019 Innovation Management System guidance provides a structured framework for translating stakeholder insights into practical solutions. The XRD total solution systems now allow plants to predict compressive strength days in advance, resolve ring formation and snowmen problems, and diagnose preheater clogging rapidly. The outcome is reduced downtime, consistent quality and faster time-to-market for sustainable formulations.
What are the most significant innovations currently transforming cement manufacturing and product development?
The industry is undergoing a fundamental transition from isolated efficiency projects to an integrated low-carbon manufacturing model. Several converging innovations are driving this shift simultaneously.
First is the low carbon belite rich clinker. By replacing a portion of traditional alite (C3S) with reactive belite (C2S), and incorporating industrial by-products such as fly ash and slag, clinker can be produced at lower kiln temperatures of 1,250-1,350°C. Optimised chemistry with a lower lime saturation factor (70-85) and silica modulus (1.5-2.5) promotes belite formation, improving hydration kinetics, enhancing sulphate resistance, reducing CO2 emissions by approximately 25 per cent, and cutting energy consumption to around 650-720 kcal/kg clinker.
Second are the alkali-activated materials (AAMs) and geopolymers that use fly ash and slag activated with alkaline solutions, bypassing high-temperature clinker production entirely. They offer excellent chemical resistance, high temperature stability and draw on industrial waste streams. The strongest results come when all these innovations are implemented as one coherent operating model not as separate research initiatives.
How are alternative materials and blended cements reshaping the market?
The concept of ‘From Waste to High-Strength Cement’ is now a commercial reality. Municipal waste, agricultural residues, old tyres, and biomass are being utilised in kilns to produce mineralised clinker. Combined with specialised grinding aids and strength enhancers, these inputs enable high grade cements EN 42.5R Grade that are both environmentally responsible and structurally superior.
Supplementary cementitious materials such as calcined clay, natural pozzolans, limestone, slag and fly ash increasingly replace virgin clinker, significantly reducing the clinker factor while maintaining required strength, durability and workability. This circular economy approach lowers costs, reduces environmental impact, and meets growing market demand.
In what ways is digitalisation improving production quality, consistency, and operational performance?
Digitalisation is linking plant data, laboratory data, maintenance data and energy data into a single operational view enabling faster decisions and more stable production. Under Industry 5.0 frameworks:
• AI-driven kiln optimisation and predictive maintenance reducing unplanned downtime and energy consumption
• IoT sensors providing real-time monitoring of temperatures, gas flows, and feed chemistry for immediate corrective action
• Digital twin technology simulating production scenarios to identify efficiency improvements
before implementation
• Automated quality control systems continuously analysing raw meal composition and clinker mineralogy
• Advanced process control software
The result is improved throughput, reduced energy consumption and enhanced operational reliability.
How do customer requirements influence your innovation roadmap?
Customer requirements are the primary driver. Innovation must begin with the customer application, a low-carbon cement must perform correctly in concrete, work with local aggregates and admixtures, meet durability specifications, and remain commercially practical.
Customers are asking for more than cement supply: consistent quality, predictable performance, lower embodied carbon, technical support and reliable delivery. Specific performance insights include:
• High-belite cement (HBC) with belite content exceeding 54 wt per cent exhibits exceptional resistance to chloride migration, freeze/thaw scaling and sulphate attack.
• When formulated as self-compacting concrete (low w/c ratio), HBC achieves over 20 MPa within one day, enabling efficient formwork turnover
• Accelerated carbonation studies show that
HBC increases compressive strength during CO2 exposure aligning sustainability with long-term structural performance
The innovation roadmap should therefore be built around customer segments and use cases, not around internal R&D calendars.
What challenges do companies face when scaling and commercialising new cement technologies?
Moving from successful trials to stable industrial production is consistently underestimated. Key barriers include:
• Capital intensity: Retrofitting existing plants or building new facilities requires substantial investment before commercial return.
• Raw material variability: Alternative inputs may have inconsistent chemistry, supply-chain limitations or different grinding behaviour.
• Certification and regulation: Product approval processes vary significantly by market, slowing adoption of even proven technologies.
• Carbon capture economics: Early commercial near-zero cement plants using CCS carry production costs materially above conventional production – making policy support essential for scale-up.
Overcoming these barriers demands a combination of government policy, industry collaboration and sustained commercial commitment – not technical innovation alone.
Which emerging innovations do you believe will have the greatest impact on the industry in the coming decade?
Three areas will define the next decade:
• Carbon capture, utilisation and storage (CCUS): The most critical pathway to net zero for process emissions that cannot be eliminated through fuel switching or clinker reduction. Approaches include post-combustion capture and oxy-fuel combustion. High capital requirements remain, but CCUS is essential for deep decarbonisation.
• Artificial intelligence (AI) and digital operations: Predictive maintenance, real-time process optimisation, advanced quality control, and autonomous kiln management will deliver
higher energy efficiency, lower variability and enhanced reliability.
• Advanced low-carbon clinker technologies and alternative energy: Belite-rich and calcium sulfo aluminate (CSAB) clinkers, electric calcination, renewable power integration, and hydrogen-based kiln firing will gradually replace fossil fuels.
The leading companies over the next decade will be those combining these technologies with strong data governance, product development capability and deep customer collaboration.














 Concrete4 weeks ago

 Concrete3 weeks ago

 Concrete2 weeks ago

 Concrete4 weeks ago