Economy & Market
A Strategic Asset for the Future
Published
11 months agoon
By
admin
As decarbonisation reshapes cement manufacturing, refractory systems have become pivotal to both operational resilience and future-ready kiln design. Professor Procyon Mukherjee explains how their evolution now defines the limits and possibilities of the industry’s transformation.
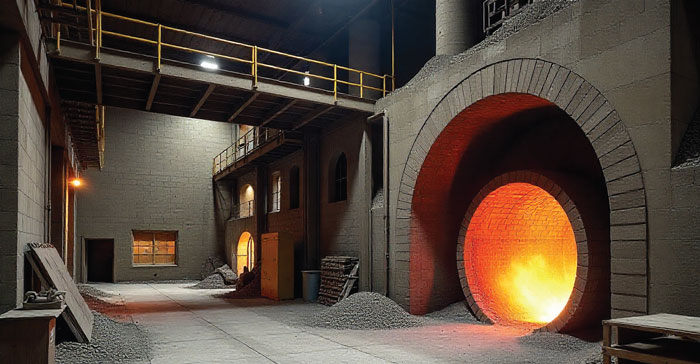
Refractory materials and pyro-processing remain the beating heart of cement manufacture. As attention shifts from incremental efficiency gains to decarbonisation and resilience, refractories and kiln-system technologies are both constraint and opportunity: they determine how fast plants can adopt alternative fuels, electrified heat, oxy-fuel systems or CCS, and they often account for a material portion of operating cost, downtime risk and capital renewal. In this article, I have tried to synthesise market signals, emerging technologies, green pathways, supplier developments and the cost outlook you need to brief for designing strategic investments for the cement industry in particular.
Demand drivers and industry structure
The global refractories market — of which cement is a major end-use alongside steel and glass — is large and growing, driven by construction activity in APAC, replacement demand (wear and corrosion), and investments related to kiln retrofits and decarbonisation projects. Recent market analyses place the refractories industry value in the multiple tens of billions of dollars and forecast steady mid-single-digit growth over the coming decade, with Asia (especially China and India) accounting for the largest regional share.
Market structure is oligopolistic at the high end. A handful of global players (RHI Magnesita, Vesuvius, Calderys/Imerys, Saint-Gobain, Krosaki Harima, Morgan Advanced Materials, etc.) supply engineered refractories, backed by regional and specialist vendors that dominate lower-cost or commodity segments. Mergers and vertical integration around alumina/magnesia feedstocks are active themes as refractory firms seek to secure raw-material supply and control quality and costs. A recent example is RHI Magnesita’s strategic acquisition of the U.S. alumina producer Resco, aimed at supply-chain security for alumina-based refractories. Most strategic sourcing models are moving to long term partnerships, which could extend to service models as well.
From the purchaser’s side, refractory selection is now evaluated not only against thermal and chemical resilience but on a broader life-cycle basis: uptime impact, ability to tolerate alternative fuels (biomass, waste-derived fuels, SRF/plastics), compatibility with oxy-fuel or electrified heat, and the ease of condition monitoring and targeted repairs. Key technical drivers include:
- Resistance to alkali attack and melt penetration under high-chloride / high-alkali fuels.
- Thermal shock tolerance as preheater/cooler cycling increases with flexible operation.
- Low thermal conductivity with structural strength to reduce heat losses.
- Compatibility with sensor embedding and digital monitoring to enable predictive maintenance.
These needs are changing refractory specifications — and therefore supplier offerings — quickly.
Emerging technologies
Several material and process innovations are maturing that directly affect kiln reliability and total cost of ownership:
1. Advanced engineered monolithics and castables: Improved bonding chemistries, nano-modifiers, and lower alkali reactivity variants lengthen campaign life and reduce patch repairs. These allow quicker repairs and less kiln downtime.
2. 3D printing and prefabricated brick assemblies: Additive manufacturing of complex refractory shapes (for riser ducts, burner blocks, throat areas) enables bespoke geometries and faster onsite installation with better dimensional control where space/access is constrained.
3. Sensorised refractories and embedded monitoring: Thermocouples, acoustic emission sensors
and distributed fibre-optic temperature measurement are being embedded to give real-time maps of lining health. These digital twins enable condition-based maintenance rather than calendar-based shutdowns.
4. Hybrid lining systems: Combining high-performance bricks in the hot face with insulating monolithics behind them to optimise performance vs cost.
Publications and industry trials in 2023–25 show pilot uptake of these technologies; embedding sensors and using predictive analytics is particularly impactful for reducing unplanned outages.
Pyro-processing trends
Decarbonisation is reshaping kiln-system choices more than any other factor this decade:
- Fuel flexibility and waste fuels: Plants are accepting higher shares of SRF, biomass and RDF. These fuels introduce chemical aggressors (chlorides, alkalis) that stress refractories and increase corrosion; refractory chemistry and cooling strategies must adapt.
- Electrification and high-temperature electricity: Technologies ranging from electrified calciners to resistive or induction heating for preheaters are under review. Recent reviews highlight electrified process heat and electrochemical routes as credible pathways, especially where grid decarbonisation is advanced.
- Oxy-fuel combustion and CCS readiness: Oxy-fuel retrofits enable easier CO2 capture but change the thermal and chemical environment in the preheater and kiln. Some pilot CCS projects in Europe, linked to cement plants and clustered transport/storage (e.g., projects coordinated out of Norway), are already operational or scaling. Cement companies with aggressive Net Zero targets are factoring refractory compatibility into their CCS roadmaps.
- Hydrogen and power-to-X: Hydrogen co-firing trials have started at modest scales; hydrogen changes flame temperature profiles and may accelerate certain refractory degradation modes if not managed.
From an engineering standpoint, conversion choices are constrained by refractory life: a kiln that can’t tolerate the chemical profile from high biomass firing, or the different flue-gas composition from oxy-fuel, will force expensive lining redesigns.
Green initiatives
Sustainability actions in cement are not solely about CO2 numbers; they alter operating envelopes:
- Clinker substitution: LC3 and blended cements reduce kiln duty and thermal load per tonne of cement, indirectly lowering refractory wear rates per unit of cement produced. LC3 deployment at scale (notably in India and other markets) is beginning to change clinker demand profiles and feedstock strategies.
- Energy efficiency upgrades: Improved preheaters/coolers and waste heat recovery change temperature gradients and gas flows; refractories must be specified for the new steady-state and transient regimes.
- Circularity in refractory materials: Recycling of spent refractories (where feasible) and substitution with lower embodied carbon raw materials (e.g., using locally sourced calcined clays or tailored industrial by-products) are receiving attention in R&D and supplier pilot programs.
- Carbon capture deployment: As CCS is pilot-scaled, refractory selection increasingly considers compatibility with capture solvents and altered flue-gas chemistries.
New suppliers and supply-chain resilience
While the well-known global refractory houses dominate engineered solutions, the landscape sees three simultaneous moves:
1. Vertical integration by majors: Acquisitions of alumina producers and feedstock businesses (e.g., RHI Magnesita’s purchase moves) to secure quality and reduce volatility.
2. Regional challengers and Chinese manufacturers: Lower-cost suppliers are increasing capacity and technical capability; large cement groups in Asia often source locally, pressuring pricing and forcing global suppliers to differentiate on performance, warranties and service.
3. Specialist technology start-ups: Firms focusing on 3D-printing of refractory shapes, sensor embedding or novel binder chemistries are becoming acquisition targets for established players.
For procurement teams, this means re-assessing TCO: supplier choice is now as much about data services, installation competence, and lifecycle guarantees as it is about price per ton of bricks.
Where are costs headed?
Costs for refractory systems will be driven by four linked forces:
1. Raw-material price pressure: Prices of magnesia, bauxite/alumina and specialty clays move with energy, mining constraints and geopolitical supply; vertical integrations indicate producers expect sustained volatility.
2. Capex for decarbonisation: Retrofits for oxy-fuel, electrification, CCS readiness, and hydrogen blending often require modified kiln internals and more frequent, higher-quality linings; these add upfront cost but can lower total emissions and long-term operating risk.
3. Service and digital premiums: Sensorised systems, data analytics and condition-based maintenance contracts add cost but lower unplanned downtime and extend campaign life — often commercially attractive for large plants.
4. Regional divergence: Costs will diverge geographically. Plants in jurisdictions with strong carbon pricing, subsidies for CCS, or higher electricity costs will see different economics than plants in low-cost coal regions. Market reports forecast moderate refractory price inflation overall, but with pockets of higher increase tied to feedstock bottlenecks and decarbonisation capex.
Practical recommendations for senior engineers and CMOs and CPOs:
1. Embed refractory strategy in decarbonisation planning: Any decision to scale biomass, oxy-fuel, hydrogen or CCS must have a refractory impact assessment and budget for both material and installation adaptations.
2. Specify for monitorability: Require suppliers to support embedded sensors and data interfaces; insist on warranties that link lining life to clearly defined operating envelopes.
3. Partner on trials: Work with one global and one regional supplier on co-funded trials for 3D-printed shapes, new monolithic mixes, or sensorised linings — accelerate learning before full retrofit.
4. Stress test supply chains: Given recent upstream consolidation, model raw-material failure modes and engage in off-take agreements or joint-stock buffering where alumina or magnesia supplies are strategic.
5. Financially model TCO, not unit price: Factor in longer campaign life, reduced outage probability, and digital services when comparing quotes.
Conclusion
Refractories and pyro-processing are no longer ‘just materials.’ They are strategic assets that determine whether a cement plant can safely and economically transition to lower-carbon fuels and new heat sources. The coming decade will be shaped by a mixture of material science advances (3D printing, sensorised linings, hybrid systems), operational technologies (electrified heat, oxy-fuel, CCS), and shifting supplier dynamics (vertical integration and new entrants). Senior engineers must therefore treat refractory strategy as a cross-functional lever — part of the decarbonisation, reliability and procurement playbook — and design decisions with total cost, not short-term price, at the fore.
About the author:
Professor Procyon Mukherjee, ex-CPO Lafarge-Holcim India, ex-President Hindalco, ex-VP Supply Chain Novelis Europe, holds deep expertise in logistics, procurement, operations and supply chain management. An author and academic, he now teaches at leading institutions and advises global firms on SCM, industrial leadership, and the aluminum and cement sectors.
Concrete
ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown
Published
1 week agoon
November 12, 2026By
admin
ABB reconditions 25 drives at ACC’s Jamul cement plant, avoiding 16 tonnes of CO₂ emissions while improving reliability through predictive maintenance.
Chhattisgarh
ABB has signed a multi-year Motion OneCare service agreement with ACC Limited, part of the Adani Group, to modernise ageing industrial drives at its Jamul cement plant in Chhattisgarh, improving operational reliability while avoiding approximately 16 tonnes of carbon dioxide (CO₂) emissions without disrupting production.
Announced on 27 October 2026, the agreement combines scheduled drive reconditioning, digital condition monitoring and energy appraisals to extend equipment lifespan, improve plant uptime and optimise maintenance costs. The initiative marks a shift from conventional equipment replacement towards a more resource-efficient approach to industrial asset management.
The first phase, completed in April 2026, involved the on-site reconditioning of 25 ABB ACS800 variable speed drives without a major plant shutdown. By retaining the existing cabinets and restoring the drive modules rather than replacing entire panels, ABB helped ACC preserve capital investment, minimise material consumption and avoid approximately 16 tonnes of CO₂ emissions.
A second phase, covering an additional 25 ACS800 drive modules, is scheduled for the fourth quarter of 2026. The programme is designed to improve long-term equipment reliability while allowing maintenance activities to be aligned with the plant’s operational schedules.
The ACS800 drives, installed at Jamul in 2010, had delivered more than a decade of near-continuous service in demanding cement manufacturing conditions. However, ageing electrical components and changing fault patterns had begun to affect their ability to meet the plant’s reliability requirements.
Rather than opting for complete equipment replacement, ACC engaged ABB’s certified engineers to conduct a comprehensive asset health assessment. The evaluation found that the existing cabinets and enclosures remained structurally sound, making targeted reconditioning a technically viable and cost-effective alternative to full replacement.
Drawing on nearly two decades of experience with ACC’s equipment and operating requirements, ABB developed a maintenance framework tailored to the plant’s shutdown windows, budget cycles and production priorities.
The Motion OneCare agreement incorporates planned equipment restoration, condition-based monitoring and energy assessments, enabling ACC to adopt a more systematic approach to maintaining critical electrical infrastructure.
As part of the programme, ACC has implemented ABB Ability™ Digital Powertrain Insights to monitor drive performance and identify emerging operational issues before they result in equipment failures.
The digital platform provides continuous visibility into parameters such as temperature, current, vibration and fault patterns. These insights allow maintenance teams to detect early signs of equipment deterioration, schedule interventions more effectively and reduce the likelihood of unexpected downtime.
Amit Gupta, Local Division Manager, Motion Services, ABB India, said: “We know what unchecked wear costs over time: a small inefficiency that eats away at ROI for years. At Jamul, the evidence pointed clearly to assets with productive life still in them.”
“Our job was to restore them properly and give the team the tools to stay ahead of the next problem. At ABB, we don’t just fix what fails. We want to protect what works.”
The initiative also demonstrates the growing relevance of circular economy principles in cement manufacturing, where extending the service life of existing industrial equipment can reduce capital expenditure, material consumption and the environmental impact associated with manufacturing replacement components.
According to ABB, drive reconditioning can reduce lifecycle emissions by 50 to 80 per cent compared with complete equipment replacement. By preserving functional components and restoring critical modules, the process helps retain the economic and material value of existing industrial assets.
The addition of energy appraisals in subsequent phases will further expand the programme beyond equipment restoration, enabling ACC to assess drive performance, identify energy-saving opportunities and improve operating efficiency.
For cement manufacturers, variable speed drives play an important role in controlling motors and optimising energy consumption across production processes. Maintaining their reliability and efficiency is essential for minimising operational disruptions and managing electricity costs.
Vinod Bahety, CEO – Cement Business, Adani Group, said: “Moving from reactive firefighting to a structured maintenance plan was exactly what this operation needed. That kind of peace of mind doesn’t come easily. It comes from a partner that understands how your business runs.”
“We didn’t need a full system overhaul; we needed expert support, actionable insights, and a plan we could execute around our schedule. That’s what we got.”
The project supports ACC’s broader strategy to improve manufacturing efficiency through digital transformation, preventive maintenance and sustainable asset management.
ACC, a subsidiary of Ambuja Cements and part of the Adani Group, operates 20 cement manufacturing facilities and 119 ready-mix concrete plants across India. The company has been advancing initiatives focused on renewable energy, circular economy practices and technology-driven operational improvements.
Alongside Ambuja Cements, ACC is part of a large-scale building materials business committed to achieving net-zero emissions by 2050, with near-term and net-zero targets validated by the Science Based Targets initiative (SBTi).
The Jamul initiative aligns with these sustainability objectives by demonstrating how equipment life extension and digital monitoring can contribute to resource efficiency without requiring large-scale replacement of existing infrastructure.
ABB, a global technology company specialising in electrification and automation, brings more than 140 years of industrial expertise and employs approximately 110,000 people worldwide. Its Motion Services business supports industrial customers through equipment maintenance, modernisation, digital monitoring and lifecycle management solutions.
The agreement also reflects a wider shift in industrial maintenance practices, with manufacturers increasingly adopting predictive technologies to improve equipment availability, manage costs and reduce unplanned shutdowns.
With 25 drives already reconditioned and another 25 scheduled for restoration, ABB’s collaboration with ACC illustrates how targeted modernisation, digital monitoring and circular maintenance practices can extend the operational life of critical equipment while supporting more efficient and sustainable cement production.
Concrete
ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K
Published
1 week agoon
November 12, 2026By
admin
ABB deploys advanced process control at TCI MAX’s Srinagar cement plant to improve clinker quality, energy efficiency and sustainable manufacturing.
Kashmir
ABB has deployed its advanced process control technology at TCI MAX Cement’s Srinagar facility in Jammu and Kashmir, marking the region’s first reported implementation of advanced process control (APC) in cement manufacturing and strengthening efforts towards more efficient, digitally enabled production.
Announced on 5 November 2026, the deployment of ABB Ability™ Expert Optimizer at the facility, operated by Trumboo Industries Pvt. Ltd., aims to improve process stability, clinker quality, energy efficiency and overall plant productivity. The implementation forms part of TCI MAX’s strategy to modernise its manufacturing operations through automation and digital technologies.
Following the integration of ABB’s advanced process control solution and supporting IT infrastructure, TCI MAX has reported improvements in operational productivity, product quality and sustainability-related performance indicators. The technology focuses on optimising the cement pyro process, a critical stage of production involving high-temperature processing and clinker formation.
Waseem Ahmed Trumboo, Director, Trumboo Industries Pvt. Ltd., said: “Introducing advanced process control at TCI MAX is an important step in how we are evolving our operations. Our focus is on improving the stability and efficiency of our processes while maintaining consistent clinker quality. We have been encouraged by the performance of the solution during commissioning and by the support from the ABB team, and we look forward to realizing its full potential.”
ABB Ability™ Expert Optimizer combines advanced process control, model predictive control (MPC) and artificial intelligence (AI) to continuously monitor and optimise manufacturing operations. By analysing process conditions, predicting operational behaviour and automatically adjusting key parameters, the system enables more consistent production while reducing process variability.
In cement manufacturing, maintaining stable pyro-processing conditions is essential for achieving uniform clinker quality and optimising thermal energy consumption. Fluctuations in operating parameters can affect fuel efficiency, production output and product consistency.
The deployment is designed to address these challenges through real-time process optimisation, helping operators maintain more stable kiln operations while improving the utilisation of fuel, electricity and raw materials.
Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries Division, ABB India, said: “Cement producers are increasingly looking to adopt digital technologies to achieve greater consistency and efficiency while addressing their sustainability priorities. ABB Ability™ Expert Optimizer brings advanced process control and deep cement process expertise together to help operators make their processes more stable and efficient. We are pleased to support TCI MAX as it takes this important step in its digital transformation.”
The technology also supports sustainability objectives by optimising fuel consumption, improving electrical energy efficiency and minimising process waste. More stable operations can contribute to lower energy intensity and reduced emissions associated with cement production.
For TCI MAX, the investment represents a move towards data-driven manufacturing, where automated control systems complement operator expertise to improve production performance and operational reliability.
The implementation is particularly significant for Jammu and Kashmir’s cement industry, as it introduces advanced process optimisation technology to a regional manufacturing facility. Its deployment could demonstrate the potential for wider adoption of digital automation across cement plants seeking to modernise their operations.
The project builds on ABB’s experience in delivering advanced process control solutions to cement manufacturers worldwide. Through the integration of industrial automation, predictive technologies and process engineering expertise, the company supports manufacturers in improving resource efficiency and maintaining consistent production quality.
As cement producers face increasing pressure to manage energy costs, improve productivity and reduce their environmental footprint, technologies such as AI-enabled process control and predictive optimisation are becoming important components of plant modernisation strategies.
ABB’s Expert Optimizer provides a platform for addressing these priorities by enabling automated adjustments based on changing process conditions, reducing reliance on manual intervention and supporting more efficient plant operation.
ABB, a global technology company specialising in electrification and automation, has more than 140 years of industrial experience and approximately 110,000 employees worldwide. Its Automation business employs around 26,000 people and provides technologies and services across process, hybrid and maritime industries.
The TCI MAX deployment reinforces ABB’s growing role in the digital transformation of cement manufacturing in India, where improving process efficiency and reducing energy consumption remain critical to the industry’s long-term sustainability.
With the advanced process control system now implemented at its Srinagar facility, TCI MAX aims to build on the initial operational improvements and further optimise production efficiency, clinker consistency and environmental performance.
Concrete
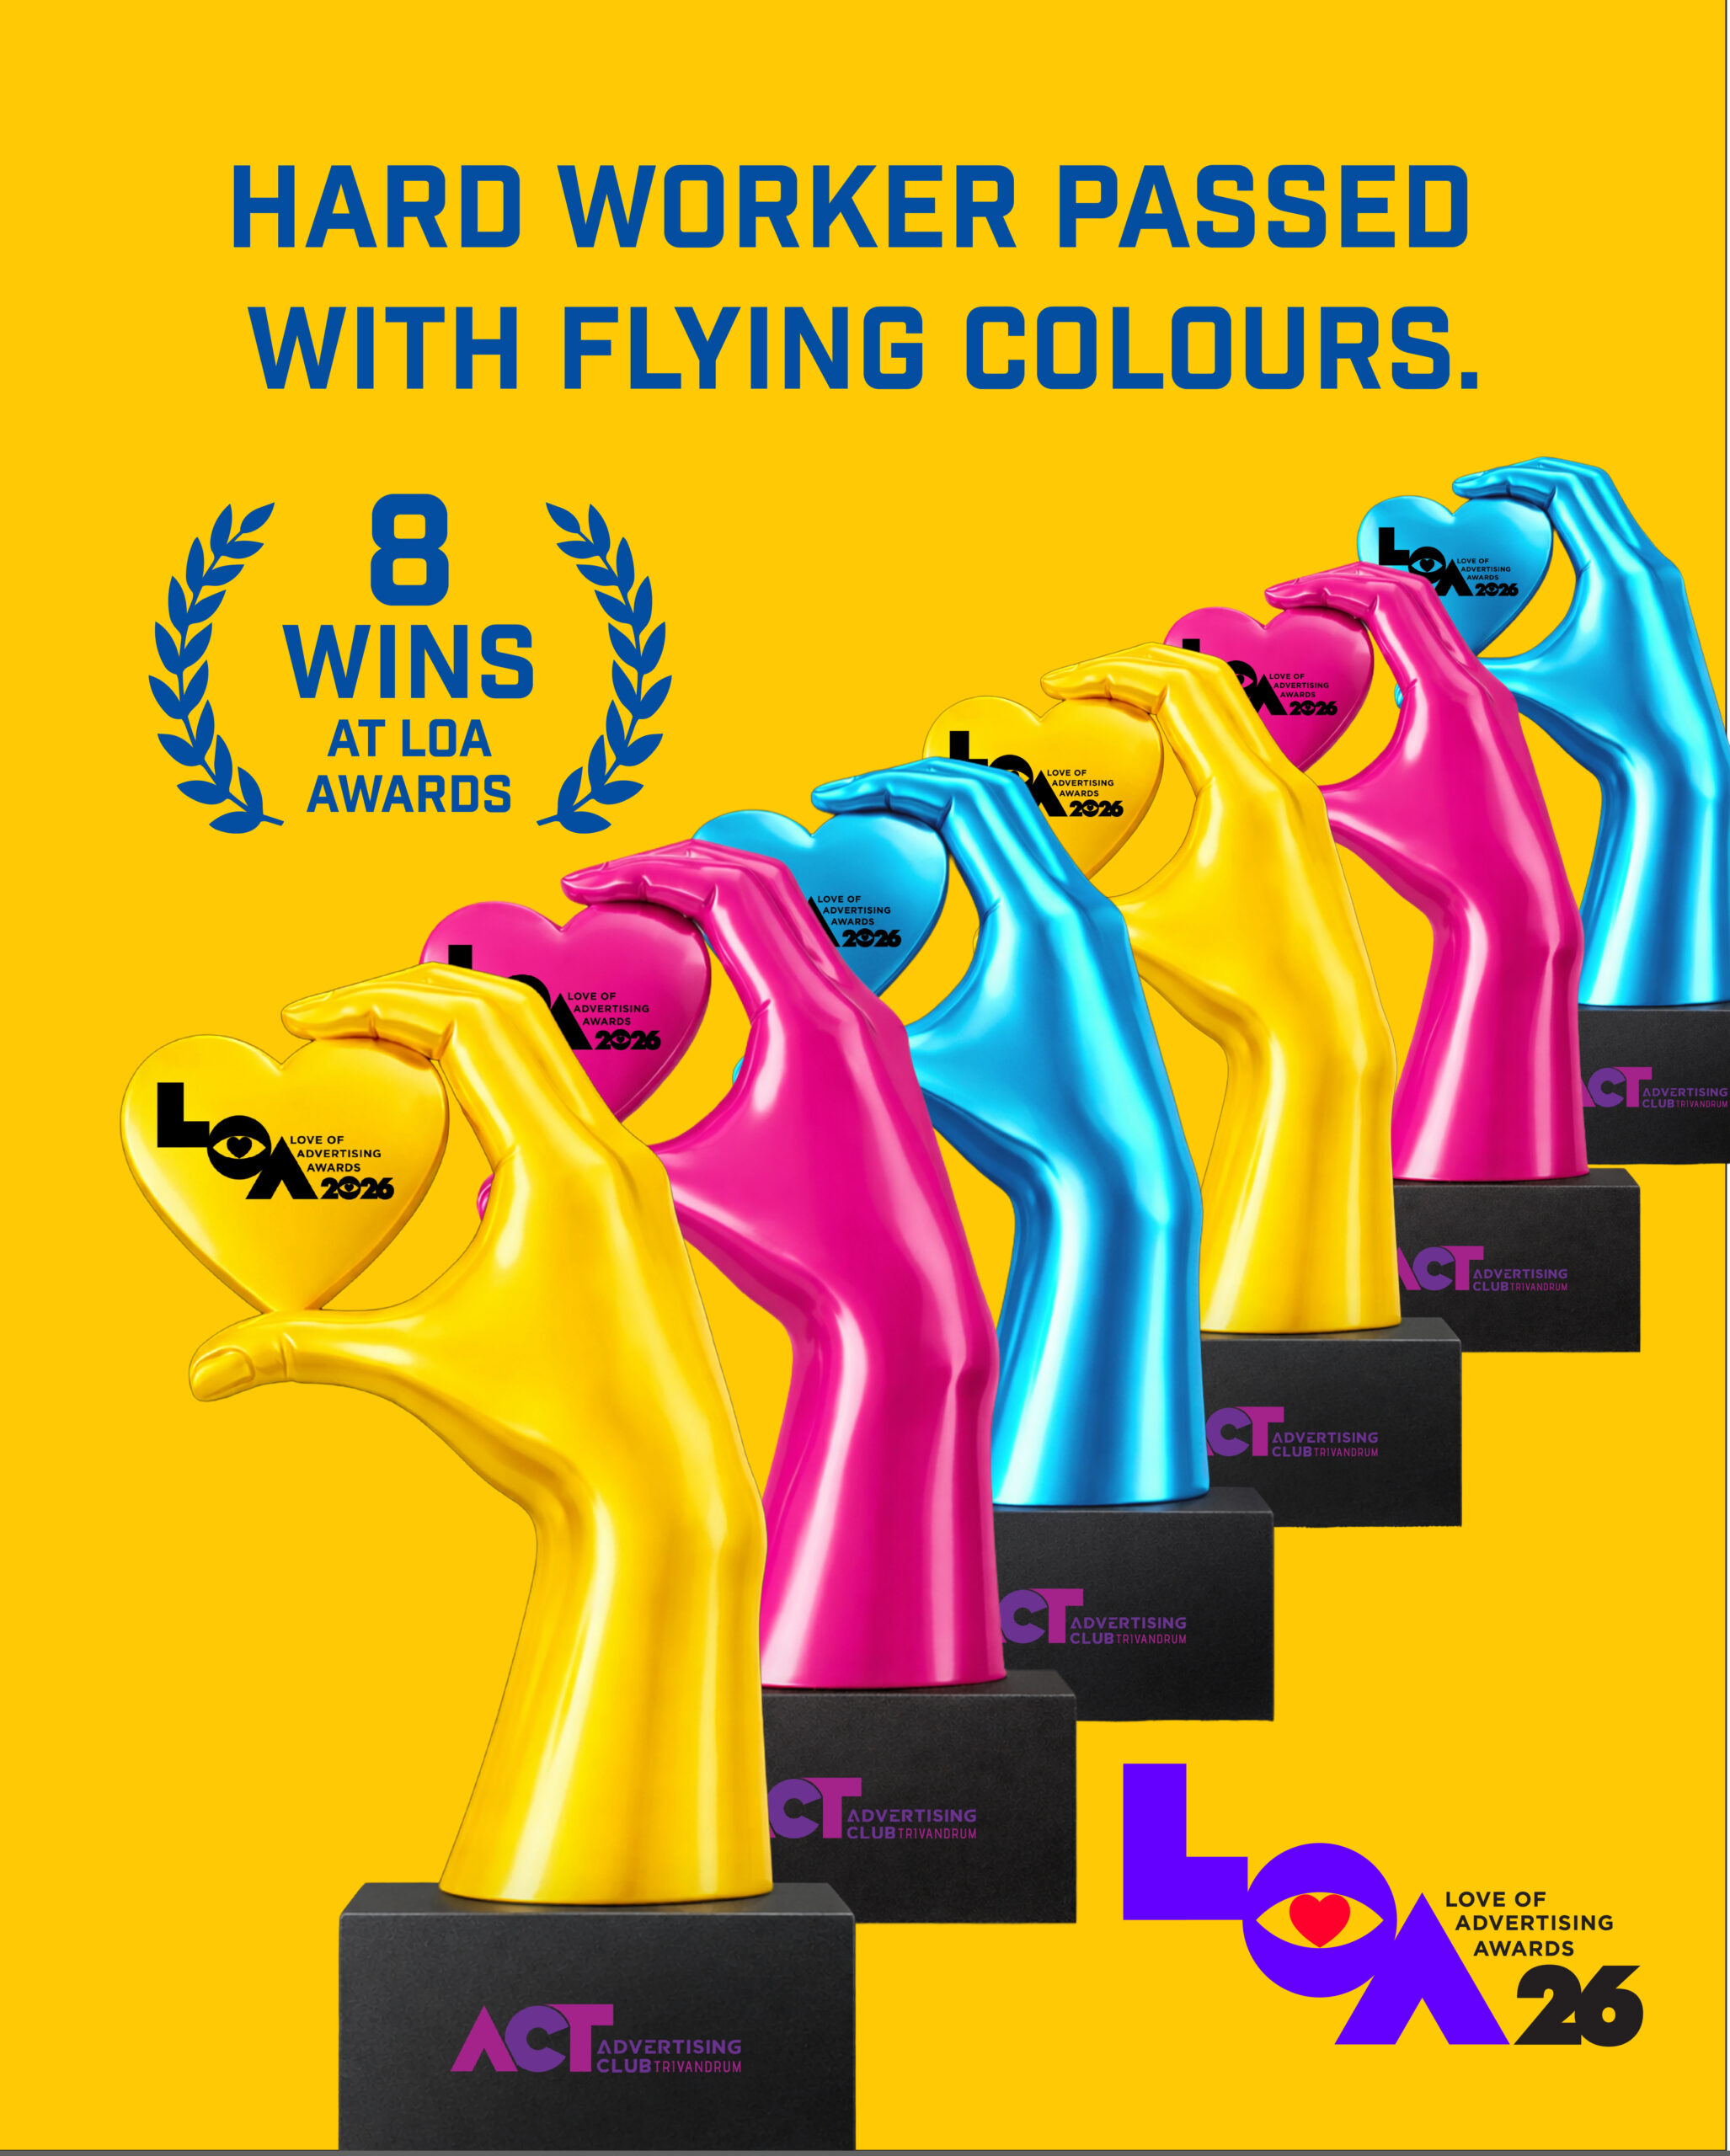
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’
Published
1 week agoon
November 12, 2026By
admin
Ramco Cements’ Hard Worker brand wins eight awards for excellence in advertising, packaging and brand identity at the Love of Advertising Awards 2026.
Hyderabad
The Ramco Cements Limited’s construction chemicals brand, Hard Worker, has secured eight awards at the Love of Advertising Awards 2026, recognising its creative excellence across television, digital advertising, packaging design and brand identity.
Organised by the Advertising Club of Trivandrum, the awards were presented at a ceremony held at The Leela Raviz, Kovalam, on 24 October 2026. The recognition highlights Hard Worker’s integrated marketing strategy and its efforts to establish a distinctive presence in India’s competitive construction chemicals market.
The eight awards span multiple creative categories, reflecting the brand’s approach to combining product-focused communication with engaging storytelling, humour and innovative design. Through its campaigns, Hard Worker has sought to simplify technical product benefits and make construction chemicals more accessible and relatable to consumers and construction professionals.
Built around the philosophy of “Hard-working products for hardworking people”, the brand focuses on communicating practical product advantages through memorable advertising narratives while maintaining a consistent identity across different marketing platforms.
Its campaigns for Ramco Hard Worker Eco Plaster and Tile Fix have been central to this approach. The Eco Plaster campaign highlights water conservation through the product’s self-curing properties, positioning it as a solution that supports more efficient construction practices. Meanwhile, Tile Fix promotes specialised tile-fixing solutions by presenting their practical benefits through relatable situations and creative storytelling.
Beyond advertising, Hard Worker has invested in distinctive packaging and brand identity development to improve product recognition and maintain consistency across customer touchpoints. This integrated approach has helped the brand differentiate itself in a category where marketing communication has traditionally focused on technical specifications and functional performance.
A V Dharmakrishnan, CEO, Ramco Cements, said, “Winning eight awards at the Love of Advertising Awards is a proud moment for Ramco Cements and the Hard Worker team. We believe that building a strong brand requires not only quality products but also the ability to communicate their value in a compelling and differentiated manner. Hard Worker’s journey reflects our commitment to combining product performance with innovative marketing to create meaningful connections with our customers and strengthen our presence in the construction chemicals market.”
The recognition comes as building materials manufacturers increasingly focus on brand differentiation, product awareness and customer engagement to strengthen their position in the construction chemicals segment.
By using humour and storytelling to explain product applications and benefits, Hard Worker aims to bridge the communication gap between technical construction solutions and the practical requirements of contractors, applicators and end-users.
Balaji K. Moorthy, Executive Director – Marketing, Ramco Cements, said, “Hard Worker was conceived to bring a fresh perspective to the construction chemicals category, where product communication has traditionally been functional and technical. Our endeavour has been to break through the clutter with distinctive ideas, humour and storytelling, while keeping the product proposition at the heart of every campaign. The recognition across TV and digital advertising, packaging design and brand identity design demonstrates our integrated approach to building the brand. These eight awards are an encouraging recognition of the creative thinking and collaborative effort behind Hard Worker’s marketing initiatives.”
The awards add to Hard Worker’s growing portfolio of creative recognitions and reinforce Ramco Cements’ emphasis on integrating product innovation with strategic marketing.
The brand’s communication initiatives also reflect a wider shift in the construction materials industry, where manufacturers are increasingly adopting consumer-focused marketing strategies to improve product understanding and strengthen relationships with construction professionals.
With its portfolio of construction chemicals, Hard Worker aims to address evolving requirements for durability, application efficiency and construction quality. Its marketing efforts seek to complement these product attributes by building stronger awareness and encouraging the adoption of specialised construction solutions.
Ramco Cements, one of India’s established cement manufacturers, operates across cement and allied building solutions. Through Hard Worker, the company is expanding its presence in the construction chemicals segment with products designed to enhance performance, quality and durability in modern construction applications.
The latest recognition strengthens Hard Worker’s brand visibility and underscores the growing importance of creative communication in promoting technical building materials. Ramco Cements intends to continue combining product development with distinctive marketing initiatives to support the brand’s growth in India’s construction chemicals market.
NCL Industries Approves Rs. 5.95 bn Solar-Wind Investment
Cement Makers See Margin Relief as Oil Prices Lower Fuel Costs
ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown
ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’
NCL Industries Approves Rs. 5.95 bn Solar-Wind Investment
Cement Makers See Margin Relief as Oil Prices Lower Fuel Costs
ABB Extends Drive Lifespan at ACC Cement Plant Without Production Shutdown
ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’
Trending News
-
Concrete4 weeks agoNuvoco reports 13.5% revenue growth in Q2 FY27
-
Concrete4 weeks agoUltraTech Cement Expands in Andhra Pradesh with Rs. 26.5 bn
-
Concrete3 weeks agoCII Calls for Greater Alternative Fuel Use in Cement Industry
-
Concrete2 weeks agoShree Cement Expands Bangur Concrete Network with Patna Plant