Refractories are vital to cement manufacturing, ensuring efficiency, durability, and sustainability in pyroprocessing. Innovations in materials, technology and recycling are transforming the industry while advancing its environmental goals.
The cement industry operates in a challenging environment of extreme temperatures, chemical reactions, and mechanical stresses, particularly during pyroprocessing. As the backbone of cement manufacturing, pyroprocessing transforms raw materials into clinker by subjecting them to temperatures of up to 1450°C. Refractories play a vital role in ensuring the efficiency, durability, and sustainability of this process by protecting equipment and enabling the process to endure hostile conditions.
This article explores the critical role of refractories in pyroprocessing, the advancements in technology improving efficiency, and the integration of sustainability in cement manufacturing through innovative refractory solutions.
Fundamentals of pyroprocessing and refractories
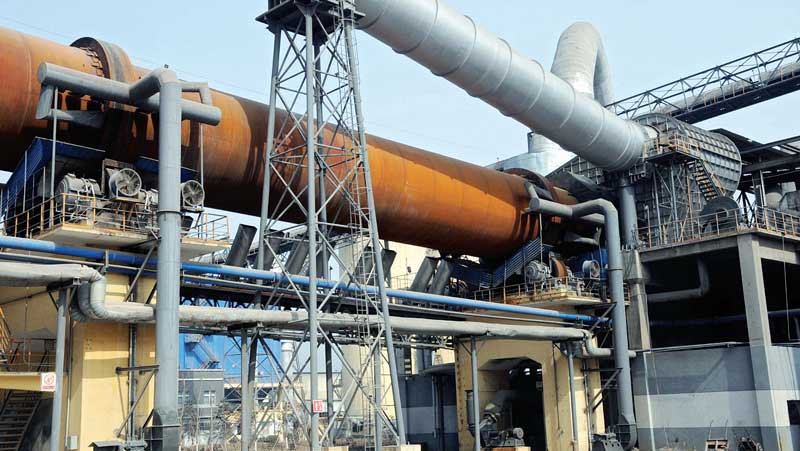
Pyroprocessing is a key stage in cement manufacturing, encompassing calcination, sintering, and fusion processes in high-temperature environments. The rotary kiln, the centrepiece of this stage, requires robust refractory linings to withstand extreme conditions, including high heat, abrasion, and chemical corrosion.
Refractories, crafted from materials like fireclay, high alumina, magnesia, and dolomite, form the protective shield of kilns, preheaters, and coolers. These materials are tailored to specific zones within the kiln, such as the:
- Burning zone: Magnesia-spinel and high alumina bricks are commonly used for their ability to resist extreme heat and mechanical stress.
- Preheater zone: Alumina-silicate refractories are selected for their thermal shock resistance and insulating properties.
- Cooling zone: Abrasion-resistant castables provide durability under high mechanical wear.
Mayank Gugalia, Director, Mahakoshal Refractories, says, “Our company focuses exclusively on alumina refractories, setting us apart from competitors. While others may diversify into basic refractories or flow controls, we prioritise becoming the best in the alumina segment. In terms of volume, we are among India’s largest manufacturers, and our quality standards have earned us a leading position domestically and in export markets, including the Middle East and Europe. Our commitment to sustainability further strengthens our reputation as a trusted and environmentally responsible manufacturer.”
For example, an Indian cement plant reported a 10 per cent reduction in fuel consumption after upgrading to magnesia-spinel bricks in the burning zone, demonstrating how material choices directly impact operational efficiency.
Challenges and advances in refractory performance
Refractories face multiple stressors, including:
- Chemical corrosion: Aggressive reactions from alternative fuels and raw materials can degrade linings.
- Thermal shock: Rapid temperature fluctuations can cause cracking and spalling.
- Mechanical wear: Continuous abrasion from clinker and raw materials erodes refractory surfaces.
Increased use of alternative fuels such as industrial waste adds another layer of complexity. These fuels can introduce unburned residues and chemical byproducts, accelerating refractory degradation.
Mayank Kamdar, Marketing Director, Lilanand Magnesite, says, “One of the biggest challenges in the refractory industry is the reliance on natural mineral resources. As these resources are finite, their quality can vary, which poses a challenge in ensuring consistent product quality. To address this, we explore new sources for raw materials and also develop synthetic products that offer consistent quality. By doing so, we ensure that our products meet the high standards required by our customers, even as natural resources become scarcer.”
“We are always striving to improve our products through continuous research and development. Currently, one of the key areas of focus is adapting our products to the increasing use of alternative fuels and municipal waste in cement kilns. Over the years, we have developed specialised products designed to withstand the challenging environments created by the burning of alternative fuels. For example, we offer anti-coating castables that are highly durable and suited for use in areas such as the kiln inlet, where AFR and municipal waste are burned,”
he adds.
To counter these challenges, the industry has developed advanced solutions:
- Active spinel technology: Improves resistance to slag attack and enhances thermal stability, especially in burning zones.
- Nanotechnology in refractories: Nano-bonded castables demonstrate up to 30 per cent higher strength, better insulation and resistance to thermal shocks.
- IS impregnation: This innovative method enhances density and corrosion resistance in alumina-based refractories, prolonging their lifespan.
Shreesh A Khadilkar, Consultant and Advisor, and Former Director Quality and Product Development, ACC, explains, “Reducing conditions can have substantial effects on clinker quality like problems with sulphur integration, Alite decomposition (strength reduction), conversion from C4AF to C3A (acceleration of setting), change in color of cement (from greenish grey to brownish), the detection of reducing conditions could be done using ‘Magotteaux Test’, it is important to assess the reducing conditions whether internal or peripheral, would indicate possible reasons.”
“Internal reducing conditions indicate that due to changes in liquid viscosity the larger clinker nodules are black from outside but yellow to brownish in the internal core. Such clinker nodules roll down from the transition zone with an unburnt core which disintegrates on cooling due to gamma C2S. Such nodules have high free lime, delocalised or peripheral reducing conditions due to larger size of solid AFR component (shredded size) showing CO peaks,”he adds.
For example, a cement plant using high-chrome refractories successfully transitioned to using 70 per cent alternative fuels, withstanding the increased chemical stress and maintaining operational reliability.
Role of technology in pyroprocessing
Modern technologies are revolutionising pyroprocessing by making it more efficient and precise. Key advancements include:
- Digital monitoring and IoT integration: Smart refractories embedded with sensors provide real-time data on temperature, stress and wear patterns. This enables predictive maintenance, reducing unplanned downtimes and extending the life of kiln linings.
- Simulation and modelling tools: Computational Fluid Dynamics (CFD) and thermodynamic modelling help optimise kiln design and refractory placement. These tools predict thermal loads and chemical reactions, ensuring that refractory materials are matched precisely to process requirements.
- Robotic installation: Automated systems for lining kilns ensure uniform installation, reducing human error and improving refractory performance.
- Artificial intelligence (AI): AI-driven systems analyse process data to optimise fuel usage, kiln rotation speeds, and temperature profiles, enhancing both energy efficiency and refractory durability.
“Technology plays a critical role in achieving our goals and supporting the cement industry. As I mentioned earlier, the reduction in specific refractory consumption is driven by two key factors: refining customer processes and enhancing refractory quality. By working closely as partners with our customers, we gain a deeper understanding of their evolving needs, enabling us to continuously innovate. For example, in November 2022, we established a state-of-the-art research centre in India for IFGL, something we didn’t have before,” says Arasu Shanmugam, Director and CEO India, IFGL.
“The primary objective of this centre is to leverage in-house technology to enhance the utilisation of recycled materials in manufacturing our products. By increasing the proportion of recycled materials, we reduce the depletion of natural resources and greenhouse gas emissions. In essence, our focus is on developing sustainable, green refractories while promoting circularity in our business processes. This multi-faceted approach ensures we contribute to environmental sustainability while meeting the industry’s demands,” he elaborates.
Such innovations help cement plants operate at peak efficiency, improving both productivity and sustainability.
Sustainability in cement manufacturing
The cement industry is under growing pressure to reduce its carbon footprint, and pyroprocessing plays a crucial role in achieving sustainability goals. Refractories, often overlooked in this context, are key enablers of sustainable practices.
“IKN plays a pivotal role in enhancing the operational efficiency of cement plants while aligning with global sustainability objectives. Historically, clinker coolers required frequent maintenance, with intervals as short as five to six months. This led to regular shutdowns, which disrupted operations and increased costs. With IKN’s advanced cooling solutions, cement plants can now operate their coolers for extended periods without significant maintenance. Our coolers are not only more reliable but also consume less power, which directly reduces energy costs. Additionally, the high heat recuperation efficiency of our systems ensures that less fuel is required for the cement-making process, contributing to a lower carbon footprint. Sustainability is embedded in our solutions. By reducing energy consumption, optimising processes, and minimising maintenance, we help our customers achieve their operational goals while supporting their commitment to environmental stewardship,” says Madhusudan Rasiraju, Country Head, IKN India.
Refractory recycling and circular economy: Used refractory linings are now being recycled to recover valuable raw materials like alumina and magnesia. This reduces waste and conserves natural resources. For instance, a medium-sized cement plant can recycle up to 30 per cent of its refractory waste annually, cutting down disposal costs and environmental impact.
Energy efficiency through advanced materials: High-performance refractories with low thermal conductivity reduce heat loss from kilns, improving energy efficiency. Magnesia bricks, for example, retain heat better, lowering fuel consumption by as much as 15 per cent.
Compatibility with alternative fuels: Sustainability efforts often involve transitioning to alternative fuels such as biomass and waste-derived fuels. Advanced refractory technologies are designed to withstand the chemical and thermal stresses associated with these fuels, enabling their wider adoption.
Low-carbon manufacturing of refractories: Manufacturers are now adopting eco-friendly processes to produce refractories. Innovations like solar calcination for raw materials and carbon-neutral binders are setting new benchmarks for sustainability.
“Sustainability is a key priority for us, and we have been actively engaged in decarbonisation efforts for many years. We launched our sustainability program five years ago, with a clear focus on reducing the environmental impact of our operations. Over time, we have become leaders in this space, particularly with the advent of hydrogen technology. We were one of the pioneers in the hydrogen sector, not only in developing hydrogen combustion solutions but also in the liquefaction of hydrogen for use in various industrial applications. In fact, we were the first company in India to sell a hydrogen burner, which was used for a 52-megawatt boiler application. Beyond hydrogen, we are also focused on finding alternative solid fuels for cement manufacturing. We are currently working on developing hybrid technologies that combine hydrogen, alternative solid fuels, and fossil fuels. This combination is crucial for reducing the carbon footprint in the cement industry. We are continuously investing in research and development to create innovative solutions that can accelerate the global shift toward decarbonisation,” says Rahul Rajgor, Managing Director, Fives Combustion.
By integrating these practices, the cement industry is making strides toward achieving net-zero emissions while maintaining operational efficiency.
Economic and operational impact
While refractory materials constitute only 2-3 per cent of total cement plant costs, their impact on efficiency and profitability is immense. Proper refractory selection, combined with advanced installation and maintenance techniques, can save plants hundreds of thousands of dollars annually. For example, extending the lifespan of linings in the preheater zone by six months can reduce maintenance costs by $200,000. Similarly, using high-quality castables in cooling zones has been shown to decrease clinker cooling times, boosting production output.
Conclusion
Refractories are the unsung heroes of cement manufacturing, ensuring the efficiency and resilience of pyroprocessing operations. Advances in technology and material science continue to push the boundaries of refractory performance, while sustainability initiatives are transforming how refractories are produced, used, and recycled.
As the cement industry evolves to meet global demands for efficiency and sustainability, refractories will remain at the forefront, enabling the industry to tackle its most critical challenges with innovation and precision. By prioritising high-quality materials, embracing technology and adopting sustainable practices, the cement industry can secure a future that balances profitability with environmental responsibility.
– Kanika Mathur















 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago

 Concrete4 weeks ago