Efficient bulk material handling has always been critical for seamless production, cost reduction and environmental compliance. Kanika Mathur delves into advanced automation, smart sensors and sustainable transport solutions that are key to overcoming challenges.
The cement industry is a cornerstone of infrastructure development, contributing significantly to economic growth. However, cement production involves the handling and transportation of vast quantities of raw materials such as limestone, clay, iron ore, fly ash and gypsum, as well as the final product—cement itself. Efficient bulk material handling (BMH) systems are crucial in ensuring uninterrupted production, reducing operational costs, minimising material wastage and improving overall efficiency.
In an industry where material losses, dust emissions, and energy consumption are major concerns, advancements in bulk material handling technology are playing a vital role in optimising operations. Automated and energy-efficient bulk handling solutions, such as pneumatic conveying systems, belt conveyors and stacker-reclaimer systems, are transforming the way cement plants manage their raw materials and finished products. This article explores the key aspects of bulk material handling in the cement industry, the latest technological advancements, and the challenges and opportunities in this space.
Importance of bulk material handling
Cement manufacturing requires the continuous movement of raw materials from mines and quarries to processing plants, followed by the transportation of the finished product to storage facilities and distribution networks. Bulk material handling systems ensure that this process runs smoothly, reducing downtime and enhancing productivity.
According to the Global Cement Report (2023), inefficient material handling contributes to 5 – 10 per cent of total cement production losses in India. Additionally, poor handling practices lead to high levels of dust pollution, which is a significant environmental and health concern. With cement production in India expected to reach 500 million metric tonnes by 2025, the demand for advanced and automated material handling systems is increasing rapidly.
Jacob Jose, CEO and Managing Director, Methods India, says, “With our advanced pipe conveyors, downhill conveyors and cross-country conveyors, we have revolutionised the way cement plants transport raw materials. Our technology helps reduce operational costs, minimise environmental impact and improve energy efficiency. Over the years, we have observed a positive impact in the industry, particularly with the growing adoption of pipe conveyors and cross-country conveyors, which have proven to be more efficient and environmentally friendly alternatives to traditional transport methods.”
Key bulk material handling technologies
1. Belt conveyors: The workhorse of cement plants
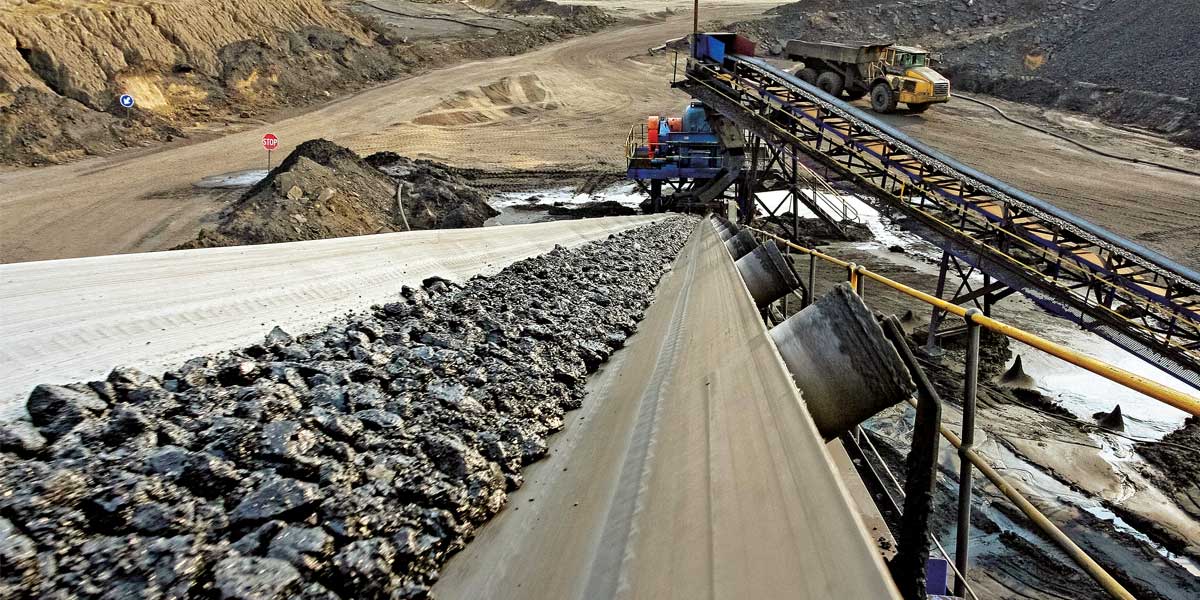
Belt conveyors are one of the most widely used bulk material handling solutions in the cement industry. They transport raw materials, clinker and finished cement over long distances within the plant and to storage facilities. Modern high-capacity belt conveyors can handle loads exceeding 10,000 tonnes per hour, significantly improving efficiency.
- Advantages: High efficiency, low operational costs, and reduced manual intervention.
- Challenges: Belt wear and tear, spillage, and maintenance requirements.
- Technological advancement: The introduction of heat-resistant and fire-retardant conveyor belts has improved durability, while sensor-based predictive maintenance systems help detect belt failures before they occur.
2. Stacker and reclaimer systems: Optimising storage and retrieval
Stackers and reclaimers are essential for managing bulk raw materials in cement plants. Stackers pile materials such as limestone, coal, and gypsum, while reclaimers retrieve them for processing. These systems ensure homogeneous blending, reducing material variability and enhancing cement quality.
- Latest innovation: Automated stacker and reclaimer systems with AI-driven optimisation help maximise storage space and minimise
retrieval time.
- Efficiency gains: Newer stacker-reclaimer designs allow for material recovery rates of over 90 per cent, reducing wastage and ensuring a steady feed to the production line.
3. Pneumatic conveying systems: Dust-free material transfer
Pneumatic conveying systems use air pressure or vacuum systems to move powdered and granular materials such as fly ash, cement and kiln dust through pipelines. They are particularly useful in reducing dust emissions and preventing material contamination.
- Advantages: Dust-free operation, reduced environmental impact, and minimal maintenance.
- Industry adoption: Many Indian cement plants are shifting from mechanical conveyors to high-pressure pneumatic conveying systems to comply with pollution control regulations set by the Central Pollution Control Board (CPCB).
4. Screw conveyors and bucket elevators: Compact and versatile solutions
- Screw conveyors: Used for short-distance material movement, particularly for handling fine and powdered materials such as cement, gypsum, and pulverised coal.
- Bucket elevators: Ideal for vertical material transport, commonly used for lifting raw meal, cement, and clinker to storage silos.
- Technological upgrades: The introduction of wear-resistant alloy buckets and variable-speed drives has enhanced the reliability and efficiency of these systems.
Challenges in bulk material handling
Despite significant advancements, several challenges continue to hinder bulk material handling efficiency in cement plants:
1. Material spillage and dust emissions
Material spillage and dust emissions pose environmental, health, and financial challenges. Uncontrolled dust emissions from conveyors, transfer points, and storage facilities not only violate regulatory norms but also lead to material losses. Studies show that up to three per cent of bulk materials are lost due to improper handling in Indian cement plants.
- Solution: Enclosed conveyors, dust suppression systems, and bag filters help reduce dust pollution.
2. High energy consumption
Bulk material handling systems consume a significant amount of energy, especially in large cement plants where materials need to be transported over long distances. According to a CII (Confederation of Indian Industry) report (2023), energy costs account for nearly 40 per cent of total production expenses in cement manufacturing.
- Solution: Energy-efficient conveyor motors, regenerative braking systems, and smart automation can help reduce power consumption.
3. Wear and tear of equipment
Continuous exposure to abrasive materials like limestone and clinker leads to significant wear and tear in bulk material handling equipment, increasing maintenance costs and downtime.
- Solution: The use of wear-resistant liners, ceramic-coated conveyor belts, and automated lubrication systems extends equipment life and reduces maintenance downtime.
4. Logistics and transportation bottlenecks
Moving bulk materials from cement plants to distribution centers requires an efficient logistics network. Rail and road congestion, inadequate infrastructure, and high transportation costs often result in delays and increased operational expenses.
- Solution: Integrated bulk terminals and automated dispatch systems improve supply chain efficiency. The Indian government’s push for multi-modal logistics parks (MMLPs) is expected to enhance cement transportation efficiency.
Indrendra Singh Raghuwanshi, Sales Head – Cement Division, ATS Conveyors, says, “Ensuring that our systems handle diverse alternative fuels reliably is at the core of our engineering approach. Alternative fuels, such as biomass, MSW, RDF and industrial waste vary significantly in terms of composition, size, moisture content, and combustibility. All our systems are designed with flexibility and robustness to meet the unique challenges posed by these fuels while maintaining operational efficiency and safety. Also, before deployment to site, we conduct extensive testing for our equipment to ensure that they can reliably handle alternative fuels under a variety of conditions. This includes testing different fuel types, moisture levels, and feeding rates to identify any potential challenges. Our systems are then fine-tuned during the commissioning phase to ensure optimal performance in real-world conditions.”
The future is automation and digitalisation
The future of bulk material handling in the cement industry lies in automation, artificial intelligence (AI), and digital twin technologies. Leading cement manufacturers are investing in IoT-enabled bulk handling systems that provide real-time monitoring, predictive maintenance, and AI-based process optimisation.
1. Smart sensors and predictive maintenance
AI-powered sensors are now being integrated into conveyors and stackers to detect early signs of wear and tear, enabling proactive maintenance and reducing unplanned downtime.
Nishith Kundar, Co-Managing Partner, Cemtech Engineering Solutions, says, “One of our latest advancements is the introduction of drone inspection technology. Since silos are confined spaces, it is often difficult to assess their internal condition, particularly at the top. We have incorporated drone inspections for both pre-cleaning and post-cleaning assessments. Pre-cleaning drone inspections help us analyse the extent of material buildup, while post-cleaning inspections ensure that the silo has been thoroughly cleaned. This technology is also applicable to pre-heaters, allowing us to monitor internal conditions in confined spaces. By leveraging drone technology, we provide precise and efficient cleaning services, improving safety and operational efficiency.”
2. Digital twin technology
Digital twin models create a virtual replica of bulk handling systems, allowing operators to simulate various scenarios and optimise material flow before implementing changes in real time.
3. Automated Guided Vehicles (AGVs) and robotics
The adoption of AGVs and robotic material handling systems is gaining traction in cement plants for automated raw material transport, warehouse management, and truck loading/unloading.
Gaurav Gautam, Business Unit Head,
Beumer Group, says, “A major recent focus has been integrating digital monitoring tools into our equipment. These tools include condition monitoring sensors that track temperature variations, vibrations and operational anomalies in real-time. By capturing this data, plant operators can take proactive actions when conditions start deviating from normal parameters. This approach prevents sudden breakdowns and, in the long term, enhances the durability and reliability of the equipment.”
“Moving forward, digitalisation will play a key role in tackling wear and tear challenges. By increasing the number of data capture points and applying advanced analytics tools, we can gain deeper insights into equipment health and performance, ensuring a more efficient and predictive maintenance strategy,” he adds.
Conclusion
Efficient bulk material handling is the backbone of cement manufacturing, ensuring a seamless flow of raw materials and finished products while minimising environmental impact and operational costs. As India’s cement industry moves towards higher production capacities and stricter environmental norms, investing in advanced, automated and energy-efficient bulk handling solutions will be key to maintaining competitiveness.
By embracing smart technologies, automation and sustainable handling practices, cement manufacturers can enhance productivity, reduce material losses, and contribute to a greener and more efficient future for the industry.















 Concrete3 weeks ago

 Concrete3 weeks ago
 Concrete4 weeks ago
 Concrete3 weeks ago