From automation to dust control, cutting-edge material handling systems are revolutionising cement production. ICR delves into how innovation is enhancing efficiency, safety, and sustainability in the cement industry.
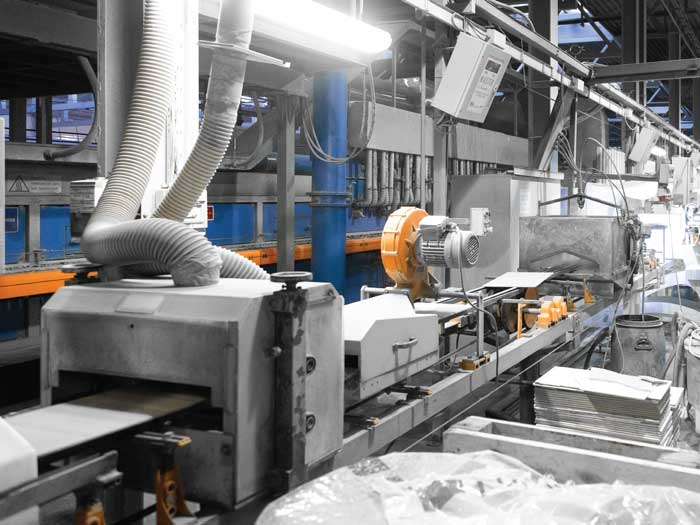
Material handling systems play a crucial role in the cement industry, ensuring the efficient and safe movement of raw materials and finished products throughout the production process. These systems encompass various equipment and technologies designed to transport, store, and manage materials, including limestone, clay, gypsum and clinker.
The importance of effective material handling in cement production cannot be overstated. First, it significantly impacts operational efficiency by minimising downtime and optimising workflows. A well-designed material handling system reduces the likelihood of blockages and equipment failures, which can lead to costly interruptions. For instance, automated systems can enhance the speed and precision of material transfers, allowing for smoother operations and faster production cycles.
Moreover, effective material handling contributes to safety in the workplace. By automating tasks that involve heavy lifting or handling hazardous materials, the risk of accidents and injuries is considerably lowered. Implementing advanced technologies such as conveyors, air cannons, and dust control systems not only enhances safety but also supports environmental compliance by minimising dust emissions and waste generation.
Furthermore, material handling systems facilitate better inventory management and resource utilisation. By accurately controlling the flow of materials, plants can maintain optimal stock levels, reducing excess inventory and the associated carrying costs. This leads to improved profitability and sustainability as resources are utilised more efficiently.
Material handling systems are integral to the cement production process, driving efficiency, safety, and sustainability. As the industry continues to evolve, investing in innovative material handling technologies will be essential for cement manufacturers seeking to enhance their competitive edge and meet growing market demands.
Dust and emissions control methods
In the cement industry, managing dust and emissions during material transfer is critical for complying with environmental regulations and ensuring a sustainable operational framework. Excessive dust not only poses health risks to workers but also contributes to environmental degradation. Therefore, cement manufacturers are increasingly adopting effective dust control methods and emission reduction technologies throughout the material handling process.
- Enclosed conveyors: Utilising enclosed or covered conveyor systems significantly reduces dust emissions during the transport of raw materials. These systems minimise the exposure of materials to ambient air, effectively containing dust and preventing it from dispersing into the atmosphere.
- Dust suppression systems: Implementing dust suppression systems, such as water sprays or misting systems, helps to control airborne particulates during material transfer. By applying water to the material surface, these systems reduce the amount of dust generated during loading and unloading operations.
- Baghouse filters: For processes that generate fine dust, baghouse filters are an effective solution. These air pollution control devices capture particulate matter from exhaust gases, ensuring that emissions meet regulatory standards. By using fabric filters to trap dust particles, baghouses significantly improve air quality.
- Air cannons and vibrators: Air cannons, such as Martin® Typhoon Air Cannons, can be employed to dislodge material buildup in transfer points. This technology helps to minimise the need for manual cleaning, reducing the likelihood of dust generation during material handling.
- Sealed transfer points: Sealing transfer points where materials are loaded and unloaded prevents dust from escaping into the environment. Implementing hoppers and chutes with proper sealing mechanisms ensures that dust remains contained during material transfer.
- Real-time monitoring: Installing continuous emissions monitoring systems (CEMS) provides real-time data on dust and emission levels. This allows operators to promptly address any issues and adjust processes as needed to comply with environmental regulations.
- Employee training: Educating employees on best practices for material handling and dust control is vital. Proper training ensures that staff understand the importance of minimising dust emissions and can implement appropriate measures effectively.
By incorporating these methods into their operations, cement manufacturers can significantly reduce dust and emissions during material transfer, ensuring compliance with environmental regulations while promoting a healthier workplace and contributing to sustainable practices. As regulations continue to evolve, ongoing investment in innovative dust control technologies will be essential for the cement industry to meet both environmental and operational goals.
Innovations in material handling
In the cement industry, efficient material handling is crucial for smooth production and operational excellence. Over the years, innovations in equipment like air cannons, conveyors, feeders, and advanced chute designs have significantly enhanced the performance and reliability of material transfer systems, improved productivity and reduced downtime.
Marco Campanari, CEO, CICSA Group, says, “Our R&D department is always active, continuously driving innovation throughout the year. Specifically, we have developed advanced techniques to refine our welding technology, focusing on the butt-flash welding technology with more effective process control. Additionally, we have perfected sophisticated heat treatments, particularly in advanced case hardening processes. These innovations significantly increase the durability and extend the lifespan of our chains.”
Air cannons: Air cannons, such as the Martin® Typhoon Air Cannons, have revolutionised material flow management by preventing blockages and material build-ups in storage vessels, silos, and chutes. These devices release powerful bursts of compressed air to clear obstructions, reducing the need for manual interventions like poking or hammering. This not only enhances material flow but also improves worker safety and plant efficiency by minimising downtime.
Conveyors: Modern conveyors have become more advanced, with enclosed or covered designs that minimise dust emissions and improve material containment. Belt and screw conveyors are now equipped with energy-efficient motors and are designed to handle larger capacities while maintaining smooth material transfer, reducing spillage and wear. Enclosed conveyors, such as pipe conveyors, are particularly effective in reducing environmental impact by containing dust during transportation.
Feeders: Innovations in feeding systems, such as gravimetric and volumetric feeders, ensure precise and consistent material flow. These feeders are crucial for dosing raw materials into the production process, allowing for better control over material proportions, which directly impacts the quality of the final product. Advanced feeders are now equipped with automation and monitoring capabilities to maintain optimal flow rates, reduce wastage, and ensure uninterrupted production.
Advanced chute designs: Chute blockages have long been a challenge in cement plants, often leading to production stoppages and increased maintenance costs. Modern chute designs incorporate features such as wear-resistant liners, curved profiles and optimally angled surfaces to prevent material sticking and reduce wear. These advanced designs also help in controlling dust and minimising material spillage during transfer, improving the overall efficiency of the material handling process.
“Another key trend fuelling growth in the CE industry is the rising demand for technologically advanced and high-performance machinery. For instance, earth-moving equipment, such as backhoe loaders, are robust machines specifically designed for heavy-duty construction tasks. The latest generation of these machines boasts superior designs, enhanced engine technologies, and innovative features. They are equipped with smart connectivity options, including modern digital instrument clusters and advanced onboard diagnostics,” says, Saroj Chouhan, Fortune Business Insights.
Together, these innovations in material handling equipment have transformed cement plant operations, improving reliability, reducing operational costs, and ensuring compliance with environmental standards. By leveraging technologies like air cannons, efficient conveyors, precision feeders, and optimised chutes, cement manufacturers can achieve higher levels of productivity while minimising downtime and enhancing sustainability.
Role of automation and Industry 4.0
The integration of automation and Industry 4.0 technologies is transforming material handling systems in cement plants, making them more efficient, reliable, and sustainable. Advanced automation systems enable real-time monitoring, precise control and optimisation of material transfer processes, reducing human intervention and minimising operational disruptions.
Automation allows for the seamless operation of conveyors, feeders and crushers, enhancing the precision of material flow while reducing energy consumption and wear. Automated systems can also monitor equipment health, predict maintenance needs, and improve decision-making through data analytics, ensuring uninterrupted material handling.
Industry 4.0 technologies such as IoT sensors, cloud computing and AI-driven analytics provide deep insights into material handling systems. Real-time data on material flow, equipment performance, and energy usage allows plant operators to optimise the entire production chain, minimising bottlenecks and maximising efficiency. Predictive maintenance powered by Industry 4.0 reduces unexpected downtimes by alerting operators to potential issues before they lead to costly stoppages.
Together, automation and Industry 4.0 are revolutionising material handling in cement plants, driving operational efficiency, reducing costs, and improving sustainability through smarter and more data-driven processes.
Energy saving in material handling
Energy-saving solutions are becoming critical in cement plants to improve operational efficiency and reduce costs. One of the most effective methods is the use of energy-efficient motors, which consume less power while delivering the same output as traditional motors. These motors reduce energy losses and have a longer operational life, contributing to both cost savings and sustainability goals. Additionally, variable frequency drives (VFDs) offer significant energy savings by adjusting the speed of motors based on the demand of the material handling process, eliminating unnecessary power consumption during low-demand periods.
Optimising equipment layouts is another crucial strategy to enhance energy efficiency. By streamlining material transfer routes, reducing unnecessary material handling steps, and ensuring shorter conveyor lengths, plants can minimise the energy required for material transport. Well-designed layouts, in conjunction with efficient motors and VFDs, help create a more energy-conscious operation that reduces power usage, lowers operational costs, and contributes to a plant’s environmental objectives.
Challenges in material handling
Material handling in cement plants presents several key challenges that impact both operational efficiency and overall productivity. One major challenge is dealing with abrasive and bulk materials such as limestone, clinker, and raw meal, which can cause significant wear and tear on equipment. This leads to frequent maintenance requirements, unexpected downtimes, and increased operational costs. Additionally, handling these materials efficiently without causing blockages or disruptions during transfer is critical, yet often difficult, due to
the complexity of conveying systems and the heavy loads involved.
Another significant challenge is controlling dust and emissions during material transfer, particularly in light of increasingly stringent environmental regulations. Dust generation not only creates health and safety risks for workers but also contributes to environmental pollution. Effective dust control systems, such as dust suppression technologies and enclosed conveyors, are essential, but implementing these solutions while maintaining high material transfer efficiency can be complex. Balancing operational demands with regulatory compliance and sustainability goals remains a constant challenge for the cement industry.
Future trends in material handling
Emerging technologies are set to revolutionise material handling in the cement industry, offering the potential to enhance efficiency, reduce costs, and improve sustainability. Automation and Industry 4.0 technologies are leading this transformation, enabling real-time monitoring and predictive maintenance through sensors and data analytics. With the integration of Internet of Things (IoT) and AI-driven systems, cement plants can optimise equipment performance, detect issues before they cause downtime, and streamline material flow, all while reducing human intervention and error. These advancements not only increase productivity but also help in energy conservation by ensuring equipment operates at optimal efficiency.
Robotics and advanced material handling equipment like autonomous conveyors, drones for inventory management, and smart feeders are also gaining traction. These technologies reduce the physical burden on workers, minimise the risk of injury, and ensure continuous operations with minimal disruption. Additionally, innovations in sustainable technologies, such as energy-efficient motors, smart grid integration, and eco-friendly materials, further support the industry’s move towards greener operations. Together, these emerging technologies promise to transform material handling systems, making them more reliable, sustainable, and cost-effective in the future.
Conclusion
Material handling plays a pivotal role in the efficiency and sustainability of cement production. As the industry faces growing challenges such as dust control, energy consumption, and environmental regulations, the need for innovative solutions has become more critical than ever. Advanced technologies like air cannons, optimised conveyors and energy-saving equipment have already begun transforming cement plants, addressing these key challenges while improving overall operational efficiency. By integrating automated systems and Industry 4.0 capabilities, cement manufacturers can enhance material handling processes, reduce downtime, and achieve better environmental outcomes.
Looking ahead, the adoption of emerging technologies, including robotics, AI-driven systems and sustainable material handling innovations, will continue to drive the evolution of cement plants. These advancements hold the potential to significantly improve material flow, reduce operational costs and contribute to the industry’s ongoing efforts toward a greener and more efficient future. As cement plants embrace these innovations, they are well-positioned to meet the demands of modern production while maintaining a strong focus on sustainability and operational excellence.
– Kanika Mathur

















 Concrete1 month ago

 Concrete4 weeks ago
 Concrete1 month ago

 Concrete3 weeks ago