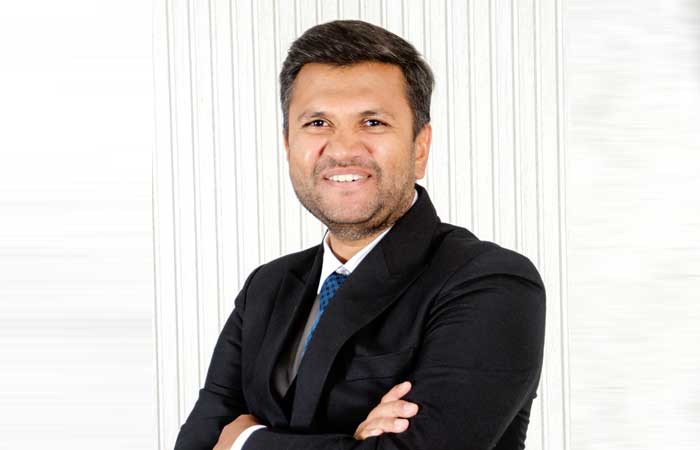
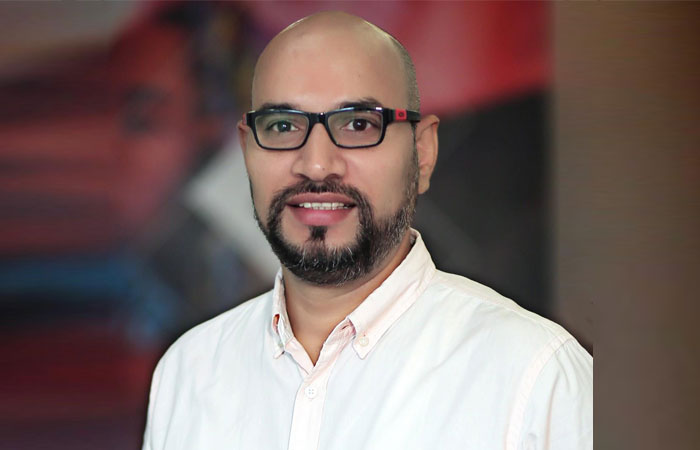
Monil Parikh, Managing Director, Techflow Enterprises Pvt Ltd, leads us to a better understanding of how cutting-edge designs and advanced technologies are revolutionising the process of filtration, driving efficiency and environmental responsibility within the cement sector.
Tell us about your air pollution control systems.
Techflow Enterprises, operating from our expansive 30,000 sq m facility, which is one of India’s largest, manufactures a comprehensive suite of air pollution control systems specifically designed for cement plants. Our solutions include:
Pulse Jet Bag Filters: Employing compressed air for efficient cleaning, these capture fine dust particles generated during grinding and packing. Techflow’s bag filters are designed to restrict the outlet emission up to 5mg/Nm3.
Electrostatic Precipitators (ESPs): Ideal for ultra-fine particulate matter in kiln exhaust gases, ESPs utilise an electric field for superior dust capture with 99.9 per cent capacity.
Centrifugal Fans: We offer various fans like induced draft (ID) fans for draft creation, process fans for dust-laden air transport, and kiln fans for high-temperature gas streams.
Techflow’s commitment to quality is evident in our proven track record. We are actively supplying solutions to leading cement players like Adani Cements, Ambuja and ACC Cement, Dalmia Bharat Cement and Wonder Cement. Our installations across India and Asia stand as a testament to our expertise in handling cement plant dust control challenges.
How do your products and systems integrate with cement plants?
Techflow’s air pollution control systems seamlessly integrate into your existing cement plant. Our pulse jet bag filters fit effortlessly downstream of grinding mills and packing stations, effectively capturing fine dust particles generated during these processes. Electrostatic Precipitators (ESPs) excel in kiln exit gas streams, working alongside existing cyclones to achieve ultra-fine particulate control, a critical step in maintaining clean air emissions.
Techflow’s comprehensive offering of centrifugal fans ensures a perfect fit for any application. Our ID fans seamlessly integrate into the kiln system, creating the necessary draft to pull exhaust gases through the air pollution control equipment. Process fans, strategically placed throughout the plant, efficiently convey dust-laden air from various generation points, like clinker coolers and raw material handling, towards the filtration units. This modular approach minimises disruption during installation and ensures optimal dust collection across your entire cement production process.
How do your innovative designs better the process of filtration at cement plants bringing efficiency to the process?
Techflow’s commitment to innovation translates to superior filtration efficiency and operational cost savings for cement plants. Our pulse jet bag filters incorporate features like:
- High-efficiency filter media: Designed for specific dust types, this media minimises pressure drop across the filter, reducing energy consumption.
- Improved flue gas entry design
- Low Pressure Cleaning Systems
- Optimised pulse cleaning systems: These systems efficiently dislodge dust cake buildup using compressed air, maximising filter media life, and minimising downtime.
Our ESPs utilise advanced electrode designs to enhance particle collection and reduce maintenance intervals. Furthermore, Techflow’s centrifugal fans are meticulously crafted for superior aerodynamic performance, leading to lower energy consumption and improved overall plant efficiency.
Techflow has developed a SMART-LINK automation module for better maintenance and real-time remote tracking of performance of each equipment. Cement plants equipped with Techflow’s systems experience reduced operational costs, minimised downtime and compliance with ever-evolving environmental regulations.
What is the key differentiator between traditional filters and modern filters?
Traditional bag filter systems often relied on manual cleaning methods, leading to inconsistent performance, increased downtime, and potential worker exposure to dust. Modern pulse jet bag filters, like those offered by Techflow, address these limitations.
Our systems leverage automated cleaning mechanisms, ensuring consistent filtration efficiency and minimal operator intervention. Additionally, advanced filter media materials in Techflow’s bag filters offer superior dust capture capabilities compared to traditional fabric filters.
This commitment to modern technology translates to a safer and more efficient and environmentally friendly dust control solution for cement plants.
Can your designs be customised as per the requirement of the customers?
At Techflow, we understand that every cement plant has unique dust control requirements. That is why we prioritise customisation across our entire product range:
Pulse Jet Bag Filters: Filter media type and micron rating based on dust properties, number of filter bags, and pulse cleaning system configuration like cycle time and pressure can all be adjusted to optimise performance for your specific dust and airflow. The system can be designed to achieve less than 5mg/Nm3 outlet emission standards as well.
- Electrostatic Precipitators (ESP): ESP design can be customised with features like the number of electrode rows, electrode spacing, and power input like voltage and current to achieve the desired dust collection efficiency for your specific outlet emission capacity less than 20mg/Nm3.
- Centrifugal Fans: Fan designs are tailored by adjusting factors like impeller diameter, blade design, and motor size to meet the specific pressure and flow requirements of various processes within a cement plant.
This focus on customisation ensures Techflow’s air pollution control systems perfectly match your cement plant’s needs, guaranteeing optimal dust capture and efficient operation.
What is the role of technology and automation in building filtration systems?
Techflow has designed a SMART-LINK System that can be integrated to our equipment which tracks and monitors performance of equipment in real time.
- Continuous diagnostics
- Condition-based maintenance
- Prevention of unplanned downtime
- Early problem detection using AI
- Data collection for process optimisation and efficiency maximisation
- Auto alert with warning driving timely human interactions
- Remote maintenance assistance by Techflow Team.
What are the major challenges in the filtration process and your system integration at cement plants?
The cement industry’s focus on sustainability, higher production and diverse fuel sources creates filtration hurdles. Adapting to changing dust properties, handling increased dust loads, and integrating seamlessly within space constraints are key challenges.
Techflow tackles these issues through advanced design techniques, exploration of innovative filter media, and modular system design. This ensures our filtration systems remain adaptable, efficient and seamlessly integrated within your cement plant, empowering your success.
How do you plan to further better your products and bring innovation in the future?
At Techflow, we are not just building filtration systems, we are shaping the future of clean air in the Indian cement industry. After successful expansion of the manufacturing facility in 2023, now it is time to improve designs and process optimisation. The future holds exciting possibilities: next-generation filter media with self-cleaning properties and
extended lifespans, minimising maintenance and maximising efficiency.
Techflow’s legendary after-sales support is about to get even better. We are expanding our global service network to provide you with 24/7 access to a team of India’s most experienced filtration specialists, ensuring your system operates flawlessly throughout its lifecycle.
Together, we will lead the way towards a sustainable future, paving the path for a greener tomorrow with green cement.















 Concrete4 weeks ago

 Concrete3 weeks ago

 Concrete4 weeks ago
 Concrete3 weeks ago