Connect with us

Economy & Market

Corrosion Busters

Published

on

Shares

Concrete structures deteriorate primarily due to corrosion of steel, which can be controlled by applying different kinds of coatings, like Fusion Bonded Epoxy.
Whenever you see a construction site of a bridge or a Metro rail, you will normally notice a green colouring in the steel used in these structures. This colouring indicates that the steel has been made resistant to corrosion by using a technique called Fusion Bonded Epoxy (EBE).

Weathering of concrete is a usual process. But if the surroundings are aggressive, the concrete undergoes degradation. The decay first attacks the steel inside the concrete, and then initiates the process of corrosion of rebars. Therefore, steel is coated with a protective layer to ward off corrosion. Presently, all infrastructure projects – bridges, viaducts, Metro tracks – use steel which has to be corrosion resistant.

There are many methods of protecting steel, but FBE coating has been the most popular one. FBE coating principally protects against corrosion by serving as an electrochemical and a physical barrier that isolates the steel from the oxygen, moisture and chloride ions that cause corrosion. Epoxy coating has high electrical resistance, which blocks the flow of electrons that make up the electrochemical process of corrosion. In addition to serving as a circuit breaker, the coating reduces the size and number of potential cathodic sites, which limits the rate of corrosion reaction that could occur.

As a matter of fact, for macrocell corrosion to take place, a large area of the steel surface is needed to serve as the cathode where oxygen reduction can occur. The coating almost eliminates such cathodic reaction.

History
Since their introduction as a protective coating in the early 1960s, FBE coating formulations have gone through vast improvements and developments. Today, various types of FBE coatings, which are tailor made to meet various requirements, are available. FBEs are available as standalone coatings as well as a part in multi-layers. FBE coatings with different properties are available to suit coating application on the main body of pipes, internal surfaces, girth welds as well as on fittings.

Chemistry of FBE coatings
Essential components of a powder coating are resin, hardener or curing agent, fillers, extenders and colour pigments.
The resin and hardener are together known as the binder. As the name indicates, in FBE coatings, the resin part is an epoxy type resin. The epoxy or oxirane structure contains a three-membered cyclic ring – one oxygen atom connected to two carbon atoms -in the resin molecule. This part is the most reactive group in the epoxy resins. Most commonly used FBE resins are derivatives of Bisphenol A and epichlorohydrin. However, other types of resins (for example Bisphenol F type) are also commonly used in FBE formulations to achieve various properties, combinations or additions. Resins are also available in various molecular lengths, to provide unique properties to the final coating.

The second most important part of FBE coatings is the curing agent or hardener. Curing agents react either with the epoxy ring or with the hydroxyl groups, along the epoxy molecular chain. Various types of curing agents used in FBE manufacture include dicyandiamide, aromatic amines, aliphatic diamines, etc. The selected curing agent determines the nature of the final FBE product – its cross-linking density, chemical resistance, brittleness, flexibility, etc. The ratio of epoxy resins and curing agents in a formulation is determined by their relative equivalent weights.

In addition to these two major components, FBE coatings include fillers, pigments, extenders and various additives, to provide desired properties. These components control characteristics such as permeability, hardness, colour, thickness, gouge resistance, etc. All of these components are normally dry solids, even though small quantities of liquid additives may be used in some FBE formulations. If used, these liquid components are sprayed into the formulation mix during pre-blending in the manufacturing process.

Surface preparation: Blast cleaning
Blast cleaning is the most commonly used method for preparation of steel surfaces. This effectively removes rust, scale, slats, etc., from the surface and produces an industrial grade cleaning and a rough surface finish. The roughness of the steel achieved after blasting is referred to as profile, which is measured in micrometers or mils. Commonly used profile ranges for FBE coatings are 37 to 100 micrometers (1.5 to 4 mils).

It is important to remove grease or oil contamination prior to blast cleaning. Solvent cleaning, burn-off, etc., are commonly used for this purpose. In the blast cleaning process, compressed air (90 to 110 psi/610 to 760 kPa) is used to force an abrasive onto the surface to be cleaned. Aluminum oxide, steel grit, steel shot, garnet, coal slag, etc., are the frequently used abrasives.

Another method of blast cleaning is centrifugal blast cleaning, which is especially used in cleaning the exterior of pipes. In this method, the abrasive is thrown to the rotating pipe body, using a specially designed wheel, which is rotated at high speed, while the abrasive is fed from the centre of the wheel.

Heating and FBE powder application Heating of the object can be achieved by using several methods, but the most commonly used ones are induction heating or oven heating. The steel part is passed through a high frequency alternating current magnetic field, which heats the metal part to the required FBE coating application temperature. Typical application temperature for a standalone FBE is 225?C to 245?C. When used as a primer in a multi-layer polyolifine system, application temperature may be dropped based on the FBE manufacturer?s recommendations, in order to meet the ?inter-coat adhesion? parameters. Special grade FBE coatings which can be applied at temperatures as low as 175?C have been developed recently by certain FBE powder manufacturers.

Other methods of heating are oven heating, infrared heating, etc. The FBE powder is placed on a fluidisation bed. In a fluidisation bed, the powder particles are suspended in a stream of air, in which the powder will ?behave? like a fluid. Once the air supply is turned off, the powder will remain in its original form. The fluidised powder is sprayed on to the hot substrate using suitable spray guns. An electrostatic spray gun incorporates an ionizer electrode on it, which gives the powder particles a positive electric charge. The steel to be coated is?grounded? through the conveyor. The charged powder particles uniformly wrap around the substrate, and melt into a liquid form. Internal surfaces of pipes are coated using spraying lances, which travel from one end to the other end of the heated pipe at a uniform speed, while the pipe is being rotated in its longitudinal axis.

Standard coating thickness
range of standalone FBE coatings is between 250 and 500 micrometers, even though lower or higher thickness ranges might be specified, depending on service conditions. The molten powder flows into the profile and bonds with the steel. The molten powder will become a solid coating, when the gel time is over, which usually occurs within a few seconds after coating application. The resin part of the coating will undergo cross-linking, which is known as ?curing? under hot conditions.

Complete curing is achieved either by the residual heat on the steel, or by the help of additional heating sources. Depending on the FBE coating system, full cure can be achieved in less than one minute to a few minutes in case of long cure FBEs, which are used for internal pipe coating applications.

Rebars are coated in a similar manner as coating applications, on the exterior of pipes. For FBE coating application on the interior of a pipe surface, a lance is used. The lance enters the preheated pipe, and starts spraying the powder from the opposite end, while the pipe is being rotated on its axis and the lance pulls out in a predetermined speed.

On fittings such as Tees, elbows, bends, etc., powder can be sprayed using handheld spray guns.

Disadvantages
Since the process of coating is quite elaborate and cannot be carried out at a construction site, additional cost is incurred on logistics to send the material and get it back from the factory.

While bending the steel, the coating breaks at sharp bends, making these locations prone to corrosion.


Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Economy & Market

Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition

Published

on

By

Shares

 Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.

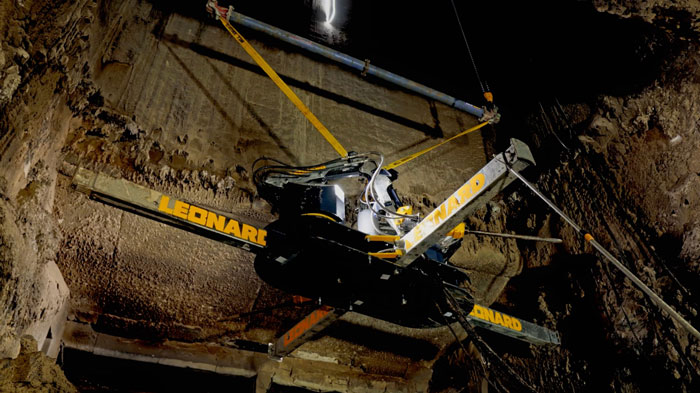
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.

Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.

Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.

Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.

According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.

First Deployment Demonstrates Shutdown Efficiency

The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.

Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.

Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”

Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.

The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.

“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.

“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”

Expanding Industrial Robotics Applications

Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.

Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.

Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.

The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.

Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

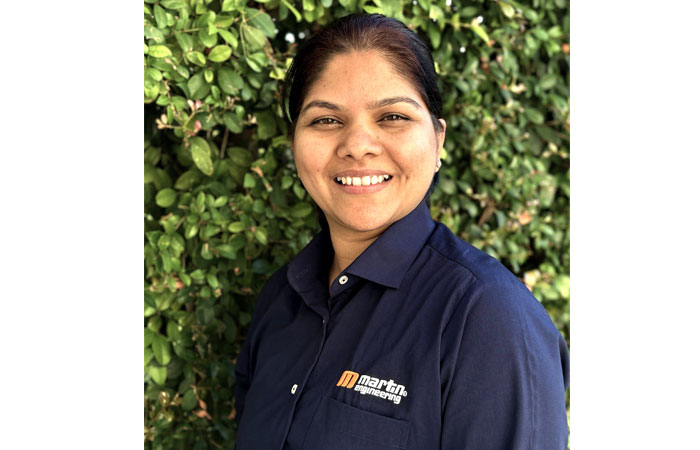
Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

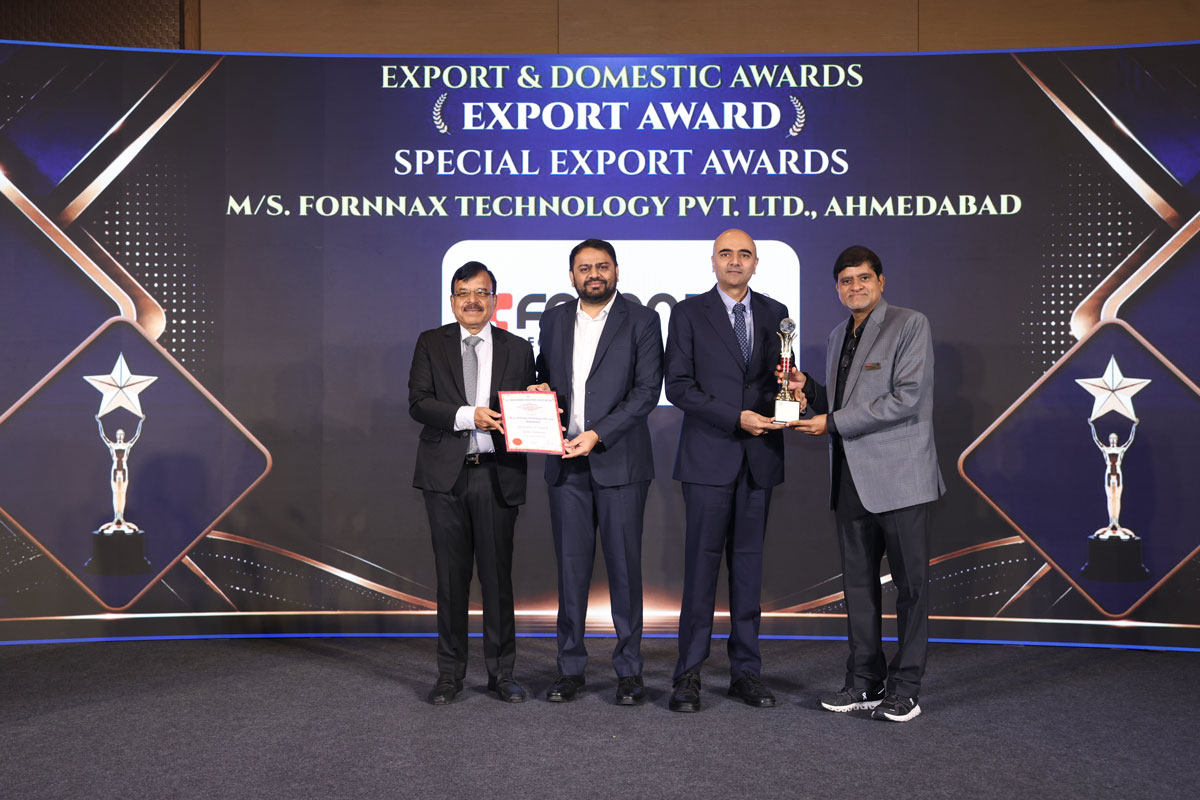
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds