Connect with us

Economy & Market

Pinions Instead of Belts – The Logical Choice!

Published

on

Shares

The direct drives of NORD drivesystems brought more than just higher reliability and reduced financial and labour expenditure for maintenance activities. The relative investment costs for purchasing new gear units also proved to be lower.Gravel plant cuts costs and reduces maintenance expenditures by using geared motors. In many gravel pits, stone crushing plants and similar operations, motive power for conveyor belts is provided by shaft and belt drives. Until recently, this was the situation at the gravel plant of NorStone AS in Tau, located in the southwest region of Norway. Recently NorStone, a subsidiary of HeidelbergCement AG, decided to change to robust geared motors. This option promised lower investment costs and increased operational reliability, along with better process security. Reduced energy consumption thanks to higher efficiency was also anticipated.NorStone is Norway’s largest producer of gravel products. The company supplies aggregates for concrete and asphalt, pipe cover gravel for coastal regions, and other special products. Each year NorStone’s production facilities produce over 6.6 million tonnes of gravel products in various sorts and quality classes. The demand is large, and even with its present annual production capacity of 2.3 million tonnes of material the Tau plant can scarcely meet the demand. This makes it especially important to ensure that the plant is operational as much as possible and to minimise unplanned downtime.Familiar advantages plus increased reliability with direct drivesGeared motors are actually not new in gravel pits. Direct drives of this sort were commonly used in the 1980s, but in subsequent years many plants changed to belt drives because spare parts for these drives were always quickly available, while manufacturers and suppliers of geared motors were unable to offer stocks of spare parts with the same good availability. "We have found that service and spare parts for geared motors are now available to us very quickly. We hold some parts in stock ourselves, and for all of the rest we have complete trust in NORD Drivesystems as a supplier", explained Ivar Ullestad, Maintenance Manager at Tau, as the reason for going back to the former solution. "This allows the known advantages of drive solutions with geared motors to be fully exploited. In particular, direct drive leads to higher reliability, which means less downtime and therefore less lost production time. Another important aspect is that less maintenance is necessary. In addition to reducing maintenance costs, this increases safety in the plant", added Ullestad.Measurably less wear than with shafts and beltsWorking conditions are a significant factor in such considerations. "You have to bear in mind that we work outdoors all year round. Most of the locations for the conveyor belt drives are open and unprotected. Due to the harsh weather conditions in the west of Norway, with wind, rain and sleet, as well as the dusty and rather unpleasant environment at the site, we try to minimise repair and maintenance times for our maintenance staff." The Tau plant runs seven days a week, 24 hours a day in shift operation. The 168 production hours include 16 hours of scheduled maintenance. The plant is only shut down for the winter break. During this break, annual maintenance inspection and overhaul tasks are performed in two to three weeks. The direct drives have contributed to a distinct increase in reliability, amounting to approximately 4.5 per cent, in the last three years. "We are very satisfied with this trend. With the change from shaft and belt drives to direct drive with geared motors from NORD Drivesystems, in the first place we eliminate the aspect of belt wear, which is considerable. Furthermore, no water or dust can enter the drive mechanism. This means that the decision in favour of compact, robust geared motor units yields clear advantages and has therefore proven to be an intelligent move", summarised Per Thu, Production Manager of the NorStone plant. The direct drives brought more than just higher reliability and reduced financial and labour expenditure for maintenance activities. The relative investment costs for purchasing new gear units also proved to be lower. Replacing a complete package, consisting of a shaft-type gear unit along with belt pulleys, belts, a shed, belt cover and motor, turned out to be more costly than purchasing a comparable geared motor. As a series of periodic gear unit replacements was anyhow in the works, a comprehensive switch from shaft and belt drive to direct drive was a logical choice for Ullestad. He is currently working to standardise drive components. "With a staged cutback in drive systems for the conveyor belts, we are standardising aspects such as motor size, shaft size and drum diameter in order to limit diversity and thereby simplify maintenance, stock management and service. We are also developing backup solutions, which among other things involves keeping components in stock ourselves," according to the maintenance manager.NORD Drivesystems Pvt. Ltd.282/2, 283/2, Village Mann,Tal. Mulshi, Adj. Hinjewadi MIDC IIPune 411057 IndiaSINGH SwetaPhone : 09765490890SSingh@nord-in.comGetriebebau NORD GmbH & Co. KGRudolf-Diesel-Stra?e 122941 Bargteheide/Hamburg, GermanyNIERMANN J?rgPhone : +49(0) 45 32 / 401 – 360Fax : +49(0) 45 32 / 401 – 254Joerg.Niermann@nord.com

Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Concrete

Wonder Cement appoints Mahesh Singh as VP Corporate Brand Communication 

Published

on

By

Shares

Singh brings 20+ years of brand and marketing experience, and will lead integrated corporate brand communication initiatives at Wonder Cement 

New Delhi

Wonder Cement, a leading cement manufacturer, has appointed Mahesh Singh as Vice President – Corporate Brand Communication. In his new role, he will oversee corporate brand strategy and communication, including digital and performance marketing, public relations, trade, events, exhibitions, sports and experiential marketing. 

Singh brings over two decades of experience across marketing and communications, with roles spanning the automotive industry, agencies and entrepreneurship. He spent more than a decade with Honda Motorcycle & Scooter India, working across integrated communication, media, digital, retail and consumer engagement. His stint also included helping build the company’s digital marketing capabilities. 

He moved to dentsu X India as Vice President – Strategy & Planning, working across categories such as automotive, auto components, electric vehicles, FMCG, consumer electronics, BFSI, apparel and brand consulting. His responsibilities included media and marketing strategy, product launches, content, performance marketing and consumer activations. 

Singh subsequently took an entrepreneurial route with Radiant Brands before joining Shriram Ltd (SPR Autotech) as Head – Marketing & Communications. There, his remit included brand and corporate strategy, communications, PR and ORM, retail identity, loyalty programmes and events. 

At Wonder Cement, Singh will be responsible for bringing together the company’s corporate brand communication initiatives across digital, performance marketing, PR, trade, sports and experiential platforms. The role will focus on creating an integrated approach to communication across consumers, trade partners and other key stakeholders. 

The appointment brings to Wonder Cement a marketer whose career has spanned the brand, agency and entrepreneurial sides of the communications ecosystem. 

Wonder Cement, part of the RK Group, is a cement manufacturer with roots in Rajasthan and a focus on quality, trust and transparency. The company has grown to six manufacturing plants, and a cement capacity of 21.5 MTPA. With more than 2,000 employees and a network of over 5,000 dealers, its operations span manufacturing, distribution and customer engagement, with a focus on consistent product quality and efficient execution. 

Continue Reading

Concrete

JSW Cement commissions additional 1 MTPA grinding unit at Nagaur

Published

on

By

Shares

With this commissioning, JSW Cement’s total cement grinding capacity has increased to 25.10 MTPA, 
Mumbai

JSW Cement, one of India’s leading green cement producers and part of the diversified JSW Group, today announced the successful commissioning of an additional 1.00 MTPA cement grinding unit at Nagaur, Rajasthan. The commissioning marks another significant milestone in the Company’s growth strategy.

With this commissioning, JSW Cement’s total cement grinding capacity has increased to 25.10 MTPA, while its total clinker manufacturing capacity, including clinker capacity at its joint venture, JSW Cement FZC, stands at 9.74 MTPA.

JSW Cement had commenced operations in North India in March 2026 with the Nagaur Integrated Plant, comprising a 3.30 MTPA clinkerisation unit and 2.50 MTPA cement grinding unit. With the commissioning of the additional 1.00 MTPA cement grinding unit, the plant’s total cement grinding capacity has increased to 3.50 MTPA, enhancing the company’s ability to cater to the growing cement demand across Rajasthan, Haryana, Punjab and the National Capital Region (NCR). The expansion has been funded through a strategic mix of equity and long-term debt.

During the quarter ended 30th September 2026, JSW Cement has also commissioned the Alternate Fuel Handling System and the Waste Heat Recovery system (WHRS) at the Nagaur Integrated Plant.

Nilesh Narwekar, CEO, JSW Cement, said: “The commissioning of additional 1.00 MTPA grinding capacity at Nagaur is a key strategic priority for us and will accelerate JSW Cement’s expansion into North India. We look forward to servicing the growing needs of the region and contributing to the economic growth of Rajasthan, Haryana, Punjab and the NCR area. I am delighted to share that the company has commissioned this grinding unit within the expected timeline, showcasing our project execution capabilities. Further, the Alternate Fuel Handling System and the Waste Heat Recovery system (WHRS) are expected to substantially reduce our production costs going forward.”

Continue Reading

Concrete

UltraTech becomes first Indian cement firm to cross 2 GW green energy

Published

on

By

Shares

UltraTech Cement has crossed 2 GW of captive green energy capacity, with renewables and waste heat recovery meeting 48 per cent of its power needs.

Mumbai

UltraTech Cement Limited has surpassed 2 GW of installed green energy capacity for captive use, becoming the first cement company in India to achieve the milestone. The Aditya Birla Group company commissioned 116.55 MW of wind capacity at its Inter-State Transmission System-connected wind-solar hybrid project in Barmer, Rajasthan, along with 10 MW of Waste Heat Recovery System capacity at Sarlanagar Cement Works in Karnataka.

With these additions, UltraTech’s cumulative installed green energy capacity has reached 2,024 MW. This includes 1,580 MW of renewable energy capacity and 444 MW of waste heat recovery capacity, together meeting around 48 per cent of the company’s current power requirements.

The company said the milestone reflects the progress of its long-term energy transition strategy. In FY27 so far, nearly one-third of UltraTech’s 76 manufacturing units in India have maintained green energy utilisation above 50 per cent of their electricity requirements, while five units have crossed 95 per cent.

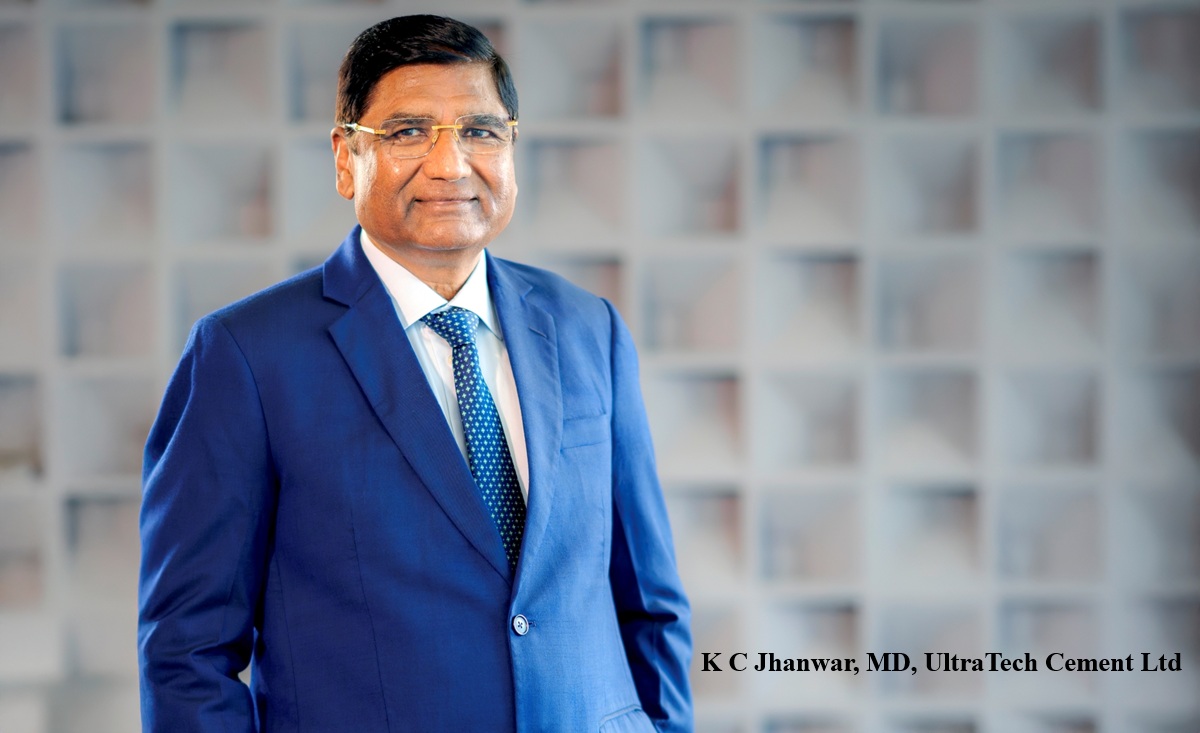
K C Jhanwar, Managing Director, UltraTech Cement Limited, said, “Crossing the 2 GW green energy milestone is the result of a strategy we have pursued consistently over the past decade. Cement is an energy-intensive, hard-to-abate sector, and showing that reliability and growth can go hand in hand with a rapid shift to green energy sets a benchmark for the industry. With nearly half of our power needs now met through green energy, we are significantly less exposed to fossil fuel supply constraints and power price volatility. As we scale up renewables, waste heat recovery and battery storage across our operations, we are building an energy foundation for stable, long-term growth.”

UltraTech commissioned 430 MW of green energy capacity in FY26 and continues to expand its renewable energy and waste heat recovery portfolio.

The company is also progressively integrating Battery Energy Storage Systems across its operations to improve renewable energy utilisation and supply reliability.

In 2025, UltraTech operationalised what it described as India’s first on-site hybrid round-the-clock renewable energy project at Sewagram Cement Works in Gujarat. The project combines solar, wind and battery storage.

As part of its decarbonisation strategy, UltraTech said it has not invested in new captive thermal power capacity for either greenfield projects or brownfield expansions at its integrated units for more than a decade.

The company said its expanding green energy portfolio is helping reduce dependence on conventional grid electricity and fossil fuel-based power, while lowering exposure to fluctuations in coal and electricity prices.

UltraTech aims to increase green energy’s share in its total power mix to 85 per cent by 2030. As a member of RE100, it has also committed to meeting 100 per cent of its electricity requirement through renewable sources by 2050.

UltraTech Cement, the cement flagship of the Aditya Birla Group, has a total grey cement capacity of 210.1 MTPA and white cement and putty capacity of 3.5 MTPA. The company is also a signatory to the GCCA Climate Ambition 2050 and has committed to the GCCA Net Zero Concrete roadmap.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds