

Concrete
Pyroprocessing and the Art of Energy Efficiency

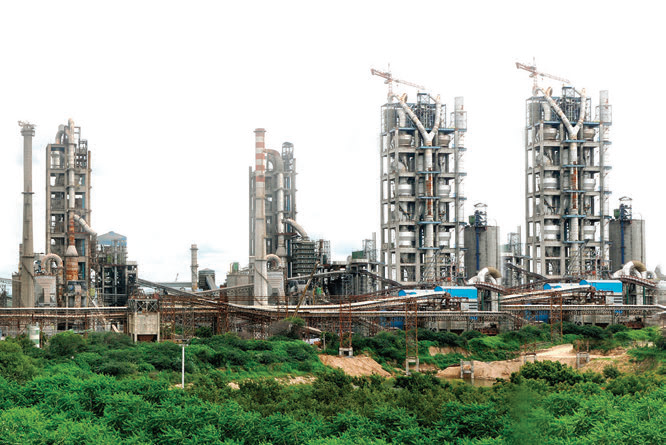
Prashant Bangur, Joint Managing Director, Shree Cement discusses the latest development in pyroprocessing along with the seamless integration of new technologies to make the process of cement production more efficient.
Prashant Bangur, Joint Managing Director, Shree Cement discusses the latest development in pyroprocessing along with the seamless integration of new technologies to make the process of cement production more efficient.
Shree Cement was in the news recently when it entered into a contract with FLSmidth. Working with the Danish multinational engineering company on a new greenfield project, Shree Cement installed a new line in Rajasthan, which is equipped with a pyroprocessing system, and aims at reducing the company’s carbon footprint while optimising energy consumption. Bangur shares his thoughts on pyroprocessing and the challenges it entails.
Which new technologies are changing the face of pyroprocessing?
In the past five to six decades, the basic nature of pyroprocessing has not changed. A little that had changed happened about twenty or thirty years ago, which was the transition from wet to semi-dry and semi-dry to dry processes. Post that, most of the processes have become more and more efficient, but haven’t changed fundamentally.
Coolers have become more efficient; the production cost has come down; the kiln system has become more competent; but has the technology changed? The answer is no. The basic nature of the pyroprocessing technology remains the same.
With innovation becoming part of this process for increased efficiency, the consumption of heat and power due to better designs and Computational Fluid Dynamics (CFD) analysis have reduced and the pressure drop has reduced significantly. Same is true for temperatures. Earlier for pre-heaters, 350o Celsius was considered to be a good temperature, but now suppliers are getting similar results at 270 or 280 degrees, which is a large improvement in heat consumption. Pressure drop also shows a dramatic reduction in its numbers.
In terms of automation, the first generation logistic systems were supplied by erstwhile companies such as Honeywell, while the latest systems are a class apart.
Give details about the processes used at Shree Cement.
There are two pyro processes that we have ordered for our two plants, at Raipur and Nawalgarh – the expansions of our organisations that are ongoing. Both these systems are ordered from FLSmidth. Both the plants are industry norms compliant and include a state-of-the-art pyro system and grinding sections. From the bouquet of technology offerings of FLSmidth, we have also picked the automation and intelligence system, which we are yet to work with. But we are hopeful that with one good experience, we will be repeating these orders for all the plants.
How has it lessened the obvious consequences of pyroprocessing?
With new technologies coming in, the heat consumption and the kiln consumption goes down in the pre-heater. The pressure drop goes down, as a result of which the power consumption also significantly reduces.
Every such efficiency parameter reduces the fuel and power consumption for clinker production, which means that carbon footprint comes down. However, these are marginal reductions in the carbon footprint with all these features. The real challenge in the cement industry is the process of calcination of limestones, which emits the maximum amount of carbon dioxide. Since that is a chemical process, there is nothing much that can be done about it.
Overall, the process of making clinker or calcination forms the core of the cement making process, which has a requirement of emitting carbon dioxide. What we can do or are doing to mitigate this situation is to use alternative materials for the processes that will reduce the carbon footprint.
What are the challenges faced by companies in making pyroprocessing more energy efficient?
I would not say that I am facing any challenges, rather we are continuously improving and so is the technology. I wouldn’t term it as a challenge, but as an ongoing improvement process.
It doesn’t happen overnight, neither does it happen in a jiffy. We try to learn new things everyday and that is when we understand processes that may work, efficient motors for the machinery, new ways to reduce power consumption, pressure drop and much more.
Reducing heat and power consumption is on everyone’s agenda. So, it is not a not a new challenge, it is an ongoing challenge and the whole industry is trying to fight and overcome it.
What kind of support are you getting from the government in making your pyroprocessing methods better?
The government is facilitating and ensuring the provision of municipal waste. They are ensuring that the producers of cement waste are required to dispose it off, efficiently and scientifically.
About a decade ago, when disposal norms were not stringent, a number of harmful chemical wastes were disposed off in the rivers, thereby polluting water sources. But, now with very strict regulations, the government is ensuring that all the waste is disposed off in a manner that doesn’t affect the environment and they also make sure that the producer of the waste has to pay.
The government ensures that harmful industrial waste is not dumped in the ground, contaminating land and underground water. Being strict about waste disposal is a big favour that the government is doing on the environment.
Which alternative source of energy can fuel the process in a similar manner?
Alternative sources in the process of cement production are a very wide range of materials available in the market, which may or may not be cheaper, but are effective for the health of the environment. Using renewable waste, plastic waste and sewage waste that comes treated from municipal plants, which are otherwise burnt and disposed by the government, can be a valuable resource in the kiln. This would be good for the company, and the environment in the larger scheme of things.
How are you minimising the impact on the environment due to CO2 and N2O emissions?
I’ll answer this question differently. Five years ago, there were no norms for CO2 and N2O emission through clinker. The new government, thankfully, has created norms, which put a limit on the carbon or sulphur that we can emit in the environment. The whole industry has to comply with these limits set by the government and monitor their emissions.
Further down the line, there are better and more efficient technologies available to reduce the carbon, sulphur and other harmful emissions in the pyroprocess or cement making process on a whole, but that comes at a higher price. However, the end consumer will have to pay for the cost that goes in reducing the impact on the environment.
This is a decision for the government to make, in balancing the affordability for the consumer and the impact on the environment.
How do all the developments in terms of new norms, rules and regulations as well as automation have an impact on your cost?
The more stringent norms we make, the more the cost will go up. As I had described, it is possible to reduce the emissions further, but at a cost. There are some technologies that are not yet mature enough to be functional on an industrial scale, but in the next few years, we can expect better technologies at a better cost that will help reduce the impact on the environment and yet are cost effective for the makers and consumers of cement.
Kanika Mathur

Concrete
India’s Core Sector Growth Eases to 4.8 Per Cent in August
Cement, electricity and iron ore offset declines in other sectors
Concrete
Jammu Division Begins First Cement Rail Traffic to Anantnag
Cement Loading From Kathua for Anantnag to Begin on September 14

Concrete
Hard Worker Wins Three Honours at Kyoorius Design Awards
Ramco Cements’ brand secures Grand Prix and two Blue Elephant honours.



India’s Core Sector Growth Eases to 4.8 Per Cent in August

Jammu Division Begins First Cement Rail Traffic to Anantnag

Hard Worker Wins Three Honours at Kyoorius Design Awards

Cement Firms to Invest Rs. 130 bn in Green Energy by FY28

Centre Defers Clearance for Limestone Mine Near Bustard Habitat
India’s Core Sector Growth Eases to 4.8 Per Cent in August
Jammu Division Begins First Cement Rail Traffic to Anantnag
Hard Worker Wins Three Honours at Kyoorius Design Awards
Cement Firms to Invest Rs. 130 bn in Green Energy by FY28
Centre Defers Clearance for Limestone Mine Near Bustard Habitat
-

 Concrete4 weeks ago
Predictive maintenance minimises the risk
-

 Concrete4 weeks ago
AI is solving longstanding challenges
-

 Concrete4 weeks ago
Fuller Technologies QCX® Lab Automation Systems
-

 Concrete4 weeks ago
Beyond the Gearbox: How a Holistic Lubrication Strategy Reduces Total Cost of Ownership in Cement Plants