Economy & Market
Revival of small scale cement manufacturing
Published
8 years agoon
By
admin
The availability of most of the AFR is limited or scattered which may not be economically viable for use in most of the large cement plants because of logistics, quantity, preparation and technical issues, says Dr KN Bhattacharjee.
The availability of most of the AFR is limited or scattered, which may not be economically viable for use in most of the large cement plants because of logistics, quantity, preparation and technical issues. This is a great roadblock for the effective use of AFR. However if an industry can find means to utilise its own by-product or waste in its own premises or nearby then it will be a win- win situation for all. Cement manufacturing process is a very appropriate process to recycle many industrial and agricultural wastes. The black meal process of vertical shaft kiln technology is a proven technology in China and India and can serve as a very good outlet for consuming AFR in the vicinity of industries generating the waste in small quantities.
This will also help in reducing environmental pollution. The author has carried out numerous plant scale trials with various industrial and agricultural wastes in VSK plants in India with reasonable success and feels that it may be worthwhile to go backward technology-wise to improve India’s usage of AFR. With the recognition of performance-based cements in most of the standards of world, composite cements are to gain ground and many alternate materials mainly industrial wastes can find profitable use again in small-sized cement plants.
The vertical shaft kiln (VSK) technology is an old technology of Portland Cement manufacture and even the modern versions have almost phased out from India mainly because of economics of scale and taxation issues. In China, still 30 per cent of its cement production comes from shaft kiln plants. The VSK process technology is still a workable proposition for use of wastes available in limited quantities. Also by virtue of the simple process a plethora of process issues associated with modern pre-heater, pre-calciner rotary kiln system are eradicated while using AFR. Plant scale trials with many wastes have shown improvement in VSK clinker quality and better productivity from the kilns. Also it is possible to add many wastes in small quantities directly to VSK clinker to produce high performing composite cements. Although the plan sounds to be reverse engineering but sometimes an old concept can regain its past glory due to changing national needs and environmental issues.
The modern vertical shaft kiln technology is technically sound and institutes like National Council of Cement and Building Materials (NCCBM) and the then Regional Research Laboratory (RRL), Jorhat had done a commendable work in modernising the technology in India. Also the village-based Saboo technology created a stir in India in the 80s when they brought cement manufacturing under the umbrella of small scale industry. During that period, the objective was to increase production as India was cement deficit and VSK technology was a partial answer to quickly bridge the gap between demand and supply. In the hilly terrain of North East, it is still a viable proposition to use scattered small limestone deposits in the midst of logistical challenges.
The advantages and disadvantages of black meal process of vertical shaft kiln technology:
Advantages:
- Small scale cement production and still suitable in hilly terrains having limestone deposits for local distribution of cement.
- Energy efficient process: Specific heat consumption is in the range 600 to 650 Kcal/kg of clinker. Specific power consumption is in the range 0f 60 to 70 Kwh/tonne OPC although authentic figures are not available. Since drying, pre-heating, calcining, burning and cooling are integrated in the same vessel, heat losses due to convection and radiation is much reduced.
- Porous VSK clinker is much easier to grind thus cement grinding power requirement is less.
- Very low refractory consumption as kiln is stationery and low abrasion as material flow is vertically downward with slow speed.
- Vast scope of using AFR available in smaller quantities is the major advantage. Some alternate waste materials can act as flux or mineraliser. Mineralising ions can increase the rate of reaction in burning zone leading to complete burning in burning zone.
- Thus the technology offers avenue not only in the use of wastes but also utilise the waste in improving burnability by stabilising phases at lower temperatures.
- recirculation of obnoxious gases and materials which ensures smooth operation and higher productivity.
- Due a constant bed of wet green nodules above the calcining zone the green nodules bed acts as an effective filter to arrest all dust particles. No additional gas cleaning device is required.
- Since fuel is inter-ground with raw materials elaborate arrangement of fuel preparation and firing is eliminated
- Very effective and controlled flow of material through flat grate using variable frequency drive (VFD). This helps to position the burning zone constantly at the same level.
- Relatively simple machines to operate and maintain.
- Gestation period of starting a new plant is very low.
- No highly skilled manpower is required and local folk/plant staff can be easily trained for operations.
- Possible to manufacture a variety of clinkers and thereafter produce various kinds of low cost Portland cements.
- Very little chance of cold air in-leakages. Diversion of combustion air during clinker discharge has been ably dealt by either triple air locking arrangement or material block tube in the modern VSKs.
- Since each nodule has its independent fuel system significantly higher temperatures are not achieved leading to no issues of NOx.
Disadvantages:
- Viability can be at stake due to taxation policies and lower scale of operation. However if Government gives tax rebates on use of AFR the plants can be viable. Also it is possible to reduce cost of production by using low cost or free of cost non- conventional materials and waste fuels available locally. Maybe the savings can be shared with customers.
- Quality issues: Many believe that VSK clinker cannot be at par with modern rotary plant clinker. In this respect a few conflicting issues are prevalent. It is true that using the same raw materials and fuel the modern rotary clinker will be better performing especially the later age compressive strengths and soundness of cements produced. However the soft burnt nature of the VSK clinker opens up possibilities of addressing customer requirements of good early age compressive strength and early setting in the case of PPC and PSC. The author has found that early age compressive strengths and setting can be matched with modern plants while making PPC with a maximum of 30 per cent fly ash absorption. The Black meal process is capable of producing sound clinkers with less than 1.5 per cent free lime and 45 per cent C3S component. The author’s experience in few VSK plants in Jodhpur-Rajasthan region supports this viewpoint. Experiences with various limestone in Northern India and Bhutan reveals that the technology cannot tolerate high magnesia limestone primarily due to the absence of rapid cooling arrangement but adding certain industrial wastes with mineralising minor constituents gives amazing results in reducing or mitigating this deleterious effect.
- Consistency of clinker: Consistency does get affected if the raw mix is not well homogenised and nodulisation is not controlled. However these can be easily solved by using good homogenisation and blending techniques. Nodulisation can be automated to yield nodules of good strength. In some cases nodule strength can be improved by double nodulisation. Various industrial wastes like bagasse from sugar industry have been found to improve nodule strength together with bonus addition of heat value. Waste oils can be added at this stage to give very good results.
- Heat difference between the central and peripheral charge especially in the large dia kilns of 100 TPD per day can be a matter of concern in some cases depending of raw materials and fuels used. The 50 tonne/day Saboo shaft kiln design was found to very efficient in this respect. Crust formations were found to be minimal. Dustry clinker due to beta to gamma conversion of C2S is prevalent in few cases but can be eliminated by stabilisation of phases even with the inherent disadvantage of rapid or quench cooling.
Plant scale trials using various alternate materials and fuels:
Use of pond ash, bottom ash and boiler fired rice husk ash in a 50 TPD VSK plant in Kanpur Dehat, Uttar Pradesh: Both bottom and pond ash were procured from Panki Thermal power plant and were used as components of raw mix separately as a source of Silica and Alumina by partial replacement of plastic clay by 15 to 20 per cent. There was drop in free lime from 2.2 per cent to 1.8 per cent and the dust content in clinker reduced drastically. There was increase of 1.5 to 2.0 MPa in 3 days and 3 MPa in 28days compressive strength of 43 grade OPC. The pond and bottom ash had substantial carbon particles (LOI- 15 to 20 per cent) which added some heat value and perhaps the reactivity of the raw mix increased by the presence of some amount of reactive alumino-silicates. Indirect effects noticed was smooth kiln operations with a slight increase of production from the 50 TPD VSK. Pond ash which is generally wet can be added directly during nodulisation if a dosing arrangement is designed to avoid the drying operation. Boiler fired Rice Husk was tried in the same plant which gave very good results in improving clinker quality. The material was black in colour with LOI around 10 per cent indicating unburnt carbon which must have supplemented the heat input. It was possible to add rice husk as it is but plant scale trial was not attempted with the apprehension that the husk fibres may not give a homozenised mix in the existing raw grinding arrangement.
Use of Phosphorus furnace slag, alkali bypass dust and bag house dust from a Calcium Carbide plant: All these materials were tried with a contention to capitalise mineralising effect from the wastes due to some minor constituents or the presence of reactive silica or Alumina. Even granulated blast furnace slag (GBFS) was also tried. Improvements in kiln productivity and quality was noticed of clinker in most of the cases. In VSK operation any measure which goes to ensure completion of the reactions in the short burning zone will definitely go in improving clinker quality and smooth kiln operations. Appropriate raw mix fineness with correct proportioning of waste materials and fuels, homogenisation hold the key to success.
Additions of alternate waste materials with VSK clinker to make composite cements The future of cement making is composite cements. This not will helps to use some industrial or agricultural wastes in the final product but also help to improve performance of cements and reduce the carbon footprint. In many cases it can lead to low cost cements together with better performance.
Significant improvement was observed when 5 per cent bag house dust from a calcium carbide plant was added in a quaternary mix of 60 per cent Granulated Blast Furnace slag (GBFS) and 3 per cent gypsum using VSK clinker. Initial setting time was reduced from 180 minutes to 40 minutes when compared with plain control sample of PSC. There was an improvement of 2 MPa at 3 days and 28 days compressive strength was more or less the same. Quaternary blends using Alkali bypass dust and 60 to 70 per cent GBFS , gypsum and VSK clinker also performed well in terms of faster setting and improvement of early age compressive strength. Similar results were obtained while using brick kiln ash and calcined clay Pozzolana in dosages of 15 to 20 per cent while making PPC mixes using VSK clinker.
Thus VSK clinker can act as a performance enhancer for early setting and early age compressive strength in presence of high dosage GBFS containing PSC cements and fly ash/CCP based Pozzolanic cements. Hydration studies have revealed that the soft burnt VSK clinker releases soft burnt lime at a faster rate in the early ages leading to higher quantity hydration products both with GBFS and Pozzolana.
Conclusion
The author was associated with VSK plants for six years while doing his Ph.D. His doctoral work is mainly associated with hydration studies of composite cements and VSK clinker doped with ions coming from various industrial and agricultural wastes. He feels that the black meal process using modern vertical shaft kiln technology can be a viable proposition to use localised waste materials available in limited quantities. The process simplicity of the Black Meal process opens up immense potential for use of wastes (both agricultural and Industrial) with improved cement performance in many cases. Waste generating plants can have captive VSK plants or sub let this activity to local entrepreneurs. All performance enhancements have been validated by actual hydration studies which is available with the author for anyone who is interested. This has been a part of the author’s doctoral work. The author feels that for India till we incorporate large scale AFR facilities catering to large cement plants the VSK plants can be revived mainly for use of localised AFR as the project cost and gestation period from concept to commissioning is very low.
Acknowledgement
The author is grateful to AKS University administration for allowing to publish this paper.
About the author
Prof (Dr) KN Bhattacharjee has 37 years experience in the global cement industry. He has worked with all process technologies of cement manufacture and has done considerable work on use of AFR in mini-cement plants. His Ph.D thesis is in applied cement chemistry and his findings helped many mini-cement plants in India to improve their profitability during the late 80s. He has publications in reputed international and national journals like Cement and Concrete Research, ZKG International, Silicate Industrials, Transactions of Indian Ceramic Society, etc. After his retirement in 2016 from Dangote-Africa, he is teaching cement technology to B.Tech students in AKS University, Satna. Dr KNB has worked with ACC in India, two plants in Oman, Lafarge Canada and Dangote, Africa.
You may like
-
“The greatest potential lies in waste streams.”
-
“AFR supports cost optimisation.”
-
More Oversight Makes Cement Plants Less Safe
-
Beyond the Gearbox: How a Holistic Lubrication Strategy Reduces Total Cost of Ownership in Cement Plants
-
Energy efficient drives improve equipment reliability
-
Digitalisation is transforming asset management
Economy & Market
Leonard Unveils Dual-Head Robotic Arm for Hazardous Industrial Demolition
Published
1 week agoon
October 30, 2026By
admin
Leonard unveils Descender Duo, a dual-head robotic demolition arm designed to improve industrial safety and reduce shutdown time by up to 50 per cent.
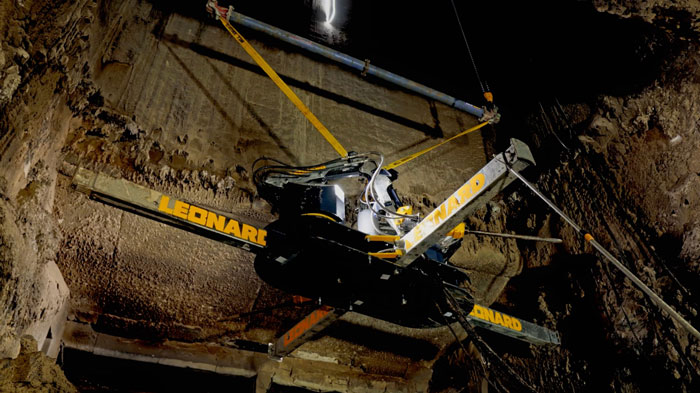
Industrial robotics and refractory services specialist Leonard has launched Descender Duo, a dual-head robotic demolition arm designed to improve safety, accelerate maintenance and reduce shutdown times in hazardous industrial environments. The system made its debut at Lisahally Power Station in Northern Ireland, removing 25 tonnes of slag material within hours.
Developed for the cement, metals, waste-to-energy and petrochemical industries, Descender Duo enables remote-controlled refractory demolition, anchor cutting and welding, and refractory spraying inside boilers, calciners and silos. Its vertical-access design eliminates the need for personnel to enter confined, high-risk spaces during these operations.
Weighing less than two tonnes, the pre-assembled system requires an access opening of just 1.2 m². Supported by an external overhead hoist, it uses electrically operated hydraulic stabilising legs to secure itself inside vessels. The robotic arm offers 360-degree rotation and is suited to vessels approximately 9 m in diameter, with its operating reach extendable through strategically positioned access points.
Equipped with two independently controlled robotic heads, Descender Duo can perform identical or different tasks simultaneously, including refractory demolition, anchor cutting and spraying. Its remote-control system incorporates live camera feeds, allowing operators to monitor operations without entering hazardous environments.
According to Leonard, the technology can deliver time savings of up to 50 per cent compared with manual methods. Its ability to operate at temperatures exceeding 100°C allows maintenance to begin as early as 24 hours after burner shutdown. An all-electric power supply further supports cleaner and more cost-efficient operations.
First Deployment Demonstrates Shutdown Efficiency
The system was first deployed at Burmeister & Wain Scandinavian Contractor’s (BWSC) Lisahally Power Station in Londonderry, Northern Ireland. The facility generates electricity from grade C waste wood, supplying approximately 40,000 homes and businesses.
Leonard and BWSC collaborated to develop a customised solution for the plant’s 26-metre furnace, where extensive external pipework created significant access challenges.
Mark Leonard, Managing Director, Leonard, said, “It required new thinking and rather than step away from the problem we were committed to solving it for the customer, with the customer. We’re relentless in our approach to tackling complex challenges, head-on. We took our years of cement plant experience, coupled with our working knowledge of the BWSC plant, and designed, engineered and tested a completely new vertical solution within just seven weeks from that initial conversation with the customer. That solution was the Descender Duo as we know it today.”
Traditionally, the furnace required a cooling period of up to 36 hours before preparatory work could begin, followed by manual slag removal using rope-access personnel. With Descender Duo, work commenced just 24 hours after shutdown, reducing downtime by up to one day.
The deployment removed 25 tonnes of slag within hours, eliminated the need for at least six workers to enter the hazardous furnace interior and saved 26 hours in the shutdown programme.
“The effectiveness exceeded expectation,” said Martin Doran, Plant Manager at Lisahally Power Station.
“When the Descender Duo concept was first discussed, we had to spend some time with the team from Leonard looking at how it was going to be moved into the furnace. Every site is different and that presented its own challenges, but nothing that the team couldn’t overcome. Once it was installed we were hugely impressed by its efficiency.”
Expanding Industrial Robotics Applications
Descender Duo joins Leonard’s existing portfolio of robotic maintenance solutions, including the Axis horizontal-access arm, Nano confined-space access arm, Charger cement mill media recharging system and Calibre cement mill media grading system.
Headquartered in Northern Ireland, Leonard provides robotic refractory demolition, installation, inspection and industrial maintenance services across the cement, metals, energy, biomass, glass and civil engineering sectors.
Formerly known as G Leonard, the company has more than 35 years of industry experience and operates across Europe, North America, the Middle East, Africa and Asia-Pacific.
The latest innovation reinforces Leonard’s focus on replacing hazardous manual processes with robotic systems that improve workforce safety, enhance operational efficiency and minimise industrial downtime.
Concrete
Martin Engineering Appoints Ashwini Khunte as India General Manager
Published
1 week agoon
October 30, 2026By
admin
Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.
Pune
Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.
Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.
A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.
In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.
Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”
Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.
“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”
Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.
Concrete
Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26
Published
3 weeks agoon
October 19, 2026By
admin
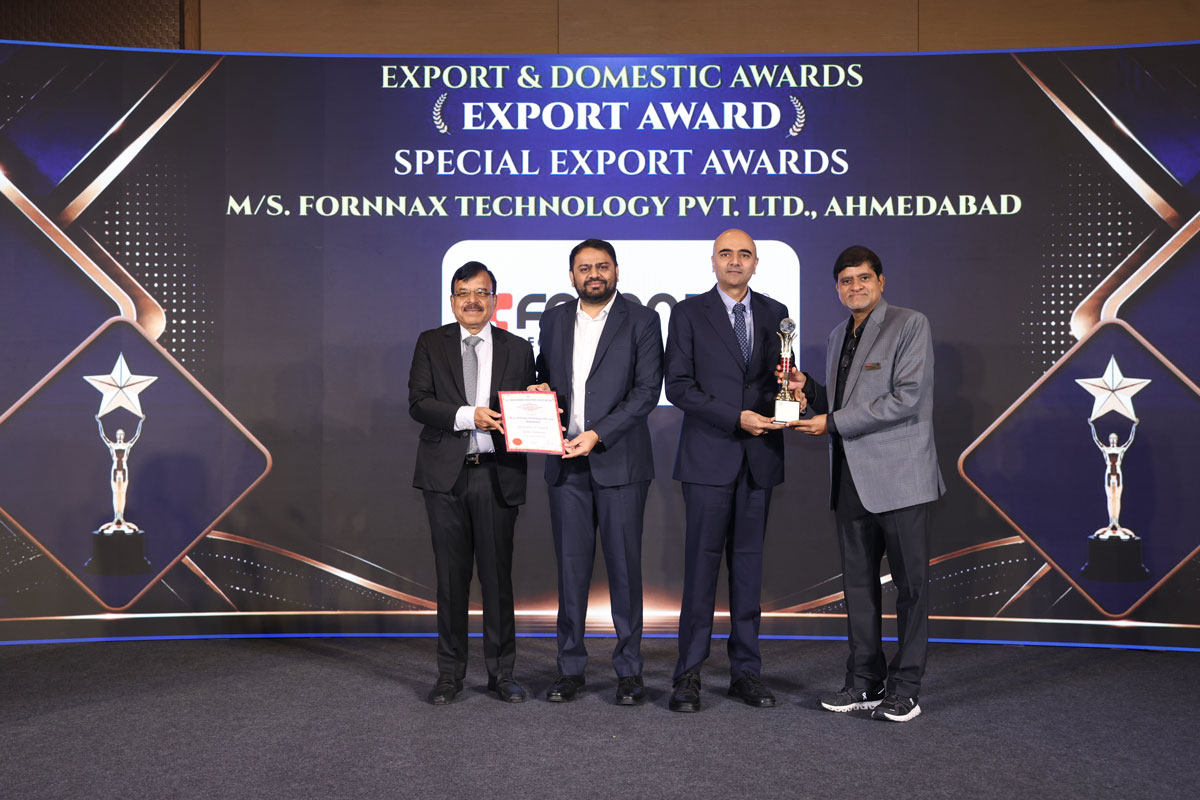
Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.
With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.
The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.
Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:
“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”
Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.
The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.
Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.
For more information, visit: www.fornnax.com
Dhanekula Institute Signs MoU with Adani Cement
JK Lakshmi Cement Begins Rs. 110 bn Assam Plant Project
Kshatriya Engineering College Signs MoU with Adani Cement
Ambuja Cements to Invest Rs. 145 bn to Raise Capacity by FY30
India’s Cement Sector Cuts Energy Use, but Worker Safety Worsens
Dhanekula Institute Signs MoU with Adani Cement
JK Lakshmi Cement Begins Rs. 110 bn Assam Plant Project
Kshatriya Engineering College Signs MoU with Adani Cement
Ambuja Cements to Invest Rs. 145 bn to Raise Capacity by FY30
India’s Cement Sector Cuts Energy Use, but Worker Safety Worsens
Trending News
-
Concrete1 month agoShiva Cement Merges with JSW Cement
-
Concrete4 weeks agoJSW Cement Boards Approve Proposed Shiva Cement Merger
-
Concrete4 weeks agoJSW Cement commissions additional 1 MTPA grinding unit at Nagaur
-
Concrete1 month agoUltraTech becomes first Indian cement firm to cross 2 GW green energy