Connect with us

Concrete

Cement-based building materials

Published

on

Shares

Cement is an intermediate product and is always converted into some other form to have a useful end product. The authors-JD Bapat and Kalpana Karthikeyan-take stock of a few new-generation products that are making inroads in the construction industry.

Concrete is a cement-based building material used in construction industry on very large scale. However there are many other cement-based materials used in to improve the economy, conserve materials, energy and to reduce the carbon footprint of construction. This article focuses on the following four cement-based building materials: dry mixed mortar (DMM) plasters, cement-based fly ash bricks, autoclaved aerated concrete (AAC) blocks, and micro-concrete for concrete repair work.

DMM plaster
The cement-based DMM plaster is different from job-site mortar plaster. It is manufactured in a factory with dedicated facilities for batching and blending of all the necessary ingredients in the controlled process. In this way, DMM plaster with well-defined properties and performance to meet specific requirements and applications can be produced.

DMM plaster provides excellent technical properties to meet the stringent performance requirements which are common in the current construction scenario, such as crack free surface, no leaching and aesthetic look. The use of DMM plaster is cost effective, reducing potential construction problems with the long-term integrity of structures with a simple materials approach. The advantages of DMM plaster are wuality controlled and factory blended to maintain consistently high quality, excellent adhesion, no cement and sand storage required at site, reduces wastage, better workability, suitable for wide range of masonry/concrete backgrounds, fibre reinforced for shrinkage crack resistance, aesthetic look due to better finish, and no leaching. Most DMM plasters require only the addition of potable water and mixed with a simple mixer to produce high-quality fresh mortar for wall application. Normal curing process is followed. Most of the high-performance plasters are usually based on extensive development process and tests in order to achieve the desired materials properties. The basic raw materials are: cement, filler and fine aggregate.

The gradation of aggregate and the choice of the filler are critical. Desirable properties of DMM plaster in fresh and hardened state are as follows.

Mixing time: Mixing time of DMM plaster is one of the important parameters to define its ease of application for the mason. Dry mortar powder should quickly mix with water to get the desired workability.

Workability retention (pot Life): Workability retention is the time taken by fresh mortar/concrete to lose its plasticity. Once the mortar is mixed with water it has to maintain its workability till application, for a reasonable period of time: minimum 60 m in peak summer noon and maximum 90 m in the morning/evening or winter season. Workability Retention can be measured from the time of adding water to dry mix till it loses its plasticity i.e. its nature to stick to wall, when mason applies. Loss of workability before application encourages meson to add water to obtain desired workability and such plaster develops cracks after hardening.

Drying time: Plaster should get surface-dried after application, within certain period of time, to start surface finishing and curing. During the process of curing, plaster attains its early strength and binds properly to the substrate (wall/roof top). Addition of polymers can delay surface drying. Polymer mixed DMM may also stick to trowel and the float used for surface finishing, making the whole process difficult and time-consuming

Coverage area: Good coverage area of a plaster offers cost saving to the customer. Coverage area can be measured by calculating the spread area for constant thickness. It depends on the bulk density of plaster. Higher is the density of plaster lower is the spread area. Density of DMM also affects porosity. Optimum bulk density should be obtained balancing the two factors. Typical coverage can be expressed for 10 mm thickness as: m2/kg

Rebound loss: Rebound loss of a plaster shows its capacity to stick to the wall. Lesser is the rebound loss, lesser the wastage of plaster during application. Rebound loss depends on many factors, irrespective of the nature of plaster.

Firstly, it varies from mason to mason. Sometimes the masons’ handling makes difference in the rebound loss.

Second factor is the water content of a plaster mortar. If water is higher than recommended, mortar applied on the wall slides and does not stick properly. If water is lesser than recommended, mortar gets brittle and falls down immediately. Third factor is "saturation of backing surface". Any readymade plaster product should be used only with recommended water content. Water content fixed by manufacturer is enough to prepare a workable mix. It is very important to make backing surface (substrate) wet till it gets saturated and surface dry. When the surface is not saturated, it absorbs water from the plaster and makes it brittle. Similarly, when the surface is over saturated, excess water makes plaster flowing down the wall. The surface of application should be saturated-surface-dry.

Binding property: The binding of DMM to the backing surface (wall with red clay bricks, fly ash bricks or AAC blocks and roof top) must be tested before application.

Compressive strength: No standards specifically mentions about the compressive strength of cement wall plaster. However, experience shows it should have strength of at least 7 MPa at three days.

Cement-based fly ash bricks
The IS 16720: 2018 gives the specification of fly ash-cement bricks. Pulverized fuel ash or fly ash (FA) is a byproduct from thermal power stations, which use pulverised coal as fuel. This national resource can be gainfully utilised for manufacture of FA-cement bricks as an alternative to common burnt clay bricks, leading to conservation of natural resources and improvement in environment quality. The FA-cement bricks are made from materials consisting of FA in major quantity, cement and aggregate. These bricks are manufactured by mixing of all ingredients, which are then moulded into bricks and are de-moulded when sufficiently hardened and then subjected to curing.

FA and cement together should be considered as binder. IS specifies, FA content should not be less than 35%. However, FA could be as high as 65 per cent depending upon quality of both cement and FA. It will be worthwhile to find the strength of FA+ cement mixture, before deciding proportions. Sand or bottom ash from boiler can be used as aggregate. Nominal maximum size of aggregate should be passing 6.3 mm sieve. The typical dimensions of FA-cement bricks are given in Table 1.

The mixing of ingredients should be done in suitable mechanical mixer. The uniformity of mixture should be tested in terms of color and consistency. The mixture thus prepared may be compacted in moulds by hydraulic or vibratory press or hydraulic-cum-vibratory press and finished to proper size without broken edges. After demoulding, the bricks should be protected till they develop sufficient strength, before curing. Curing can be done with water as per IS 456, mist or steam, so as to develop sufficient strength as required by the designated category. Table 2 gives classification of FA-cement bricks on the basis of 28-day wet compressive strength. The average drying shrinkage is limited to 0.05 per cent (max). The water absorption should be below 20 per cent (mass) for Class up to 10 and below 15 per cent (mass) for higher classes. Typical FA-Cement bricks and red clay bricks are shown in Plate 1.

Advantages of FA-cement bricks over conventional red clay bricks:

  • The strength of common red clay bricks lies in the range of 3.5 to 5 MPa; whereas that of FA-Cement bricks goes up to 15 MPa. Strength also increases over a period of time.
  • Lesser water absorption hence requires less water for curing.
  • Uniform dimensions and more dimensional stability.
  • Lesser transit waste.

AAC blocks
They are also known as cellular blocks. Specification is given in IS 2185 (Part 3). Autoclaved aerated concrete (AAC) is a versatile lightweight construction material and usually used as blocks. Compared to normal dense concrete, AAC has low density and excellent sound and heat insulation properties. The density of AAC is in the range of 450-1000 Kg/m3 as against 2300-2500 Kg/m3 for that of the dense concrete. Plate ? 2 shows typical AAC blocks. The common raw materials used while making AAC are given in the Table – 3

The above proportions may vary subject to different plant practices and requirement of AAC. Quartz-rich sand and gypsum is also be used in the raw mix. Aluminium is added as a pore forming agent. Instead, suitable foaming agent can also be added; however, that method is out of the scope of the present paper. The aluminium reacts with soluble alkalies from cement and calcium hydroxide to form hydrogen bubbles according to chemical reaction: Al + 2OH- + 2H2O ? Al(OH)4- + H2 Hydrogen bubbles formed in reaction are responsible for the pore formation in AAC blocks. The raw mix is poured in the moulds, after mixing. The mixture rises in the moulds after formation of bubbles. It is cured at ambient temperature for about 45 minutes and cut into block pieces of required unit size, with wires. The blocks are further cured in the autoclave with high pressure steam, which also improves their compressive strength. Typical conditions in the curing chamber are steam pressure of 4-16 MPa and curing duration of 8-16 hours.

AAC blocks contain more than 80 per cent air by volume and its mass is about one-fourth of the red clay bricks, making it the lightest building material. The comparison of AAC blocks and burnt (red) clay bricks is given in Table 4.

Micro-concrete for concrete repair work
Micro concrete is a proportionate mixture of Portland cement, graded aggregate of 10 mm down size or 6 mm down size. Micro-concrete also has a non-shrink additive in the mix to limit the plastic shrinkage up to 0.4 per cent.

It is generally used in sections which are inaccessible and where there is thick reinforcement. Generally, micro-concreting is done as a repair job in structures. The distressed concrete section or spalled concrete is removed and after application of suitable bonding agent over the existing surface, micro-concrete is poured or applied. Micro-concrete is dimensionally stable and compatible to the existing structural material and section. It is to be noted that shuttering to be done leak proof while micro-concreting and proper curing methods to be followed since the heat of hydration of micro-concrete is higher than normal concrete mixes. Micro-concrete is useful for the following areas of application:

Repair of damaged reinforced concrete elements, like slabs, beams, columns, wall, etc., where access is restricted and compaction is not possible.

To jacket RCC columns, to increase load-bearing capacity (Plate – 3)

The general features and advantages of micro-concrete are as follows.

  • Can be pumped or poured into restricted locations
  • Flowable mortar, hence does not require compaction
  • Develops high initial and ultimate final strength
  • Offers excellent resistance to moisture ingress
  • Makes repaired sections durable
  • Rapid strength gain to facilitate early reinstatement

Free-flowing micro-concrete has been found to be more effective in comparison with conventional OPC concrete. When conventional mix of high strength concrete is used for repair, small gaps may remain around the reinforcement steel either due to poor compaction or settlement, providing a potential site to initiate corrosion. Free-flowing micro-concrete eliminates that problem. The mix proportion of micro-concrete for a typical strength range of 30-50 MPa is given in Table 5.

Note: Fine, sharp washed sand from zone III to IV, as per IS 383 – 2016 May also contain a non-shrink additive to limit plastic shrinkage < 0.4%

ABOUT THE AUTHORS:
Dr J D Bapat is with the Development Professional for Cement and Concrete. Email Email: consult@drjdbapat.com | Web: www.drjdbapat.com
Kalpana Karthikeyan is R&D Manager, Sanghavi Industries

Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Concrete

JK Lakshmi Cement Begins Rs 110 Billion Assam Plant Project

The 2.5 MTPA integrated cement plant is expected to be completed by FY2029.

Published

on

By

Shares
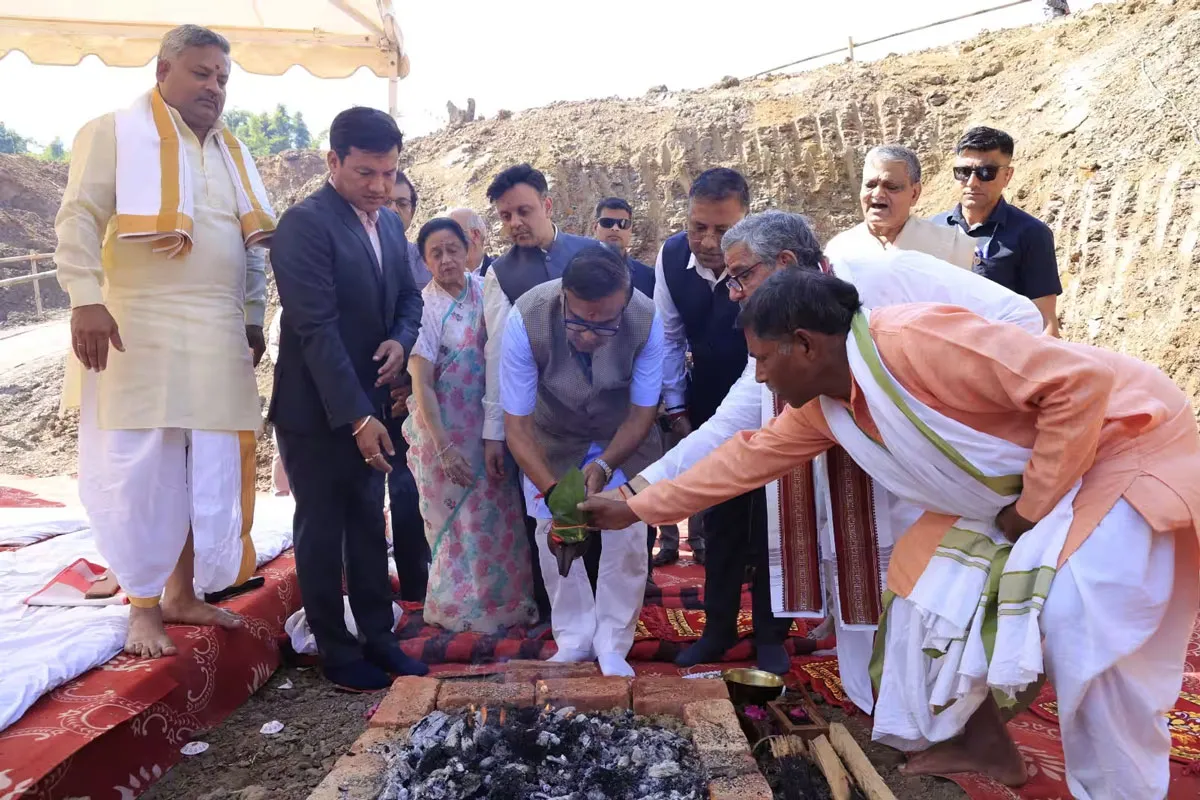
JK Lakshmi Cement has recently laid the foundation stone for Project Kamakshi, its first integrated cement manufacturing facility in Assam, marking its entry into Northeast India. The groundbreaking ceremony was held at Umrangso village in Dima Hasao district in the presence of Assam Chief Minister Himanta Biswa Sarma.
The project involves an investment of Rs 110 billion, including the mining lease, and will have an annual cement production capacity of 2.5 million tonnes, supported by a 1 million tonne clinkerisation unit. Scheduled for completion by FY2029, the facility is expected to generate employment for over 2,000 people while catering primarily to the growing Northeast market.
The integrated plant will feature dedicated railway sidings to facilitate efficient transportation of raw materials and finished cement, strengthening supply chain reliability and regional distribution.
Vinita Singhania, Chairperson and Managing Director, JK Lakshmi Cement, said, “”Project Kamakshi is the start of a long-term relationship with Assam and the wider North East. This is a region that is building fast, and it deserves quality cement made close to home. With this plant, we want to bring scale, jobs, and dependable supply to the region. At JK Lakshmi Cement, we believe that building a stronger India goes beyond infrastructure. It is also about growing together with the communities we serve.””
The investment aligns with the company’s strategy to expand into high-growth markets beyond its established presence in Northern, Western and Eastern India. The project is also expected to support regional economic development and infrastructure growth.
JK Lakshmi Cement aims to pursue its expansion plans while working towards its long-term target of achieving net-zero emissions by 2047.

Continue Reading

Concrete

JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027

JK Lakshmi Cement has deployed more than 70 EVs across its logistics network.

Published

on

By

Shares

JK Lakshmi Cement has deployed more than 70 electric vehicles (EVs) across its logistics network and plans to increase the fleet to 120 vehicles by March 2027. The expansion is part of its decarbonisation strategy, which aims to reduce transport-related emissions and improve operational efficiency.

The company has achieved nearly 100 per cent EV-based clinker dispatches from its Sirohi plant in Rajasthan to the Kalol Grinding Unit in Gujarat. The transition marks an increased use of electric mobility for long-haul cement transportation and is intended to lower the environmental impact of logistics operations.

The existing fleet operates on routes connecting the Sirohi plant with the Kalol Grinding Unit, Palanpur Unit and Surat Grinding Unit. JK Lakshmi Cement is working with electric vehicle logistics providers SwitchLabs and Billion E to support fleet deployment and manage transportation requirements across these routes.

The company expects the planned expansion to increase the use of electric mobility throughout its logistics network for moving cement and clinker. Chairperson and Managing Director Vinita Singhania said the programme reflected the integration of sustainable practices with the company’s focus on long-term business efficiency, while describing the Sirohi–Kalol transition as an important step in its wider decarbonisation strategy.

The EV programme forms part of JK Lakshmi Cement’s green logistics and sustainability roadmap, alongside initiatives to improve efficiency and reduce emissions across its value chain. The company has set a long-term target of achieving net-zero emissions by 2047. It is part of the JK Organisation and operates integrated cement plants in Rajasthan and Chhattisgarh, along with grinding units in Gujarat, Haryana and Odisha. The company has an annual turnover of more than Rs. 60 bn, combined cement capacity of approximately 18 mn t per annum and a target to raise capacity to 30 mn t by 2030. Its portfolio includes ready-mix concrete, gypsum plaster, wall putty, primer, adhesives and fly ash blocks.

Continue Reading

Concrete

Martin Engineering Appoints Ashwini Khunte as India General Manager

Published

on

By

Shares

Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

Pune

Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

“Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

Continue Reading

Video Thumbnail
â–

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    Concrete

    Cement-based building materials

    Published

    on

    Shares


    Cement is an intermediate product and is always converted into some other form to have a useful end product. The authors-JD Bapat and Kalpana Karthikeyan-take stock of a few new-generation products that are making inroads in the construction industry.

    Concrete is a cement-based building material used in construction industry on very large scale. However there are many other cement-based materials used in to improve the economy, conserve materials, energy and to reduce the carbon footprint of construction. This article focuses on the following four cement-based building materials: dry mixed mortar (DMM) plasters, cement-based fly ash bricks, autoclaved aerated concrete (AAC) blocks, and micro-concrete for concrete repair work.

    DMM plaster
    The cement-based DMM plaster is different from job-site mortar plaster. It is manufactured in a factory with dedicated facilities for batching and blending of all the necessary ingredients in the controlled process. In this way, DMM plaster with well-defined properties and performance to meet specific requirements and applications can be produced.

    DMM plaster provides excellent technical properties to meet the stringent performance requirements which are common in the current construction scenario, such as crack free surface, no leaching and aesthetic look. The use of DMM plaster is cost effective, reducing potential construction problems with the long-term integrity of structures with a simple materials approach. The advantages of DMM plaster are wuality controlled and factory blended to maintain consistently high quality, excellent adhesion, no cement and sand storage required at site, reduces wastage, better workability, suitable for wide range of masonry/concrete backgrounds, fibre reinforced for shrinkage crack resistance, aesthetic look due to better finish, and no leaching. Most DMM plasters require only the addition of potable water and mixed with a simple mixer to produce high-quality fresh mortar for wall application. Normal curing process is followed. Most of the high-performance plasters are usually based on extensive development process and tests in order to achieve the desired materials properties. The basic raw materials are: cement, filler and fine aggregate.

    The gradation of aggregate and the choice of the filler are critical. Desirable properties of DMM plaster in fresh and hardened state are as follows.

    Mixing time: Mixing time of DMM plaster is one of the important parameters to define its ease of application for the mason. Dry mortar powder should quickly mix with water to get the desired workability.

    Workability retention (pot Life): Workability retention is the time taken by fresh mortar/concrete to lose its plasticity. Once the mortar is mixed with water it has to maintain its workability till application, for a reasonable period of time: minimum 60 m in peak summer noon and maximum 90 m in the morning/evening or winter season. Workability Retention can be measured from the time of adding water to dry mix till it loses its plasticity i.e. its nature to stick to wall, when mason applies. Loss of workability before application encourages meson to add water to obtain desired workability and such plaster develops cracks after hardening.

    Drying time: Plaster should get surface-dried after application, within certain period of time, to start surface finishing and curing. During the process of curing, plaster attains its early strength and binds properly to the substrate (wall/roof top). Addition of polymers can delay surface drying. Polymer mixed DMM may also stick to trowel and the float used for surface finishing, making the whole process difficult and time-consuming

    Coverage area: Good coverage area of a plaster offers cost saving to the customer. Coverage area can be measured by calculating the spread area for constant thickness. It depends on the bulk density of plaster. Higher is the density of plaster lower is the spread area. Density of DMM also affects porosity. Optimum bulk density should be obtained balancing the two factors. Typical coverage can be expressed for 10 mm thickness as: m2/kg

    Rebound loss: Rebound loss of a plaster shows its capacity to stick to the wall. Lesser is the rebound loss, lesser the wastage of plaster during application. Rebound loss depends on many factors, irrespective of the nature of plaster.

    Firstly, it varies from mason to mason. Sometimes the masons’ handling makes difference in the rebound loss.

    Second factor is the water content of a plaster mortar. If water is higher than recommended, mortar applied on the wall slides and does not stick properly. If water is lesser than recommended, mortar gets brittle and falls down immediately. Third factor is "saturation of backing surface". Any readymade plaster product should be used only with recommended water content. Water content fixed by manufacturer is enough to prepare a workable mix. It is very important to make backing surface (substrate) wet till it gets saturated and surface dry. When the surface is not saturated, it absorbs water from the plaster and makes it brittle. Similarly, when the surface is over saturated, excess water makes plaster flowing down the wall. The surface of application should be saturated-surface-dry.

    Binding property: The binding of DMM to the backing surface (wall with red clay bricks, fly ash bricks or AAC blocks and roof top) must be tested before application.

    Compressive strength: No standards specifically mentions about the compressive strength of cement wall plaster. However, experience shows it should have strength of at least 7 MPa at three days.

    Cement-based fly ash bricks
    The IS 16720: 2018 gives the specification of fly ash-cement bricks. Pulverized fuel ash or fly ash (FA) is a byproduct from thermal power stations, which use pulverised coal as fuel. This national resource can be gainfully utilised for manufacture of FA-cement bricks as an alternative to common burnt clay bricks, leading to conservation of natural resources and improvement in environment quality. The FA-cement bricks are made from materials consisting of FA in major quantity, cement and aggregate. These bricks are manufactured by mixing of all ingredients, which are then moulded into bricks and are de-moulded when sufficiently hardened and then subjected to curing.

    FA and cement together should be considered as binder. IS specifies, FA content should not be less than 35%. However, FA could be as high as 65 per cent depending upon quality of both cement and FA. It will be worthwhile to find the strength of FA+ cement mixture, before deciding proportions. Sand or bottom ash from boiler can be used as aggregate. Nominal maximum size of aggregate should be passing 6.3 mm sieve. The typical dimensions of FA-cement bricks are given in Table 1.

    The mixing of ingredients should be done in suitable mechanical mixer. The uniformity of mixture should be tested in terms of color and consistency. The mixture thus prepared may be compacted in moulds by hydraulic or vibratory press or hydraulic-cum-vibratory press and finished to proper size without broken edges. After demoulding, the bricks should be protected till they develop sufficient strength, before curing. Curing can be done with water as per IS 456, mist or steam, so as to develop sufficient strength as required by the designated category. Table 2 gives classification of FA-cement bricks on the basis of 28-day wet compressive strength. The average drying shrinkage is limited to 0.05 per cent (max). The water absorption should be below 20 per cent (mass) for Class up to 10 and below 15 per cent (mass) for higher classes. Typical FA-Cement bricks and red clay bricks are shown in Plate 1.

    Advantages of FA-cement bricks over conventional red clay bricks:

    • The strength of common red clay bricks lies in the range of 3.5 to 5 MPa; whereas that of FA-Cement bricks goes up to 15 MPa. Strength also increases over a period of time.
    • Lesser water absorption hence requires less water for curing.
    • Uniform dimensions and more dimensional stability.
    • Lesser transit waste.

    AAC blocks
    They are also known as cellular blocks. Specification is given in IS 2185 (Part 3). Autoclaved aerated concrete (AAC) is a versatile lightweight construction material and usually used as blocks. Compared to normal dense concrete, AAC has low density and excellent sound and heat insulation properties. The density of AAC is in the range of 450-1000 Kg/m3 as against 2300-2500 Kg/m3 for that of the dense concrete. Plate ? 2 shows typical AAC blocks. The common raw materials used while making AAC are given in the Table – 3

    The above proportions may vary subject to different plant practices and requirement of AAC. Quartz-rich sand and gypsum is also be used in the raw mix. Aluminium is added as a pore forming agent. Instead, suitable foaming agent can also be added; however, that method is out of the scope of the present paper. The aluminium reacts with soluble alkalies from cement and calcium hydroxide to form hydrogen bubbles according to chemical reaction: Al + 2OH- + 2H2O ? Al(OH)4- + H2 Hydrogen bubbles formed in reaction are responsible for the pore formation in AAC blocks. The raw mix is poured in the moulds, after mixing. The mixture rises in the moulds after formation of bubbles. It is cured at ambient temperature for about 45 minutes and cut into block pieces of required unit size, with wires. The blocks are further cured in the autoclave with high pressure steam, which also improves their compressive strength. Typical conditions in the curing chamber are steam pressure of 4-16 MPa and curing duration of 8-16 hours.

    AAC blocks contain more than 80 per cent air by volume and its mass is about one-fourth of the red clay bricks, making it the lightest building material. The comparison of AAC blocks and burnt (red) clay bricks is given in Table 4.

    Micro-concrete for concrete repair work
    Micro concrete is a proportionate mixture of Portland cement, graded aggregate of 10 mm down size or 6 mm down size. Micro-concrete also has a non-shrink additive in the mix to limit the plastic shrinkage up to 0.4 per cent.

    It is generally used in sections which are inaccessible and where there is thick reinforcement. Generally, micro-concreting is done as a repair job in structures. The distressed concrete section or spalled concrete is removed and after application of suitable bonding agent over the existing surface, micro-concrete is poured or applied. Micro-concrete is dimensionally stable and compatible to the existing structural material and section. It is to be noted that shuttering to be done leak proof while micro-concreting and proper curing methods to be followed since the heat of hydration of micro-concrete is higher than normal concrete mixes. Micro-concrete is useful for the following areas of application:

    Repair of damaged reinforced concrete elements, like slabs, beams, columns, wall, etc., where access is restricted and compaction is not possible.

    To jacket RCC columns, to increase load-bearing capacity (Plate – 3)

    The general features and advantages of micro-concrete are as follows.

    • Can be pumped or poured into restricted locations
    • Flowable mortar, hence does not require compaction
    • Develops high initial and ultimate final strength
    • Offers excellent resistance to moisture ingress
    • Makes repaired sections durable
    • Rapid strength gain to facilitate early reinstatement

    Free-flowing micro-concrete has been found to be more effective in comparison with conventional OPC concrete. When conventional mix of high strength concrete is used for repair, small gaps may remain around the reinforcement steel either due to poor compaction or settlement, providing a potential site to initiate corrosion. Free-flowing micro-concrete eliminates that problem. The mix proportion of micro-concrete for a typical strength range of 30-50 MPa is given in Table 5.

    Note: Fine, sharp washed sand from zone III to IV, as per IS 383 – 2016 May also contain a non-shrink additive to limit plastic shrinkage < 0.4%

    ABOUT THE AUTHORS:
    Dr J D Bapat is with the Development Professional for Cement and Concrete. Email Email: consult@drjdbapat.com | Web: www.drjdbapat.com
    Kalpana Karthikeyan is R&D Manager, Sanghavi Industries

    Continue Reading
    Click to comment

    Leave a Reply

    Your email address will not be published. Required fields are marked *

    Concrete

    JK Lakshmi Cement Begins Rs 110 Billion Assam Plant Project

    The 2.5 MTPA integrated cement plant is expected to be completed by FY2029.

    Published

    on

    By

    Shares


    JK Lakshmi Cement has recently laid the foundation stone for Project Kamakshi, its first integrated cement manufacturing facility in Assam, marking its entry into Northeast India. The groundbreaking ceremony was held at Umrangso village in Dima Hasao district in the presence of Assam Chief Minister Himanta Biswa Sarma.
    The project involves an investment of Rs 110 billion, including the mining lease, and will have an annual cement production capacity of 2.5 million tonnes, supported by a 1 million tonne clinkerisation unit. Scheduled for completion by FY2029, the facility is expected to generate employment for over 2,000 people while catering primarily to the growing Northeast market.
    The integrated plant will feature dedicated railway sidings to facilitate efficient transportation of raw materials and finished cement, strengthening supply chain reliability and regional distribution.
    Vinita Singhania, Chairperson and Managing Director, JK Lakshmi Cement, said, “”Project Kamakshi is the start of a long-term relationship with Assam and the wider North East. This is a region that is building fast, and it deserves quality cement made close to home. With this plant, we want to bring scale, jobs, and dependable supply to the region. At JK Lakshmi Cement, we believe that building a stronger India goes beyond infrastructure. It is also about growing together with the communities we serve.””
    The investment aligns with the company’s strategy to expand into high-growth markets beyond its established presence in Northern, Western and Eastern India. The project is also expected to support regional economic development and infrastructure growth.
    JK Lakshmi Cement aims to pursue its expansion plans while working towards its long-term target of achieving net-zero emissions by 2047.

    Continue Reading

    Concrete

    JK Lakshmi Cement to Expand EV Fleet to 120 Vehicles by March 2027

    JK Lakshmi Cement has deployed more than 70 EVs across its logistics network.

    Published

    on

    By

    Shares


    JK Lakshmi Cement has deployed more than 70 electric vehicles (EVs) across its logistics network and plans to increase the fleet to 120 vehicles by March 2027. The expansion is part of its decarbonisation strategy, which aims to reduce transport-related emissions and improve operational efficiency.

    The company has achieved nearly 100 per cent EV-based clinker dispatches from its Sirohi plant in Rajasthan to the Kalol Grinding Unit in Gujarat. The transition marks an increased use of electric mobility for long-haul cement transportation and is intended to lower the environmental impact of logistics operations.

    The existing fleet operates on routes connecting the Sirohi plant with the Kalol Grinding Unit, Palanpur Unit and Surat Grinding Unit. JK Lakshmi Cement is working with electric vehicle logistics providers SwitchLabs and Billion E to support fleet deployment and manage transportation requirements across these routes.

    The company expects the planned expansion to increase the use of electric mobility throughout its logistics network for moving cement and clinker. Chairperson and Managing Director Vinita Singhania said the programme reflected the integration of sustainable practices with the company’s focus on long-term business efficiency, while describing the Sirohi–Kalol transition as an important step in its wider decarbonisation strategy.

    The EV programme forms part of JK Lakshmi Cement’s green logistics and sustainability roadmap, alongside initiatives to improve efficiency and reduce emissions across its value chain. The company has set a long-term target of achieving net-zero emissions by 2047. It is part of the JK Organisation and operates integrated cement plants in Rajasthan and Chhattisgarh, along with grinding units in Gujarat, Haryana and Odisha. The company has an annual turnover of more than Rs. 60 bn, combined cement capacity of approximately 18 mn t per annum and a target to raise capacity to 30 mn t by 2030. Its portfolio includes ready-mix concrete, gypsum plaster, wall putty, primer, adhesives and fly ash blocks.

    Continue Reading

    Concrete

    Martin Engineering Appoints Ashwini Khunte as India General Manager

    Published

    on

    By

    Shares

    Martin Engineering names Ashwini Khunte India General Manager to strengthen operations and drive growth across key bulk material handling sectors.

    Pune

    Martin Engineering, a global provider of bulk material handling solutions, has appointed Ashwini Khunte as General Manager of its India business, strengthening its leadership as the company expands its presence across the country’s cement, mining, steel, power and infrastructure sectors.

    Khunte brings more than a decade of experience with Martin Engineering, having joined its Indian operations in 2013 as a Design Engineer, shortly after the company established its presence in the country in 2012.

    A mechanical engineer by qualification, she spent her initial five years developing bulk material handling solutions in collaboration with the company’s operations team. During this period, she gained extensive experience addressing operational challenges in the steel, cement and coal industries. She subsequently moved into project engineering, managing major engineering, procurement and construction (EPC) and original equipment manufacturer (OEM) projects from initial enquiry to commissioning. Her responsibilities later expanded to overseeing Martin Engineering’s conveyor product portfolio in India, involving customer engagement, technical presentations and site visits across heavy industries.

    In 2024, Khunte was promoted to Head of Sales & Marketing for the company’s Europe, Middle East, Africa and India (EMEAI) region. The position broadened her international market exposure and strengthened her strategic and commercial leadership capabilities.

    Commenting on her appointment, Ashwini Khunte, General Manager, Martin Engineering India, said: “India represents a tremendous opportunity for Martin Engineering. The country’s continued investment in cement, mining, steel, power and infrastructure is creating increasing demand for safer, cleaner and more productive bulk material handling, and that’s exactly what we do. My priority will be to build on the strong foundations already established in India, while continuing to develop our people, strengthen customer relationships and bring practical solutions to the challenges faced by our industry.”

    Robert Whetstone, Area Vice President – EMEAI, Martin Engineering, highlighted Khunte’s technical expertise, market understanding and leadership experience.

    “Ashwini brings an exceptional combination of technical understanding, customer knowledge and commercial leadership. She has grown as Martin Engineering has grown, and has consistently demonstrated outstanding capability to transform her expertise into practical solutions. Her knowledge of the Indian market, together with her international experience, makes her ideally suited to lead our India business through its next stage of growth for years to come.”

    Since establishing its Indian business in 2012, Martin Engineering has expanded its local workforce, manufacturing capabilities and dealership network. The company supplies conveyor products, transfer point solutions, material flow aids, training and technical support to bulk material handling industries. Khunte’s appointment positions the company to further strengthen customer relationships and expand its solutions portfolio in India’s growing industrial and infrastructure markets.

    Continue Reading

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds