Connect with us

Economy & Market

Versatile, Vital & Dependable

Published

on

Shares

Roots Blowers have been a common utility in cement plants for a very long time now. Whenever a large volume of air is to be used at constant pressure, a Roots Blower is the right equipment.
The Roots Blower design was patented way back in 1860 by Philander Higley and Francis Marian Roots. The name of the equipment is derived from the name of the scientist; the blower is recognised as ?Roots Blower? or ?Rotary Air Blower? in the industry.
The executing mechanism of the blower is intake of air from the inlet; dual impellers rotating in different directions or the same direction trap the air during the rotation between the casing and impeller and discharge at the outlet. The mechanism of the blower is unique and traditional. The blower throws a consistent volume of gas to the outlet without discharge. The gas-blowing capacity of a Roots Blower depends on the size of casing and rotating part. Thus, a Roots Blower is unique compared to a compressor. The manufacturing of Roots Blowers is done either by SMEs or MSMEs in various parts of the country. There are a good number of manufacturers meeting the requirement of the industry.

The blowers have higher efficiency at moderate compression ratios, and are most efficient in the compression ratios of 1.1 to 2. They find use in applications which require relatively constant flow rate at varying discharge pressures. There are various types of Roots Blowers, mainly categorised as air-cooled blowers and water-cooled blowers. The capacity of blowers varies from 10 M3/Hr to 14000 M3/Hr. The blower should be made up of good quality and sturdy parts. There should be no machine vibration during operation execution, as this may bring down the blowing capacity of the machine. The Roots Blower must be a power-saving unit, and continue functioning over a long period of time, with low electricity consumption.

Twin-lobe rotary air blowers consist of a pair of involute profiled (shape of 8) lobes/rotors rotating inside an oval-shaped casing, closed at ends by side plates. One lobe is the driving lobe, which is driven by external power, while the driven lobe is driven by a pair of equal ratio gears. Both lobes rotate at the same speed, but in opposite directions. As the rotors rotate, air is drawn into the inlet side of the cylinder and forced out of the outlet side against the system pressure. With each revolution, four such volumes are displaced.

In the case of three-lobe rotary blowers, the shape of the rotor is different. The two three-lobe rotors rotate in a direction opposite to each other. Running on the same operating speed, three-lobe blowers can deliver larger air flow and volume than conventional two-lobe blowers.

Since the lobes run within the casing with finite clearances, no internal lubrication is required. Thus, the air delivered is 100 per cent oil-free. These blowers deliver, practically, a constant flow rate independent of the discharge pressure conditions. The flow rate is largely dependent on the operating speed.

These machines are extensively used in applications such as pneumatic conveying, aeration, cement plants, water treatment plants for filter backwash, aquaculture, aeration etc. They are used as general utilities, more commonly where the distance is short and a large volume of air is required (during blending, aeration, fluidisation and conveying).

Fuller-Kinyon (FK) Pump
The Fuller-Kinyon (FK) Pump was first introduced in 1926. It is a very versatile equipment, popular for lower power consumption, less maintenance needs, and increased efficiency, flexibility and reliability over other pneumatic systems. It is commonly known as an FK pump or a Screw Pump and it is ideal for conveying fine powders without risk of blowback. The design of the pump ensures that a material seal is formed when the product is compacted in the barrel and forced against the counterweighted flapper valve preventing air leakage back through the screw. Only one moving part means less maintenance and high reliability in the most demanding environments. It has an inlet for supply of compressed air.

The FK Pump operates with line pressures up to 30 psig. Parts can be replaced without removing the pump from service. Recent technological improvements on the FK Pump include the use of high-wear pump screws, and the pneumatic flap controller for optimisation of throughput of the system.

Screw Pumps are constructed of mild and structural steel, and mounted on a base. These pumps can be equipped with pedestal blocks that support a pump screw which helps to provide a smooth, balanced operation. The screw is dynamically balanced. Areas of this screw, along with other parts of the pump in direct contact with the material to be conveyed, are made of hardened, wear-resistant material and special hard surfacing where required. The screw is directly coupled to the driving motor but can be V-belt driven.

The materials to be conveyed enter from the hopper by gravity. Then the material is compacted as it is advanced. Its density is further increased in the space between the terminal flight of the screw and the face of the non-return valve to form a seal against the transport line pressure, thus preventing blowback.

The material then enters the discharge body, is fluidised by compressed air, and is conveyed into the transport line.

Dry bulk materials are conveyed literally anywhere a pipeline can be run and to any number of delivery points. Distances of 4,500 feet (1,371 meters) are not uncommon.

Multinational companies like FLSmidth are well-known suppliers of these types of pumps. Currently, upgrades of the pump are available.


Continue Reading
Click to comment

Leave a Reply

Your email address will not be published. Required fields are marked *

Concrete

Fornnax Wins AIRIA’s Special Export Award for Rubber Machinery in 2025-26

Published

on

By

Shares

Fornnax Technology Pvt. Ltd. has been honoured with the Special Export Award – Rubber Machinery for 2025–26 by the All-India Rubber Industries Association (AIRIA), in recognition of its highest exports of tyre recycling plants to the European region.

With more than a decade of experience in India’s tyre recycling industry, Fornnax has contributed to the development of advanced recycling technologies and infrastructure. The company currently holds a 90% market share in India’s domestic tyre recycling sector, while exports account for 30% of its business, spanning markets such as Europe, Australia and the GCC.

The award marks another milestone for Fornnax, whose tyre recycling lines and advanced shredding technologies are supporting the growth of the circular economy in India and international markets.

Commenting on the recognition, Mr. Jignesh Kundaria, Founder and Director of Fornnax, said:

“This honour from AIRIA is a reflection of an incredible journey we have undertaken over the years. When we started Fornnax, there was no established recycling industry in India to follow. We chose to build for the future instead. Today, when you see India’s tyre recycling sector, it has already transformed into a dynamic, high-growth industry and we are extremely proud to have played our part in building it.”

Unlike standalone equipment suppliers, Fornnax focuses on developing complete, high-capacity recycling infrastructure. Its integrated systems combine multiple stages of shredding and size reduction to enable efficient, continuous operations. This system-level engineering approach helps recycling operators improve throughput, equipment reliability and operational consistency.

The recognition reinforces Fornnax’s commitment to developing engineering technologies that contribute to a more efficient and circular recycling ecosystem.

Looking ahead, the company aims to expand its international presence while continuing to develop advanced shredding and recycling solutions to address the growing volumes and evolving requirements of the global recycling industry.

For more information, visit: www.fornnax.com

Continue Reading

Concrete

Wonder Cement appoints Mahesh Singh as VP Corporate Brand Communication 

Published

on

By

Shares

Singh brings 20+ years of brand and marketing experience, and will lead integrated corporate brand communication initiatives at Wonder Cement 

New Delhi

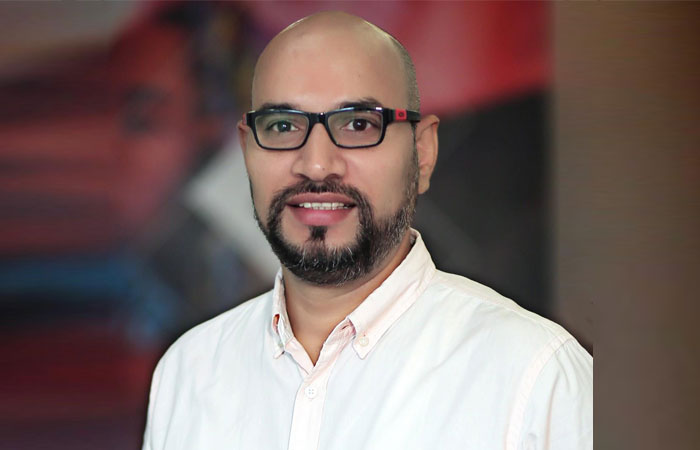
Wonder Cement, a leading cement manufacturer, has appointed Mahesh Singh as Vice President – Corporate Brand Communication. In his new role, he will oversee corporate brand strategy and communication, including digital and performance marketing, public relations, trade, events, exhibitions, sports and experiential marketing. 

Singh brings over two decades of experience across marketing and communications, with roles spanning the automotive industry, agencies and entrepreneurship. He spent more than a decade with Honda Motorcycle & Scooter India, working across integrated communication, media, digital, retail and consumer engagement. His stint also included helping build the company’s digital marketing capabilities. 

He moved to dentsu X India as Vice President – Strategy & Planning, working across categories such as automotive, auto components, electric vehicles, FMCG, consumer electronics, BFSI, apparel and brand consulting. His responsibilities included media and marketing strategy, product launches, content, performance marketing and consumer activations. 

Singh subsequently took an entrepreneurial route with Radiant Brands before joining Shriram Ltd (SPR Autotech) as Head – Marketing & Communications. There, his remit included brand and corporate strategy, communications, PR and ORM, retail identity, loyalty programmes and events. 

At Wonder Cement, Singh will be responsible for bringing together the company’s corporate brand communication initiatives across digital, performance marketing, PR, trade, sports and experiential platforms. The role will focus on creating an integrated approach to communication across consumers, trade partners and other key stakeholders. 

The appointment brings to Wonder Cement a marketer whose career has spanned the brand, agency and entrepreneurial sides of the communications ecosystem. 

Wonder Cement, part of the RK Group, is a cement manufacturer with roots in Rajasthan and a focus on quality, trust and transparency. The company has grown to six manufacturing plants, and a cement capacity of 21.5 MTPA. With more than 2,000 employees and a network of over 5,000 dealers, its operations span manufacturing, distribution and customer engagement, with a focus on consistent product quality and efficient execution. 

Continue Reading

Concrete

JSW Cement commissions additional 1 MTPA grinding unit at Nagaur

Published

on

By

Shares

With this commissioning, JSW Cement’s total cement grinding capacity has increased to 25.10 MTPA, 
Mumbai

JSW Cement, one of India’s leading green cement producers and part of the diversified JSW Group, today announced the successful commissioning of an additional 1.00 MTPA cement grinding unit at Nagaur, Rajasthan. The commissioning marks another significant milestone in the Company’s growth strategy.

With this commissioning, JSW Cement’s total cement grinding capacity has increased to 25.10 MTPA, while its total clinker manufacturing capacity, including clinker capacity at its joint venture, JSW Cement FZC, stands at 9.74 MTPA.

JSW Cement had commenced operations in North India in March 2026 with the Nagaur Integrated Plant, comprising a 3.30 MTPA clinkerisation unit and 2.50 MTPA cement grinding unit. With the commissioning of the additional 1.00 MTPA cement grinding unit, the plant’s total cement grinding capacity has increased to 3.50 MTPA, enhancing the company’s ability to cater to the growing cement demand across Rajasthan, Haryana, Punjab and the National Capital Region (NCR). The expansion has been funded through a strategic mix of equity and long-term debt.

During the quarter ended 30th September 2026, JSW Cement has also commissioned the Alternate Fuel Handling System and the Waste Heat Recovery system (WHRS) at the Nagaur Integrated Plant.

Nilesh Narwekar, CEO, JSW Cement, said: “The commissioning of additional 1.00 MTPA grinding capacity at Nagaur is a key strategic priority for us and will accelerate JSW Cement’s expansion into North India. We look forward to servicing the growing needs of the region and contributing to the economic growth of Rajasthan, Haryana, Punjab and the NCR area. I am delighted to share that the company has commissioned this grinding unit within the expected timeline, showcasing our project execution capabilities. Further, the Alternate Fuel Handling System and the Waste Heat Recovery system (WHRS) are expected to substantially reduce our production costs going forward.”

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds