Connect with us

Concrete

JK Cement plans to foray into the paints business

JK Cement (JKCE) in a conference call has announced its plans to invest ?6 billion in the business of decorative paints over the span of next five years focussed in the North and Central markets.

Published

on

Shares

JK Cement (JKCE) in a conference call has announced its plans to invest ?6 billion in the business of decorative paints over the span of next five years focussed in the North and Central markets. JKCE aims to start with an initial capacity of 60,000 kilo litres in Uttar Pradesh by April 2024.

The company is planning to spend ?3 billion on the plant and equipment. The remaining balance will be put into branding, working capital and funding losses in the initial years. The yearly out go in the paints business has been planned to be capped at 8-10 per cent of EBITDA of the existing business. Subsequent investments will be funded via internal accruals of the paints business and will be funded through a mix of equity and preference share capital without raising any debt at the paint subsidiary level.  

JKCE has set the target revenue as ?1-1.5 billion in the first year (FY25) and has projected it to grow at the same rate each year, with ?7-8 billion revenues on full utilisation of initial capacity. The core cement business will continue to be the focus area, and a de-merging of the paint business may be considered and listed separately once it achieves a sizeable scale. JKCE management mentions that ?the paints business is an extension of its putty business as it shares a common retail channel and influencers. JKCE sells putty via over 60,000 dealers (one-third in the North and UP markets), of which 70 per cent are paint outlets and 30 per cent are hardware stores.?

Concrete

ABB Drives Digital Transformation at TCI MAX Cement Plant in J&K

Published

on

By

Shares

ABB deploys advanced process control at TCI MAX’s Srinagar cement plant to improve clinker quality, energy efficiency and sustainable manufacturing.

Kashmir 

ABB has deployed its advanced process control technology at TCI MAX Cement’s Srinagar facility in Jammu and Kashmir, marking the region’s first reported implementation of advanced process control (APC) in cement manufacturing and strengthening efforts towards more efficient, digitally enabled production.

Announced on 5 November 2026, the deployment of ABB Ability™ Expert Optimizer at the facility, operated by Trumboo Industries Pvt. Ltd., aims to improve process stability, clinker quality, energy efficiency and overall plant productivity. The implementation forms part of TCI MAX’s strategy to modernise its manufacturing operations through automation and digital technologies.

Following the integration of ABB’s advanced process control solution and supporting IT infrastructure, TCI MAX has reported improvements in operational productivity, product quality and sustainability-related performance indicators. The technology focuses on optimising the cement pyro process, a critical stage of production involving high-temperature processing and clinker formation.

Waseem Ahmed Trumboo, Director, Trumboo Industries Pvt. Ltd., said: “Introducing advanced process control at TCI MAX is an important step in how we are evolving our operations. Our focus is on improving the stability and efficiency of our processes while maintaining consistent clinker quality. We have been encouraged by the performance of the solution during commissioning and by the support from the ABB team, and we look forward to realizing its full potential.”

ABB Ability™ Expert Optimizer combines advanced process control, model predictive control (MPC) and artificial intelligence (AI) to continuously monitor and optimise manufacturing operations. By analysing process conditions, predicting operational behaviour and automatically adjusting key parameters, the system enables more consistent production while reducing process variability.

In cement manufacturing, maintaining stable pyro-processing conditions is essential for achieving uniform clinker quality and optimising thermal energy consumption. Fluctuations in operating parameters can affect fuel efficiency, production output and product consistency.

The deployment is designed to address these challenges through real-time process optimisation, helping operators maintain more stable kiln operations while improving the utilisation of fuel, electricity and raw materials.

Kapil Agarwal, Senior Vice President and Local Division Manager, Process Industries Division, ABB India, said: “Cement producers are increasingly looking to adopt digital technologies to achieve greater consistency and efficiency while addressing their sustainability priorities. ABB Ability™ Expert Optimizer brings advanced process control and deep cement process expertise together to help operators make their processes more stable and efficient. We are pleased to support TCI MAX as it takes this important step in its digital transformation.”

The technology also supports sustainability objectives by optimising fuel consumption, improving electrical energy efficiency and minimising process waste. More stable operations can contribute to lower energy intensity and reduced emissions associated with cement production.

For TCI MAX, the investment represents a move towards data-driven manufacturing, where automated control systems complement operator expertise to improve production performance and operational reliability.

The implementation is particularly significant for Jammu and Kashmir’s cement industry, as it introduces advanced process optimisation technology to a regional manufacturing facility. Its deployment could demonstrate the potential for wider adoption of digital automation across cement plants seeking to modernise their operations.

The project builds on ABB’s experience in delivering advanced process control solutions to cement manufacturers worldwide. Through the integration of industrial automation, predictive technologies and process engineering expertise, the company supports manufacturers in improving resource efficiency and maintaining consistent production quality.

As cement producers face increasing pressure to manage energy costs, improve productivity and reduce their environmental footprint, technologies such as AI-enabled process control and predictive optimisation are becoming important components of plant modernisation strategies.

ABB’s Expert Optimizer provides a platform for addressing these priorities by enabling automated adjustments based on changing process conditions, reducing reliance on manual intervention and supporting more efficient plant operation.

ABB, a global technology company specialising in electrification and automation, has more than 140 years of industrial experience and approximately 110,000 employees worldwide. Its Automation business employs around 26,000 people and provides technologies and services across process, hybrid and maritime industries.

The TCI MAX deployment reinforces ABB’s growing role in the digital transformation of cement manufacturing in India, where improving process efficiency and reducing energy consumption remain critical to the industry’s long-term sustainability.

With the advanced process control system now implemented at its Srinagar facility, TCI MAX aims to build on the initial operational improvements and further optimise production efficiency, clinker consistency and environmental performance.


Continue Reading

Concrete

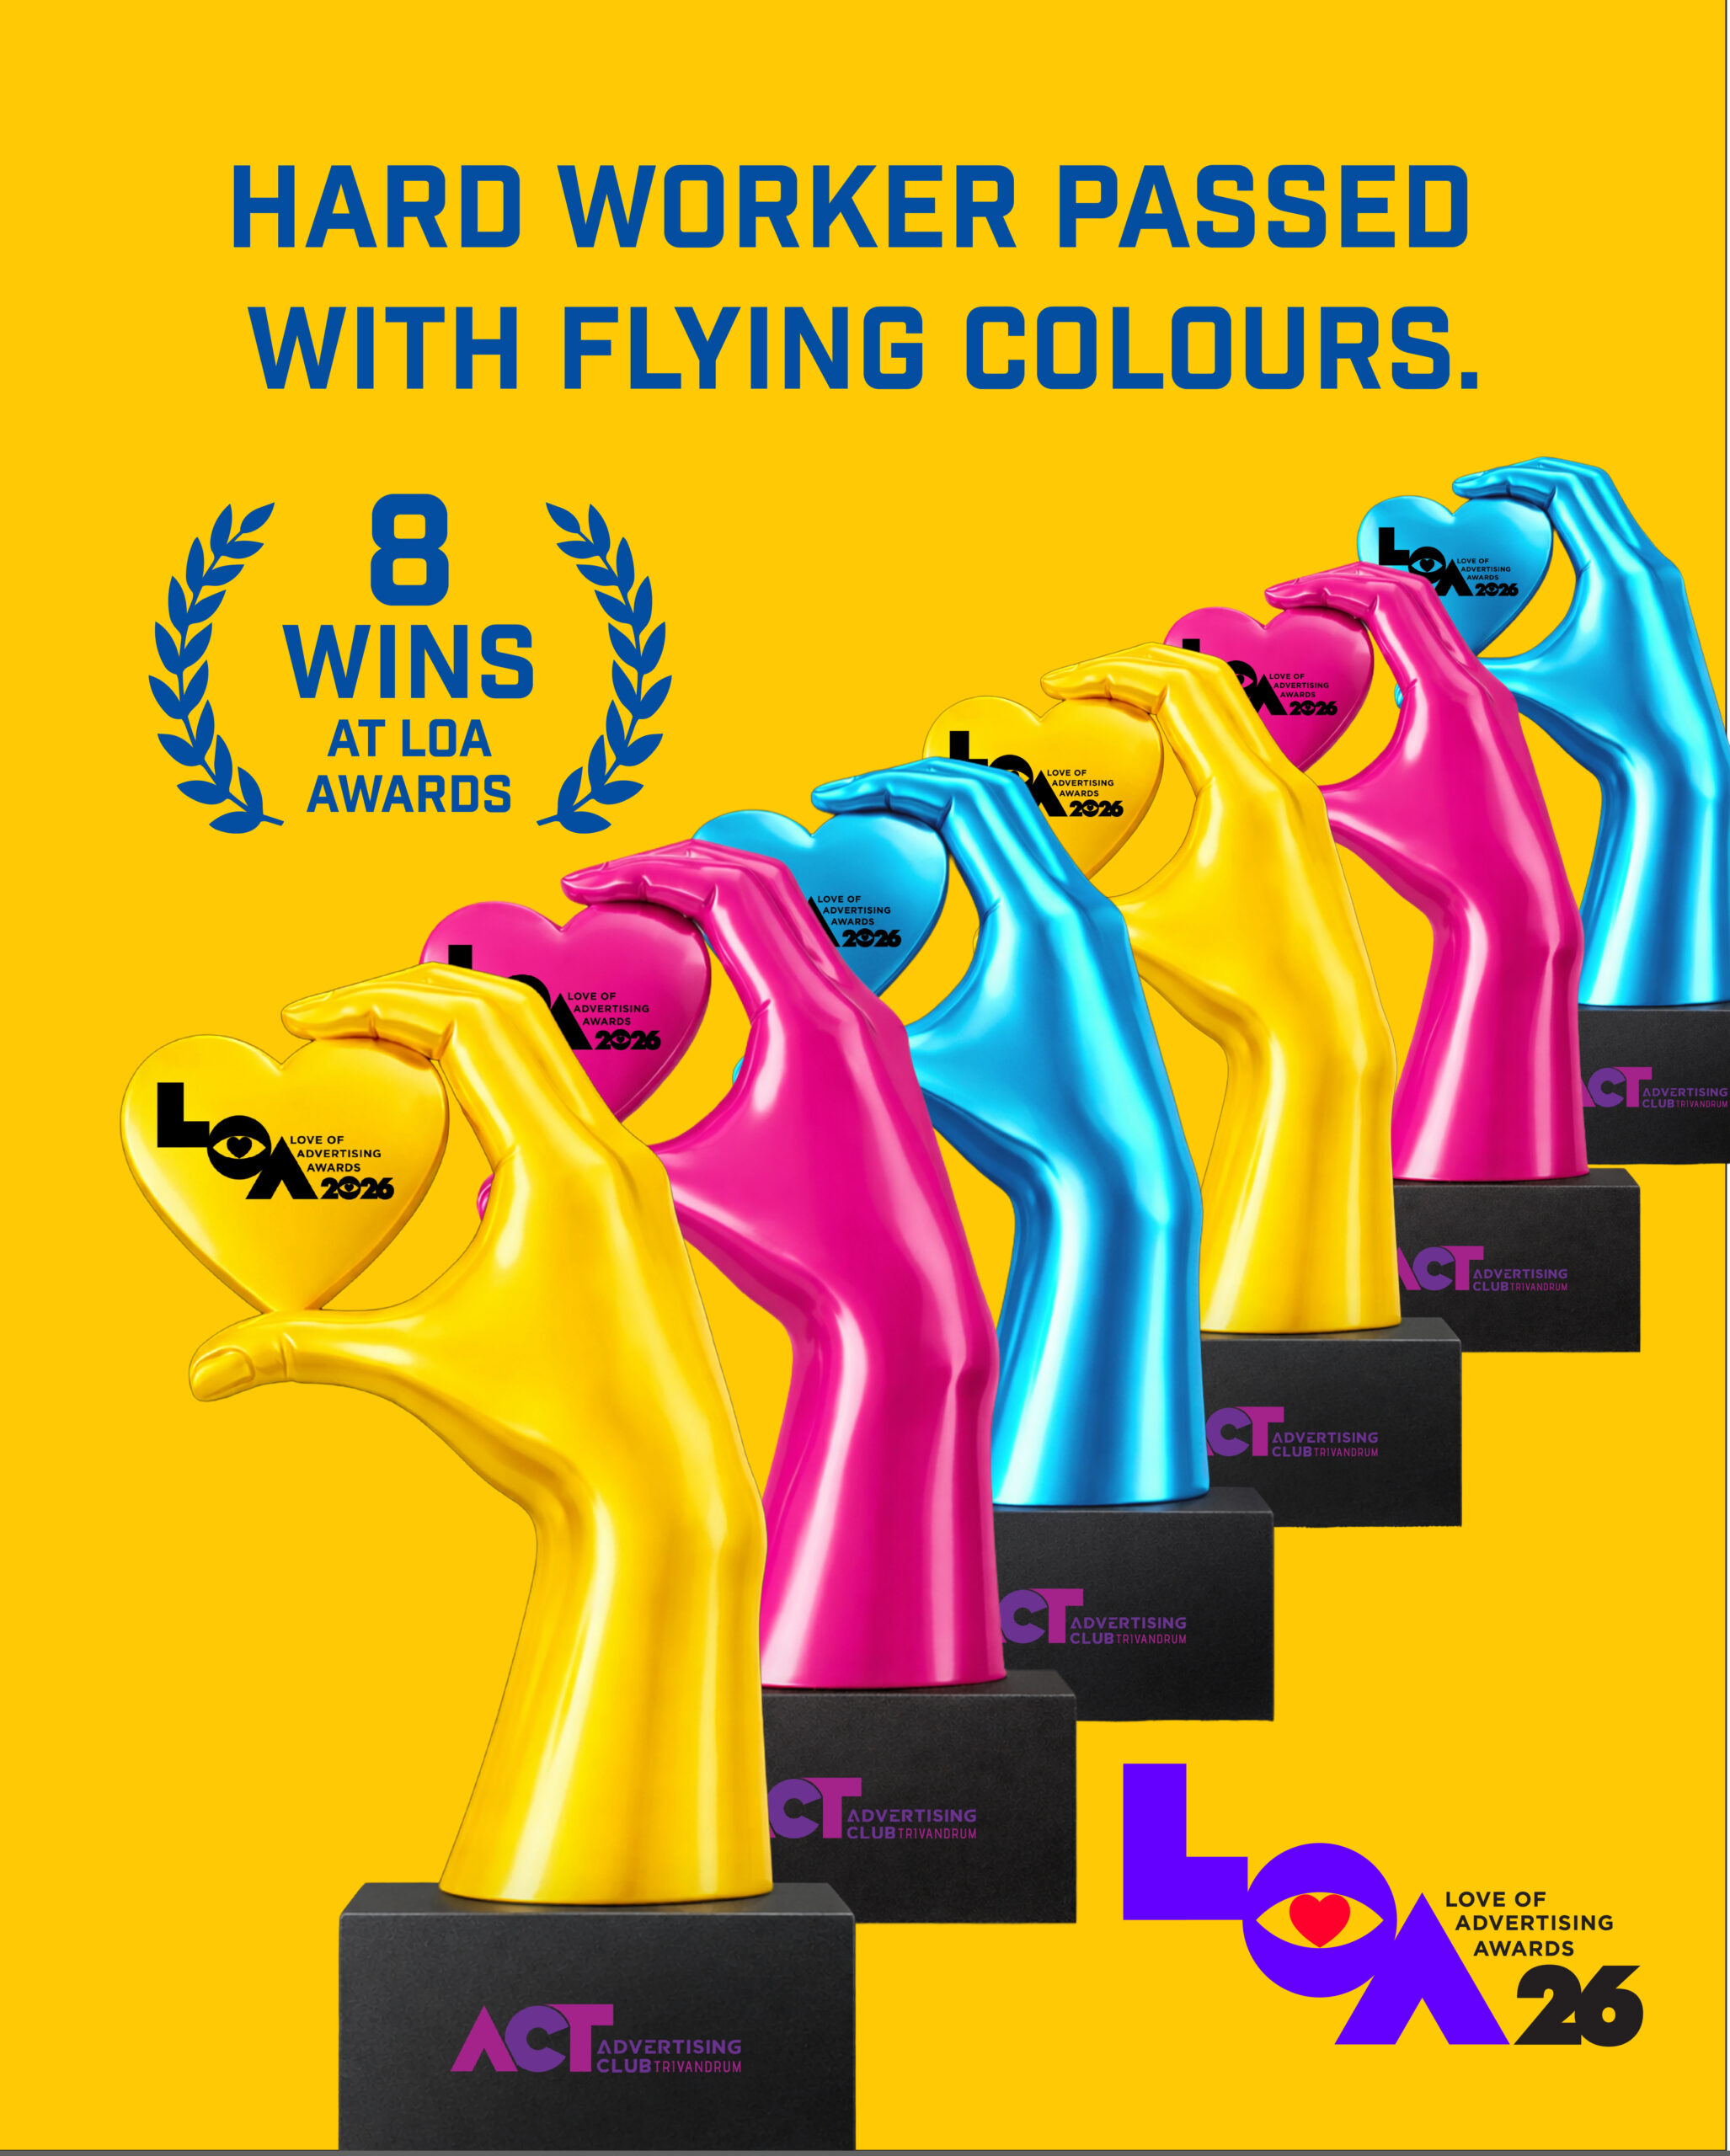
Ramco Cements’ Hard Worker Wins Eight Awards at ‘Love of Advertising Awards 2026’

Published

on

By

Shares

Ramco Cements’ Hard Worker brand wins eight awards for excellence in advertising, packaging and brand identity at the Love of Advertising Awards 2026.

Hyderabad 

The Ramco Cements Limited’s construction chemicals brand, Hard Worker, has secured eight awards at the Love of Advertising Awards 2026, recognising its creative excellence across television, digital advertising, packaging design and brand identity.

Organised by the Advertising Club of Trivandrum, the awards were presented at a ceremony held at The Leela Raviz, Kovalam, on 24 October 2026. The recognition highlights Hard Worker’s integrated marketing strategy and its efforts to establish a distinctive presence in India’s competitive construction chemicals market.

The eight awards span multiple creative categories, reflecting the brand’s approach to combining product-focused communication with engaging storytelling, humour and innovative design. Through its campaigns, Hard Worker has sought to simplify technical product benefits and make construction chemicals more accessible and relatable to consumers and construction professionals.

Built around the philosophy of “Hard-working products for hardworking people”, the brand focuses on communicating practical product advantages through memorable advertising narratives while maintaining a consistent identity across different marketing platforms.

Its campaigns for Ramco Hard Worker Eco Plaster and Tile Fix have been central to this approach. The Eco Plaster campaign highlights water conservation through the product’s self-curing properties, positioning it as a solution that supports more efficient construction practices. Meanwhile, Tile Fix promotes specialised tile-fixing solutions by presenting their practical benefits through relatable situations and creative storytelling.

Beyond advertising, Hard Worker has invested in distinctive packaging and brand identity development to improve product recognition and maintain consistency across customer touchpoints. This integrated approach has helped the brand differentiate itself in a category where marketing communication has traditionally focused on technical specifications and functional performance.

A V Dharmakrishnan, CEO, Ramco Cements, said, “Winning eight awards at the Love of Advertising Awards is a proud moment for Ramco Cements and the Hard Worker team. We believe that building a strong brand requires not only quality products but also the ability to communicate their value in a compelling and differentiated manner. Hard Worker’s journey reflects our commitment to combining product performance with innovative marketing to create meaningful connections with our customers and strengthen our presence in the construction chemicals market.”

The recognition comes as building materials manufacturers increasingly focus on brand differentiation, product awareness and customer engagement to strengthen their position in the construction chemicals segment.

By using humour and storytelling to explain product applications and benefits, Hard Worker aims to bridge the communication gap between technical construction solutions and the practical requirements of contractors, applicators and end-users.

Balaji K. Moorthy, Executive Director – Marketing, Ramco Cements, said, “Hard Worker was conceived to bring a fresh perspective to the construction chemicals category, where product communication has traditionally been functional and technical. Our endeavour has been to break through the clutter with distinctive ideas, humour and storytelling, while keeping the product proposition at the heart of every campaign. The recognition across TV and digital advertising, packaging design and brand identity design demonstrates our integrated approach to building the brand. These eight awards are an encouraging recognition of the creative thinking and collaborative effort behind Hard Worker’s marketing initiatives.”

The awards add to Hard Worker’s growing portfolio of creative recognitions and reinforce Ramco Cements’ emphasis on integrating product innovation with strategic marketing.

The brand’s communication initiatives also reflect a wider shift in the construction materials industry, where manufacturers are increasingly adopting consumer-focused marketing strategies to improve product understanding and strengthen relationships with construction professionals.

With its portfolio of construction chemicals, Hard Worker aims to address evolving requirements for durability, application efficiency and construction quality. Its marketing efforts seek to complement these product attributes by building stronger awareness and encouraging the adoption of specialised construction solutions.

Ramco Cements, one of India’s established cement manufacturers, operates across cement and allied building solutions. Through Hard Worker, the company is expanding its presence in the construction chemicals segment with products designed to enhance performance, quality and durability in modern construction applications.

The latest recognition strengthens Hard Worker’s brand visibility and underscores the growing importance of creative communication in promoting technical building materials. Ramco Cements intends to continue combining product development with distinctive marketing initiatives to support the brand’s growth in India’s construction chemicals market.

Continue Reading

Concrete

Shree Cement Expands Bangur Concrete Network with Patna Plant

New facility takes the company’s national RMC network to 36 plants

Published

on

By

Shares


Shree Cement has inaugurated a 60 m³/hour ready-mix concrete plant in Patna, Bihar, under its Bangur Concrete brand. The facility takes the company’s ready-mix concrete (RMC) network to 36 plants across India and strengthens its presence in eastern markets.

The plant was inaugurated by Neeraj Akhoury, managing director of Shree Cement, in the presence of senior company officials and other guests. It has been established to serve demand for ready-mix concrete in Patna and neighbouring areas, where infrastructure development, urban expansion and real estate activity are supporting construction growth.

The facility is designed to supply construction projects across Patna and surrounding markets. Its installed capacity of 60 m³/hour will enable Bangur Concrete to serve customers across the region while improving distribution and supply capabilities in eastern India.

The expansion is intended to improve customer service, strengthen the company’s market presence and support development activity in Bihar. The plant incorporates modern batching technology, material handling systems and quality control processes aimed at maintaining consistency in production and improving operational efficiency.

With the addition of the Patna facility, Bangur Concrete now operates 36 RMC plants across India. The business is expanding its footprint in key construction markets to improve customer access to ready-mix concrete, which is increasingly used in infrastructure, commercial and residential projects because it supports controlled production, consistent quality and more efficient material management at construction sites.

The facility will also follow environmentally responsible operating practices, in line with Shree Cement’s focus on sustainable construction solutions. The latest addition adds capacity to the company’s RMC operations and supports its efforts to serve regional construction markets as development activity continues across Bihar.

Continue Reading

Video Thumbnail
▶

    SIGN-UP FOR OUR GENERAL NEWSLETTER

    Trending News

    SUBSCRIBE TO THE NEWSLETTER


    Don't miss out on valuable insights and opportunities to connect with like minded professionals.


      This will close in 0 seconds